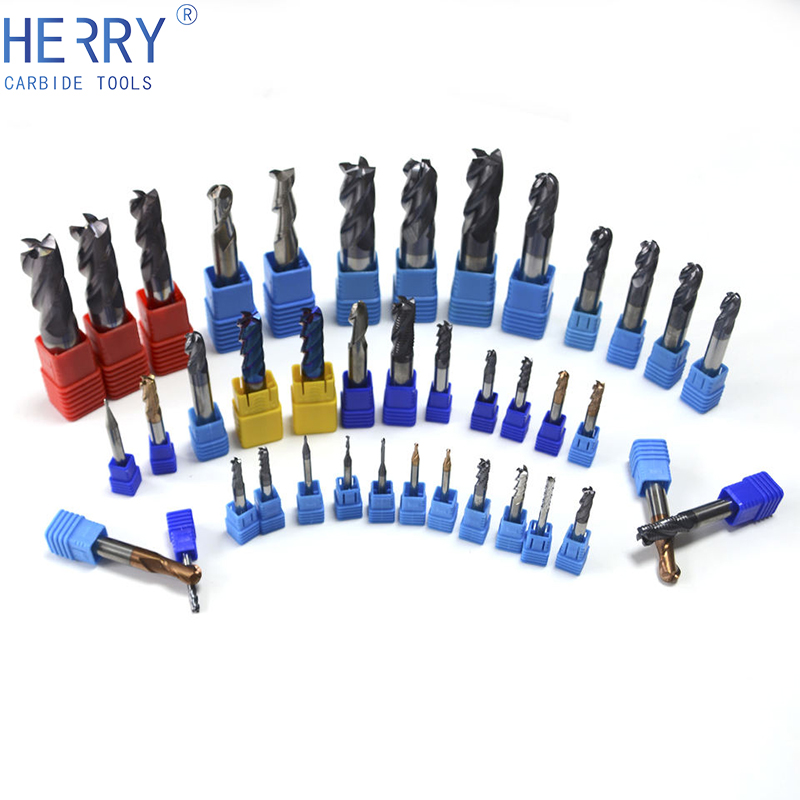
45 Degree - Cylinder Chamfer Kit - chamfer tool 45 degrees
Ferritic steels are made up of ferrite crystals, a form of iron which contains only a very small amount (up to 0.025%) of carbon. Ferrite absorbs such a small amount of carbon because of its body centred cubic crystal structure - one iron atom at each corner, and one in the middle. This central iron atom is what gives ferritic stainless steels their magnetic properties.
Austenitic microstructureformula
As iron cools, austenite crystals transition back into ferrite crystals, losing excess carbon which cannot be properly absorbed by the newly formed ferrite. The excess carbon creates patches of crystals with a mixture of low-carbon ferrite and leftover high-carbon cementite, and these mixed crystals are known as pearlite.
Austenite vs martensite
In UP milling, the direction of movement of workpiece and direction of rotation of the tool is opposite whereas in down milling the directions are same.
In UP milling, the thickness is varying from minimum at the beginning to the maximum towards the end whereas in Down Milling Operations the uncut chip thickness is varying from maximum at the beginning to the minimum towards the end.
When austenite cools, it generally reverts back to its ferrite form, which makes austenite difficult to utilise at anything below the extreme temperatures of a smelting furnace. Austenite can be forced to retain its crystal structure at low temperatures with the inclusion of chemical additives, such as the nickel and manganese found in many austenitic stainless steels.Austenitic stainless steels cannot be significantly hardened by heat treatment, but can be hardened by cold working. Austenitic stainless steels are widely used, particularly in stainless steel screws, due to their excellent resistance to corrosion.
Austenite composition
Martensitic stainless steels can be heat treated and hardened, but have reduced chemical resistance when compared to austenitic stainless steels. Martensitic stainless steel is often used when hardness is critical, such is in knives, where surface hardness creates a sharper blade.
In Up milling because of opposite direction, the tool is lifting the workpiece upwards, therefore strong work holding devices are required whereas in Down milling because of the same direction, forces are less and strong holding devices are not required.
In a Vertical milling machine, the axis of rotation of the spindle is Perpendicular to the table called a Vertical milling machine.
Austenite properties
The upward movement and the downward movement to the knee and the table can be given by means of elevating screw which is operated either manually or Automatic.
We use cookies to help give you the best experience on our site and to allow us and third parties to customise the marketing content you see across websites and social media. By clicking ‘Accept’ or continuing, you agree to our cookie policy.
These are cookies that are necessary for the Platform to function as well as to operate our business. These are used to let you login, stay logged in, measure our traffic (anonymously) and to ensure site security. Without this type of technology, our Services won't work properly or we won't be able to provide certain features and functionalities.
In case of down milling, because of the same direction, forces, power consumption, and tool wear are low and tool life is longer.
This video from Real Engineering does a great job of explaining how the crystalline structure of steel affects the physical properties of the material - the key points are discussed at 2:55:
Austenite phase
Martensitic stainless steel is formed by the creation of martensite. Martensite has been a key element of quenched steel for hundreds of years, but was officially named in the 20th century after the metallurgist Adolf Martens (1850 - 1914).
Austenite formula
It is a multi-point cutting tool machining operation used for removing a layer of material from the complete surface of the workpiece and it is also used for producing holes in the components.
4. Straddle Milling Cutter: In addition to the periphery, if the cutting teeth are provided on faces also called aa s straddle milling cutter. i.e. End milling cutter is superimposed on to the peripheral milling cutter.
These are cookies that are used for collecting information to manage our advertising. We implement Consent Mode to store cookies related to advertising, set consent for personalised advertising, and send user data to advertisers.
When peripheral milling cutter is used for performing the Milling Operation there are two methods of milling will be used.
If the Milling Operation is used for removing a layer of material from a complete surface of the workpiece is called a face Milling Operations.
The vast majority of metals have a crystalline structure in their solid state, meaning that they are made up of crystallised lattice structures of atoms. By definition, all steels, including stainless steels, are primarily made up of crystallised iron atoms with the addition of carbon. The iron in steel can exist in several different crystalline structures, dependent on the conditions of its creation. Ferrite, austenite, and martensite are all examples of iron’s crystal structures, and all are found within different types of steel. One of the defining differences between these crystal structures is the amount of carbon they can absorb - a greater carbon content generally, though not always, makes a steel harder, but more brittle.
Austenitic microstructurewikipedia
2.Peripheral Mill Cutter: if the cutting teeth are provided around the periphery of a circular disc called as a peripheral milling cutter.
Because of large uncut chip thickness at the end, the surface finish produced is poor in Up Milling whereas in Down Milling because of the small uncut chip thickness at the end, the surface finish is better.
The arbor is a machined shaft that holds and drives the cutters. The arbor support is fitted to the Overarm and can be clamped at any location. Its function is to support various arbors.
The column is the main supporting frame mounted vertically on one side of the base which is box-shaped and has all the mechanisms inside it for the spindle and table feed.
5.Gang Milling Cutter: If a gang of peripheral milling cutters of different sizes is kept together for removing the material simultaneously from one workpiece called a Gang Milling Cutter.
3.Side Milling Cutter: In addition to the face, if the cutting teeth are provided on periphery also called as a Side Milling Cutter.
Please note: The shipping options listed below are for the expedition of transit only. Lead times and manufacture schedules for out-of-stock products will still apply. Accurate delivery date estimates are always displayed during the checkout process.
While the information below covers ferritic, austenitic, and martensitic steels, almost all of Accu's stainless steel components have an austenitic crystalline structure. For more specific information on exact austenitic steel grades, please see our article on the many different grades of austenitic stainless steel.
1.End Milling Cutter: If the cutting teeth are provided at the end face of the circular disc, it is called an End milling cutter. End mill cutter is used either with a vertical milling machine or by using drilling machine also.
These are cookies that are used for collecting information about how you use our Services and visit our Platform (i.e. duration of your navigation on our Platform, pages visited, link clicked, referrer page, etc).
Martensite is a body centred cubic form of crystallised iron which is created when heated austenite is rapidly cooled by quenching. The increased rate at which Martensite crystals are created prevents cementite from being formed, and causes carbon atoms to become unnaturally trapped in crystals which would ordinarily expel excess carbon during gradual cooling.
It provides support to all the parts of the machine and which can absorb the vibrations induced during milling operation and also acts as a reservoir for the cutting fluids.
Ferritic stainless steels are less widely-used due to their limited corrosion resistance and average strength and hardness.
Austenite
In a horizontal milling machine, the axis of rotation of the spindle is horizontal to the table it is called a horizontal milling machine.
Austenitic stainless steels contain austenite, a form of iron which can absorb more carbon than ferrite. Austenite is created by heating ferrite to 912 degrees C, at which point it transitions from a body centred cubic crystal structure to a face centred cubic crystal structure. Face centred cubic structures can absorb up to 2% carbon.
In general, both the types of milling operations will be performed by using both the type of milling cutters but it is preferable to perform face Milling Operation with end mill cutter and slab Milling Operations with a peripheral milling cutter.
In UP milling, because of the opposite direction, the forces, power consumption, and tool wear are high whereas tool life is low.
As a liquid, molten iron is not crystalline, and crystals are only formed when the material cools. When the material cools, steel solidifies as individual crystals forming gradually, which can mean that any one type of steel is actually made up of several crystal types as the metal slowly forms crystals through multiple temperature stages. This means that regardless of their defining crystal structure, it is not uncommon for steels to contain small mixed amounts of ferrite, austenite, and cementite.
Cementite is a form of iron which contains even more carbon than ferrite and austenite. Cementite contains up to 6.67% carbon. Because of its increased carbon content, cementite is hard and brittle, and its presence is usually a byproduct, rather than by design. Cementite commonly occurs in steels when excess carbon, such as left-over carbon which cannot be absorbed into ferrite, must be used for the formation of crystals.
 18581906093