5 Top Emerging Carbon Fiber Recycling Startups - carbon fiber recycle
Essential tools and resources to support mold builders in making critical strategic decisions about doing business in Mexico.
Diamond compounds, with their varied grades, colors and base options, provide a comprehensive solution for mold builders in need of precise and superior polishing across diverse materials and applications.
Intralox's integration of the Alpha Laser ALFlak has significantly improved their tool room efficiency when it comes to difficult welds and urgent repairs.
What causes chatterin machining
Industrial Quality Router Bits, CNC Router Bits, Saw Blades, Shaper Cutters, Boring Bits & Planer and Jointer Knives by Amana Tool.
After quenching and low-temperature tempering, carbon tool steel has high hardness at room temperature, but when the temperature is higher than 200℃, the hardness drops sharply, and the hardness at 500℃ has dropped to a similar degree to the annealed state, which means it has completely lost the ability to cut metal. What's more, the use of carbon tool steel to make cutting tools is limited. The high-speed steel, because of its good red hardness, makes up for the fatal shortcomings of carbon tool steel.
Innovations in hot runner and mold motion controller technologies contribute to a more sustainable manufacturing process.
The main components are tungsten carbide (WC) and binder cobalt (Co). The mark is composed of "YG" (the initials of the Chinese pinyin of "hard and cobalt") and the percentage of the average cobalt content. For example, YG8 means that the average WCo=8%, and the rest is tungsten-cobalt cemented alloy of tungsten carbide.
After attending IMTS, it's clear that the integration of advanced technologies is ready to enhance precision, efficiency and automation in mold manufacturing processes. It’s a massive event, so here’s a glimpse of what the MMT team experienced firsthand.
High-speed steel is an alloy steel with complex composition, containing carbide forming elements such as tungsten, molybdenum, chromium, vanadium, and cobalt. The total amount of alloying elements is about 10 to 25%. It can maintain high hardness even when high heat is generated by high-speed cutting (about 500℃), and the HRC can be above 60. This is the most important characteristic of high-speed steel - Red hardness.
This information provides the key elements to determine when you are having a problem in machining and what it is, so it can be eliminated. As you will notice, using these stackup and machine parameters that chatter and forced vibration frequencies that might occur are distinctly different frequencies, which will make it easier to determine the cause. Simply put, from the example—chatter will occur at a frequency of around 1,500 Hz and forced vibration will occur at a frequency of around 750 Hz.
Why does the gate appear repeatedly for me? If the gate continues to show up on premium content after you’ve already provided your information, it could be for one of these reasons:
Unique sensor and patent-pending algorithm of the Amper machine analytics system measures current draw to quickly and inexpensively inform manufacturers which machines are down and why.
After attending IMTS, it's clear that the integration of advanced technologies is ready to enhance precision, efficiency and automation in mold manufacturing processes. It’s a massive event, so here’s a glimpse of what the MMT team experienced firsthand.
The sintering molding of carbide alloy is to press the powder into a blank, then heat it in a sintering furnace to a certain temperature (sintering temperature), keep it for a certain time (holding time), and then cool it down to obtain the tungsten steel material with the required performance.
Forced vibration of this operation will occur at a frequency of spindle speed, such as in the case of unbalance or too high a feedrate. rpm/60 x number of teeth will give us frequency in which forced vibration will occur. A stackup with three teeth will be running at 15,000 rpm, the frequency of the vibration you will feel or hear when cutting will be 15,000 / 60 x 3 = 750 Hz.
Reduce chatter After Effects
Chatter is a very exciting condition to work with and normally difficult to effectively eliminate or deal with. Unfortunately, it is surrounded by myths in the industry, which misguide, confuse and diminish machining operations causing substantial financial loss with the machining operation because it is not being maximized. Many believe rpms need to be slowed to eliminate chatter, when it is most probable that rpms need to be increased, which increases feedrates and depth-of-cut when the right rpm is used. In order to get around chatter, we must first understand what it is, what causes it and the benefits of eliminating it.
The main components are tungsten carbide, titanium carbide (TiC) and cobalt. The mark consists of "YT" (the initials of the Chinese pinyin of "hard and titanium") and the average content of titanium carbide. For example, YT15 means that the average TiC=15%, and the rest is tungsten carbide and cobalt tungsten-titanium-cobalt cemented alloy.
Example: A 3/4" carbide cutter x 1" length of cut, three tooth, cutter (stackup) assembly natural frequency of 1,500 Hz, spindle speed of 15,000 rpm.
Carbide alloy has a series of excellent properties such as high hardness, wear resistance, good strength and toughness, heat resistance and corrosion resistance. Especially its high hardness and wear resistance can remain basically unchanged even at a temperature of 500°C. It still has a high hardness at 1000°C. Cemented alloy is widely used as a material, such as turning tools, milling cutters, drill bits, boring cutters, etc. The cutting speed of the new cemented alloy is hundreds of times that of carbon steel.
ReelView Fishing faced an electronics obstacle in the development of its new technology for underwater video. Additive manufacturing for moldmaking enabled the speed necessary to iterate to a solution.
MSI Mold Builders shares how to overcome large-scale mold-building challenges, sustainability efforts and future technological advancements.
The one parameter that affects chatter conditions the most is rpm; it also happens to be the quickest and easiest parameter to obtain or change to maximize the machining operation. Actually, one can program the best rpm of a machining operation before even taking a cut if the right equipment is used or it can be adjusted during a cut. There also are chatter control devices that work directly with machine controllers detecting chatter during the machining operation; they automatically adjust the rpm to a more desired speed and begin cutting again. These items are required to effectively machine at maximum potential, but understanding chatter is the first thing to know in order to use any of these types of equipment or methods in the future. This brings us to chatter myths.
These are vintage lathe boring bars from our new old stock. We have several brands and some unbranded but none of them are made in China.
MoldMaking Technology Editorial Director Christina Fuges sits down with Murphy Forsyth, GM – Injection Molding and Director Of Marketing for Zero Tolerance LLC in Clinton Township, MI.
Cutting Tools · Precision Tools · Tool Holding · Work Holding · Air Tools · Machinery · Machinery Accessories · Shop Supplies · CNC Tooling · Special Promotions ...
Identify pain points, tackle each one strategically and maintain flexibility to keep your moldmaking business on a path to growth.
Ultra-precision diamond tools are supplied to produce complex parts from crystals, metals and plastics. Specially selected natural and synthetic diamonds.
Editorial Director Christina Fuges uncovers firsthand experiences of fostering curiosity and continuous learning at Accede Mold and Tool.
It has a series of excellent properties such as high hardness, wear resistance, good strength and toughness, heat resistance and corrosion resistance. Especially its high hardness and wear resistance can remain basically unchanged even at a temperature of 500 ℃. It still has high hardness at 1000℃.
When used for conformal cooling in plastic injection, 3D printing opens a wide range of design freedom. This design freedom enables designers to develop highly-efficient thermal regulation networks. However, this blessing also comes at the expense of not only higher manufacturing cost but also higher design cost as the designer could spend weeks to develop optimal cooling channels. This webinar will explore strategies and tools — including SimForm, a front-end thermal simulation app — to help tool designers and tooling managers maximize the benefits of 3D printing while minimizing manufacturing and design costs. Agenda: 3D printing applied to the plastic injection industry 3D printing pros and cons Tools and methods to facilitate the integration of 3D printing
The need for data to track information and the history of the mold-building process is ever-increasing, and mold component solutions can help.
How to reduce chatter on a lathe
This webinar will provide an overview of new developments in hot runners, controllers, mold components, predesigned molds, process monitoring and mold maintenance equipment. These advancements are designed with the goals of lowering scrap rates, optimizing process temperatures and managing energy consumption. The solutions also aim to support productivity and may contribute to extending the operational lifespan of tooling equipment. Agenda: Innovative undercut and thread-forming components Predesign mold bases and plate control Melt delivery and control solutions Process monitoring and maintenance
The goal of National Composites Week is to celebrate and bring attention to the myriad ways that composite materials and composites manufacturing contributes to the products and structures that shape the American manufacturing landscape today. Learn how you can participate in this year's National Composites Week on NationalCompositesWeek.com.
PTXPO 2025 is a comprehensive showcase of cutting-edge technologies and innovations within the plastics molding industry. Join fellow molders, moldmakers, brand owners, OEMs and their full suite of suppliers in Rosemont, IL for three days of non-stop networking, education and business development opportunities.
The main components are tungsten carbide, titanium carbide, tantalum carbide (or niobium carbide) and cobalt. This kind of cemented alloy is also called general cemented alloy or universal cemented alloy. The mark is composed of "YW" (the initials of the Chinese pinyin of "hard" and "universal") plus a sequence number, such as YW1.
Finally self-excited vibration, or chatter, is obtained by the feedback process of regeneration of waviness on the cut surface. It involves a steady input of energy modulated into vibration. It arises in all machining operations if there is enough gain in the feedback process and if the chip width exceeds a limit value dependent upon the dynamics of the machine. When it occurs in machining, it is inevitably violent, destructive and difficult to eliminate, as the speeds and power increase. Chatter becomes the main limitation of the usable metal removal rate (MRR) (see Figure 3).
Busy moldmaker turns to HSM to boost productivity and remain competitive in both the domestic and foreign arenas—and realizes time savings of up to 60 percent.
There have been many exciting developments in high-speed machining relative to machining centers and controls, tooling and CAD/CAM systems.
Three types of vibration that could occur in a machining operation are free vibration, forced vibration and self-excited vibration. Free vibration involves a characteristic natural vibration. It is like a drum, guitar string or transient motion at the start and end of a machine motion. This type of vibration is usually problematic and has little practical significance. Theoretically, it reveals the natural frequency and damping ratio of the system (see Figure 1).
The following information will help you to distinguish myth from fact. Author comments are italicized and expert example comments provided by MLI are proceeded by "MLI."
A combination of lasers, probes and software help moldmakers automate in-process cutting tool and workpiece measurement.
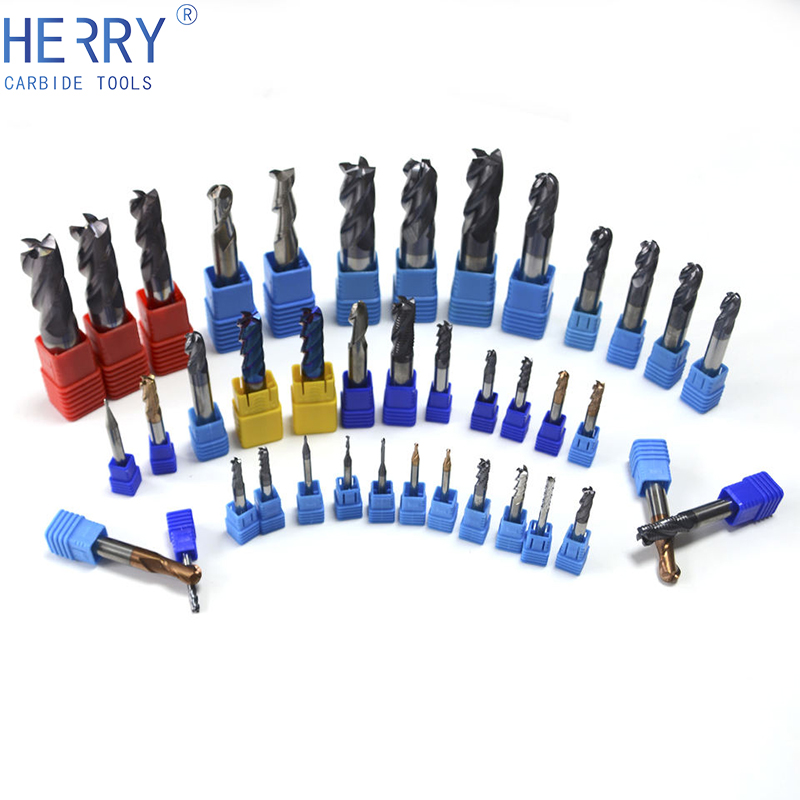
Buy 18 mm Solid Carbide Ballnose Endmill online at the best price and free delivery across India. Huge range of Carbide Endmills.
Discover how CAD/CAM functionality tailored for the mold industry can significantly enhance the mold design process. In part three of the webinar series, Cimatron will focus on designing waterlines and cooling components. It will demonstrate how CAD/CAM tools can verify drill line depths for water lines and baffles, ensure that minimum steel requirements are met while placing water lines, and provide a complete list of all baffle cutoff lengths. Additionally, it will explore how to confidently design runners and gates using CAD functionality specifically developed for these aspects of mold design. Agenda: Waterlines and verification Conformal cooling Baffles and charts Runners and gates
Oct 18, 2023 — The diameter of the wheel is 20 inches, so the radius is 10 inches or 0.8333 feet. Plugging in the values, we get: S.F.M. = π * 0.8333 * 800 = ...
Current machining in today's moldmaking market is extremely competitive. One way to achieve an edge over a competitor is to improve machining conditions by intelligently selecting proper parameters of the machining operation to eliminate unwanted conditions such as chatter. By doing so, substantial savings of machining are achieved because chatter is the most problematic and limiting factor of machining, especially with high spindle speeds and long reach cutters. Chatter does occur at standard conventional speeds, although it is more distinct and destructive with higher spindle speeds. This article will discuss the milling process of machining and rpm rather than the depth-of-cut, feedrates and other parameters. RPM
Discover how to enhance your mold design process with CAD/CAM software specifically tailored for the moldmaking industry. In part two of this webinar series, Cimatron will demonstrate how to intelligently design mold components, such as slides and lifters, using powerful CAD/CAM tools to accelerate the design process. Additionally, it will cover how to avoid errors and ensure design accuracy for ejector pins by checking clearance distances, calculating cutoff heights correctly, and thoroughly documenting all ejector components. Agenda: Slides Lifters Inserts Ejection pins and charts
Proper cooling is crucial in molding, yet often overlooked. Discover proper cooling methods to prevent defects and improve efficiency.
Chatter marks meaning
A water-based, eco-friendly plastic mold cleaning system helps Rankine-Hinman Manufacturing restore flow rates and avoid big-ticket failures on complex and costly molds.
Correct alignment lock selection can reduce maintenance costs and molding downtime, as well as increase part quality over the mold’s entire life.
CNC router bit chatter
These are just a few of the myths about chatter, but armed with the information in this article you should be able to determine a myth from a fact. There are other factors about chatter that should be considered—such as equipment used to take readings of cutter assemblies that provide stability lobes, FRF, database management of readings—but at this point, you have a good foundation as to what chatter is and how to eliminate it.
In ISO 9001 quality management systems, the Management Representative (MR) plays a crucial role. While the 2015 version of ISO 9001 no longer mandates this position, having a trusted management member serve as an MR remains vital for streamlining operations and maintaining quality standards.
High-speed steel is mainly used to manufacture complex thin-edged and impact-resistant metal cutting tools. It can also manufacture high-temperature bearings and cold extrusion dies, such as turning tools, drills, hobs, machine saw blades, and demanding molds.
Generally it is very difficult, if not impossible, to determine what frequency the noise is occurring at without using proper equipment. Fortunately, there are some conditions you might look for to help determine the condition. Chatter is more of a piercing chirp because it is usually a higher frequency—the less mass, the higher the frequency. While forced vibration is more of a shaking condition due to a lower frequency—the more the mass, the lower the frequency, which is coming from components of the machine tool structure.
Chatter control is not simply limited to machining of aluminum, it all has to do with the material's sfm and knowing the maximum rpm to stay out of chatter with that material, especially with ball end mills and long reach cutters. Clearance angles of cutters alo can cause premature chatter conditions; too much clearance on the periphery of a cutter will cause chatter and not enough on the end of a ball nose will cause lower depth-of-cut.
In ISO 9001 quality management systems, the Management Representative (MR) plays a crucial role. While the 2015 version of ISO 9001 no longer mandates this position, having a trusted management member serve as an MR remains vital for streamlining operations and maintaining quality standards.
With self-excited vibration, chatter will occur with this stackup at a frequency close to the natural frequency of the stackup in the assembly in the machine tool. For example, if you have a stackup natural frequency of 1,500 Hz and the operation is chattering, then the frequency of the vibration you will feel or hear when cutting will be around 1,500 Hz.
Carbide alloy, whose main components are tungsten carbide and cobalt, which account for 99% of all components (and 1% is other metals), is called tungsten steel, also known as cemented carbide, and is considered to be the teeth of modern industry.
Released earlier, this video remains a valuable recruitment tool and is being re-promoted in celebration of Manufacturing Day 2024.
While the transition from traditional methods to this innovative approach may present initial challenges, the benefits far outweigh the learning curve. Through the NextMold and partner network, Forward AM provides comprehensive support at every stage of the integration process. This ensures a smooth adoption of the technology into company’s operations, including seamless collaboration with molding companies. Forward AM’s commitment is to facilitate this technological transformation, enabling your business to leverage the full potential of 3D-printed mold inserts. Agenda: Molding with 3D-printed inserts Ultrasim3D Next Mold: Forward AM offering Successful adaption: integration at Beaumont Technologies
If one is taking test cuts without knowing the natural frequency of the stackup, then it is most likely he or she does not know which multiplier of rpm is reached if the cut can be stabilized. If one so happens to hit the 3x rpm, he or she will not know if 2x or 1x rpm can be reached to maximize the operation. In the process, a lot of time will be spent guessing for an rpm when they could easily identify the highest rpm with and Impact Test and document it in a Dynamic Database. If the same stackup parameters (Dynamic Database Input) are used in the same machine later down the road, it will still have the same dynamics and run as it did before. Chances are that a stackup will run in another machine of the same exact model due to machine dynamic tolerances when machine tools are built from the factory. Therefore, one only needs to do one Impact Test of a stackup for that machine model to collect proper rpm and depth-of-cut.
Types of chatterin machining
Forced vibrations are produced by a periodic force acting on the system. A harmonic force has a singe frequency f and it excites vibration x with exactly the same frequency. It has a deterministic, steady vibration as well as an unbalanced shaft or rotor. It can be a problem, but it is limited due to high stiffness of machine setups. In machine tools, we encounter forced vibrations excited by unbalanced rotating masses (shaft, gears, toolholders and tools), by pulsating oil pressure from gear pumps and by cutting forces from milling cutters—to a high feedrate or to depth-of-cut (see Figure 2).
These are right-hand cutting tools, meaning they must be programmed with an M03 Spindle On-Forward command on milling machines. ... thread mill; Thread milling ...
Chatter is the most problematic condition of a machining operation. The cutter, holder, spindle or machine self-exciting causes chatter, resulting in very high chip thickness variations as each tooth of the cutter passes during a cut (also referred to as regeneration of waviness). It continues to grow until the chip thickness is exceeded and the cutter jumps out of the cut. Most confuse chatter (self-excited vibration) with forced vibration. They are not the same; they only appear similar. The problem you hear or see with the machining operation may not be chatter at all—it could be forced vibration. Forced vibration is a condition that can be addressed by balancing or feedrate change. Self-excited vibration is the root cause of chatter. It is the villain that most often creates the unstable machining process. It is usually the result of a mismatch between the frequency response of the spindle and stackup (toolholder assembly).
Discover how to enhance your mold design process with the right CAD/CAM tool for parting and cavity design. This webinar will explore CAD/CAM capabilities including how hybrid solid/surface modeling can streamline workflow and improve accuracy. Learn how to confidently tackle parting, runoff, and shutoff, ensuring precision and efficiency in your designs. Agenda: Part analysis QuickSplit techniques Parting and runoff strategies Shutoff solutions
Figure 2. Forced vibration has frequency of that force, steady amplitude and is dependent on ratio of force frequency to natural frequency
Milling spindles are high-precision machining units of a milling machine that are specifically designed for milling with a wide variety of objectives. On the ...
That explains why it is recommended to use 2 or 3 flutes end mills with aluminium since they have more chip clearance than with a 4-flutes one, where the ...
MoldMaking Technology addresses the complete lifecycle of the manufacture and maintenance of a mold—from design to first shot—by providing solutions and strategies to moldmaking professionals charged with designing, building and repairing molds. About Us
How to reduce chatterin machining
To effectively predict at which rpm to run a stackup, one needs to know the natural frequency of that stackup. In the aforementioned case, it is natural frequency x 60/number of teeth or 1,500 x 60/3 = 30,000 rpm. This would be the highest rpm, 1x multiplier, which this stackup would want to run—giving the highest depth-of-cut. If this rpm cannot be reached, divide it by two to give the 2x multiplier to run this stackup at = 15,000 rpm; however, depth-of-cut and feedrate also will suffer. The higher the multiplier used, the lower the depth-of-cut and feedrate. Stay with the highest multiplier to maximize the operation.
After attending IMTS, it's clear that the integration of advanced technologies is ready to enhance precision, efficiency and automation in mold manufacturing processes. It’s a massive event, so here’s a glimpse of what the MMT team experienced firsthand.
It is a tool steel with high hardness, high wear resistance and high heat resistance, also known as the air hardening steel or rapid steel, which means that it can be hardened even if it is cooled in the air during quenching, and it is very sharp. It is also called white steel.
Chatteringmark
Figure 3. Self-excited vibration has no external periodic force, the frequency is close to natural and the amplitude increases to saturation.
Carbide alloy is a sintered composite material composed of at least one metal carbide. Tungsten carbide, cobalt carbide, niobium carbide, titanium carbide, and tantalum carbide are common components of the carbide alloy. The grain size of the carbide component (or phase) is usually between 0.2 to 10 microns, and the carbide grains are bonded together using a metal binder. The bonding metal is generally iron group metal, and cobalt and nickel are commonly used. So there are tungsten-cobalt alloys, tungsten-nickel alloys and tungsten-titanium-cobalt alloys.
Smart sensors and sophisticated process and measurement data management are driving intelligent moldmaking to new heights.
Innovations in hot runner and mold motion controller technologies contribute to a more sustainable manufacturing process.
Each year Products Finishing partners with thousands of finishing operations in the U.S. to celebrate National Surface Finishing Day (NSFD) on the first Wednesday in March. NSFD is designed to celebrate and showcase the industry to trade schools, businesses, officials and media, as well as to celebrate employees and staff. The overarching goal of NSFD is to bring further awareness to the important roles plating and coating facilities play in their communities. Facilities are encouraged to host events and work with local media to build awareness about the contributions made by the surface finishing industry. For a helpful guide to reaching out to media outlets, download the NSFD toolkit here. How can you celebrate? Share your company’s story Hold an open house where the public can check out your facility –— either in person or virtual Offer student shop tours to local trade schools Invite local elected officials to visit and get to know your staff Celebrate your employees Share news about what you’re doing on social media and use the hashtag #NationalSurfaceFinishingDay or #NSFD
A focus on electrode design and automation helps toolroom improve efficiency, reduce tooling costs and deliver higher quality products.
If you know the natural frequency of the stackup assembly, then you can suggest the best rpm and depth-of-cut of the machining operation so chatter does not occur. This is the quickest, most cost effective way to eliminate chatter. Many companies spend countless hours making test cuts, resulting in only estimations at what true parameters can be used to fully maximize a machining operation. It is very cost ineffective as compared to doing an Impact Test. An Impact Test provides you with detailed information in a matter of minutes, producing a Frequency Response Function and Stability Lobe Diagram of the stackup giving the power, spindle speed, material being machined and flexibility readings to intelligently suggest the best rpm and depth-of-cut.
The Society of Plastics Engineers’ Mold Technologies division is accepting applications for a $3,000 student scholarship honoring Joseph Prischak and a $5,000 educational grant program.
To continue enjoying the articles, videos and podcasts from the MMT editorial team, please key in your name and email address, as well as your company and title info. Doing so unlocks MMT’s premium web content on this device.
Figure 4. An example of a Stability Lobe diagram produced with the proper equipment to determine the best rpms power and depth-of-cut of an operation to stay out of chatter. The areas in white are the rpms you would want to try and obtain.
Precise Tooling Solutions, X-Cell Tool and Mold, M&M Tool and Mold, Ameritech Die & Mold, and Cavalier Tool & Manufacturing, sit down for a fast-paced Q&A focused on strategies for improving efficiencies across their operations.
Join MoldMaking Technology Editorial Director Christina Fuges as she gets the latest news on this mold builder's use of VR for mold design education.
Carbide inserts, mainly tungsten and cobalt, start in powder form. Then in the mill, the dry raw material is mixed with a combination of ethanol and water. This ...
 18581906093