5 Ways To Fix a Screw That Has Stripped Out - bored out hole
If you are a CNC programmer, you know that feed rate and spindle speed are two important parameters that affect the quality of your machined parts. But do you know how they work and how to optimize them for different materials and tools? In this article, we will explain the difference between feed rate and spindle speed, and how they affect the surface finish and dimensional accuracy of CNC machined parts.
The depth that the toolisplunged into the surfaceiscalled as
Please keep in mind that tool reservations can only be made at least 2 weeks in advance. Proper Laser Cutter Operations on MyLearning.com under MyJH is ...
Whichofthe following codeisused to specify coolant on
In wood working... We use feed rate, rpm and number of flutes or cutting edges to calculate 'chip load'. Proper chip load keeps tooling cooler/lasting longer and lowers stress on the 'machine' all while improving cut quality.... See the tooling geometry section of this article below for much more accurate information on this topic.
For CNC machining skilled part programmers are needed
Spindle speed is the rotational speed of the cutting tool. It is usually measured in revolutions per minute (RPM) or surface feet per minute (SFM). Spindle speed determines how fast the cutting edges of the tool contact the workpiece, and how much force is applied on the material. A higher spindle speed means more cutting edges per unit of time, but also more vibration and noise, which can affect the dimensional accuracy and the surface finish. A lower spindle speed means fewer cutting edges per unit of time, but also less vibration and noise, which can improve the dimensional accuracy and the surface finish.
Free Stainless Steel - 303, 410,. 416, 440F. -250. 275-350. All4. FeinAL, TiXCo4 ... HSS Endmills Reduce SFM 50%. With coating, add 10% to the SFPM.
G codes are also known as
The harmonics of the machine also play a roll in surface finish. I have had a machine that leaves better surface finish at 12k RPM than at 10k because the harmonics of the spindle was smoother. You can feel this by placing your hand on the machine running the spindle, with the finishing tool, at different RPM to find out where it’s the smoothest.
The optimal feed rate and spindle speed depend on the material properties of the workpiece and the tool. Different materials have different hardness, strength, ductility, and thermal conductivity, which affect how they react to the cutting forces and heat. For example, harder materials require lower feed rates and higher spindle speeds to avoid excessive tool wear and chipping. Softer materials require higher feed rates and lower spindle speeds to avoid excessive heat and deformation.
Feed rate is the speed at which the cutting tool moves along the workpiece. It is usually measured in inches per minute (IPM) or millimeters per minute (MM/MIN). Feed rate determines how much material is removed per unit of time, and how much heat is generated by the cutting process. A higher feed rate means faster material removal, but also more heat and friction, which can degrade the tool life and the surface quality. A lower feed rate means slower material removal, but also less heat and friction, which can improve the tool life and the surface quality.
To use your 3D printer with Implant Studio you will need to establish the integration through the Formlabs 2 option.
Surface finish is impacted by several issues, thus 1-material to be machined 2-speed 3-feed 4-depth of cut 5-cooling lubricant 6-tool geometry Some hard material like chrome when being machined with ceramic inserts would require high speed (ceramic inserts cut better and last longer with more heat emanating from friction), same material when cut using ni- hard/amborite inserts would require slower speeds for better finish ....softer material like copper would require both high speed and high feed and oil based lubricant for better finish so it all boils down to a combination of a variety of factors.
InCNC systems multiple microprocessors and programmable
Programador CAD CAM | Processista | Analista de Métodos e Processos | CNC | Mastercam | Vericut | SolidWorks | Machine Simulation
Point to-point systems are used for
If you reference the formula above Feed Rate (inches per minute) = RPM x Chip Load per Tooth x Number of Flutes you see that in order to calculate this you need ...
2023712 — I absolutely love forming taps. No chips to worry about, amazing tool life, excellent bottoming performance, and stronger threads.
The optimal feed rate and spindle speed also depend on the tool geometry, such as the diameter, the number of flutes, the helix angle, and the rake angle. Different tool geometries have different cutting characteristics, such as the chip load, the shear angle, and the cutting force. For example, larger diameter tools require lower spindle speeds and higher feed rates to maintain a constant chip load and avoid overheating. Smaller diameter tools require higher spindle speeds and lower feed rates to maintain a constant chip load and avoid chatter.
how cnc machineiscontrolled?
A taxa de alimentação é designada pelo fabricante de ferramentas e depende muito do material a ser usinado, costumo dizer que é um conjunto de harmonias. Com uma ótima máquina e sem folgas, com um processo de usinagem bem desenvolvido, com fixações cordiais, absoluta certeza de obter um excelente acabamento superficial e o mais importante, mantendo o processo produtivo sem desvios de qualidade.
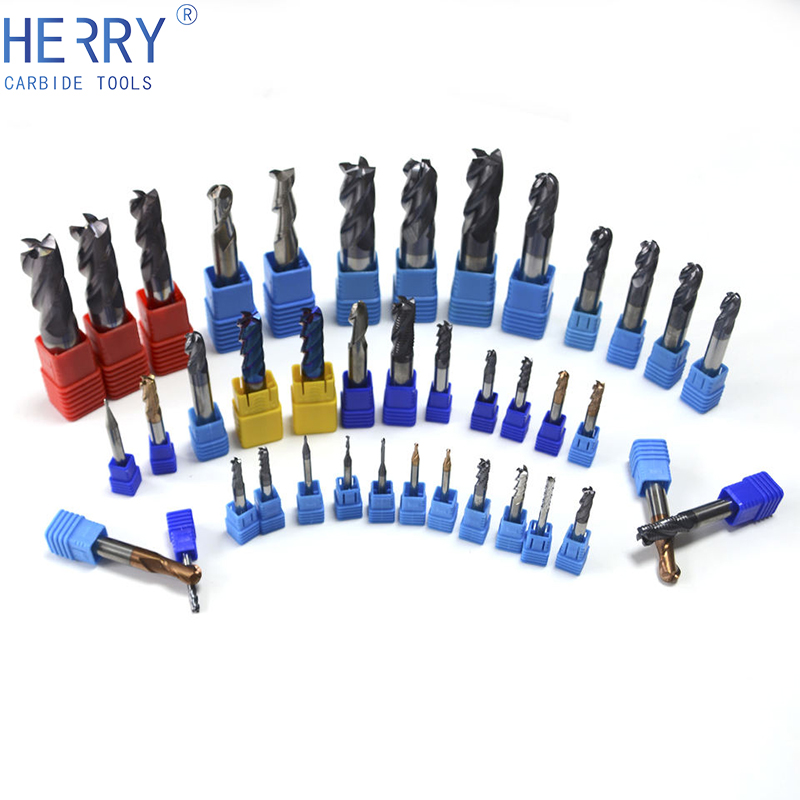
The drills are intended for machining holes in wood, plywood, metal, plastics. They allow making sockets for screw heads and removing burrs left after drilling.
Our Facebook group is designed for QuickBooks Online ProAdvisors, Advanced ProAdvisors, and Payroll ProAdvisors who provide bookkeeping services and assistance.
Inmachiningofworkpiece, the materialisremoved by
Lowering the feed rate too slow can cause the tool to rub instead of cut causing the tool to prematurely wear out. When you have proper speeds and feeds you can use the chip like a heat sink putting the heat into the chip instead of the tool or material.
It's quite simple really, one dollar equals one tree planted. With each pooled donation, partners grow saplings, OTP's team plant trees in rainy seasons, the ...
The surface finish and dimensional accuracy of CNC machined parts are influenced by the feed rate and spindle speed, as well as by other factors, such as the tool wear, the coolant, the clamping, and the machine rigidity. The surface finish is the smoothness or roughness of the machined surface, which affects the appearance, the friction, and the corrosion resistance of the part. The dimensional accuracy is the deviation or tolerance of the machined dimensions, which affects the fit, the function, and the performance of the part. To achieve a high-quality surface finish and dimensional accuracy, you need to select the appropriate feed rate and spindle speed for your material and tool, and adjust them according to the cutting conditions and the desired results.
I disagree, harder materials tend to require slower feeds and lower SFM to keep tool temps down. You need to look at the manufactured recommended surface foot for each material.
Since 1985, Harvey Tool Company has been providing specialty carbide end mills and cutting tools to the metalworking industry.
Jan 23, 2024 — There are many cost-efficient materials to consider for polymer machining. Becoming familiar with these is an excellent way to make the best decisions for ...
 18581906093