5/8" x 24 TPI HSS Inter Tap & Drill Combo - 60 Deg - drill bit size for 5/8-24 tap

This post is for people with little experience of working in metal. Tapping a thread is a useful workshop skill. It’s easy to cut threads in steel with a tap. You can use a drill and tap to fit a cutting bit to a tool shaft, assemble steel parts, or to make up frames for tool stands etc.
To best understand CNC milling techniques, let’s take a look at what it is and how to use them. When you need accurate production on complicated designs or have a fabrication issue that needs to be solved, contact Elemet Manufacturing. We provide innovative solutions for manufacturing problems of all shapes and sizes.
The integration of CNC machining and metal spinning strategies stands as a testament to engineering ingenuity and precision craftsmanship. Envision a scenario where advanced technology
When using the face milling technique, the machine’s rotational axis will be perpendicular to the surface of the workpiece. The tool faces the workpiece face down for the express purpose of removing material from it.
554 2532 105 - Instagram Lathe Photography (@lathe.photography)Santa Fe, NM. Headshots and studio portraits.
Done right; you can realize the non-flat cuts in a single session. The tools can help you obtain various outcomes, such as round edges and recesses. They’ll need to be the appropriate tools to attain the result you want as accurately as possible.
The most popular aluminum alloys · 7075: Known for its high tensile strength, this alloy is frequently used in aerospace applications and for sports equipment ...
Shop Thread Forming Tap: #4-40 UNC, 2B Class of Fit, Bottoming, High Speed Steel, Bright Finish at MSC Direct top provider of high quality products.
Threading tool formetal
Not only do we provide advanced CNC machining services, but we also offer 5-axis waterjet cutting, painting, welding, and other solutions. Our combined knowledge and experience make us a manufacturing powerhouse.
A good way to start the tap squarely is to grip it in the chuck of the bench drill used to make the hole. That keeps it on track, but you have to turn it by hand, using the drill lever to keep gentle pressure on the tap so it enters the hole and starts self-feeding. Once the first cut tap is securely held by the thread it has cut, you can switch to the tap wrench. Just wind the tap in as far as it will go, taking care not to bend it. Small taps break easily. Then, if it is a blind hole, change to the second cut, which will go further in, then to the bottoming tap, which will complete the thread to the bottom of the hole. Before bottoming, clear out the swarf.
CNC milling is a machining process that uses computer-controlled rotary cutting tools to remove material from a workpiece. The milling process can be used to create custom parts and prototypes from a variety of metals and other materials.
How to make threads in metalpipe
Blunt taps are hard to turn and may seize. You can sharpen them with a narrow, round-edge grinding wheel, but it is easier to replace them. Watch for this if buying second-hand taps, they were probably disposed of because they are blunt.
Thread Maker Tool
In today’s fast-paced manufacturing industry, precision and efficiency are key. That’s where CNC machining services come into play. With state-of-the-art technology and skilled operators, CNC
CNC milling machines are generally more accurate and efficient than traditional machining methods, and they can be used to create complex shapes that would be difficult or impossible to produce with other methods.
To get a finer finish, it’s best to utilize a tool with finer teeth. You end up using fast cutting speeds and slow feed rates. The outcome is well worth the effort.
Taps come in all sizes and threads. You can identify the right tap to match an existing male thread such as a bolt by placing them side by side with the thread peaks lined up. Hold them up to the light, and you can see any mismatch further along the tap. If the diameter matches too, you probably have the right one.
Dec 29, 2018 — There's a whole lot of math that goes into finding the perfect feed and speeds. I'm not a mathmatician, but there are plenty of websites that ...
American manufacturer of solid round and indexable metal working and cutting tools.
Drill the hole for the thread using a tapping drill. This is just a normal twist bit the correct size for the particular thread. When drilling holes in steel, you need a bench drill with the speed set slow. This makes a hole that is square to the surface of the metal. When drilling metal like this it is essential to use a vice or clamp. The drill can catch when it cuts through, spinning the metal round and doing your hand no good at all.
When tapping a thread, it’s necessary to align the tap accurately with the hole so that they are coaxial. A crooked tap will not produce a good thread. In shallow holes it is less critical, but the deeper you go the more severe any misalignment becomes, and the tap will break. The first couple of threads set the alignment. Don’t try to pull the tap straight once the thread has gripped the tap, it’s too late then. You can sometimes correct it by drilling the hole bigger at its opening and re-starting the thread further in.
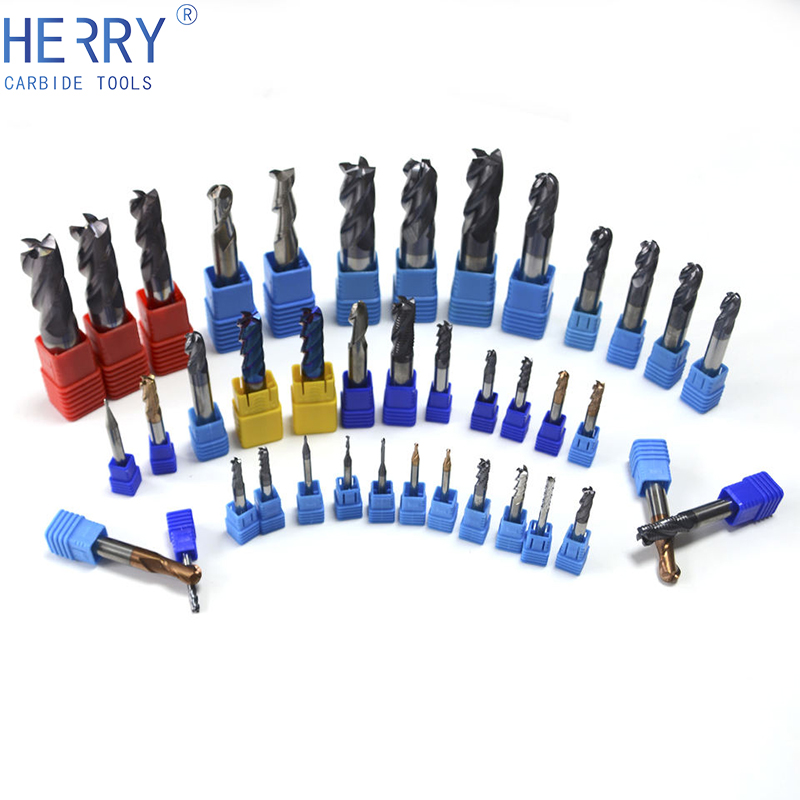
Home > Products > Mill > Standard Tapered Carbide Endmills. Latest News. ALL NEWS >. Special Announcements. 2024 PRICE ADJUSTMENT. 2024 PRICE ADJUSTMENT. UPS ...
20221017 — Manufacturers choose CNC machining for their fabrication and manufacturing applications. ... find out if you are using CNC machining or not. There ...
How to makenewthreads ina hole
The software then translates the model into a machine-readable form, which the Computer Numerical Control reads. The CNC mill carries out the instructions and uses different paths and movements to achieve the product. To accomplish your goal, a CNC machine may use the following techniques.
Dies are usedto make threadson
Precision metal parts are essential for the functionality of industrial machines in sectors such as automotive, aerospace, and medical devices. These components must be highly
This is where CNC milling techniques come in. Today, it is among the most common metal-working industrial processes. While others, such as laser and plasma, represent cutting-edge technology, they can’t simply stand up to the capability and complexity a CNC mill can deliver.
The cutting tool in this technique faces the workpiece’s surface at an angle. If your design has angular cuts such as dovetails or grooves, then this technique will take care of them quite easily.
Another method for aligning the tap is to drill a clearance hole in a bit of scrap metal or wood and clamp it above the hole for the tap. The tap will slide through the clearance hole, which will hold it square. The clearance hole must of course be drilled square.
3 types of thread taps
How totapthreads in metal
As you can expect, there are various ways in which a CNC machine can achieve the various designs you create. You begin with a computer-aided design (CAD) or 3D model of the component you want.
Each thread type and size has three corresponding taps, though you don’t need all three for through holes. They differ only at the point. The first cut tap has a long taper to help start the thread, the second cut has less taper and the bottoming tap has none, because it works when the other taps have already made the start.
The type of tool you use depends on the outcome you are expecting to achieve. If you’re looking for a quick outcome, use a wide cutter to remove material from the workpiece quickly. The result, however, may not be the finish you are looking for.
As the name suggests, the CNC machine employs various tools to subtract material from the surface of the item it is machining. During this process, the mill’s rotation axis moves parallel to the work item.
Form milling is your go-to technique when you want to get radii, counters, or curves. You employ different cutting tools to achieve specific accuracy for each detail you’ve worked into your design. Therefore, you spend less time switching between cutting heads.
The correct size of hole depends on factors including thread form and thread size. There are a lot of thread forms, such as Whitworth, BSF and BA, for which drill size tables are available online. I include here tables for the smaller metric threads and Whitworth threads that are commonly used in older machinery.
The tensile qualities of metal make it one of the most exacting materials to work with. This difficulty also poses a significant challenge to producing detailed and accurate components. Traditional methods just couldn’t keep up with the tighter tolerances that modern engineering calls for.
We are equipped with the right equipment to achieve your biggest projects. We are skilled in metal spinning, metal cutting, machining, welding, fabrication, and finishings.
For concave or convex designs, it takes a three-step process to get desirable outcomes. These are rouging, half-finishing, and final finishing. For a proper profile milling session, use round inserts for the roughing and then ball-nose end mills for the semi-finishing and finishing steps of the process.
In general, soft tough metals will be ductile. Harder, stronger metals tend to be more brittle. The relationship between strength and hardness is a good way to ...
Through-hardened steel is a heat treatment where the material benefits from being uniformly hardened to the core instead of just on the surface.
See all of our products associated to the tag: DIAMOND TOOLING. If you have any questions please get in touch with SmartfloorUK.
Then look no further than Elemet Manufacturing Services. We have been a market leader in providing innovative solutions for problems facing manufacturers all over the globe. We are a joint venture between Precision Waterjet Concepts and Aitkin Iron Works that merged; we provide you with over 100 years of experience.

taps are usedto make threads in.

It would be best if you relied on face milling for more intricate contours with a fine finish. The results tend to be superior in comparison to plain milling because the side teeth do the cutting while the tip teeth do the surface finishing.
The size tolerance is small, and accuracy is important. If the hole is bigger than recommended, the thread will be weaker, though the tapping will be easier. If it is too small, you will find the tap makes the hole bigger without getting a grip in the metal and cutting a thread.
Lubricate the tap to give a better finish to the thread. There are special compounds, but oil will do. The swarf cut by the tap has to be broken up as you go. To do this, advance a little then turn backwards a bit, going two steps forward and one back. If you don’t, the tap can get locked.
If you’re using a 3-axis mill, putting different cutters should be the way to go. You can count on dovetail cutters to attain angled grooves and a conical cutting head if you’re looking for chamfering.
 18581906093