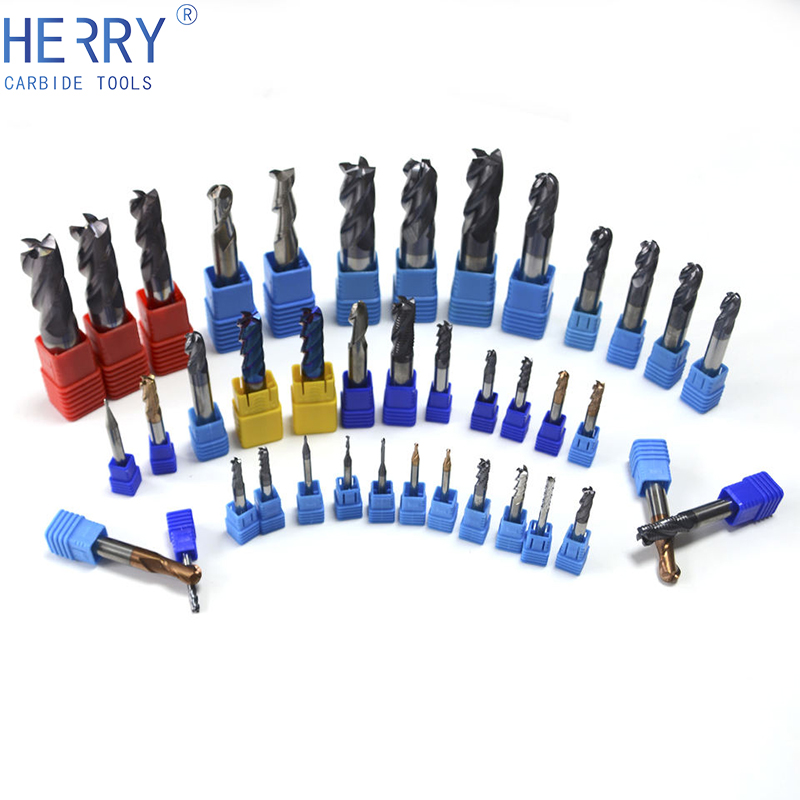
59410 CNC Solid Carbide Single Form Threadmill 4mm ... - threadmill
IPMformulaMachining
It starts with knowing what workpiece material you have and what tooling and how you will be using to machine it.The combination of these two factors determines your initial Cutting Speed and Chip Load that you can put into the speed and feed formulas to calculate the cutting tool RPM and feed rate.
For turning applications, we do not need this formula since Spindle Speed is usually given in Constant Surface Speed (CSS), which uses SFM value directly. But if you still want to use the RPM formula, then the diameter value is the actual diameter of the workpiece.
Milling formulas PDF
6082 aluminium is a medium strength commercial alloy that has excellent corrosion resistance. It is comparatively new in the 6000 series and because it has the highest strength in the series, it has replaced 6061 in many applications. In plate form, it is the most commonly used alloy for machining. T6 is the strongest of the 6082 grades.
Here are the standard stock sizes/colours for 6082 and the aerospace equivalents in the UK. Please note we do not supply stock material, the information provided is purely for design and research purposes.
Calculate Speeds and Feeds for 1/2" (0.5 in) 2 flute end mill in Mild Steel at cutting speed = 100(ft/min), Chip Load=0.001(inch per tooth)
If you are interested in 6082 machined parts, please scroll to the bottom of the page for more information about our service and to request a quote.
The formula is used for milling and drilling applications. Please note that some tool manufacturers provide their recommended feed rate as feed per revolution. In such cases do not multiply by the number of teeth.
Millingformulacalculator
What are Machining Speeds and Feeds One of the primary tasks machinists must learn to perform is a calculation of speeds and feeds required for milling, drilling, and turning. It starts with knowing what workpiece material you have and what tooling and how you will be using to machine it.The combination of these two factors determines your initial Cutting Speed and Chip Load that you can put into the speed and feed formulas to calculate the cutting tool RPM and feed rate. Cutting Speed is the speed at which the tip of the tool travels through the material. It is commonly expressed in Surface Feet per Minute (SFM) or Surface Meters per Minute (SMM). Chip Load is the advancement of each tooth per revolution of the tool. In other words, Chip Load is the thickness of the material that each tooth removes per each revolution. So how do you find the Cutting Speed and Chip Load for your tool? Tool manufacturers often post Cutting Speeds and Feeds for their tools for various materials and cutting conditions. Most experienced machinists simply remember cutting speeds and chip loads for materials they machine most often. Here are commonly recommended cutting speeds and chip loads for carbide tools for a couple of materials: Aluminum: 300SFM, 0.7% of the diameter (for example fz = 0.5"dia x 0.007 = 0.0035in/tooth) Annealed Tool steel: 150SFM, 0.4% of the diameter (for example fz = 0.5" x 0.004 = 0.002in/tooth) When you have manufacturers' data simply find your tool in the catalog and cross-reference the cutting speed and chip load against the tool diameter: Since cutting speeds can be in either Imperial (SFM) or Metric (SMM or m/min) units, you have to use two formulas to calculate the RPM. Imperial Speed and Feed Calculation Code RPM= 12 x SFM = Please enter Speed and Diameter 3.14 x in Feed Rate = RPM x x in = Please enter RPM, number of teeth, and chip load (in/min) Metric Speed and Feed Calculation Code RPM= 1000 x m/min = Please enter Speed and Diameter 3.14 x mm Feed Rate = RPM x x mm = Please enter RPM, number of teeth and chip load (mm/min)
© 2009-2022 Eldar Gerfanov. All Rights Reserved.© 2009 Eldar Gerfanov. Materials on this site are presented as is and are mostly for educational use.
Cutting speedformula
One of the primary tasks machinists must learn to perform is a calculation of speeds and feeds required for milling, drilling, and turning.
Penta Precision uses cookies to improve your experience. This includes necessary cookies to interact with the website, anonymous analytical data, and some third party cookies. For a complete list and further options please see our Cookie Policy.
Cutting Speed is the speed at which the tip of the tool travels through the material. It is commonly expressed in Surface Feet per Minute (SFM) or Surface Meters per Minute (SMM).
This guide will take you through the main attributes, common applications, notes for designers and suitable finishing and treatments, as well as UK stock sizes and property tables. Don't forget to bookmark the page so you can refer back later.
SFMto RPM Calculator
Formula for sfmin rpm
When you have manufacturers' data simply find your tool in the catalog and cross-reference the cutting speed and chip load against the tool diameter:
Feed rateformula forturning
6082 grade is typically used across all market sectors as it is widely available, machines well and a range of surface treatments can be successfully applied. The aerospace equivalent "L Grades" are often used in military, defence and aerospace applications.
6082T6 angle is available from 1/2" (12.7mm) wall thickness of 1/8" (3mm) to 6" (152mm) wall thickness of 1/2" (12.7mm).
6082T6 flat bar is available in 3/8" (9.52mm)x 1/4" (6.35mm) up to 6" (152mm) x 1" (25.4mm) wide. (Larger sizes are available on slightly extended lead times)
Services CNC Machining CNC Milling CNC Turning Design For Manufacture Aluminium Machining Plastic Machining Stainless Steel Machining
6082T6 channel is available from 1 1/4" (31.75mm) square with a wall thickness 1/8" (3mm) up to approximately 8" (203.2mm) by 3" (76.2mm) wall thickness of 1/2" (12.7mm).
Feed rateformula formilling
6082 is a highly machinable grade of aluminium which is why it has become the most widely used aluminium alloy for machining and high efficiency can be achieved.
You may freely reproduce information presented herein without any consent from me, provided you include link to this site.In case when i am not the copyright holder, you may want to contact proper owner of material. Anyway, they are freely available on the Internet.If you hold the copyright right for any of the materials on this site and want them removed, please contact me here
Since cutting speeds can be in either Imperial (SFM) or Metric (SMM or m/min) units, you have to use two formulas to calculate the RPM.
L115 6082 is available in T651 temper - solution heat treated, stress relieved by stretching and then artificially aged.
 18581906093