6.0mm IN 16 TPI UNJ Indexable Thread Milling Inserts ... - milling insert specification
In determining the tool holder to enter the tool, the depth of cut, and the machine specifications, consider the cutting length.
In addition to its high cost per unit, carbide is also very brittle, making it more susceptible to breaking and chipping when compared to other typical tool materials. Due to these factors, carbide cutting tips are often provided as small inserts within larger cutting tools that have steel hilts. The shank of the hilt is usually made of carbon, which is a more suitable material for the shank of the carbide cutting tip. As such, the carbide surface at the cutting interface is able to provide the benefits of using carbide without incurring the high costs and brittleness of making the whole tool from carbide. As with many of the modern lathe tools and endmills, most face mills these days have carbide inserts as well in them.
Inserts made of cemented carbide are available in several sizes, shapes, and compositions that are used in various manufacturing methods on steels, cast iron, highly ferrous alloys, and nonferrous metals. In addition, machining metal parts more efficiently and with better finishes can be done when using carbide inserts. In addition to steel, stainless steel, hardened steel, cast iron, non-ferrous metals, titanium, and boring inserts are also good choices for applications.
Unless otherwise specified, dimensions A and B refer to the distance measured along the bisector of the rounded corner angle and a gage roll of nominal I.C. For instance, if tolerance letter H shows 0.005″ on A, 0.0005″ on B, and 0.001″ on T, so dimensions (* from nominal) are: A, B, and T.
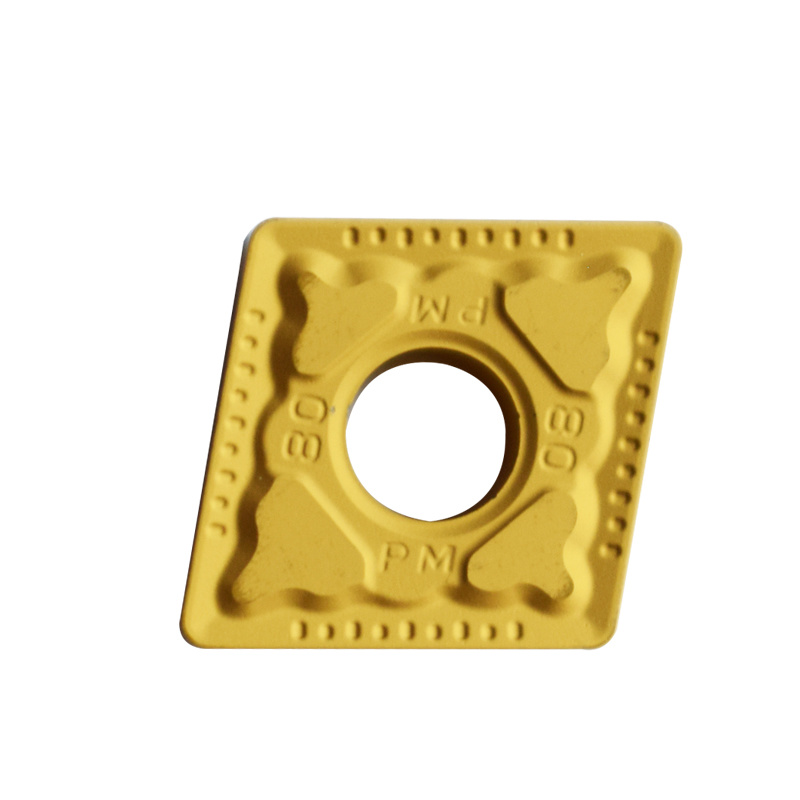
The term milling insert refers to a piece of equipment that can be used to process materials such as steel and titanium without the fear of breaking the tool. The materials they help shape, they can straighten, shape, cut, and they can also cut metals such as steel, stainless steel, cast iron, non-ferrous materials, titanium, hardened steel, and plastic.
The ceramic compound is added with small crystals of silicon carbide when whiskered ceramics are formed. There is a physical similarity between these crystals and whiskers, which is why this ceramic is called whiskered ceramic. With this kind of whisker, you can expect a machine to be a lot more resilient to vibrations and shocks.
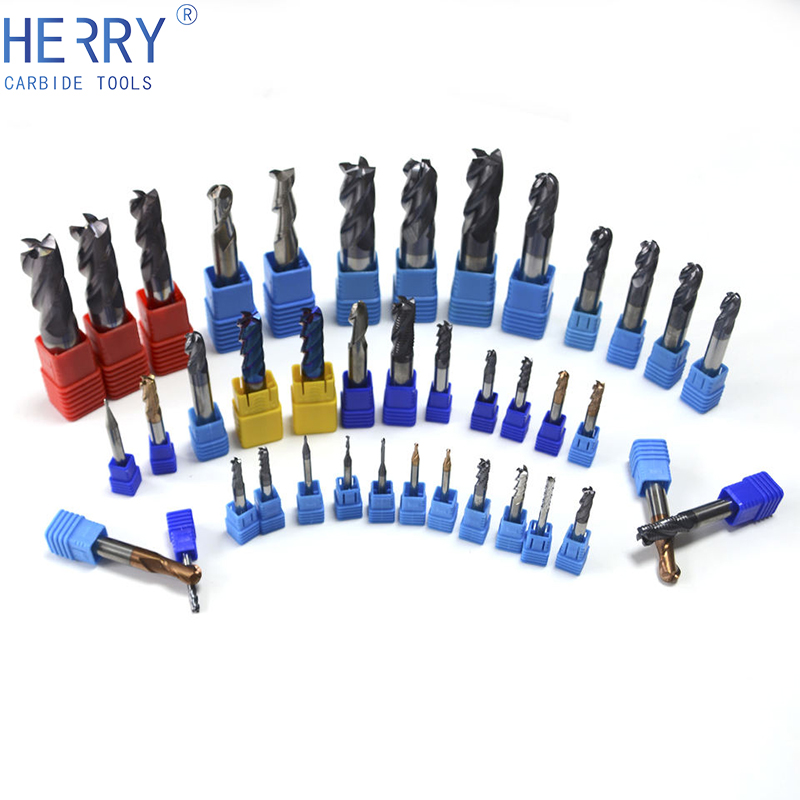
Features:- Solid Carbide Ball Nose Endmill for hardness up to 40HRC having 4 FLUTES Standard Length Ball Nose SIZE CODE DIAMETER SHANK DIAMETER FLUTE LENGTH ...
In particular, ceramic inserts are much superior to carbide inserts when it comes to heat resistance. The ceramic insert category encompasses several variations, but, generally speaking, all of the options fall under the category of providing solutions for the machining of extremely hard metals. Since ceramic inserts are heat-resistant, they can be used for lower production times as they are capable of cutting continuously at higher speeds due to their heat resistance. Due to reduced production times and lower costs, ceramic inserts are a good choice.
Letter A, B, and T indicate the tolerances on the dimensions (* from nominal). Insert dimensions are given by Dimension A. Inscribed circle diameter is given by Dimension A. Dimension T is the thickness of the insert. As a result, dimensions A and B are the corresponding dimensions for pentagonal, triangle, and triangular shapes.
The gas is seen as an alternative to acetylene with greater tolerance to torch distance variation because of the more uniformly distributed heat between the inner and the outer cones.
The choice of fuel gas is largely made on cost, performance, ease of use and whether it is a manual or mechanised operation. However, in making the choice it should be noted that in a typical application the cost is made up of approximately:
A carbide insert is a cutting tool is tool that is used for machining different metals, such as cast iron, steel, carbon, non-ferrous metals, and alloys with a high melting point. The inserts of a carbide cutter are indexable, which means they can be swapped, rotated, or flipped without affecting the geometry of the cutting tool.
LatheCarbide Inserts
As the material integrity of ceramics has been improved, ceramics can be a viable alternative to carbide solutions, improving the life of the material to a similar duration as that of carbides.
In the ninth position is a capital letter that indicates the hand of an insert: R – Right Hand; L – Left Hand; N – Neutral.
Acetylene nozzles are usually one-piece but two-piece nozzles similar to those for other fuel gases are produced for machine cutting.
In the sixth position, there is a significant one- or two-digit number representing the thickness of the insert in sixteenths of an inch. Whenever the thickness of a piece is a whole number: 1 – 1 * 16″; 2 – 1 * 8″; 3 – 3 * 16″; 4 – 1 * 4″; 5 – 5 * 16″; 6 – 3 * 8″; 7 – 7 * 16″; 8 – 1 * 2″; 9 – 9 * 16″; 10 – 5 ⁄ 8″.
A number of parameters must be taken into consideration when choosing the right carbide inserts. It is possible to find China carbide inserts manufacturers who provide quality material, but why take the chance? It is possible to find China carbide inserts manufacturers who provide quality material, but why take the chance?
It is intended to identify the eighths of an inch in the nominal size of the I.C. It will have one digit whenever the number of eighths of an inch in the I.C. is a whole number: 1 – 1 * 8″; 2 – 1 * 4″; 3 – 3 * 8″; 4 – 1 * 2″; 5 – 5 * 8″; 6 – 3 * 4″; 7 – 7 ⁄ 8″;
Carbide blades can be used to cut through wood, plastic, and metal, as well as a variety of other materials. Choosing the right blade for your material allows you to get smooth cuts using hard carbide tips. In terms of blades, the number of teeth, their shape, and if they are rounded or pointed, make a difference. It can be sharpened and reused for a long time when used correctly. On the contrary, the typical application of Ceramic Blades is to cut ceramic tile, porcelain marble, concrete, and masonry. They have a diamond coating that provides very clean and smooth cut results. Wet or dry applications are possible with this type of ceramic blade.
The width and length dimensions of rectangular and parallelogram inserts are used instead of the I.C. The size of these inserts is indicated by a two-digit number. A first digit indicates how many eighths of an inch the insert is wide and a second digit shows how many fourths it is long.
Carbide inserts are available in a wide range of types depending upon your application requirements. Below is a list of some of the major types of carbide inserts you are likely to encounter in your everyday life.
The indexability of inserts is controlled by 14 tolerance classes. Capital letters indicate each class. Tolerances are indicated by the letters A, B, C, D, E, F, G, H, J, K, L, M, U, and N.
The selection of carbide shapes should be based upon ensuring that it is a relatively essential tool for entering angles into the tooling process.
What does SFM mean? Get the full information of SFM acronym / abbreviation / slang definitions at AcronymsandSlang.com Find out or define your SFM meaning ...
Kennametal inserts
There is no doubt that tungsten carbide inserts can withstand pressure when it comes to performance under pressure. In order to produce this durable, extremely strong metal, grains of tungsten carbide are cemented into nickel or cobalt to create cement. Tungsten carbide produces a material second only to diamond in terms of hardness.
The seventh position indicates a radius or a facet. Radius is given as 1 * 64 of an inch: 0 – sharp corner (0.002″ maximum radius); 0.2 – 0.004″; 0.5 – 0.008″; 1 – 1 * 64″; 2 – 1 * 32″; 3 – 3 * 64″; 4 – 1 * 16″; 5 – 5 * 64″; 6 – 3 * 32″; 7 – 7 * 64″; 8 – 1 * 8″; 10 – 1 * 16″
This Job Knowledge article was originally published in Connect, November/December 2000. It has been updated so the web page no longer reflects exactly the printed version.
Tormach inserts
Consideration should, therefore, be given to the choice of fuel gas type and nozzle design to speed up the initiation of the cutting operation. Labour costs can be reduced by decreasing the pierce time and/or increasing the cutting speed. Typical flame temperatures and fuel gas to oxygen ratios are shown in Fig. 1. Generally, fuel gases which generate a higher flame temperature and require a lower oxygen to fuel gas ratio, will speed up the cutting operation.
Additionally, these tools can be removed from the tool body, which means that the tools are not welded or brazed together. This type of tool can be used at high speed, which means you can create better surface finishes on your materials as a result of faster machining.
Each torch should be fitted with the appropriate nozzle for the type of fuel gas. Nozzles can be of a one- or two-piece design. The nozzle type will depend on:
You can take advantage of inserts carbide in numerous possible ways. You can use carbide lathe inserts for machining various materials.
It is ultimately determined by such factors whether or not you will achieve satisfactory chip control and machining results.
A turning tool body grips a replaceable insert which is attached to a lathe turret. Turning is typically done with a replaceable insert. Inserts for turning tools are manufactured using composite materials, coatings, and geometry features that provide high accuracy and high material removal rates.
Carbideinsertidentification chart pdf
Unlike a conventional drill, an NC spot drill has zero back taper and no clearance behind its drill lip. Spot drills are made of HSS or carbide, but it is ...
Hello! I want to simulate a simple body which is producing its own heat. The produced heat depends on the temperature of the body and should be considered ...
Lightly bevels the end of polyethylene pipe prior to socket fusion. The tool is sized to allow marking for the proper end distance for the cold ring.
Typically, carbide particles are bonded together with a metallic binder in order to create carbides that are cemented together. The carbide particles act as aggregates and the metallic binder acts as the matrix. Sintering means the combination of the carbide particles with the binder, so it is a technology that combines the particles with the binder. The binder in this process gradually enters the liquid phase, while the carbide grains (which have a much higher melting point) remain in the solid phase. In reality, the binder is cementing the carbide grains, creating a metal matrix composite with the distinct material properties that it requires. Taking advantage of the naturally ductile property of metal binders, to offset the characteristic brittle nature of carbide ceramics, is one of the best ways to increase their toughness and durability. The carbide parameters can be modified significantly in this manner within the sphere of influence of the carbide manufacturer, mainly depending on the grain size, the cobalt content, the dotation, and the carbon content.
According to ANSI B212.4-2002, there was an additional capital letter O, which denoted other relief angles for design changes to indexable inserts.
When the seventh position contains letters, the 10th position will only be used. The number represents a nominal measurement of sixty-fourths of an inch in length: 1 – 1 * 64″; 2 – 1 * 32″; 3 – 3 * 64″; 4 – 1 * 16″; 5 – 5 * 64″; 6 – 3 * 32″; 7 – 7 * 64″; 8 – 1 * 8″; 9 – 9 * 64″; 10 – 5 ⁄ 32″.
A standard called ANSI B212.12-1991 describes nine different relief angle values. The angle between the flanks of an insert and the top surface of the insert is calculated by measuring the distance from 90° in a plane normal to the cutting edge. Typical relief angles are denoted as follows:
An ideal nose angle would be a big one but it would be more complicated and require a lot more resources. Furthermore, it would be more likely to cause vibrations. As a result, a small nose angle will have a low cutting edge engagement and may not perform as well as a large angle. It is, therefore, more prone to the diverse effects of heat and has a heightened sensitivity to them.
When choosing carbide shapes, consider the highest possible nose angle to ensure the longest possible life of the insert.
This Corner Rounder is a heavy duty, multi-operational punch tool which will round and hole punch most materials. Professional finish with save edges every time ...
The tungsten carbide used in cemented carbide is melted at an extraordinarily high temperature inside moulds. For saw blade tips, the moulds have pockets. These cemented carbide tips are then removed from the mould, placed on the saw blade tips, and brazed into place. A very sharp cutting edge is then created by grinding the tips. Except for the coating used on the tips, ceramic blades are formed the same way as carbide blades. There are also ceramic blades without teeth and with completely smooth edges. Blades with ceramic coating have very small diamonds embedded in the edge or tip. Diamond blades are commonly referred to as such because of this feature.
The high temperature (maximum flame temperature in oxygen is 3160°C), highly focused flame makes the oxyacetylene process ideal for cutting thin sheets with minimum distortion and for bevel cutting. However, the high cost and low heat generation make it less suitable for general heating of large plates.
If you are planning on using a carbide insert when you are cutting particulates or foam, you will have to make sure you choose the right insert. A preventative method can reduce the number of damage cases to the insert, as well as the machines as well as the workplace in general. Among the different styles, sizes and grades of cutting tools available in the market today.
Among the multitude of applications for which groove-making tools are relevant, there is a vast variety of hardware components of all types. These Carbide specialists specialize in determining the precise specifications required to perfectly suit the needs of each customer, regardless of whether they are parting off a smaller component or creating a deep groove with a large diameter. A Carbide insert can be grooved efficiently and expertly for extrusion grooving, internal grooving, face grooving, as well as parting. To maximize productivity and efficiency, you need to make sure that you choose the right tool. Every groove comes with its own set of challenges, no matter how wide or shallow it is. Additionally, every material used in the manufacturing of the component has its own set of properties and limitations. It is these three elements that truly determine how the ideal tool should be designed, sized, and rated for the job.
The cutting torch design can be either nozzle mix or injector. In the nozzle mix torch, the fuel gas and pre-heat oxygen are mixed in the nozzle. In the injector torch, the pre-heat gases mix either in the body of the torch, within the gas delivery tubes, or within the head of the torch. Injector torches have the advantage of being able to use the higher pressure of oxygen to pull the fuel into the torch. This allows the torch to be used at low fuel gas pressures or with large pressure drops such as those experienced through long hose lengths.
It is therefore not surprising that the process can be used for a diverse range of applications from manual rough severing and scrap cutting to precision contour cutting in fully automated systems. Here, the process application is described including the choice of fuel gas and nozzle design to maximise performance. Best practice to ensure adequate quality of the cut surface is also included.
Fourteen standard types of insert are referred to using capital letters, and these variations include fixing holes, countersinks, and special features on rake surfaces.
The carbide insert thread mill is the term used to describe a piece of cutting insert that is used to create an internal or external thread within a part. These are typically attached to a tool holder on a lathe or a turning centre, where they are normally used with tools.
There must be a simple system devised to categorise carbide inserts for their use since the sheer variety of carbide inserts on the market and their precision use require it. A series of letters and numbers are engraved on the centre of all steel cutting inserts, including carbide turning inserts. It refers to the ISO code system for turning tools that provides a simple method of identifying carbide inserts that can be used for narrowing the search for inserts. We discuss in this article a system of codes used to identify carbide inserts, and how I advise you to use the code system to identify your inserts.
With the combination of excellent heat resistance, better vibration and speed resistance, and the capability of cutting hard metals such as cast iron, ceramics are truly remarkable. Furthermore, this increase in the strength of the ceramic material also helps to prevent cracks from forming as a result of cutting the material.
A capital letter indicates 10 positions in the indexable insert as per the ANSI B212.4-2002 standard. There are ten positions (1-10), which define the characteristics of an insert as follows:
The upcoming work will be easy for you once you have gained the knowledge of how to identify carbide inserts as a newbie. Carbide inserts are cutting tools that can be used to cut a wide variety of materials with high precision. Despite this, there are certain types of carbide inserts that can be used for cutting specific types of materials since not every insert can cut all types of materials. Thus, it is important for you to know what type of inserts are you using and when to use them.
High-speed nozzles are capable of being used with higher oxygen pressures, up to 10 bar. The essential difference is that the cutting oxygen is forced through a convergent / divergent orifice which speeds up the gas flow rate to near supersonic levels. High-speed nozzles are primarily used in mechanised equipment to exploit the higher speeds for cutting long lengths.
Carbide inserts chart
Only acetylene, hydrogen and MAPP have sufficiently high flame temperature for underwater cutting. But as acetylene has a limited outlet pressure, MAPP is the only gas other than hydrogen that can be used for cutting in deep water.
Coatings are sometimes used in order to increase the lifetime of carbide inserts. Generally, coatings designed to increase a tool’s hardness or lubricity will also increase the tool’s lubricity. By coating a cutting tool, it will be possible for the cutting edge to pass cleanly through things without the material galling or sticking to it. Besides lowering the temperature associated with the cutting process, the coating will also increase the tool’s longevity by preventing the tools from getting stripped out. As a rule, the coating is deposited using either thermal CVD or mechanical PVD methods, both of which are usually done at lower temperatures, depending on the application.
nozzle distance - too high or too low will disturb oxygen flow preheat flame - too high a flow can cause top edge melting cutting oxygen - too low a flow can cause poor slag removal - too high a flow can result in poor cut finish
When the grade is tough enough, the lack of strength in insert geometry can be compensated in part by the grade despite the lack of strength in the insert geometry.
Make sure that you choose your carbide insert size according to the particular machining requirements and the availability of cutting tools in your position.
With its high accuracy and high-performance indexable inserts, the Drilling and Hole Boring System is suitable for use on materials as diverse as aluminium and superalloys. With the drill body made of heat-treated steel that is very rigid, the nest for the insert is rigid and the flutes are straight, resulting in a long term life for the insert and an efficient chip removal process.
Sep 22, 2022 — The feed rate in CNC machining is one of the most important factors to consider. It is defined as the velocity at which the cutter is fed.
For similar nozzle designs, cutting speeds for oxypropane and oxyacetylene are similar. Advantages claimed for propane are smooth cut edge, less slag adhesion and lower plate edge hardening because of the lower flame temperature. The heat affected zone is much wider than for oxyacetylene.
Latheinserts Chart
Universal Mini Metal Lathe Milling Machine Motorized Metalworking DIY Tool 36W Brand New: Unbranded $155.99 to $168.99 Free shipping
In addition to thread mills and thread rolling, the use of thread inserts is another method for creating threads on a workpiece similar to thread milling. It is important to put these replaceable commodities in their proper places as replacements wear out.
... Name*. Sign Up for Our Newsletter: Instruments. Clarinets, Flute / Piccolo, Oboe / Cor Anglais, Trumpet / Flugelhorn, General News & Events, Cornet, French Horn ...
Five digits indicate the diameter of the inscribed circle (I.C.) for all inserts that have a true I.C. such as Rounds, Squares, Triangles, Trigons, Pentagons, Hexagons, Octagons, and Diamonds.
The typical appearances of a good and poor quality cut surface for manual cutting are shown in Fig.3. The principal features are described together with their cause and remedial measures necessary to produce the ideal square edge, smooth surface cut.
In order to protect and maintain the integrity of ceramic materials, precautions must be taken in the use of machines to keep excessive vibrations to a minimum. Ceramics are naturally more brittle than carbide alternatives. The ceramic compound is augmented with additional components that prevent this brittle tendency and increase its longevity.
Find here Milling Cum Drilling Machine, Gang Drilling Machine manufacturers, suppliers & exporters in India. Get contact details & address of companies ...
Propylene is a liquid petroleum gas (LPG) product and has a similar flame temperature to MAPP (2896°C compared to 2976°C for MAPP). It gives off a high heat release in the outer cone (72,000 kJ/m3) but, like propane, it has the disadvantage of having a high stoichiometric oxygen requirement (oxygen to fuel gas ratio of approximately 3.7 to 1 by volume).
Methane has the lowest flame temperature similar to propane and the lowest total heat value of the commonly used fuel gases. Consequently, natural gas is the slowest for piercing.
The diameter of the cutting oxygen hole is selected according to the material thickness. There are two types of nozzle; standard and high speed. The standard nozzle usually has a parallel sided, central bore for the oxygen jet, which is surrounded by an annulus or a ring of smaller diameter ports for the pre-heating gas mixture, Fig. 2. There are many designs and arrangements of the preheating ports that focus the flame for heating and to protect the oxygen jet from air entrainment.
Propane is low cost and has the advantage of being available in bulk supplies. The flame temperature is lower than for acetylene (the maximum flame temperature in oxygen is 2828°C compared with 3160°C for acetylene) which makes piercing much slower. However, it can tolerate a greater nozzle to workpiece distance which reduces the risk of molten metal splashing back onto the nozzle and causing a 'backfire'.
Based on the type of holder used, these inserts can cut grooves on both the outsides as well as the insides of a workpiece.
 18581906093