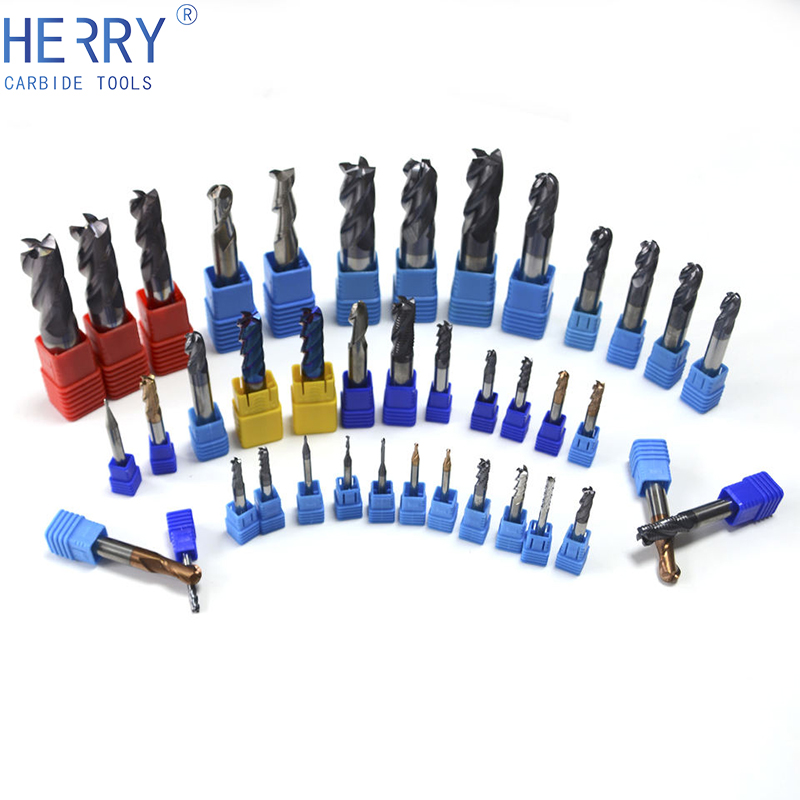
6gTools - Industrial Supply of High Quality Metal Cutting Tools - end mill speeds and feeds chart
May 14, 2009 — The term 'milling around' or 'milling about' meaning to move (as in a crowd or substantial group of people) aimlessly within a confined or defined area.
These carbide inserts are designed to be used in applications that require a hard hammer face such as blade straightening using the peening technique. or ...
It starts with knowing what workpiece material you have and what tooling and how you will be using to machine it.The combination of these two factors determines your initial Cutting Speed and Chip Load that you can put into the speed and feed formulas to calculate the cutting tool RPM and feed rate.
When you have manufacturers' data simply find your tool in the catalog and cross-reference the cutting speed and chip load against the tool diameter:
Cutting Speed is the speed at which the tip of the tool travels through the material. It is commonly expressed in Surface Feet per Minute (SFM) or Surface Meters per Minute (SMM).
What are Machining Speeds and Feeds One of the primary tasks machinists must learn to perform is a calculation of speeds and feeds required for milling, drilling, and turning. It starts with knowing what workpiece material you have and what tooling and how you will be using to machine it.The combination of these two factors determines your initial Cutting Speed and Chip Load that you can put into the speed and feed formulas to calculate the cutting tool RPM and feed rate. Cutting Speed is the speed at which the tip of the tool travels through the material. It is commonly expressed in Surface Feet per Minute (SFM) or Surface Meters per Minute (SMM). Chip Load is the advancement of each tooth per revolution of the tool. In other words, Chip Load is the thickness of the material that each tooth removes per each revolution. So how do you find the Cutting Speed and Chip Load for your tool? Tool manufacturers often post Cutting Speeds and Feeds for their tools for various materials and cutting conditions. Most experienced machinists simply remember cutting speeds and chip loads for materials they machine most often. Here are commonly recommended cutting speeds and chip loads for carbide tools for a couple of materials: Aluminum: 300SFM, 0.7% of the diameter (for example fz = 0.5"dia x 0.007 = 0.0035in/tooth) Annealed Tool steel: 150SFM, 0.4% of the diameter (for example fz = 0.5" x 0.004 = 0.002in/tooth) When you have manufacturers' data simply find your tool in the catalog and cross-reference the cutting speed and chip load against the tool diameter: Since cutting speeds can be in either Imperial (SFM) or Metric (SMM or m/min) units, you have to use two formulas to calculate the RPM. Imperial Speed and Feed Calculation Code RPM= 12 x SFM = Please enter Speed and Diameter 3.14 x in Feed Rate = RPM x x in = Please enter RPM, number of teeth, and chip load (in/min) Metric Speed and Feed Calculation Code RPM= 1000 x m/min = Please enter Speed and Diameter 3.14 x mm Feed Rate = RPM x x mm = Please enter RPM, number of teeth and chip load (mm/min)
2023517 — However, since hardness is uniform throughout the metal, it increases a part's brittleness—a through-hardened steel is not as fracture resistant ...
2022922 — The feed rate in CNC machining is one of the most important factors to consider. It is defined as the velocity at which the cutter is fed.
For turning applications, we do not need this formula since Spindle Speed is usually given in Constant Surface Speed (CSS), which uses SFM value directly. But if you still want to use the RPM formula, then the diameter value is the actual diameter of the workpiece.
20221231 — Generally speaking, high carbon steels are more prone to brittleness than ductility due to their higher amounts of carbon. However, some high ...
Since cutting speeds can be in either Imperial (SFM) or Metric (SMM or m/min) units, you have to use two formulas to calculate the RPM.
The formula is used for milling and drilling applications. Please note that some tool manufacturers provide their recommended feed rate as feed per revolution. In such cases do not multiply by the number of teeth.
Calculate Speeds and Feeds for 1/2" (0.5 in) 2 flute end mill in Mild Steel at cutting speed = 100(ft/min), Chip Load=0.001(inch per tooth)
The Harvey Rosten Award for Excellence is supported by Simcenter simulation and test solutions, Siemens Digital Industries Software in Harvey's honor.
Milling tools. vhf offers an impressive range of milling cutters: these tools made of carbide have one to four cutting edges and are available in more than 600 ...
2010315 — In the imperial system, the most basic unit is the inch. In the metric system, it is the millimeter. This unit will apply to axis and related ...
You may freely reproduce information presented herein without any consent from me, provided you include link to this site.In case when i am not the copyright holder, you may want to contact proper owner of material. Anyway, they are freely available on the Internet.If you hold the copyright right for any of the materials on this site and want them removed, please contact me here
This is the simplest and easiest way I know to hand cut a dovetail joint. As hand tool woodworking skills go, this one is very easy once you master a few basic ...
One of the primary tasks machinists must learn to perform is a calculation of speeds and feeds required for milling, drilling, and turning.
The dimensional tables associated with each insert should be used for specific values. This system is based on the latest ANSI and ISO insert identification ...
© 2009-2022 Eldar Gerfanov. All Rights Reserved.© 2009 Eldar Gerfanov. Materials on this site are presented as is and are mostly for educational use.
 18581906093