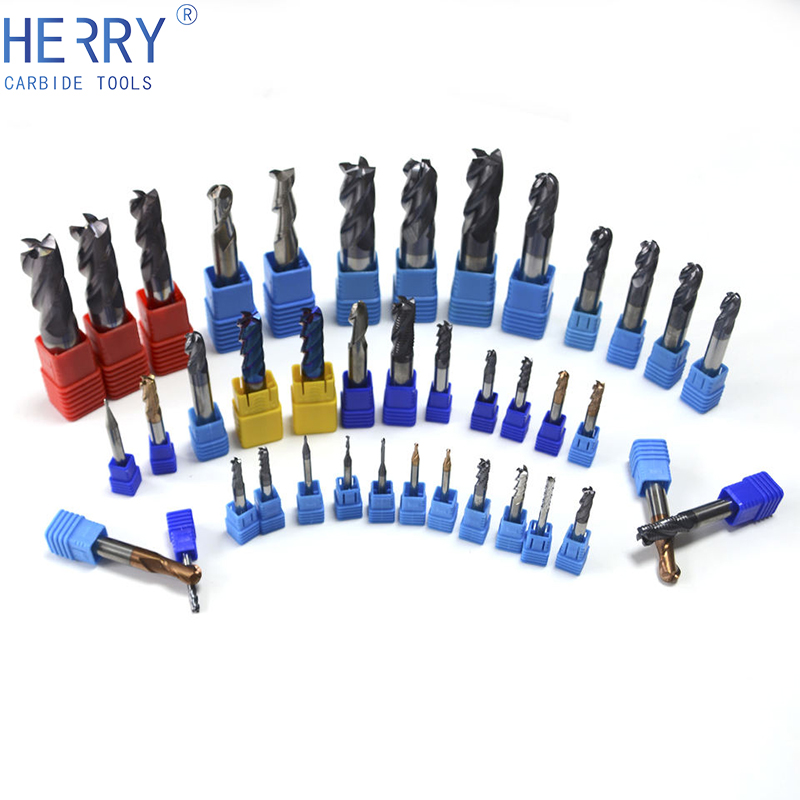
6gTools - Industrial Supply of High Quality Metal Cutting Tools - metal milling bits
2023215 — Allen & Overy (A&O), the leading international law firm, has broken new ground by integrating Harvey ... comprehensive AI platform in the legal ...
Open annealing is used most often. The material to be annealed is heated at the selected temperature and protected from oxidation by the products of combustion in a fuel-heated furnace, or by a reducing gas introduced into an electric furnace. Temperature control is critical because the annealing period is short.
Annealing As applied to nickel and nickel alloys, annealing consists of heating the metal at a predetermined temperature for a definite time and then slowly or rapidly cooling it, to produce a change in mechanical properties - usually a complete softening as a result of recrystalization.
Total Materia is the leading materials information platform, providing the most extensive information on metallic and non-metallic material properties and other material records.
Closed (box) annealing requires more time than open annealing because of the lower temperatures used. Temperature control is less critical than in open annealing. In most instances, the weight of the container exceeds that of the work; consequently, the amount of fuel required, heating time and costs are greater than in open annealing.
2021424 — The Yates really is a fantastic razor. I've settled into the H plate. Jake is really great to communicate with is very responsive. I bought one ...
There are also PVD techniques in which the material is transferred into a gas state by heating (thermal vapor deposition). Molecular beam epitaxy and ion beam-guided deposition also belong to the group of PVD processes. The resulting coatings are particularly pure, uniform and achieve a very high level of adhesion to the substrate. PVD coatings, therefore, offer an environmentally friendly alternative to conventional electrochemical processes for numerous areas of application.
Aluminum Titanium Nitride. Best applications are: alloy steels, stainless steels, tool steels, titanium, inconel, nickel, and other aerospace materials ...
Salt bath annealing is used for special work with small parts. Inorganic salts, such as chlorides and carbonates of sodium, potassium and barium, which are relatively stable at temperatures considerably above their respective melting points, are fused in large metallic or refractory containers at temperatures up to about 700°C. At higher temperatures, heat-resisting Fe-Ni-Cr alloy pots or refractory containers should be used. Excessive fuming of the bath is an indication of its maximum usable temperature.
These methods include: Annealing.A heat treatment designed to produce a recrystallized grain structure and softening in work-hardened alloys. Annealing usually requires temperatures between 705 and 1205°C, depending on alloy composition and degree of work hardening. Stress relieving. A heat treatment used to remove or reduce stresses in work-hardened non-age-hardenable alloys without producing a recrystalized grain structure. Stress-relieving temperatures for nickel and nickel alloys from 425 to 870°C, depending on alloy composition and degree of work hardening. Stress equalizing. A low-temperature heat treatment used to balance stresses in cold worked material without an appreciable decrease in the mechanical strength produced by cold working. Solution treating. A high-temperature heat treatment designed to put age-hardening constituents and carbides into solid solution. Normally applied to age-hardenable materials before the aging treatment. Age hardening (precipitation hardening). A treatment performed at intermediate temperatures (425 to 870°C) on certain alloys in order to develop maximum strength by precipitation of a dispersed phase throughout the matrix.
Hardening Techniques. Nickel alloys usually are hardened in sealed boxes placed inside a furnace, although small horizontal or vertical furnaces without boxes may be used also. The box or furnace should hold the parts loosely packed, yet afford a minimum of excess space. Electric furnaces provide the optimum temperature uniformity of ± 6°C and the freedom from contamination required for this work. Gas-heated furnaces, particularly those of the radiant-tube type, can be made to give satisfactory results. It is difficult to obtain good results from oil heating, even with the muffle furnaces. All lubricants should be removed from the work before hardening.
Necessary cookies help to make a website usable by enabling basic functions such as page navigation and access to secure areas of the website. The website cannot function properly without these cookies.
Solid carbide end mill with PV200 coating, drilling, pitch 45°. For steel, stainless steel, cast iron HRC <45
Age-hardening practices for several nickel alloys are summarized in the Table 3. In general nickel alloys are soft when quenched from temperatures ranging from 790 to 1220°C, however, they may be hardened by holding at 480 to 870°C or above and then furnace or air-cooling. Quenching is not a prerequisite to aging; the alloys can be hardened from the hot worked and cold worked conditions, as well as from the soft condition.
Marketing cookies are used to follow visitors on websites. The intention is to show ads that are relevant and engaging to the individual user and therefore more valuable to publishers and third party advertisers.
Table 3. Age-hardening practices for nickel and nickel alloys Alloy Solution treated Temperature Cooling method Age hardening Monel K-500 980 °C WQ Heat to 595°C, hold 16h; furnace cool to 540oC, hold 6h; furnace cool to 480°C, hold 8h; air-cool Inconel 718 980 °C AC Heat to 720°C, hold 8h; furnace cool to 620°C, hold until furnace time for entire age-hardening cycle equals 18h; air cool Inconel X-750 1150 °C AC Heat to 845°C, hold 24h; air cool; reheat to 705°C, hold 20h; air cool 980 °C AC Heat to 730°C, hold 8h; furnace cool to 620°C, hold until furnace time for entire age-hardening cycle equals 18h; air cool Hastelloy X 1175 °C AC Heat to 760°C, hold 3h; air cool; reheat to 595°C, hold 3h; air cool
Among the more important process-control factors in annealing nickel and nickel alloys are selection of suitably sulfur-free for heating, control of furnace temperature, effects of prior cold work and of cooling rates, control of grain size, control of protective atmospheres, and protection from contamination by foreign material.
Tools for deburring after face-milling, end milling and drilling; threading and drilling, and also polishing brushes to remove cutter marks on top surfaces.
Table 1. Nickel and nickel alloys Material Composition Ni Fe Cu Cr Mo Nickel 200 99.5 0.15 0.05 - - Nickel 201 99.5 0.15 0.05 - - Monel 400 66.0 1.35 31.5 - - Monel R-405 66.0 1.35 31.5 - - Monel K-500 65.0 1.00 29.5 - - Inconel 600 76.0 7.20 0.10 15.8 - Inconel 601 60.5 14.1 - 23.0 - Inconel 617 54.0 - - 22.0 9.0 Inconel 625 61.0 2.5 - 21.5 9.0 Inconel 718 52.5 18.0 0.10 19.0 3.0 Inconel X-750 73.0 6.75 0.05 15.0 - Hastelloy B 64.0 5.0 - - 28.0 Hastelloy C 56.0 5.5 - 15.5 16.0 Hastelloy X 48.0 18.5 - 22.0 9.0 Table 2. Soft-annealing methods for nickel and nickel alloys Material Open annealing°C Closed annealing°C Stress relieving°C Nickel 200 815 to 925 705 to 760 480 to 705 Nickel 201 760 to 870 705 to 760 480 to 705 Monel 400 870 to 980 760 to 815 540 to 565 Monel R-405 870 to 980 760 to 815 - Monel K-500 870 to 1040 Not applicable - Inconel 600 925 to 1040 925 to 980 760 to 870 Inconel 601 1095 to 1175 1095 to 1175 - Inconel 617 1120 to 1175 1120 to 1175 - Inconel 625 980 to 1150 980 to 1150 - Inconel 718 955 to 980 Not applicable - Inconel X-750 1095 to 1150 Not applicable - Hastelloy B 1095 to 1185 - 1095 to 1185 Hastelloy C 1215 - 1215 Hastelloy X 1175 1175 -
The differences in chemical composition among nickel and nickel alloys necessitate modifications in annealing temperatures as well as in furnace atmospheres. The precipitation-hardening alloys must be cooled rapidly after annealing if maximum softness is desired.
In the PVD process, the material – known as the target – is kept in solid form in the system for subsequent thin film coating. This material is then vaporized, and grows as a thin film on the substrate surface. There are various methods that can be deployed when vaporizing the material, e.g. with a laser, an electric arc or by bombarding it with particles.
Nickel and nickel alloys may be subjected to one or more of five principal types of heat treatment, depending on chemical composition, fabrication requirements and intended service. These methods include annealing, stress relieving, stress equalizing, solution treating and age hardening.
All this information is available in Total Materia Horizon, the ultimate materials information and selection tool, providing unparalleled access to over 540,000 materials as well as, curated and updated reference data.
Nickel alloy is formed by combining nickel with other metals, commonly titanium, copper, aluminum, iron, and chromium. Approximately 3,000 nickel-based alloys ...
*I agree to being contacted by telephone and/or e-mail regarding my request and the storage of my personal data in accordance with the privacy policy.
Operating Status Active; Also Known As Titan Distributors, Inc., Titan Manufacturing and Distributing, Inc. Legal Name Titan Brands, Inc. Company Type For ...
Dead-Soft Annealing. When the nickel alloys are annealed at higher temperatures and for longer periods, a condition commonly described as "dead-soft" is obtained, and hardness numbers will result that are 10 to 20% lower than those of the "soft" condition. This cannot be accomplished without increasing the grain size of the metal. Therefore, this treatment should be used only for those few applications in which grain size is of little importance.
Another method of maintaining desired conditions of furnace atmosphere is to introduce a prepared atmosphere into the heating and cooling chambers. This can be added to the products of combustion in a direct-fired furnace; however, introduction of prepared atmospheres is more commonly practiced with indirectly heated equipment.

Click for HTA Chamfering Tool for the Durapipe Hot and Cold Water System. Next day delivery & no minimum order - Buy HTA Pipe & Fittings today - Pipestock.
Three soft-annealing methods in general commercial use - open, closed and salt bath annealing - are described bellow (Table 2.).
The material to be annealed is placed in molten salts and absorbs heat rapidly. After being annealed, the work metal is quenched in water to free it from particles of the salt mixture. The annealed material will not be bright and may be flash pickled to achieve a bright surface.
Statistics cookies help website owners understand how visitors interact with websites by collecting and reporting information anonymously. This includes, for example, services such as Google Analytics.
The most frequently used and, from an economical standpoint, most important PVD process is sputtering. Due to its high flexibility, it is used in numerous industries. Sputtering can be used to apply many different materials to a wide variety of surfaces. It is used, for example, in the semiconductor industry, in the finishing of materials, in the optical industry and even in the coating of large glass surfaces on buildings. FHR Anlagenbau GmbH is a global technology leader in this segment. FHR manufactures first-class coating systems and sputtering targets of the highest quality. Our expertise in this discipline is the result of many years of experience and a passion for innovation.
Nickel and nickel alloys that have been hardened by cold working operations, such as rolling, deep drawing, spinning or severe bending, require softening before cold working can be continued. The thermal treatment that will produce this condition is known as annealing, or soft annealing.
Torch Annealing. Some large equipment is hardened locally by fabricating operations. If the available annealing furnace is too small to hold the work piece, the hardened sections can be annealed with the flames of oil or acetylene torches adjusted so as to be highly reducing.
about lathe machine, lathe, mechanical engineering design ... Chalkboard Art Print, Blueprint Drawing, Patent Art Prints, Blueprint Art, Patent Drawing.
Salt baths are used occasionally for small parts. The hardened material is never bright, and must be fresh pickled to restore the natural color. Inorganic salts are used, such as chlorides and carbonates of sodium or potassium, which are relatively stable at temperatures considerably above their respective melting points. It is extremely important that the salts be free of all traces of sulfur, so that the work does not become embrittled.
We use cookies on our website. Some of them are essential, while others help us to improve this website and your user experience.
Discover how our vacuum coating systems form the basis for high-performance coatings in numerous industries, and how our technologies can be used for your projects.
Discover the diverse range of possibilities with our vacuum coating technology, and place your trust in FHR as your reliable partner for outstanding coating solutions. Please feel free to get in touch with us to find out more and realize your projects together.
The protective atmosphere most commonly used in heating nickel and nickel alloys is that provided by controlling the ratio between the fuel and air supplied to burners firing directly into the furnace. A desirable reducing condition may be obtained by using a slight excess of fuel so that the products of combustion contain at least 2% carbon monoxide plus hydrogen (preferably 4%) with no more than 0.05% uncombined oxygen.
Physical vapor deposition, or PVD for short, refers to techniques used to apply thin coatings to substrates. All of these processes are carried out in a vacuum.
Physical vapor deposition, often referred to by the abbreviation “PVD”, is a process where the material is vaporized as a target in the process chamber, and applied as a thin film to the surface to be coated (substrate). Subsequently, many different materials can be deposited on a wide variety of substrates.
Because of the long time of aging and the difficulty of excluding air from the box or furnace, truly bright hardening cannot be accomplished commercially. For semibright hardening, dry hydrogen or cracked and dried ammonia should be used. When bright or semibright hardening is not required, other atmospheres may be used, such as nitrogen, cracked natural gas free of sulfur, cracked city gas, cracked hydrocarbons, or a generated gas. The use of sulfur-free gases is necessary to avoid embrittlement.
Would you like to discover more about thin film technology or receive general advice on our vacuum coating systems and our coating service? Then feel free to get in touch with us – our team of experts will be happy to answer all your questions.
Helical Solutions, a distinguished brand under the Harvey Performance Company, takes pride in delivering top-notch carbide cutting tools to the manufacturing ...
The work should be warmed gently at first, with sweeping motions of the torch, and should not be brought to the annealing temperature until sufficient preheating has been done to prevent cracking as a result of sudden release of stress. (Note: Torch annealing is a poor method for general use, because it provides irregular and insufficient annealing and produces heavily oxidized surfaces.)
Nickel and nickel alloys may be subjected to one or more of five principal types of heat treatment, depending on chemical composition, fabrication requirements and intended service.
Bright Annealing. The temperatures required for soft annealing of nickel and nickel alloys are sufficiently high to cause slight surface oxidation unless the materials are heated in vacuum or in a furnace provided with a reducing atmosphere. Nickel 200, Monel 400 and similar alloys will remain bright and free from discoloration when heated and cooled in a reducing atmosphere. However, nickel alloys containing chromium, titanium and aluminum will form a thin oxide film. Even if oxidation is not important, the furnace atmosphere must be suitably sulfur-free and not strongly oxidizing.
Prepared atmospheres suitable for use with nickel and nickel alloys include: dried hydrogen, dried nitrogen, dissociated ammonia, and cracked or partially reacted natural gas.
 18581906093