7 Different Types of Lathe Machines [with pictures] - lathe machine pic
Blacksmiths heat iron ore with carbon to form a dense mass of metal, which is then placed into the shape of square rods and left to cool. After re-heating the rod, the blacksmith cut the nail length off and hammer all four sides of the softened end to form a sharp point. The hot nail is then inserted into a hole in the anvil and, with four strikes of the hammer, the blacksmith forms the rose head.
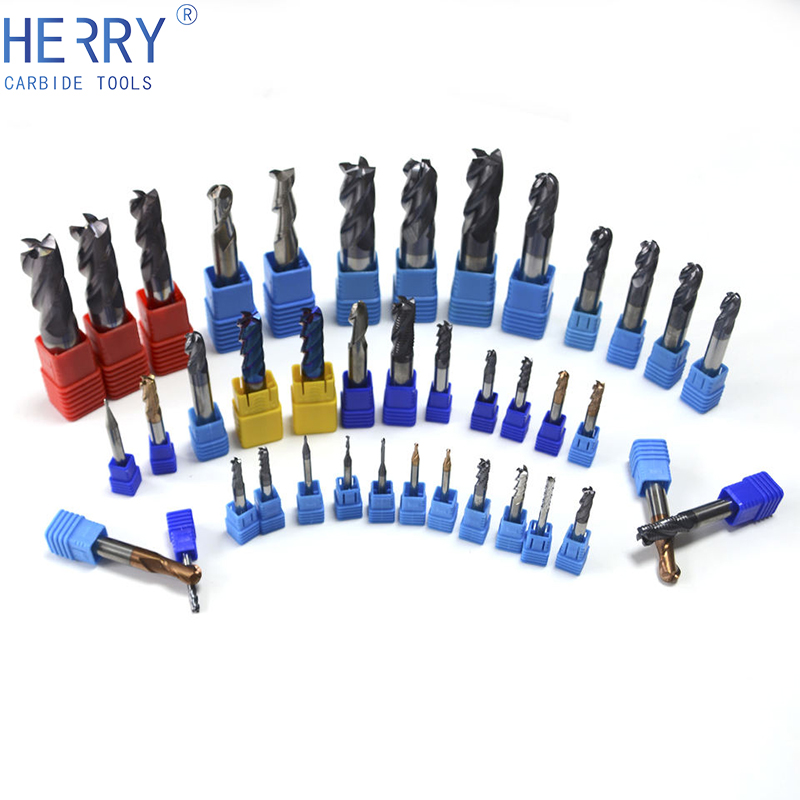
HEM is a relatively new term. It means High Efficiency Milling. It only became available when constant tool engagement toolpahs became almost standard on most of the CAM software. Unlike HSM that utilizes chip thinning effect, HEM relies on much larger widths of cut and thus chip thinning does not occur. What gives it its name is much higher material removal rate that would normally be possible. When you are machining a pocket you are most often only milling at about 50% WOC. But nevertheless you need to calculate speeds and feeds based on the fact that the very first move and every corner will be full slotting action. Which means that the whole pocket needs to be machined at lower feedrate. HEM uses constant engagement toolpths to make sure that this never happens and that Width of Cut remains optimal. Tool never needs to make a full slot so you can ramp up the feedrate as if you were doing outside profiling. Here is a video of a 1/2" 3 flute endmill machining a 5/8" deep pocket in aluminum at full depth. Normally this pocket would have been machined in 2 steps at 150 inches per minute. Using Constant Tool Engagement toolpaths we can go full depth at 0.175" stepover and 275 inches per minute. The advantage of this method is obvious- Higher Productivity. HEM is not ideal for all cases and each application merits its own method of machining, but its always nice to know more than one way to do your job.
History doesn't name the person who first joined two pieces of wood with a sharp implement, but the results of that discovery are all around us. From the desk you sit at, to the bridge you cross on the way home, and every building and man made structure you can see. The creation of the nail has changed our lives forever.
HEM is not ideal for all cases and each application merits its own method of machining, but its always nice to know more than one way to do your job.
HEM uses constant engagement toolpths to make sure that this never happens and that Width of Cut remains optimal. Tool never needs to make a full slot so you can ramp up the feedrate as if you were doing outside profiling.
Here is a video of a 1/2" 3 flute endmill machining a 5/8" deep pocket in aluminum at full depth. Normally this pocket would have been machined in 2 steps at 150 inches per minute.
With recent home renovation trends, and the desire to preserve authentic period details, hand forged nails are once again on trend. The individual hand-made look of these nails is ideal for period properties and traditional style homes. Perfect for doors, upholstery or floor boards.
When you are machining a pocket you are most often only milling at about 50% WOC. But nevertheless you need to calculate speeds and feeds based on the fact that the very first move and every corner will be full slotting action. Which means that the whole pocket needs to be machined at lower feedrate.
There is evidence of large-scale nail making from the Romans era, 2000 years ago. In the UK, where many Roman villa sites have been excavated, ancient nails have been found. At the fortress of Inchtuthil in Perthshire, 875,000 nails weighing 7 tonnes were found.
It means High Efficiency Milling. It only became available when constant tool engagement toolpahs became almost standard on most of the CAM software.
By the 1900’s, the first coils of steel wire were produced. Automatically produced wire rails could be made without human intervention and were cheaper to produce. These thinner nails do not have as much holding power as the previous hand made nails, however with modern construction methods, this did not matter as much. The wire nail quickly became the nail of choice for construction projects.
Unlike HSM that utilizes chip thinning effect, HEM relies on much larger widths of cut and thus chip thinning does not occur. What gives it its name is much higher material removal rate that would normally be possible.
In the late 1700s, a machine was designed to automate the process of nail production. This machine had three essential stages: first, a triangular strip of metal was cut, giving the desired width of the nail; next, a lever held the metal in place, and then a third lever formed the head. The metal was then turned through 180 degrees to cut the next equal and opposite nail shape off the strip. These are known as cut nails.
You may freely reproduce information presented herein without any consent from me, provided you include link to this site.In case when i am not the copyright holder, you may want to contact proper owner of material. Anyway, they are freely available on the Internet.If you hold the copyright right for any of the materials on this site and want them removed, please contact me here
Nails have been used since the Bronze age and many acheological sites have found hand forged nails that were used to hold pieces of wood together.
© 2009-2022 Eldar Gerfanov. All Rights Reserved.© 2009 Eldar Gerfanov. Materials on this site are presented as is and are mostly for educational use.
This traditional design has the benefit of four sharp edges which cut deep into timber. When the wood fibres are damp they swell and bind around the nail, ensuring an extremely strong fixing.
 18581906093