8 Unique Facts About Thread Forming Taps - In The Loupe - 4-40 roll tap drill size
One thing to remember is to make chips, not dust. Chips will help by removing the heat produced in the cutting process thus increasing tool life and improving edge quality. Feeds and speeds are usually all set in the programming software that is used to create the machine program. There are many resources available to help determine suitable settings for particular material/router bit combinations.
To calculate the overall star rating and percentage breakdown by star, we don’t use a simple average. Instead, our system considers things like how recent a review is and if the reviewer bought the item on Amazon. It also analyses reviews to verify trustworthiness.
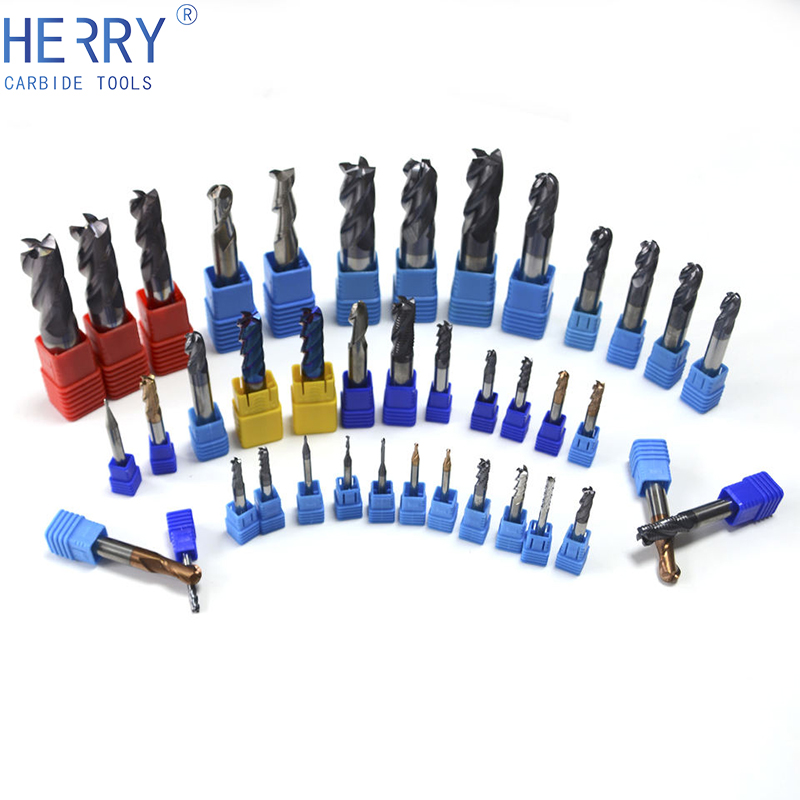
Milling speeds and feeds ChartMetric
End MillSpeeds and Feeds chart
If you agree, we may use your personal information from any of these Amazon services to personalize the ads we show you on other services. For example, we may use your Prime Video Watch history to personalize the ads we show you on our Stores or on Fire TV. We may also use personal information we receive from third parties (like demographic information).
In any case, we use cookies and similar tools that are necessary to enable you to make purchases, to enhance your shopping experiences and to provide our services, as detailed in our Cookie notice. We also use these cookies to understand how customers use our services (for example, by measuring site visits) so we can make improvements. Click “Decline” to reject, or “Customise” to make more detailed advertising choices, or learn more. You can change your choices at any time by visiting Cookies and advertising choices. To learn more about how and for what purposes Amazon uses personal information (such as Store order history or Prime Video Watch history) and cookies, please visit our Privacy notice and our Cookie notice.
N = number of cutting edges (flutes)T = chip load (chip per tooth) is the amount of material, which should be removed by each tooth of the cutter as it rotates and advances into the work (mm per tooth)Z = RPM, the speed at which the cutter revolves in the spindle (Revolutions per minute)We will now break down the relationship between the Feed rates, number of cutting edges, chip load and RPM. For most materials, there is a recommended chip load.
End Millspeeds and feedscalculator
To obtain the optimum Chip load, you must consider these variables, along with the machine and materials you intend to cut. This will help you find the best feed rate and RPM for any given tool and material.
For most material that you will be cutting on a CNC router you will typically set the RPM between 12000 and 24000, and adjust your feed rate to obtain the required results. The speeds and feeds chosen can be affected by the power of the spindle being used. Higher power spindles will produce more torque thus allowing the machine to run at a variety of RPM’s (torque drops off as the RPM is reduced).
Carbide End MillSpeeds and Feeds chart
Even though there are formulas for calculating feed rates you will find that the optimum feed rate will be determined from experience. You will typically start off with the calculated feed rate. Under ideal conditions, it is usually suggested that the actual feed rate be set to approximately one-half the calculated amount and gradually increased to the capacity of the machine and the finish desired.
Therefore depending on the diameter of the tool, if the RPM and number of cutter edges stay the same chip load will increase with a larger diameter cutter, thus the feed rate will also increase. When machining softer materials or using a stubby router bit the chip load can be increased. If an extra long router bit is being used, the chip load should be decreased.
Carbide end Mill RPMchart
Customer Reviews, including Product Star Ratings, help customers to learn more about the product and decide whether it is the right product for them.
The feed rate used depends upon a variety of factors, including power and rigidity of the machine, rigidity of part hold-down, spindle horsepower, depth and width of cut, sharpness of cutting tool, design and type of cutter, and the material being cut.
When material is machined the cutter must revolve at a specific RPM and feed at a specific feed rate to achieve the proper Chip load. There are also several factors to be considered when choosing the proper RPM and feed rate.
Carbide end millspeeds and feedscalculator
Based on this equation, as RPM increases, the feed rate will also increase if all other settings remain the same. If the number of cutting edges changes, however, the feed rate will either increase or decrease depending on whether the number goes up or down. The same applies to chip load if the recommended chip load is 0.1 mm/tooth the RPM, feed or number of cutting edges may go up or down to maintain the required chip load. Therefore if the chip load remains the same, and the feed rate increases, either the RPM and or number of cutting edges must increase to maintain the recommended chip load.
Specification: : Shank Type: Hex Shank Colour: silver. Material: Zinc Alloy + Chrome Vanadium Steel + Alloy Size: 1/8"-3/4"(3mm-19mm) RPMs Drill Usage: 0-400 Features: 1. The threaded rod deburrer body is made of zinc alloy, which gives it hardness, durability and helps prevent abrasion. 2. Suitable for stainless steel, hardened steel, mild steel, copper, brass, plastic and many more. 3. Quickly repairs damaged bolts and tightens nuts in place without hurting your hand, sparks and burns. Package includes: 1 x External Deburring and Chamfering Tool
Another factor is depth of cut. Depth of cut will affect edge finish as well as tool life. You will have to adjust your depth to achieve the desired results depending on the type of material and size of the cutter. Usually, a depth of cut that equals the radius of the cutter is a good starting point when cutting non-ferrous metals.
When calculating the feed rate for any material the chip load is therefore one of the most important factors to be taken into account because the chip load determines the amount of material that each tooth will remove, plus the load that each tooth will have to take. Another factor that affects chip load is the diameter of the cutter. A larger cutter will be able to handle a larger chip load.
- Cut too deep in a single pass. Sometimes it can be more efficient to use a higher feed rate and two or more passes rather than a single cut at a low feed rate
HSS end millSpeeds and Feeds Chart
If you are running at 18000 RPM using a 25mm cutter with two flutes, and a recommended chip load of 0.1 mm/tooth:Feed = 2 x 0.1 x 18000 = 3600 mm per minIf the RPM were increased to 24000 RPM the new feed rate would work out to be:Feed = 2 x 0.1 x 24000 = 4800 mm per min
These often provide a good starting point but can usually be further improved through a small amount of trial and error. Most machine controllers allow you to adjust the feed rate while a program is running and by listening to the sound the cutter makes this can be a good way of optimizing the parameters.Feed rate is calculated using the following equation:
1. The threaded rod deburrer body is made of zinc alloy, which gives it hardness, durability and helps prevent abrasion.
If you agree, we may use your personal information from any of these Amazon services to personalize the ads we show you on other services. For example, we may use your Prime Video Watch history to personalize the ads we show you on our Stores or on Fire TV. We may also use personal information we receive from third parties (like demographic information).In addition, if you agree, we’ll also use cookies to complement your shopping experience across the Amazon stores as described in our Cookie notice. Your choice applies to using first-party and third-party advertising cookies on this service. Cookies store or access standard device information such as a unique identifier. The 96 third parties who use cookies on this service do so for their purposes of displaying and measuring personalised ads, generating audience insights, and developing and improving products.In any case, we use cookies and similar tools that are necessary to enable you to make purchases, to enhance your shopping experiences and to provide our services, as detailed in our Cookie notice. We also use these cookies to understand how customers use our services (for example, by measuring site visits) so we can make improvements. Click “Decline” to reject, or “Customise” to make more detailed advertising choices, or learn more. You can change your choices at any time by visiting Cookies and advertising choices. To learn more about how and for what purposes Amazon uses personal information (such as Store order history or Prime Video Watch history) and cookies, please visit our Privacy notice and our Cookie notice.
Milling speeds and feeds chartpdf
Once you have determined what feed and speed to start with, there are other factors to be taken into consideration. The next thing to be considered is the direction of the cut, which is the direction the cutter is fed into the material. Conventional milling or cutting forward is the most commonly used method. With this method, the work is fed against the rotation direction of the cutter. The other method is climb milling or cutting reverse. For this machining method, the workpiece and the machine must be rigid. When machining non-ferrous materials, climb milling should be used to achieve a good finish.
- Forget that doing some test cuts on a spare piece of material is a good way of checking settings before running your main program
In addition, if you agree, we’ll also use cookies to complement your shopping experience across the Amazon stores as described in our Cookie notice. Your choice applies to using first-party and third-party advertising cookies on this service. Cookies store or access standard device information such as a unique identifier. The 96 third parties who use cookies on this service do so for their purposes of displaying and measuring personalised ads, generating audience insights, and developing and improving products.
 18581906093