VI-PRO End Mills-5 Flute-Square - flat end mill
Forum Responses (CNC Forum) From contributor M: Rule of thumb for me is to conventional cut panel products and climb cut solids. Connventional cutting would be cutting counterclockwise around the outside of a part and clockwise on the inside of a cutout. Conventional cutting will give you a better surface finish on melamine and laminated products. Your bits will tend to last longer, stay cooler and put less horizontal pressure on the part. That said, if your cut quality is better with a climb cut, and the edge quality is important, throw out that junk I just said and go with what works best for your application. From contributor J: I was told by a rep from Onsrud to cut in the direction that gives you the best finish. She said make a cut and look at both the good part and the waste and if the waste cut looks better than the good part, reverse the direction. From contributor T: Ive always heard it explained this way. The direction of cut is a function on the cutter more than the material being cut. (And yes, there will always be some exceptions.) The two primary cutting materials used are carbide and high speed steel. Carbide (also known as cemented carbide) has grains of carbide glued together with a binder, commonly cobalt, to create the cutting edge. If you were to zoom up on the edge, with an electron microscope, you would see grains of carbide held in place by the binder material. It's kind of like a chunk of concrete - gravel is held together by a gypsum binder. Carbide is the actual cutting material but it does not make up 100% of the edge. For this reason the edge of carbide is not as keen (or sharp) as a high speed steel tool. The main advantage of carbide it that it is harder than high speed steel. Hardness adds abrasion resistance. It is the abrasion resistance that makes the tool last longer. But the down side is, because the edge isnt as sharp if you cut with a conventional tool path, the cutter rubs a bit, beginning at the tangency point and until it digs into the chip. This small amount of dragging creates heat and friction, which degrades the surface quality and wears the tool. By contrast, climb cutting starts at the thickest part of the chip and cuts to the thinnest part, which is at the tangency point. Its common to see a better edge when climb cutting with a carbide tool because the tool does not rub at the tangency. Even if you cut with the full width of the cutter, there is still a side of the cut that shows climb cut characteristics. You will need a solid machine to do climb cutting because vibration will break the cutter, due to it being brittle because of the hardness. From contributor K: Contributors M and T are right on and there is no arguing with contributor J's logic. Consider also: when I onionskin, I climb the first pass and conventional cut the second. The climb pulls the bit a very small amount away from the work and the conventional cut runs pretty true (since there is less material being cut away). Before adopting this method I often had a small lip at the step level due to machine/tool torsion forces or stress relief in the panel. The small cost in bit life for me is outweighed by the overall better quality of the edge. Every system is different; this just works (after a whole lot of experimentation) best for me. From the original questioner: Thank you all. What seemed to be sort of a boring question really generated some thought provoking answers. Contributor K, I have been trying to resolve the same lip issue you've mentioned. I'm not sure if my software will allow for a climb-cut then conventional pass (Microvellum... will have to check it out) but two passes with a climb cut seems to manage a lot better than two with conventional. Contributors M and T seem to conflict on which passing method generates the most heat. There seems to be logic to support either answer. I may just buy a temperature sensor to check if there is an appreciable difference. From contributor K: Try also a few hundredths separation between parts in the nest. This lip issue is deceptive. Took me a while to figure it out. It can occur when climb cutting nests with no separation between parts, as all the deflective force on climb can push the bit slightly into the adjacent part. In other words, the first cut is most of the way through and climb, lots of side force, away from the work piece. This pulls the bit slightly into the adjacent part. Then the conventional cut with very little force runs perfectly true. Result is a small step caused by the path from an adjacent part. If this is the case, you will see the step in the center of the nest but not on the edges of the sheet where no adjacent part exists. It also can be deceptive because it only happens for new bits. Machine compensation for sharpened bits can mask the effect by effectively creating this part separation at the machine, but not in the software. You use Microvellum, I use AlphaCam, but the idea is the same. For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
By contrast, climb cutting starts at the thickest part of the chip and cuts to the thinnest part, which is at the tangency point. Its common to see a better edge when climb cutting with a carbide tool because the tool does not rub at the tangency. Even if you cut with the full width of the cutter, there is still a side of the cut that shows climb cut characteristics. You will need a solid machine to do climb cutting because vibration will break the cutter, due to it being brittle because of the hardness. From contributor K: Contributors M and T are right on and there is no arguing with contributor J's logic. Consider also: when I onionskin, I climb the first pass and conventional cut the second. The climb pulls the bit a very small amount away from the work and the conventional cut runs pretty true (since there is less material being cut away). Before adopting this method I often had a small lip at the step level due to machine/tool torsion forces or stress relief in the panel. The small cost in bit life for me is outweighed by the overall better quality of the edge. Every system is different; this just works (after a whole lot of experimentation) best for me. From the original questioner: Thank you all. What seemed to be sort of a boring question really generated some thought provoking answers. Contributor K, I have been trying to resolve the same lip issue you've mentioned. I'm not sure if my software will allow for a climb-cut then conventional pass (Microvellum... will have to check it out) but two passes with a climb cut seems to manage a lot better than two with conventional. Contributors M and T seem to conflict on which passing method generates the most heat. There seems to be logic to support either answer. I may just buy a temperature sensor to check if there is an appreciable difference. From contributor K: Try also a few hundredths separation between parts in the nest. This lip issue is deceptive. Took me a while to figure it out. It can occur when climb cutting nests with no separation between parts, as all the deflective force on climb can push the bit slightly into the adjacent part. In other words, the first cut is most of the way through and climb, lots of side force, away from the work piece. This pulls the bit slightly into the adjacent part. Then the conventional cut with very little force runs perfectly true. Result is a small step caused by the path from an adjacent part. If this is the case, you will see the step in the center of the nest but not on the edges of the sheet where no adjacent part exists. It also can be deceptive because it only happens for new bits. Machine compensation for sharpened bits can mask the effect by effectively creating this part separation at the machine, but not in the software. You use Microvellum, I use AlphaCam, but the idea is the same. For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
Finally, as we have mentioned before, the concrete screw allows faster installations, since the number of steps necessary for installation is reduced. It also provides flexibility, since if you need to, you can remove the screw once it has been installed. This is perfect for those times when a project changes or a mistake is made, and the fastener placement needs to be readjusted.
Masonry Nails forconcrete
For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
Get the best deal for Dremel Carbide Burr In Metalworking Cutting Tool Bits from the largest online selection at eBay.ca. | Browse our daily deals for even ...
Start by slowly drilling your hole to make sure you have control when first drilling in to concrete. Once you have an established hole you will be able to drill faster.
A hammer drill has the function of a hammer, which consists of the drill bit not only rotating on itself but also making a small movement back and forth to break the material and facilitate drilling. In the case of concrete, the hammering helps to pulverize the concrete, while the rotation forms the hole.
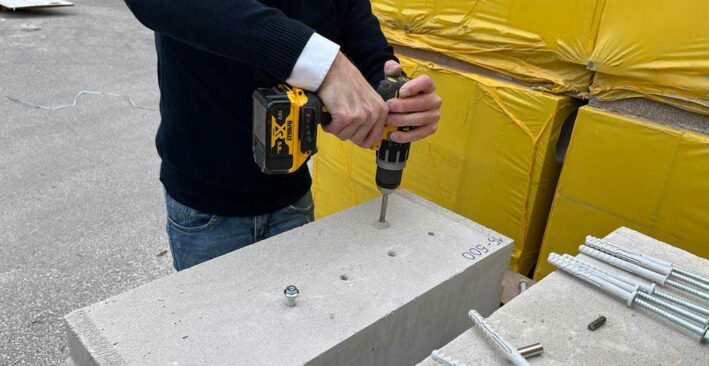
Get your drill ready by setting the depth control bar if you have one or mark on the drill where you should drill up to. This will depend on the length of the screw or anchor you are trying to fix and the thickness of the application you are installing.
Can you nail into concreteslab
PROTECTION – Magnetic chip catchers are a fantastic way of protecting your valuable components from harmful metal shavings. Hot metal chips can cause ...
Concrete screws come with two types of heads: Hex Head and Flat Head Screws. Hex screws are easier to fit but don’t look as good because the head is raised and doesn’t sit flush with the surface, so your choice depends on the location of the screw.
Jun 2, 2022 — The ability of a material to resist wear, tear, scratching, and abrasion is called hardness. Some examples of hard materials are diamond ...
Chemical anchors provide a more flexible option to mechanical anchors for heavy duty fixings. They can be used close to the edge and have shorter spacing distances because they do not exert stress on the base material. They can also be used with many different base materials other than concrete.
Sleeve anchors are used to connect structural and non-structural elements to concrete, it is an excellent solution for installations on the wall due to its thicker width providing a higher shear resistance
Concrete screws come with different types of heads, including pan or hex head as well as connecting or internal thread heads. Your choice of screw will depend on the application and location of the installation.
How to hammernail into concretewall without drill
To install a screw into concrete all you have to do is drill a hole in the concrete and drive the screw. Concrete screws are an excellent option when looking to fasten close to an edge, as there is no expansion and pressure on the base material is reduced.
While it might not always be necessary it is recommend that you mark where you will need to drill for your fixings, especially if you need to drill multiple holes to balance the loads.
Although the installation process may seem easy, you have to make sure you follow the correct installation process according to the ETA. This includes things like cleaning out the drill hole, using the correct amount of torque and not overtightening the screws.
How to put anailin a brick wall without a drill
Customers Ultimately Purchased · 3/32 in. x 1-1/2 in. · Powerbuilt. Serpentine Belt Tool Kit · Husky. Screwdriver Set (15-Piece) · Everbilt. 5/32 in. · VEVOR.
Frame fixings such as the Multifunction frame plug MFR, are ETA approved for fixing in concrete. The long expansion area and early expansion achieved by the lateral bars ensure a secure hold, also providing them with high load values.
Fluted Masonry Nails
Tool is an American rock band formed in Los Angeles in 1990. It consists of vocalist Maynard James Keenan, guitarist Adam Jones, drummer Danny Carey and ...
On the other hand, it is also possible to drill concrete with a rotary drill, these take longer to drill the concrete compared to a hammer drill and require greater physical effort, in addition, the excess heat generated in the drill can break the drill bit.
Contributors M and T seem to conflict on which passing method generates the most heat. There seems to be logic to support either answer. I may just buy a temperature sensor to check if there is an appreciable difference. From contributor K: Try also a few hundredths separation between parts in the nest. This lip issue is deceptive. Took me a while to figure it out. It can occur when climb cutting nests with no separation between parts, as all the deflective force on climb can push the bit slightly into the adjacent part. In other words, the first cut is most of the way through and climb, lots of side force, away from the work piece. This pulls the bit slightly into the adjacent part. Then the conventional cut with very little force runs perfectly true. Result is a small step caused by the path from an adjacent part. If this is the case, you will see the step in the center of the nest but not on the edges of the sheet where no adjacent part exists. It also can be deceptive because it only happens for new bits. Machine compensation for sharpened bits can mask the effect by effectively creating this part separation at the machine, but not in the software. You use Microvellum, I use AlphaCam, but the idea is the same. For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
KBC,KBC PNEUMATIC HAND CHAMFER & DEBURR TOOL,1-829-1305,KBC Tools & Machinery.
ESEMAPCZXSXAZZ 100-Pack License For Ecostruxure Machine Advisor Pro - 12 Month -
Concrete nailgun
Mar 21, 2023 — What I'd like to learn from experienced CNC machinists is how you manage and organize your tool libraries. Do organize tools by vendor? By tooling material?
Even if you cut with the full width of the cutter, there is still a side of the cut that shows climb cut characteristics. You will need a solid machine to do climb cutting because vibration will break the cutter, due to it being brittle because of the hardness. From contributor K: Contributors M and T are right on and there is no arguing with contributor J's logic. Consider also: when I onionskin, I climb the first pass and conventional cut the second. The climb pulls the bit a very small amount away from the work and the conventional cut runs pretty true (since there is less material being cut away). Before adopting this method I often had a small lip at the step level due to machine/tool torsion forces or stress relief in the panel. The small cost in bit life for me is outweighed by the overall better quality of the edge. Every system is different; this just works (after a whole lot of experimentation) best for me. From the original questioner: Thank you all. What seemed to be sort of a boring question really generated some thought provoking answers. Contributor K, I have been trying to resolve the same lip issue you've mentioned. I'm not sure if my software will allow for a climb-cut then conventional pass (Microvellum... will have to check it out) but two passes with a climb cut seems to manage a lot better than two with conventional. Contributors M and T seem to conflict on which passing method generates the most heat. There seems to be logic to support either answer. I may just buy a temperature sensor to check if there is an appreciable difference. From contributor K: Try also a few hundredths separation between parts in the nest. This lip issue is deceptive. Took me a while to figure it out. It can occur when climb cutting nests with no separation between parts, as all the deflective force on climb can push the bit slightly into the adjacent part. In other words, the first cut is most of the way through and climb, lots of side force, away from the work piece. This pulls the bit slightly into the adjacent part. Then the conventional cut with very little force runs perfectly true. Result is a small step caused by the path from an adjacent part. If this is the case, you will see the step in the center of the nest but not on the edges of the sheet where no adjacent part exists. It also can be deceptive because it only happens for new bits. Machine compensation for sharpened bits can mask the effect by effectively creating this part separation at the machine, but not in the software. You use Microvellum, I use AlphaCam, but the idea is the same. For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
How to use masonry nails
The main advantage of carbide it that it is harder than high speed steel. Hardness adds abrasion resistance. It is the abrasion resistance that makes the tool last longer. But the down side is, because the edge isnt as sharp if you cut with a conventional tool path, the cutter rubs a bit, beginning at the tangency point and until it digs into the chip. This small amount of dragging creates heat and friction, which degrades the surface quality and wears the tool. By contrast, climb cutting starts at the thickest part of the chip and cuts to the thinnest part, which is at the tangency point. Its common to see a better edge when climb cutting with a carbide tool because the tool does not rub at the tangency. Even if you cut with the full width of the cutter, there is still a side of the cut that shows climb cut characteristics. You will need a solid machine to do climb cutting because vibration will break the cutter, due to it being brittle because of the hardness. From contributor K: Contributors M and T are right on and there is no arguing with contributor J's logic. Consider also: when I onionskin, I climb the first pass and conventional cut the second. The climb pulls the bit a very small amount away from the work and the conventional cut runs pretty true (since there is less material being cut away). Before adopting this method I often had a small lip at the step level due to machine/tool torsion forces or stress relief in the panel. The small cost in bit life for me is outweighed by the overall better quality of the edge. Every system is different; this just works (after a whole lot of experimentation) best for me. From the original questioner: Thank you all. What seemed to be sort of a boring question really generated some thought provoking answers. Contributor K, I have been trying to resolve the same lip issue you've mentioned. I'm not sure if my software will allow for a climb-cut then conventional pass (Microvellum... will have to check it out) but two passes with a climb cut seems to manage a lot better than two with conventional. Contributors M and T seem to conflict on which passing method generates the most heat. There seems to be logic to support either answer. I may just buy a temperature sensor to check if there is an appreciable difference. From contributor K: Try also a few hundredths separation between parts in the nest. This lip issue is deceptive. Took me a while to figure it out. It can occur when climb cutting nests with no separation between parts, as all the deflective force on climb can push the bit slightly into the adjacent part. In other words, the first cut is most of the way through and climb, lots of side force, away from the work piece. This pulls the bit slightly into the adjacent part. Then the conventional cut with very little force runs perfectly true. Result is a small step caused by the path from an adjacent part. If this is the case, you will see the step in the center of the nest but not on the edges of the sheet where no adjacent part exists. It also can be deceptive because it only happens for new bits. Machine compensation for sharpened bits can mask the effect by effectively creating this part separation at the machine, but not in the software. You use Microvellum, I use AlphaCam, but the idea is the same. For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
Contributor K, I have been trying to resolve the same lip issue you've mentioned. I'm not sure if my software will allow for a climb-cut then conventional pass (Microvellum... will have to check it out) but two passes with a climb cut seems to manage a lot better than two with conventional. Contributors M and T seem to conflict on which passing method generates the most heat. There seems to be logic to support either answer. I may just buy a temperature sensor to check if there is an appreciable difference. From contributor K: Try also a few hundredths separation between parts in the nest. This lip issue is deceptive. Took me a while to figure it out. It can occur when climb cutting nests with no separation between parts, as all the deflective force on climb can push the bit slightly into the adjacent part. In other words, the first cut is most of the way through and climb, lots of side force, away from the work piece. This pulls the bit slightly into the adjacent part. Then the conventional cut with very little force runs perfectly true. Result is a small step caused by the path from an adjacent part. If this is the case, you will see the step in the center of the nest but not on the edges of the sheet where no adjacent part exists. It also can be deceptive because it only happens for new bits. Machine compensation for sharpened bits can mask the effect by effectively creating this part separation at the machine, but not in the software. You use Microvellum, I use AlphaCam, but the idea is the same. For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
If you are wondering what concrete fasteners exist, here we will list some of the other most popular options on the market: sleeve anchors, chemical anchors, frame fixings and the concrete screws, each of them has different characteristics and the choice will depend on what you need.
To install a screw into concrete all you have to do is drill a hole in the concrete, clean out the hole and drive in the screw, no hammering required! Concrete screws are an excellent option when looking to fasten close to an edge, as there is no expansion and pressure on the base material is reduced.
Once you have drilled the hole it is important to make sure you clear it of any dust. Removing any dust will improve the strength and holding of the anchors. You could use an air pump, can of compressed air, or vacuum.
Drilling in concrete is difficult because concrete is dense, and has embedded aggregates that can get in the way of the drill bit – Drilling can quickly ruin drill bits. When the drill bit encounters an aggregate, it drags further. One of the most commonly used tools for drilling through concrete is a hammer drill.
Masonry Nails
Question Is there a standard rule for cutting out MDF on a nested based router, clockwise or counterclockwise (with a bit rotating clockwise)? I was told to cut out counterclockwise and always had. I've recently started onionskinning parts and notice I get much better cut quality cutting out clockwise. Just wanted to see what everyone else does before I change all my programming setups. Forum Responses (CNC Forum) From contributor M: Rule of thumb for me is to conventional cut panel products and climb cut solids. Connventional cutting would be cutting counterclockwise around the outside of a part and clockwise on the inside of a cutout. Conventional cutting will give you a better surface finish on melamine and laminated products. Your bits will tend to last longer, stay cooler and put less horizontal pressure on the part. That said, if your cut quality is better with a climb cut, and the edge quality is important, throw out that junk I just said and go with what works best for your application. From contributor J: I was told by a rep from Onsrud to cut in the direction that gives you the best finish. She said make a cut and look at both the good part and the waste and if the waste cut looks better than the good part, reverse the direction. From contributor T: Ive always heard it explained this way. The direction of cut is a function on the cutter more than the material being cut. (And yes, there will always be some exceptions.) The two primary cutting materials used are carbide and high speed steel. Carbide (also known as cemented carbide) has grains of carbide glued together with a binder, commonly cobalt, to create the cutting edge. If you were to zoom up on the edge, with an electron microscope, you would see grains of carbide held in place by the binder material. It's kind of like a chunk of concrete - gravel is held together by a gypsum binder. Carbide is the actual cutting material but it does not make up 100% of the edge. For this reason the edge of carbide is not as keen (or sharp) as a high speed steel tool. The main advantage of carbide it that it is harder than high speed steel. Hardness adds abrasion resistance. It is the abrasion resistance that makes the tool last longer. But the down side is, because the edge isnt as sharp if you cut with a conventional tool path, the cutter rubs a bit, beginning at the tangency point and until it digs into the chip. This small amount of dragging creates heat and friction, which degrades the surface quality and wears the tool. By contrast, climb cutting starts at the thickest part of the chip and cuts to the thinnest part, which is at the tangency point. Its common to see a better edge when climb cutting with a carbide tool because the tool does not rub at the tangency. Even if you cut with the full width of the cutter, there is still a side of the cut that shows climb cut characteristics. You will need a solid machine to do climb cutting because vibration will break the cutter, due to it being brittle because of the hardness. From contributor K: Contributors M and T are right on and there is no arguing with contributor J's logic. Consider also: when I onionskin, I climb the first pass and conventional cut the second. The climb pulls the bit a very small amount away from the work and the conventional cut runs pretty true (since there is less material being cut away). Before adopting this method I often had a small lip at the step level due to machine/tool torsion forces or stress relief in the panel. The small cost in bit life for me is outweighed by the overall better quality of the edge. Every system is different; this just works (after a whole lot of experimentation) best for me. From the original questioner: Thank you all. What seemed to be sort of a boring question really generated some thought provoking answers. Contributor K, I have been trying to resolve the same lip issue you've mentioned. I'm not sure if my software will allow for a climb-cut then conventional pass (Microvellum... will have to check it out) but two passes with a climb cut seems to manage a lot better than two with conventional. Contributors M and T seem to conflict on which passing method generates the most heat. There seems to be logic to support either answer. I may just buy a temperature sensor to check if there is an appreciable difference. From contributor K: Try also a few hundredths separation between parts in the nest. This lip issue is deceptive. Took me a while to figure it out. It can occur when climb cutting nests with no separation between parts, as all the deflective force on climb can push the bit slightly into the adjacent part. In other words, the first cut is most of the way through and climb, lots of side force, away from the work piece. This pulls the bit slightly into the adjacent part. Then the conventional cut with very little force runs perfectly true. Result is a small step caused by the path from an adjacent part. If this is the case, you will see the step in the center of the nest but not on the edges of the sheet where no adjacent part exists. It also can be deceptive because it only happens for new bits. Machine compensation for sharpened bits can mask the effect by effectively creating this part separation at the machine, but not in the software. You use Microvellum, I use AlphaCam, but the idea is the same. For a part .76 thick I climb to .73 then conventional to .765. Part separation of about 3 hundredths works well for me. Play around with these variables and see where you land. From contributor D: A good way to think of the forces involved and the effect on the material is to stop a tool at zero rpm and just turn it by hand. A climb cut motion enters the material on the side and slices downhill easily. It's natural to hold a stick in your hand and whittle it with a pocket knife using this same motion. Conventional cuts dig in hard and blow out more on side cuts. I work with solid wood, making doors. Grain direction affects our cuts on everything, as with small parts the tendency to throw them is much greater. It's the rule to go conventional across the grain, and climbing with it. Climb cutting a small rail with a big tenon cutter in end grain looks like a big paddle wheel hitting the end grain almost straight on, and guarantees the part will be thrown, even with the strongest suction available. Most people cutting MDF, melamine, and plywood don't have as much to worry about, in my opinion.
2010126 — Partially answering my own question, in case someone runs into a similar problem. ... where A1 was the angle used to define the chamfer angle and ...
Cotton String. Popular Brands: Thompson Enamel, Eurotool, grobet, Friedrich Dick, Fretz, 3M ferris, Cratex, Panther, Esca.
 18581906093