
Weiss Watch Company - wiess watches
Turningspeeds and feedscalculator
This research was funded by [National key R&D Program of China] grant number [2017YFB0305100, 2017YFB0305101] and [National Natural Science Foundation of China] grant number [51561018, 51871116].
The hardness and impact toughness of the steel sample obviously increased under the same quenching conditions. The grain size decreased after forging, and microstructure refinement improved the hardness and toughness of the metal [32]. After heat treatment, the pearlite of the forged state transformed into bainite, martensite, and retained austenite. The increase in the martensite content was beneficial for enhancing the hardness, and bainite and film-like retained austenite clearly improved the impact toughness [33]. The transformation induced plasticity (TRIP) effects resulted from the deformation during forging, and this contributed to the enhanced toughness because the austenite was rich in manganese and carbon [34]. Smaller prior austenite grains formed a finer martensite lath after heat treatment, whereas the longer martensite in the specimens also meant that there were larger grains before austenite transformed to bainite and martensite [35,36]. With an increase in deformation, the hardness of the forged billet slightly decreased before and after heat treatment. The work hardening effect was inherited by the subsequent microstructural transformation process due to thermal deformation. The material appeared to undergo dynamic recovery and flow softening because of the influence of the annihilation of dislocation when the strain was further increased to some extent [37,38]. With increased deformation at different values of H/D, the specimens were completely recrystallized, and this reduced the deformation energy storage and led to decreased hardness. However, the hardness of steel was improved compared to that of the as-cast steel because of deformation.
Tackle thick skin near nail folds and perform delicate callus removal. Effectively work on keratinized nails, rough skin, and calluses. Address nail fungus ...
Millingspeeds and feedsChart
Generally speaking, spindle speeds and feed rates are less critical in woodworking than metalworking. Most woodworking machines including power saws such as circular saws and band saws, jointers, Thickness planers rotate at a fixed RPM. In those machines, cutting speed is regulated through the feed rate. The required feed rate can be extremely variable depending on the power of the motor, the hardness of the wood or other material being machined, and the sharpness of the cutting tool.
Official websites use .gov A .gov website belongs to an official government organization in the United States.
Mechanical properties of the 0.4C-Si-Mn-Cr steel showing the development of (a) hardness and (b) impact toughness before and after heat treatment.
The spindle speed is the rotational frequency of the spindle of the machine, measured in revolutions per minute (RPM). The preferred speed is determined by working backward from the desired surface speed (sfm or m/min) and incorporating the diameter (of workpiece or cutter).
Most metalworking books have nomograms or tables of spindle speeds and feed rates for different cutters and workpiece materials; similar tables are also likely available from the manufacturer of the cutter used.
How to calculateFeed Rate for lathe
Compared with steel that was not subjected to heat treatment, the hardness and impact toughness of the steel samples after heat treatment showed obvious improvements. When the H/D value was 2.0, the maximum impact toughness was 87 J/cm2. Heat treatment had a significant contribution to improving the mechanical properties of the forged samples. Hardness decreased slightly with an increase in the H/D value. Furthermore, the impact toughness gradually increased, and this was related to the microstructure, dynamic recovery, and softening of the grains.
where Gt0 and Gt are the grain diameter (μm) at the times t0 and t, respectively. m is the average mobility of the grain boundary, and m depends on the index of Gt/Gt0. k = k0exp(−Q/RT), where Q is the activation energy of the grain boundary and T is the heating temperature.
As with meteorology and pharmacology, however, the interrelationship of theory and practice has been developing over decades as the theory part of the balance becomes more advanced thanks to information technology. For example, an effort called the Machine Tool Genome Project is working toward providing the computer modeling (simulation) needed to predict optimal speed-and-feed combinations for particular setups in any internet-connected shop with less local experimentation and testing.[15] Instead of the only option being the measuring and testing of the behavior of its own equipment, it will benefit from others' experience and simulation; in a sense, rather than 'reinventing a wheel', it will be able to 'make better use of existing wheels already developed by others in remote locations'.
Millingspeeds and feedscalculator
Dec 4, 2019 — depending on how thin the metal is and how well it is held in place. a end mill just might work on a drill press. more then likely you might get ...
Excessive spindle speed will cause premature tool wear, breakages, and can cause tool chatter, all of which can lead to potentially dangerous conditions. Using the correct spindle speed for the material and tools will greatly enhance tool life and the quality of the surface finish.
e.g. for a cutting speed of 100 ft/min (a plain HSS steel cutter on mild steel) and diameter of 10 inches (the cutter or the work piece)
Outside of the context of machine tooling, "speeds and feeds" can be used colloquially to refer to the technical details of a product or process.[3]
When calculating for copper alloys, the machine rating is arrived at by assuming the 100 rating of 600 SFM. For example, phosphorus bronze (grades A–D) has a machinability rating of 20. This means that phosphor bronze runs at 20% the speed of 600 SFM or 120 SFM. However, 165 SFM is generally accepted as the basic 100% rating for "grading steels".[12] Formula Cutting Speed (V)= [πDN]/1000 m/min Where D=Diameter of Workpiece in meter or millimeter N=Spindle Speed in rpm
In woodworking, the ideal feed rate is one that is slow enough not to bog down the motor, yet fast enough to avoid burning the material. Certain woods, such as black cherry and maple are more prone to burning than others. The right feed rate is usually obtained by "feel" if the material is hand fed, or by trial and error if a power feeder is used. In thicknessers (planers), the wood is usually fed automatically through rubber or corrugated steel rollers. Some of these machines allow varying the feed rate, usually by changing pulleys. A slower feed rate usually results in a finer surface as more cuts are made for any length of wood.
Aug 2, 2024 — Nuclear Facilities: Uranium Mines and Mills in Canada. Nuclear facility – Key Lake Operation. Cameco owns and is licensed to operate the Key ...
"Following World War II, many new alloys were developed. New standards were needed to increase [U.S.] American productivity. Metcut Research Associates, with technical support from the Air Force Materials Laboratory and the Army Science and Technology Laboratory, published the first Machining Data Handbook in 1966. The recommended speeds and feeds provided in this book were the result of extensive testing to determine optimum tool life under controlled conditions for every material of the day, operation and hardness."[4]
Grain size of 0.4C-Si-Mn-Cr steel with different H/D values for the deformation process. (a) As-cast, (b) H/D = 1.5, (c) H/D = 1.7, and (d) H/D = 2.0.
Spindle speed becomes important in the operation of routers, spindle moulders or shapers, and drills. Older and smaller routers often rotate at a fixed spindle speed, usually between 20,000 and 25,000 rpm. While these speeds are fine for small router bits, using larger bits, say more than 1-inch (25 mm) or 25 millimeters in diameter, can be dangerous and can lead to chatter. Larger routers now have variable speeds and larger bits require slower speed. Drilling wood generally uses higher spindle speeds than metal, and the speed is not as critical. However, larger diameter drill bits do require slower speeds to avoid burning.
The cutting speed is given as a set of constants that are available from the material manufacturer or supplier. The most common materials are available in reference books or charts, but will always be subject to adjustment depending on the cutting conditions. The following table gives the cutting speeds for a selection of common materials under one set of conditions. The conditions are a tool life of 1 hour, dry cutting (no coolant), and at medium feeds, so they may appear to be incorrect depending on circumstances. These cutting speeds may change if, for instance, adequate coolant is available or an improved grade of HSS is used (such as one that includes [cobalt]).
Secure .gov websites use HTTPS A lock ( Lock Locked padlock icon ) or https:// means you've safely connected to the .gov website. Share sensitive information only on official, secure websites.
How to calculatefeed rate for milling
The study was designed by Q.S., Z.L. and R.Z. The data was collected by F.Z., Y.Y. and J.B., and the literature was searched by Y.Y. and J.B. The figures and data analysis wereperformedby F.Z. and Z.L. The data interpretation was carried out by Q.S. The manuscript was written by F.Z. and Q.S. All authors have read and agreed to the published version of the manuscript.
Herein, to determine an appropriate forging temperature, Gleeble simulated compression deformation of medium carbon (0.4C-Si-Mn-Cr) steel under different temperatures. Samples with different height-diameter ratios (H/D) were forged and quenched. The microstructures of specimens were characterized using optical microstructure (OM) analysis, scanning electron microscopy (SEM), X-ray diffraction (XRD), and transmission electron microscopy (TEM). The hardness and impact toughness were investigated, and the microstructure evolution and mechanical properties of 0.4C-Si-Mn-Cr steel contributed towards providing a theoretical basis for the change rule of the deformation process.
Speeds and feeds have been studied scientifically since at least the 1890s. The work is typically done in engineering laboratories, with the funding coming from three basic roots: corporations, governments (including their militaries), and universities. All three types of institution have invested large amounts of money in the cause, often in collaborative partnerships. Examples of such work are highlighted below.
Herein, the effects of height-diameter ratios (H/D) on the microstructure evolution and mechanical properties of 0.4C-Si-Mn-Cr steel during high temperature deformation are reported. The compression experiments were performed on steel samples using Gleeble to obtain a reasonable deformation temperature, and the degree of deformation was assessed in the range of 1.5 to 2.0 H/D via forging. The forged specimens were quenched using the same heat treatment process. The hardness and impact toughness of the steel samples were tested before and after heat treatment. Grain sizes gradually increased with an increase in the compression temperature from 950 °C to 1150 °C, and the grain sizes decreased with an increase in H/D. The microstructure of the steel samples contained pearlite, bainite, martensite, and retained austenite phase. The microstructure after forging was more uniform and finer as compared to that of as-cast steel samples. The hardness and impact toughness of the steel samples were evaluated after forging; hardness first increased and then decreased with an increase in H/D, while the impact toughness continuously increased with an increase in H/D. Hence, the microstructure and properties of steel could be improved via high temperature deformation, and this was primarily related to grain refinement.
Machinability ratings can be used in conjunction with the Taylor tool life equation, VTn = C in order to determine cutting speeds or tool life. It is known that B1112 has a tool life of 60 minutes at a cutting speed of 100 sfpm. If a material has a machinability rating of 70%, it can be determined, with the above knowns, that in order to maintain the same tool life (60 minutes), the cutting speed must be 70 sfpm (assuming the same tooling is used).
The optical microstructure (OM) of 0.4C-Si-Mn-Cr steel before and after heat treatment with different H/D values is shown in Figure 4. The microstructure was primarily composed of pearlite and ferrite before the heat treatment, and the pearlite and ferrite were distributed among each grain. As shown in Figure 4a–d, the size of the pearlite in the forged samples was finer than that of the pearlite in the as-cast steel. The pearlite in the forged steel was mainly distributed on the shear bands, and the pearlite was deformed in the growth direction. Compared with forged steels, the as-cast specimen had a distinct grain orientation, which could be because a temperature gradient field was formed in the crystal body due to the quantitative loss of heat in the uncompressed state. This led to the formation of fibrous tissue parallel to the direction of heat dissipation. The microstructures of samples after heat treatment for different H/D values are shown in Figure 4e–h. The microstructure was mainly composed of acicular bainite, martensite, and retained austenite. Compared with Figure 4e, the bainite and martensite of specimens were finer and had a dispersed distribution, as shown in Figure 4f–h. According to the color metallographic techniques [19], with an increase in H/D, the bainite content increased gradually while the martensite content decreased.
Diamenter tolerance of the shafts. Shaft type, Diameter tolerance. W, h6. WV, h7. WRA, h6. WRB, h6. WH, h6. Straightness tolerance of the shafts. Shaft diameter ...
Figure 5 shows SEM images of steel before and after heat treatment. Figure 5a is an SEM image of the sample with an H/D value of 2.0 before heat treatment. Different pearlite clusters were distributed and grew along the grain boundary. The sizes of ferrite and cementite in all the grains were different and regularly arranged in a specific direction. The SEM microstructure of steel after heat treatment is shown in Figure 5b, and the microstructure was similar to that shown in Figure 4e–h. Figure 6 shows the XRD spectra for the steel samples before and after heat treatment, and the peaks observed before and after heat treatment corresponded to the body-centered cubic structure. These results showed that the sample had the face centered cubic structure after heat treatment. With the combined analysis of Figure 4 and Figure 5, it could be confirmed that before treatment, the body centered cubic structure of the steel was ferrite, while after treatment, there was a mixed structure of bainite and martensite. The face centered cubic structure was the retained austenite phase after quenching, and these results were consistent with the experimental results.
For a given machining operation, the cutting speed will remain constant for most situations; therefore the spindle speed will also remain constant. However, facing, forming, parting off, and recess operations on a lathe or screw machine involve the machining of a constantly changing diameter. Ideally, this means changing the spindle speed as the cut advances across the face of the workpiece, producing constant surface speed (CSS). Mechanical arrangements to effect CSS have existed for centuries, but they were never applied commonly to machine tool control. In the pre-CNC era, the ideal of CSS was ignored for most work. For unusual work that demanded it, special pains were taken to achieve it. The introduction of CNC-controlled lathes has provided a practical, everyday solution via automated CSS Machining Process Monitoring and Control. By means of the machine's software and variable speed electric motors, the lathe can increase the RPM of the spindle as the cutter gets closer to the center of the part.
There will be an optimum cutting speed for each material and set of machining conditions, and the spindle speed (RPM) can be calculated from this speed. Factors affecting the calculation of cutting speed are:

Some materials, such as machinable wax, can be cut at a wide variety of spindle speeds, while others, such as stainless steel require much more careful control as the cutting speed is critical, to avoid overheating both the cutter and workpiece. Stainless steel is one material that hardens very easily under cold working, therefore insufficient feed rate or incorrect spindle speed can lead to less than ideal cutting conditions as the work piece will quickly harden and resist the tool's cutting action. The liberal application of cutting fluid can improve these cutting conditions; however, the correct selection of speeds is the critical factor.
According to Equation (3), when time is constant, m is proportional to exp(−Q/RT); thus, the rate of grain growth is related to m. When the temperature is higher, the grain boundary migration and the growth rate were faster due to the increased atomic diffusion rate; also, the grain size increased exponentially with an increase in temperature. Temperature affects the plastic deformation of a material, which as a consequence, directly influences the microstructure evolution. The growth rate of grains at a low temperature was lower than that at a high temperature, which was because recovery and recrystallization were more pronounced at a high temperature.
TEM images of the morphology and SAED of steel with an H/D value of 2.0 in the deformation process. (a–b) Before heat treatment and (c–d) after heat treatment.
The spindle speeds may be calculated for all machining operations once the SFM or MPM is known. In most cases, we are dealing with a cylindrical object such as a milling cutter or a workpiece turning in a lathe so we need to determine the speed at the periphery of this round object. This speed at the periphery (of a point on the circumference, moving past a stationary point) will depend on the rotational speed (RPM) and diameter of the object.
Cutting speed may be defined as the rate at the workpiece surface, irrespective of the machining operation used. A cutting speed for mild steel of 100 ft/min is the same whether it is the speed of the cutter passing over the workpiece, such as in a turning operation, or the speed of the cutter moving past a workpiece, such as in a milling operation. The cutting conditions will affect the value of this surface speed for mild steel.
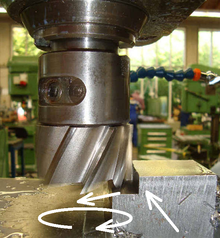
Feed rate is the velocity at which the cutter is fed, that is, advanced against the workpiece. It is expressed in units of distance per revolution for turning and boring (typically inches per revolution [ipr] or millimeters per revolution). It can be expressed thus for milling also, but it is often expressed in units of distance per time for milling (typically inches per minute [ipm] or millimeters per minute), with considerations of how many teeth (or flutes) the cutter has then determined what that means for each tooth.
One analogy would be a skateboard rider and a bicycle rider travelling side by side along the road. For a given surface speed (the speed of this pair along the road) the rotational speed (RPM) of their wheels (large for the skater and small for the bicycle rider) will be different. This rotational speed (RPM) is what we are calculating, given a fixed surface speed (speed along the road) and known values for their wheel sizes (cutter or workpiece).
Get pricing & availability information for part CL-4-RFK & browse all Carr Lane Locating Pins in the online catalog.
Stress–strain curves (a) and grain size data (b) of compressed 0.4C-Si-Mn-Cr steel under temperatures from 950 to 1150 °C.
The phrase speeds and feeds or feeds and speeds refers to two separate parameters in machine tool practice, cutting speed and feed rate. They are often considered as a pair because of their combined effect on the cutting process. Each, however, can also be considered and analyzed in its own right.
Schematic diagram of the experimental process. (a) High temperature compression deformation process at T = 950 °C, 1050 °C, and 1150 °C; (b) specimens under unidirectional compression in Gleeble; (c) stress and deformation of a cylinder during high temperature forging; (d) forging and pressing process of casting rod with height-diameter ratios (H/D) values of 1.5, 1.7, and 2.0; (e) heat treatment process of casting and forging.
A study on the effect of the variation of cutting parameters in the surface integrity in turning of an AISI 304 stainless steel revealed that the feed rate has the greatest impairing effect on the quality of the surface, and that besides the achievement of the desired roughness profile, it is necessary to analyze the effect of speed and feed on the creation of micropits and microdefects on the machined surface.[18] Moreover, they found that the conventional empirical relation that relates feed rate to roughness value does not fit adequately for low cutting speeds.
The exact RPM is not always needed, a close approximation will work. For instance, a machinist may want to take the value of π {\displaystyle {\pi }} to be 3 if performing calculations by hand.
The microstructure was pearlite, ferrite, bainite, martensite, and retained austenite with different H/D values. The microstructure was clearly more uniform and finer than that of the as-cast steel. The optimum deformation process was a heating temperature that was less than 1050 °C, and the H/D value was 2.0. Changes in grain size depended on the grain nucleation and dislocation movement during forging.
The diameter of the cross-section of the round bar decreased during forging. Under the action of external force, the round bar was deformed and expanded outward in the radial direction. The two end faces were elongated along the vertical axis (Figure 1c). The dislocation density of pearlite during the forging deformation process increased, and its value changed from 2.02 × 10¹⁴ m−2 to 6.07 × 10¹⁴ m−2; this provided nucleation sites for cementite and promoted diffusion of iron and carbon atoms. An increase in the H/D value accelerated the migration of atoms along the dislocation line, and this led to a decrease in the deformation resistance. When the strain was higher than the critical strain, the lattice was distorted because the number of slippages and twinning increased via atoms through dislocation. The initial grains began to break, and the slip resistance increased in this case. Dislocation density and deformation energy were formed in the ferrite, and this was beneficial for obtaining fine grains during DRX [25,26]. Furthermore, the temperature of the core slowly decreased because of the large volume of steel, providing sufficient time for grain recovery in the forging process. However, with a continuous decrease in temperature during the forging process, it was difficult to recrystallize deformed austenite because delayed nucleation inhibited DRX [27]. In addition, the high content of Si increased the hot deformation energy and reduced the rate of DRX, which made the steel deformation difficult, and the grain growth gradually stopped [28,29,30]. The microstructure of the undeformed billet was relatively stable under same heating conditions and still retained a large grain size. When the billet was air cooled to room temperature after forging, transformation of the ferrite and pearlite occurred during the cooling process [31]. Because of nucleation and grain growth during the transformation process, it was difficult to obtain quantitative information for DRX during deformation.
Stress–strain curves and the grain size of the compressed steels at various temperatures are shown in Figure 2. The shape of the flow curve was mainly unimodal. At different temperatures, with an increase in strain, the true stress first increased to a maximum value and then decreased to the steady-state region. When the temperature increased from 950 to 1150 °C, the maximum flow stress decreased from 219.93 to 117.23 MPa. This may be because of the increase in temperature and the activation energy of thermal deformation. Furthermore, the kinetic energy of atoms increased, and the critical shear stress slip line decreased. The behavior of strain softening was considered to be due to new dynamic recrystallization (DRX), and the asymptotic behavior was characteristic of dynamic recovery (DRV) [21,22]. The shape of the grains was a polygon or a block. With an increase in compression temperature, the grain size increased significantly. The maximum value grain size was obtained under a compression temperature of 1150 °C. When the compression temperature was more than 1050 °C, the microstructure appeared to be clearly the feature of an equiaxed crystal. DRX incompletely produced granular crystal grains at a low temperature. Moreover, the average grain size gradually increased from 6.2 to 17.8 μm with an increase in the compression temperature. The variation rule of the actual grain size was obtained via numerical fitting. The relationship between grain size and compression temperature is as follows:
Varalakshmi Sharp Tools - Offering 12mm Carbide Drill Bit, Carbide Drill Bit at Rs 1440/piece in Bengaluru, Karnataka. Get contact number of verified ...
The mechanical properties of steel with different H/D values are shown in Figure 8. As shown in Figure 8a, the hardness values (40–45 HRC) of the steel samples after heat treatment were larger than the hardness values (21–29 HRC) of the steel samples before heat treatment. As shown in Figure 8b, the impact toughness after heat treatment was greater than 12 J/cm2, which was higher than that of the steel samples before heat treatment (3–9 J/cm2). The hardness and the impact toughness were significantly enhanced after heat treatment. Before heat treatment, with an increase in the H/D value, hardness first increased and then decreased. However, the impact toughness of the samples before and after heat treatment increased linearly.
Grain refinement during deformation has a positive effect on the microstructure and properties of steel. G.P. Chaudhari et al. [11,12,13,14] found that the grain was clearly refined after multidirectional forging of steel, which induced fine austenite grains because of continuous dynamic recrystallization and dynamic recovery. The formation of fine grains is beneficial for enhancement of tensile strength and hardness. Crystal slips are the primary mode of deformation, and the mechanism of ferrite refinement is comprised grain segmentation and recovery. Sumit et al. [15] found that when the steel was forged in pure ferrite regions, the mechanical properties of steel had the best combination of yield strength and ductility. Hot compression deformation at different temperatures (950–1150 °C) and rates (0.01–10 s−1) can significantly promote grain refinement of as-cast samples [16]. Yang et al. [17] conducted hot deformation experiments of 35CrMoV steel with a degree of deformation that was about 50% at temperatures of 850 °C, 950 °C, and 1050 °C and concluded that grain size increased gradually with an increase in the deformation temperature under the same strain rate. Furthermore, the performance of the forging can be further enhanced via heat treatment. Smaropoulos [18] achieved excellent tensile strength, hardness, and toughness of a low alloy steel after forging followed by heat treatment. The as-obtained medium carbon steel had extraordinary mechanical properties, and this was achieved by alternating timed quenching in water and air [19,20]. However, the current research on microstructure evolution and mechanical properties of 0.4C-Si-Mn-Cr steel under different degrees of deformation is still limited, especially in the high temperature forging process. Therefore, understanding of microstructure evolution in steels and the associated mechanism is beneficial for further formulating and improving the deformation process.
How to calculatefeed rate for drilling
Microstructure evolution mechanism of medium carbon 0.4C-Si-Mn-Cr steel during the process of compression-forging-heat treatment.
The grain sizes were fine for the compression temperatures in the range of 950–1050 °C. Therefore, to obtain fine original austenite grains before heat treatment, the forging temperature was selected to be 1050 °C, which is in the range of 950–1050 °C. The sizes of grains with different H/D values are provided in Figure 3. The results showed that the shape of the samples was elliptical and band-like, and the grain size decreased with an increase in the H/D value. For cast steel, the grain size was about 26.4 μm, and the grains were shaped as irregular blocks. Furthermore, the distribution was relatively dispersed, and the grain roundness was not good enough. When the H/D value was from 1.5 to 2.0, the grains were mainly elliptical. After forging, the grain size decreased to 3.6 μm, and the distribution of grains was relatively uniform and dense. With forging, the variations in grain size with different H/D values were obtained via numerical fitting:
Cutting speed and feed rate come together with depth of cut to determine the material removal rate, which is the volume of workpiece material (metal, wood, plastic, etc.) that can be removed per time unit.
Feed rate formula for turning
Oct 30, 2005 — especially for 30lbs of metal. The big issue iw that you have not indicated what you are intrested in doing. The lathes might be fine for pens ...
Conventional milling, especially when roughing, can help save your tools a bit with cast iron. Because of the casting nature of this material, it will have ...
Owing to their excellent comprehensive performance, medium carbon steels have been widely used in essential fields such as energy development, machine manufacturing, and rail traffic [1,2,3,4]. In recent years, there has been an intense focus on the improvement of material properties through deformation technologies such as hot rolling, cold rolling, and forging [5,6,7,8]. Forging is a method for refining the grain size of steel via severe plastic deformation to enhance the strength and toughness. Internal cracks and defects of raw materials can be reduced during forging, and the microstructure and grain distribution are more uniform and compact after forging [9,10].
The ratio of the spindle speed and the feed rate controls how aggressive the cut is, and the nature of the swarf formed.
If variables such as cutter geometry and the rigidity of the machine tool and its tooling setup could be ideally maximized (and reduced to negligible constants), then only a lack of power (that is, kilowatts or horsepower) available to the spindle would prevent the use of the maximum possible speeds and feeds for any given workpiece material and cutter material. Of course, in reality those other variables are dynamic and not negligible, but there is still a correlation between power available and feeds and speeds employed. In practice, lack of rigidity is usually the limiting constraint.

Schematically, speed at the workpiece surface can be thought of as the tangential speed at the tool-cutter interface, that is, how fast the material moves past the cutting edge of the tool, although "which surface to focus on" is a topic with several valid answers. In drilling and milling, the outside diameter of the tool is the widely agreed surface. In turning and boring, the surface can be defined on either side of the depth of cut, that is, either the starting surface or the ending surface, with neither definition being "wrong" as long as the people involved understand the difference. An experienced machinist summed this up succinctly as "the diameter I am turning from" versus "the diameter I am turning to."[4] He uses the "from", not the "to", and explains why, while acknowledging that some others do not. The logic of focusing on the largest diameter involved (OD of drill or end mill, starting diameter of turned workpiece) is that this is where the highest tangential speed is, with the most heat generation, which is the main driver of tool wear.[4]
Feed per revolution Calculator
Dec 9, 2011 — If you look at a thread diagram, you'll see that the depth of thread (sharp crest to flat root), is given geometrically by: D ...
Speed-and-feed selection is analogous to other examples of applied science, such as meteorology or pharmacology, in that the theoretical modeling is necessary and useful but can never fully predict the reality of specific cases because of the massively multivariate environment. Just as weather forecasts or drug dosages can be modeled with fair accuracy, but never with complete certainty, machinists can predict with charts and formulas the approximate speed and feed values that will work best on a particular job, but cannot know the exact optimal values until running the job. In CNC machining, usually the programmer programs speeds and feedrates that are as maximally tuned as calculations and general guidelines can supply. The operator then fine-tunes the values while running the machine, based on sights, sounds, smells, temperatures, tolerance holding, and tool tip lifespan. Under proper management, the revised values are captured for future use, so that when a program is run again later, this work need not be duplicated.
With an increase in deformation temperature in the range of 950–1150 °C, the grain size of samples increased from 6.2 μm to 17.8 μm. The relationship between the grain size and temperature conformed to the fitting formula (Equation (1)). The steel had an abundance of blocky grains during the deformation process. Moreover, the grain size decreased from 26.4 μm to 3.6 μm with an increase in the H/D value. The relationship between the grain size and H/D was close to Equation (2).
Figure 9 presents a series of schematic diagrams of the microstructure evolution of steel during the process of compression-forging-heat treatment. When the temperature was greater than point A1, pearlite and ferrite dissolved and formed austenite grains. When the specimens began to yield, plastic strain and recrystallization driving force increased with an increase in compression temperature. The grain boundary migration rate accelerated, and this promoted rapid grain growth.
Cutting feeds and speeds, and the spindle speeds that are derived from them, are the ideal cutting conditions for a tool. If the conditions are less than ideal then adjustments are made to the spindle's speed, this adjustment is usually a reduction in RPM to the closest available speed, or one that is deemed (through knowledge and experience) to be correct.
In the 1890s through 1910s, Frederick Winslow Taylor performed turning experiments[16] that became famous (and seminal). He developed Taylor's Equation for Tool Life Expectancy.
When deciding what feed rate to use for a certain cutting operation, the calculation is fairly straightforward for single-point cutting tools, because all of the cutting work is done at one point (done by "one tooth", as it were). With a milling machine or jointer, where multi-tipped/multi-fluted cutting tools are involved, then the desired feed rate becomes dependent on the number of teeth on the cutter, as well as the desired amount of material per tooth to cut (expressed as chip load). The greater the number of cutting edges, the higher the feed rate permissible: for a cutting edge to work efficiently it must remove sufficient material to cut rather than rub; it also must do its fair share of work.
Optical microstructure (OM) of 0.4C-Si-Mn-Cr steel before and after heat treatment with different H/D values for the deformation process. (a–d) Before heat treatment and (e–h) after heat treatment. P: pearlite, F: ferrite, B: bainite, M: martensite, and RA: retained austenite.
The specimens were prepared at half the distance from the center of the instrument before and after heat treatment. The samples were then processed into unnotched impact specimens with dimensions of 10 × 10 × 55 mm. Hardness and impact tests were performed using a Rockwell tester (HR-150A, Dongshan, China) and semi-automatic tester (JB-300B, Dongshan, China). The specimens used a mixture of saturated picric acid, purified water, detergent, and hydrochloric acid to corrode the grains. The diameter of the grain in different fields was measured using the cut line method in the experiment, and then, the average value was counted as the grain size. The samples were corroded using 4% nitric acid alcohol solution and picric acid solution. XRD (MiniFlex 600, Rigaku, Japan) was performed on a diffractometer (Copper Kα radiation) at 10°/min for the counting time from 30° to 100°. Furthermore, for TEM, the specimens were prepared via electrolytic double spraying of 5% perchloric acid and 95% alcohol solution. The microstructure of the steel was observed using an optical microscope (Nikon ECLIPSE MA200, Japan), scanning electron microscope (ZEISS EVO18, Baden-Wurttemberg, Germany), and transmission electron microscope (FEI G220, Hillsboro, Oregon State, U.S.).
Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (http://creativecommons.org/licenses/by/4.0/).
Grinding wheels are designed to be run at a maximum safe speed, the spindle speed of the grinding machine may be variable but this should only be changed with due attention to the safe working speed of the wheel. As a wheel wears it will decrease in diameter, and its effective cutting speed will be reduced. Some grinders have the provision to increase the spindle speed, which corrects for this loss of cutting ability; however, increasing the speed beyond the wheels rating will destroy the wheel and create a serious hazard to life and limb.
This formula[14] can be used to figure out the feed rate that the cutter travels into or around the work. This would apply to cutters on a milling machine, drill press and a number of other machine tools. This is not to be used on the lathe for turning operations, as the feed rate on a lathe is given as feed per revolution.
Cutting speed (also called surface speed or simply speed) is the speed difference (relative velocity) between the cutting tool and the surface of the workpiece it is operating on. It is expressed in units of distance across the workpiece surface per unit of time, typically surface feet per minute (sfm) or meters per minute (m/min).[1] Feed rate (also often styled as a solid compound, feedrate, or called simply feed) is the relative velocity at which the cutter is advanced along the workpiece; its vector is perpendicular to the vector of cutting speed. Feed rate units depend on the motion of the tool and workpiece; when the workpiece rotates (e.g., in turning and boring), the units are almost always distance per spindle revolution (inches per revolution [in/rev or ipr] or millimeters per revolution [mm/rev]).[2] When the workpiece does not rotate (e.g., in milling), the units are typically distance per time (inches per minute [in/min or ipm] or millimeters per minute [mm/min]), although distance per revolution or per cutter tooth are also sometimes used.[2]
Figure 7 shows TEM images and the selected area electron diffraction (SAED) pattern of steel with an H/D value of 2.0. As shown in Figure 7a, after forging, the steel had a large number of dislocation lines and dislocation tangles between the ferrite and cementite. Furthermore, cementite (<100 nm) is observed in Figure 7b. The deformation ability of pearlite with ferrite and cementite was variable because of different stresses during high temperature forging. A dislocation in the ferrite formed because of the plastic deformation of the pearlite during forging. When there was a large amount of deformation, the layer size and grain size of pearlite were fine. The deformation resistance decreased via adjustments in the orientation of lamella during continuous impact compression. The cementite in the pearlite grain group gradually fractured, and the ferrite formed a high density of dislocations and a substructure that could reduce the strain energy [23]. TEM images of the morphology of the steel after heat treatment with an H/D value of 2.0 are shown in Figure 7c–d. After heat treatment, the steel obtained the multiphase microstructure that included dislocation-type lath martensite, bainite, and retained austenite and a number of dislocations gathered around the martensite. According to the inserted SAEDP in Figure 7d, the orientation relationships of the multiphase microstructure were (1¯10)α // (1¯11¯)γ. In addition, the retained austenite was mainly found to be film-like and blocks.
6351 West Trans Canada Hwy. Savona. British Columbia. Dealing in used equipment for the mining, pipe, mineral processing, soil remediation, aggregate, ...
The machinability rating of a material attempts to quantify the machinability of various materials. It is expressed as a percentage or a normalized value. The American Iron and Steel Institute (AISI) determined machinability ratings for a wide variety of materials by running turning tests at 180 surface feet per minute (sfpm). It then arbitrarily assigned 160 Brinell B1112 steel a machinability rating of 100%. The machinability rating is determined by measuring the weighed averages of the normal cutting speed, surface finish, and tool life for each material. Note that a material with a machinability rating less than 100% would be more difficult to machine than B1112 and material and a value more than 100% would be easier.
Scientific study by Holz and De Leeuw of the Cincinnati Milling Machine Company[17] did for milling cutters what F. W. Taylor had done for single-point cutters.
The chemical composition of the steel investigated in this work is listed in Table 1. The steel was smelted and poured into a cylindrical billet in an intermediate frequency furnace. A direct reading spectrometer was used to determine the chemical composition of the tested alloy. A schematic diagram of the experimental process is provided in Figure 1. The billet was processed into a round rod of size Φ8 × 12 mm. Specimens were heated to 50 °C below the predetermined temperature at a rate of 10 °C/s on a Gleeble-1500D dynamic thermal simulator (Data Sciences International INC, St. Paul, MI, USA), and then, the heating rate was reduced to 2 °C/s. The strain rate was 5 s−1, and deformation was 50%. Compression tests were conducted at temperatures of 950 °C, 1050 °C, and 1150 °C and maintained at the specified temperatures for 5 min followed by water quenching to cool the sample to room temperature (Figure 1a,b). The round bar was subjected to multidirectional force and then formed into a ball in a high temperature forging process (Figure 1c). Cylindrical billets with different H/D values (1.5, 1.7, and 2.0) were taken to 1050 °C for hot forging, and the billets were forged into a sphere of 150 mm (Figure 1d). The heat treatment was carried out by alternating the cycle cooling process in water and air (Figure 1e). After forging, samples were subjected to a quenching treatment under the same conditions. Moreover, all the samples were heated to 900 °C for 3 h, followed by alternating cycle cooling in water and air (after water cooling, the sample was cooled in air). Because the cooling rate of steel in water was higher than that in air, the temperature of samples could be reduced relatively uniformly to the isothermal region. As the quenching temperature decreased, the slope of the curve during water cooling was reduced gradually. The time of water cooling was 10 s, and that of air cooling was 15 s. The samples were treated at 330 °C for 3 h in a salt bath and further cooled to room temperature in air.



 18581906093