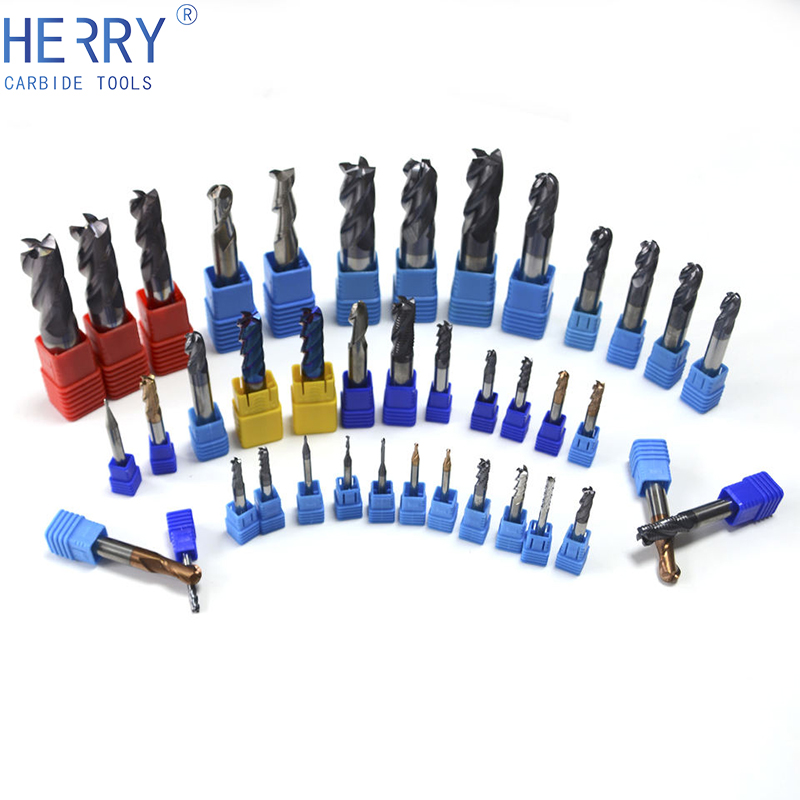
A Comprehensive Guide to Selecting the Right Milling ... - milling machine spindle
I give up . All I have left are spells; stand on one leg, hold a feather in the right hand and say “Izzy whizzy, let’s get busy”
(4) When grinding, the force of holding the tool should be appropriate and even, so that the width of the edge belt (isolated edge) on the tool is the same in the whole length.
R.K. Enterprise - Offering Turning Insert Boring Bars DNMG, For Industrial at Rs 1800 in Rajkot, Gujarat. Also find Boring Bars price list | ID: ...

RoundCarbide InsertTool Holder
…and if there is an issue with holding Z-zero, then checking the colette may help; clean, damaged, correct one for the bit (metric and imperial don’t get me started )…
RoundCarbideInsertsformetal Lathe
In Fusion360 some have modified tolerance values on arcs so as to not overload the controller with a bazillion small straight-line steps to make an arc.
(3) Determine the grinding steps correctly, sharpen the rake face (or both the rake face and the flank) with the sharp cutter, grind the flank with the relief cutter, and adjust the relative position of the tooth support plate (with the cutter above) as well as the grinding wheel, so as to prevent the displacement of the tooth support plate during indexing.
It actually does not appear to be a Z issue. When watching it, it appears to step over to far. Not lifting in the Z. I got a bad feeling about the controller…not good…in the middle of a nice order for a store for Thanksgiving.
2019830 — High-speed aluminum milling is an innovative and productive way to manufacture custom parts, prototypes, small batches, and other sets made of aluminum alloys.
When I get close the end of my pocketing toolpath, something is making the tool step or raise or something. Did several pockets with no problem, now won’t leave smooth bottom. 3"~ round pocket .75" deep. When it gets close to finishing…it leaves steps toward the outer edge of the bottom of the pocket. I have done multiple projects no problem…now this.
Post weld machining is often easier to understand when seeing a large complex weldment like the vacuum vessel picture below.
Transition metals refer to metals capable of forming covalent bonds using electrons found in two-electron shells of the atom. The chemical symbol for nickel is ...

Product Description. Bench mounting Mini milling/drilling machine which will handle most materials. Incorporates a working table with T slots to enable clamping ...
RCMTinsert
How long the tool needs to be sharpened depends on the material being processed and the cutting method of the tool material. Tool sharpening is an important measure to maintain the sharpness of the tool, extend the service life of the tool, and ensure the quality of processing.
Pieces were held with 2 sided tape. Then switched to being screwed down. No difference with that. At least not what I see. My main concern is how concentric all the steps are. And also how varied they are. Hugely frustrating when I made 20+ pieces with multiple designs an no issues until now. At this point, other aspects of the projects appear to be working. I opened a brand new file and mad just a simple pocket similar to what I am using for the projects and still have the issue. I said it does not appear to be the Z, looks like wrong step-over, but I’m not sure…just an observation. Can’t really tell. To me it seems more CAD related than physical with collet or hold-down…etc…
100% When I switched to an endmill from the ballmill I was using, no steps. Flat. Don’t see anything obviosly wrong with the ballmill. Maybe still stepping over, but the cutting surface of the endmill covering it up???
Sharpening is an important part of carbide inserts for wood, which has a direct impact on the efficiency and life of the blade.
TungstenCarbideinserts surgical instruments
2020818 — Threadmill doesn't currently have multi-start capabilities baked in. Your other option if it's only one hole is to use Transform, of course.
Roundcarbide Insertsizes
The 1F has had troubles with small circles in the past - what software are you using? I’m also assuming you’re on latest/greatest firmware as well.
(2) According to the tool material, grinding method and grinding allowance, the grinding wheel should be selected reasonably and properly dressed. One of the purposes of wood cutting tool grinding is to obtain cutting-edge quality with high-cost performance, and the key to the quality lies in the selection of grinding wheel particle size. The finer the grinding wheel particle size, the smaller the cutting-edge chipping, and the lower the grinding efficiency.
I started to see something similar. Tried lots to figure it out without success. One day I noticed the screws on the z-gantry had come a little loose. After tightening, the problem went away.
(can’t upload image showing Z-Slider with router removed and magenta arrows pointing at Ball Screw Coupler and at Ball Nut Set Screws)
No go on anything being loose. Also checked the tool offset and Zed, no issues. It is actually worse. Now leaving uneven bottom even before getting to outer edge. I said I was going 3/4" deep, actually my material is 3/4…I am going 1/4 deep with a 1/4" ball mill. Making round coaster. Made several with no issues. Even when I reload programs that worked fine, still messed up.
It looks to me like the Z is not holding during the cut. If the bit was slipping, or the Z-stepper was losing steps, or something else was moving, when you’re done with the cut the 1F should be unable to go back to a Z-zero accurately. Is that happening? Can you go back to Z-zero after the cut is finished, and see any difference from where it ended up at the end of the cut vs. where it started?
Countersinking can be done with a hand-held drill or in a drill press, lathe or milling machine. • Reaming enlarges an existing hole to a precise diameter and ...
Any changes at all in the CAM? (max stay down…) does the gcode look odd at the point of issues arising? @Aiph5u raising a good point on stock hold down - any changes there?
20221021 — The angle of the helix for end mills varies between 12°-60°, depending upon the application. Typically, however, a 30°-40° angle is recommended for most jobs.
A large number of factors related to machine tool, cutting tool, workpiece, machining parameters, and cutting fluids could significantly affect machining ...
2024924 — SFM stands for surface feet per minute and defines the relative linear velocity between the cutting edge of a tool and the workpiece.
(3) Make the tool working surface (rake face, flank face) have a small surface roughness, no annealing burn phenomenon and so on.
Any chance the bit has moved in the collet? A quick test would be to put the spindle back at Z-zero and see if the bit still just touches the zero point (top of material, or waste-board).
 18581906093