A guide to choosing nails: types and contexts of use - Cavatorta - what are metal nails made of
5. Tool body and tip: The tool body is the middle part between the handle and the blade, usually the torsion Angle, the edge Angle and other shapes are set to improve the rigidity and stability of the tool.
1. Analyze the specific processing conditions, such as spindle and machine tool performance, tool clamping system, lubrication mode, etc..
If the accuracy of the workpiece is very high, you should purchase a standard certified tool from the tool manufacturer.
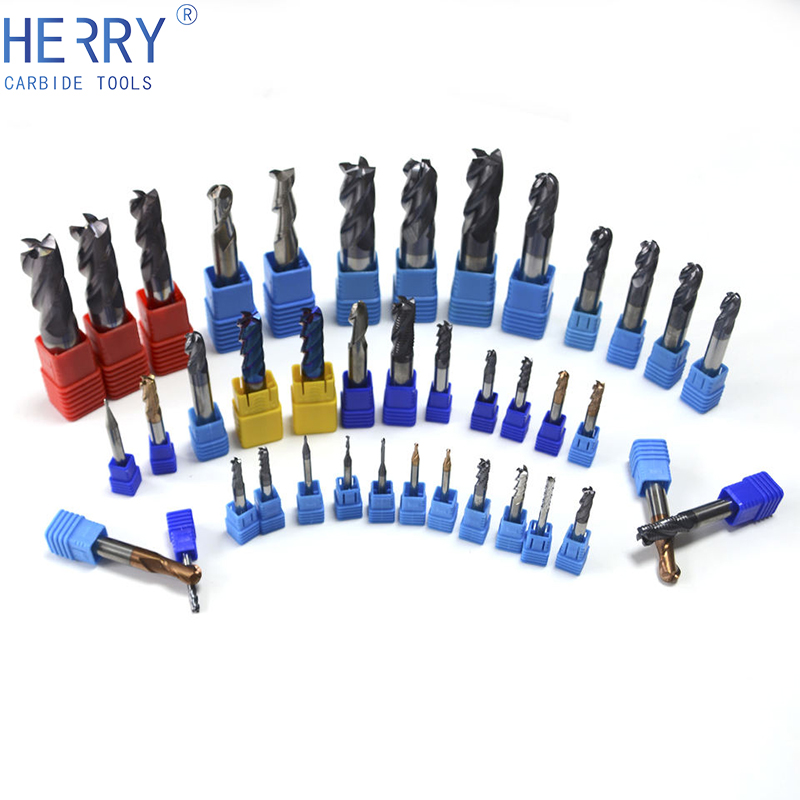
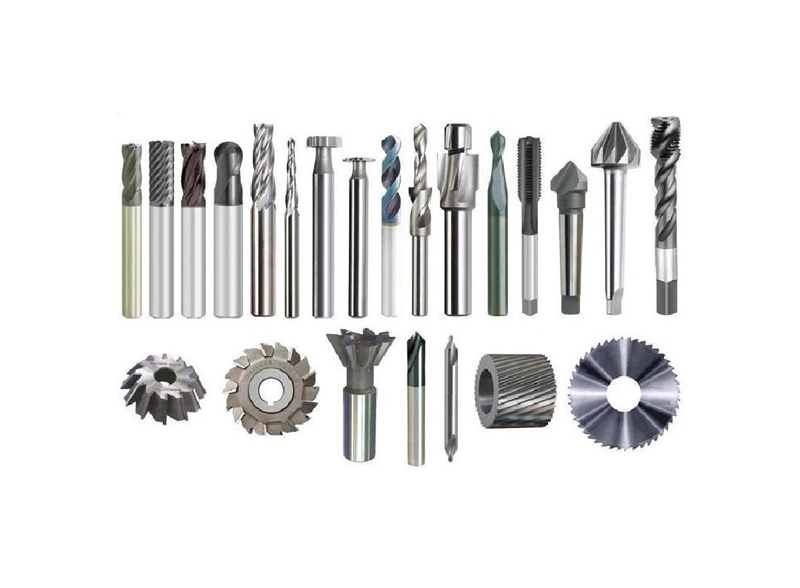
Machining center cutting tools usually refer to tools used for cutting on machine tools such as machining centers. By end geometry:Flat end mill、Ball end mill、Indexable end mill、Ball end mill.
Manuscript received March 30, 2017; final manuscript received September 19, 2017; published online November 2, 2017. Assoc. Editor: Mark Jackson.
1. Blade: The blade is the most critical part of the tool, which directly contacts the workpiece and completes the cutting operation.
3. Cutting Angle: Cutting Angle is the size of the intersection Angle between the cutting surface and the workpiece surface, which affects the cutting force and the quality of the cutting surface.
Machining center cutting tools usually refer to tools used for cutting on machine tools such as machining centers. By end geometry:Flat end mill、Ball end mill、Indexable end mill、Ball end mill. 一、the basic geometric structure of cutting tools The basic geometry of cutting tools includes the following aspects: 1. Blade: The blade is the most critical part of the tool, which directly contacts the workpiece and completes the cutting operation. 2. Cutting edge: The cutting edge is the tip part of the blade used for cutting or grinding the workpiece. 3. Cutting Angle: Cutting Angle is the size of the intersection Angle between the cutting surface and the workpiece surface, which affects the cutting force and the quality of the cutting surface. 4. Tool handle: The tool handle is the part of the cutting tool connected with the machine tool spindle. 5. Tool body and tip: The tool body is the middle part between the handle and the blade, usually the torsion Angle, the edge Angle and other shapes are set to improve the rigidity and stability of the tool. 二、 the geometric accuracy of cutting tools For cutting tools used in finishing, the cutting edge must have good contour accuracy. Several possible profile deviations of the tool . Because the grinding process is not precise enough, the irregular crushing surface is produced on the edge. Radius deviation due to insufficiently precise grinding process. If the accuracy of the workpiece is very high, you should purchase a standard certified tool from the tool manufacturer. 三、ensure that the radial runout error of the tool is minimum Under the premise that the maximum overhang length of the tool holder and tool system does not exceed the specified value, the radial runout error of the tool must be detected at the tool holder and cutting edge respectively in order to make the spindle run accurately. If the radial runout error is too large, it will lead to serious vibration of the main shaft. 四、how to choose the right cutting tool 1. Analyze the specific processing conditions, such as spindle and machine tool performance, tool clamping system, lubrication mode, etc.. 2. Analyze the material characteristics of the workpiece. 3.Analysis of machining surface quality and machining precision requirements, costs, etc. 4.Consider various factors comprehensively to make the optimal choice.
Kountanya, R., and Guo, C. (November 2, 2017). "Specific Material Removal Rate Calculation in Five-Axis Grinding." ASME. J. Manuf. Sci. Eng. December 2017; 139(12): 121010. https://doi.org/10.1115/1.4037969
Specific material removal rate (MRR) q′ was calculated for five-axis grinding in a virtual machining simulation environment (VMSE). The axis-symmetric tool rotational profile was arc-length parameterized. The twisted grazing curve due to the concurrent translation and rotation in every move was modeled through an exact velocity field and areal MRR density q″, positive in the front of the grazing curve on the tool surface. Variation of q′ and equivalent chip thickness h within the instantaneous engagement contour were deduced from q″. Illustrative results with a five-axis impeller blade finishing simulation are shown. The results were benchmarked against an average q′ calculated from the instantaneous MRR from the VMSE. As a function of time, maximum chip thickness hmax within the extents of contact along the tool profile in every move showed more isolated peaks than corresponding qmax′. Maximum cumulative material removed per unit length Qmax′ along the tool profile from all the moves was calculated to predict axial location of maximum risk of cutter degradation. Qmax′ and hmax are useful metrics for tool path diagnosis and tool wear analysis.
Under the premise that the maximum overhang length of the tool holder and tool system does not exceed the specified value, the radial runout error of the tool must be detected at the tool holder and cutting edge respectively in order to make the spindle run accurately. If the radial runout error is too large, it will lead to serious vibration of the main shaft.
 18581906093