What is CNC Milling? A Complete Guide - what do milling machines do
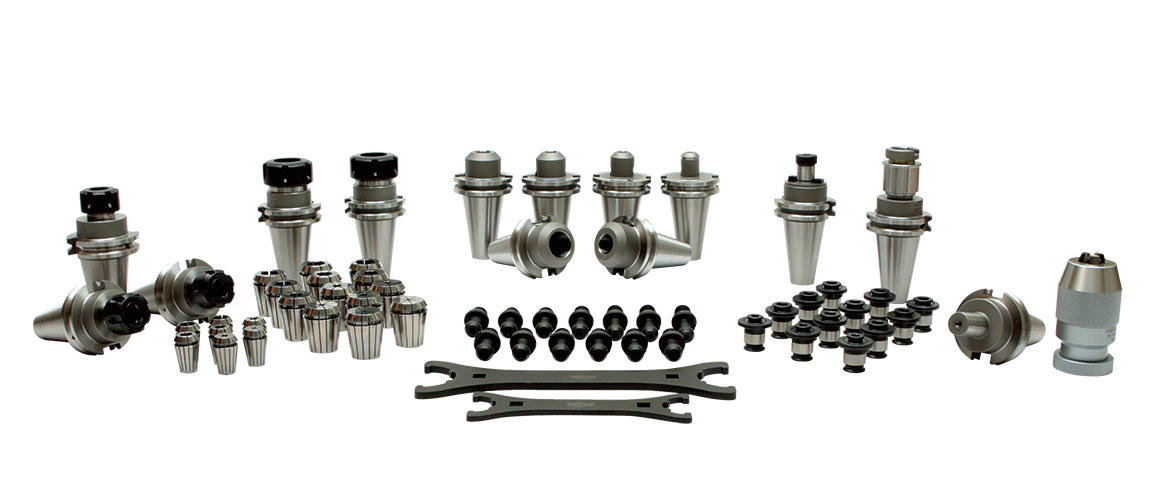
CAT tooling comes in a range of sizes designated as CAT 30, CAT 40, CAT 50, etc. The number refers to the Association for Manufacturing Technology’s (formerly the National Machine Tool Builders Association (NMTB)) taper size of the tool. CAT tool holders were developed for the Caterpillar tractor company and are sometimes called V-Flange Tools. They are of a robust design used primarily for a range of applications from precision machining to heavy duty roughing. This type of CNC tool holder is supported by ATC (automated tool change) technology. The tool holder body is pulled into the milling spindle with the aid of a retention knob and centered via the taper contact. Spindle speeds up to 12,000 rpm are standard with steep-taper tools. CAT tool holders will accept both imperial and metric-sized tools.
Hydraulic chucks are used for milling, drilling, reaming, and boring. Hydraulic chucks can be run up to 50,000 rpm and are concentric to .00012". There are a wide range of coolant sealed or coolant flush reduction sleeves available. Our Hydraulic Chucks are balanced to G2.5 @ 25,000 rpm.
HSK tool holders offer a few advantages over CAT tool holders, especially in high-speed milling machine spindles, tool collisions and maintenance. HSK tool holders are lighter in mass which allows machines to accelerate and decelerate quicker than CAT tool holders. At spindle speeds higher than 8,000 rpm, the spindle receiver expands faster than the shank. Because HSK tool holders have a hollow design, its shank acts like a fuse and during a crash, will break off protecting the shank of the machine.
Shrink Fit Holders require a shrink fit machine which expandsthe bore when heated to accept a cutting tool. Once cooled the toolis held securely over the entire length of the shank resulting insuperior gripping force with minimal runout.
HSK tool holders are a relatively new design and common on European machines imported into the United States. HSK is a German acronym for “hollow taper shank”. They do not have the retention knob of the CAT tool holders but instead have a hollow shank. The clamping mechanism in a HSK tool holder is operated from the inside, incorporating segmented collets that expand radially under pressure. The collet’s chamfer matches that of the inner wall of the shank allowing it to lock securely when the drawbar is actuated. Twice as much clamping force is generated on the flange in a HSK tool than that of the CAT type. The increased clamping force generated is due to the simultaneous taper and flange spindle connection. This creates radial stiffness up to five times that of steep-taper tool holders. HSK tool holders are balanced for high-speed machining and have a lower tolerance between the spindle receiver and the taper body than CAT tools.
A collet chuck is a type of chuck that forms a collar around a tool and applies a high static friction force, holding the object firmly and in accurate alignment. The "ER" collet system, developed and patented by Rego-Fix in 1973 is the most widely used collet system in the world today. The ER line consist of ER-8, ER-11, ER-16, ER-20, ER-25, ER-32, ER-40, and ER-50. The numbers in the series are the inner diameter of the collet. RedLine Tools offers a full line of ER collet chuck holders that are balanced to G2.5 @ 18,000 rpm.
CNC machine tool calibration is the process of measuring, diagnosing and operating within the manufacturing tolerance. Over time your machine will drift out of calibration. Calibrating your machine will:

 18581906093