a randomised controlled trial in India, Sri Lanka, and ... - low helix
Mildsteel cutting speedCarbide
U-slots (Fig. 1) are generally preferred if slots are accessible for easy cleaning. If cut carefully, these slots are effective until commutator has worn down full depth of undercut. Slot should be cut 1/32”-3/64” (.031-.046) deep, or to OEM specifications. If slot cut too deep, accumulated dust will not be thrown out by the centrifugal action of the rotating commutator.
When undercutting with compound land saws, bottom of slot will appear flat. However, as a result of reverse taper on alternate teeth, slot bottom will have slight pyramid or convex profile.
Cutting speed for steelwith carbide
Circular cutter must be accurately centered on mica (see Fig. 4). When cutter is not accurately centered, wedge-shaped mica fins in V-slots are more difficult to remove than fins with uniform thickness left after U-slot.
Cutting speed foraluminum
Undercutting may leave a bur (see Fig. 2). Edge of bar might become work hardened, leading to nonuniform wear and possible damage to brushes. Edges of bars must be chamfered to remove bur and work hardened area through use of suitable slotting file or specialty scraper. A chamfer of 1/64” (.4mm) is usually adequate. See Hand Tools section of catalog for slotting files and chamfering tools.
Cutting tool surface coatings are available upon request. Tool coatingsprovide tool wear resistance while significantly improving theperformance of saws in most applications, particularly when cuttingferrous materials. These coatings are extremely thin, harder than steeland greatly reduce friction and wear. The most common coatingsavailable for Martindale/Gaylee Saws are:
Commutator surface should then be lightly polished with fine-grain commutator stone or rubber bond cleaning stone to properly finish commutator surface.
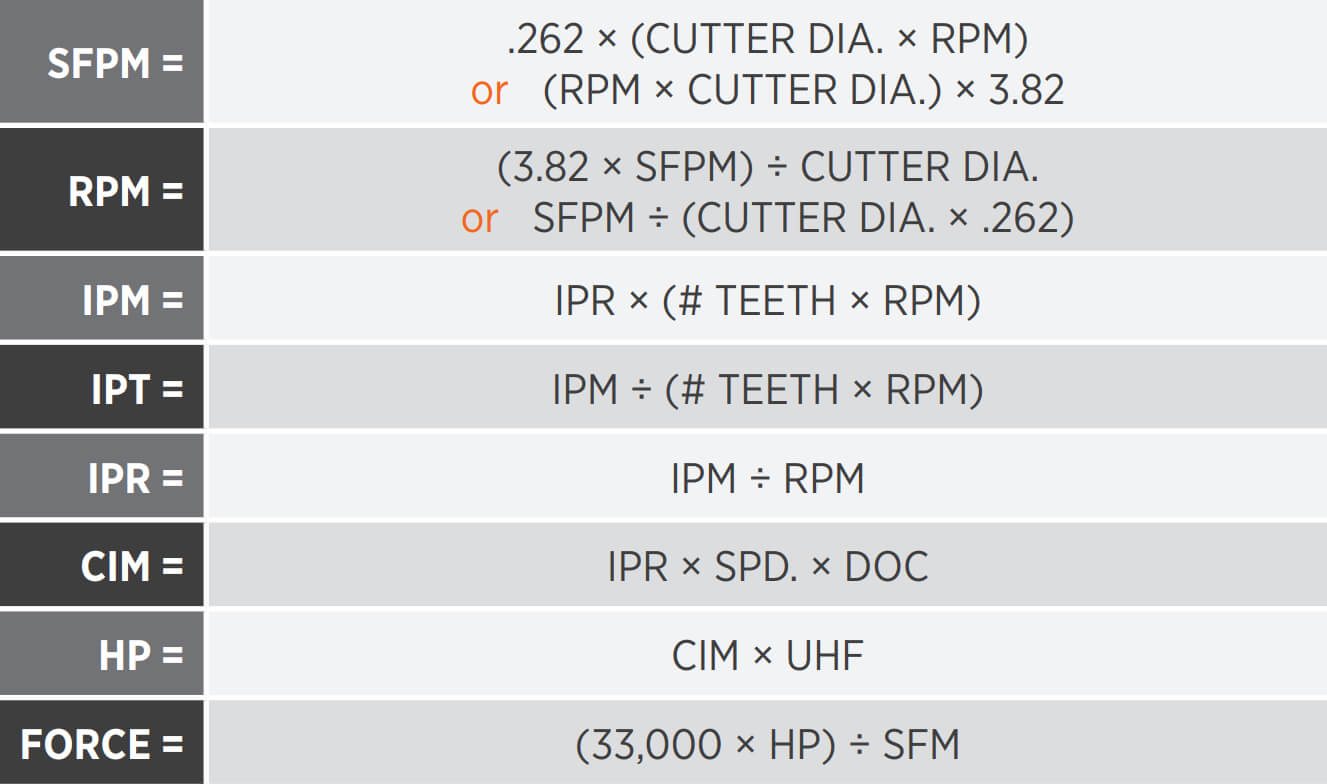
Cutting speedformula
Cutting speed formildsteel
These are general cutting speed recommendations, and may vary from application to application. Martindale/Gaylee does not assume any liability in the following recommendations, which are basically suggestions on where to start. Please contact us if you have questions.
“Angle of thread.” Merriam-Webster.com Dictionary, Merriam-Webster, https://www.merriam-webster.com/dictionary/angle%20of%20thread. Accessed 7 Nov. 2024.
Millspeed for steel
After undercutting, commutator must be carefully inspected to assure all copper particles removed, all bars chamfered, and all sharp edges and burs eliminated. Slots should be individually checked and reworked to remove any traces of fin or side mica.
You must — there are over 200,000 words in our free online dictionary, but you are looking for one that’s only in the Merriam-Webster Unabridged Dictionary.
V-slots keep slots free from dust accumulations at low speeds, and do not require a separate operation for chamfering of bar edges. V-slots are usually made with either a slotting file, or a “V” tooth circular cutter. Usual practice is to use a circular cutter having an included angle between cutting edges such that a cut made 1/16” (1.6mm) deep will also leave 1/32” (.8mm) free copper above the mica. Standard V-cutters are available with 40°, 50°, or 60° angles between cutting edges.
Choose cutter width to slightly exceed mica thickness (recommend +.003” / .08mm). This allows saw to remove full width of mica plus .0015” (.04mm) copper on each side of slot. If unable to determine mica width, a feeler gage may help determine required saw thickness.
Teeth on compound land mica saws are alternately ground to a special taper which reduces impact on each individual tooth and produces chips just slightly over half of slot width. This eliminates chips’ tendency to clog slot. Saw will operate cooler and clear chips better, prolonging saw life.
Variations to number of teeth, rake angle, clearance angle, bevel, side clearance, material, land, etc. may improve performance and tool life.
Once commutator has been resurfaced, mica insulation separating copper segments must be undercut. Undercutting is most easily accomplished with armature removed from machine. However, various tools are available to undercut commutator “in place”.
 18581906093