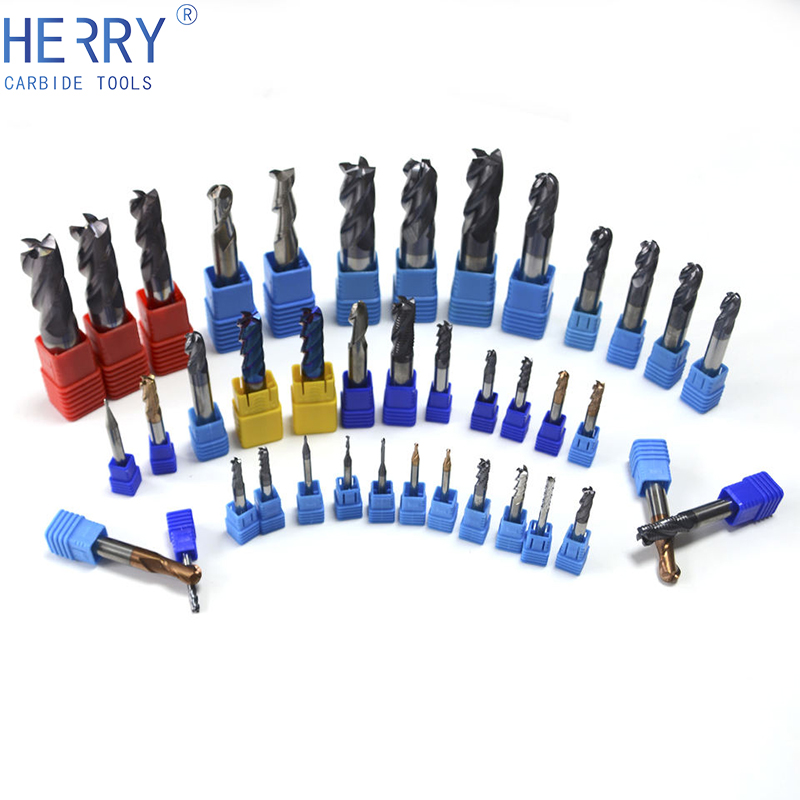
A4SS Integral Small Diameter Face Grooving - face grooving insert
Let’s talk about milling stability, force, and displacement. The middle plot displays a stability map that separates unstable (chatter) pairs of spindle speed and axial depth from stable pairs. The feed direction force and tool displacement are shown for three example pairs. The radial depth of cut is 5 mm (20 mm diameter, four tooth endmill) and the axial depth of cut is 5 mm for all three down milling cases. The red box displays results for 6000 rpm. We see the unstable spindle speed-axial depth pair gives large forces and displacements. We also see that the behavior does not repeat from tooth to tooth (these are the red dots). The blue box shows the unstable result for 9000 rpm. We observe similar behavior to 6000 rpm. The outcome is poor surface finish, premature tool failure, and potential catastrophic damage to the workpiece, tool, and spindle. The green box displays stable milling at 7500 rpm. The behavior now repeats with each tooth and the desired surface finish is obtained. This selection of stable machining parameters is possible when we know the vibration behavior of our cutting tool in its holder and spindle/machine. To learn more about milling dynamics, register for our ACE online, no-cost CNC machining course. For measurement after milling, register for our metrology course. https://lnkd.in/ejFqkhtH
End milldepthof cut chart
Richard Rosenberg Distinguished Professor, University of Tennessee, Knoxville | Joint Faculty, Oak Ridge National Laboratory | Director, SEAMTN | Director, Machine Tool Research Center
End milldepthof cut rule of thumb
Let’s talk about milling stability. The top left figure depicts a down milling operation where the radial depth of cut linearly increases as the 20 mm diameter, 4 tooth endmill feeds horizontally to the right. The bottom left figure provides the stability limit for three radial depths: 1 mm (red), 10 mm (blue) and 20 mm (green). The latter represents slotting. Axial depth-spindle speed pairs above the limit are unstable; those below are stable. The selected spindle speed is 7000 rpm and the axial depth is 5 mm (black circle). The top right figure displays the tool vibration in the feed direction as the radial depth increases. The cut is initially stable (red box), but chatter occurs at the end (green box). The bottom right figure shows the frequency content for the stable (red) and chatter (green) conditions. For stable cutting at radial depths from 0 to 6 mm, we see the tooth passing frequency (7000*4/60 = 467 Hz). For chatter at radial depths above 14 mm, we see both the tooth passing frequency and the chatter frequency (520 Hz, near the natural frequency of 500 Hz). If you'd like to learn more about the chatter in milling, register for our ACE online, no-cost CNC machining course. Register for the metrology course to learn more about measurement and uncertainty. https://lnkd.in/ejFqkhtH
Let’s talk about milling stability. The top left figure depicts a down milling operation where the radial depth of cut linearly increases as the 20 mm diameter, 4 tooth endmill feeds horizontally to the right. The bottom left figure provides the stability limit for three radial depths: 1 mm (red), 10 mm (blue) and 20 mm (green). The latter represents slotting. Axial depth-spindle speed pairs above the limit are unstable; those below are stable. The selected spindle speed is 7000 rpm and the axial depth is 5 mm (black circle). The top right figure displays the tool vibration in the feed direction as the radial depth increases. The cut is initially stable (red box), but chatter occurs at the end (green box). The bottom right figure shows the frequency content for the stable (red) and chatter (green) conditions. For stable cutting at radial depths from 0 to 6 mm, we see the tooth passing frequency (7000*4/60 = 467 Hz). For chatter at radial depths above 14 mm, we see both the tooth passing frequency and the chatter frequency (520 Hz, near the natural frequency of 500 Hz). If you'd like to learn more about milling stability, register for our online, no-cost ACE CNC machining course. To learn more about part measurement, register for our metrology course. https://lnkd.in/dWnixj6c
#snsinstitutions #snsdesignthinking #designthinkers Milling is the process of machining using rotary cutters to remove material[1] by advancing a cutter into a workpiece. This may be done by varying directions[2] on one or several axes, cutter head speed, and pressure.[3] Milling covers a wide variety of different operations and machines, on scales from small individual parts to large, heavy-duty gang milling operations. It is one of the most commonly used processes for machining custom parts to precise tolerances. Milling can be done with a wide range of machine tools. The original class of machine tools for milling was the milling machine (often called a mill). After the advent of computer numerical control (CNC) in the 1960s, milling machines evolved into machining centers: milling machines augmented by automatic tool changers, tool magazines or carousels, CNC capability, coolant systems, and enclosures. Milling centers are generally classified as vertical machining centers (VMCs) or horizontal machining centers (HMCs). The integration of milling into turning environments, and vice versa, began with live tooling for lathes and the occasional use of mills for turning operations. This led to a new class of machine tools, multitasking machines (MTMs), which are purpose-built to facilitate milling and turning within the same work envelope.
What isdepthof cut
Let’s talk about chatter in milling. The top panel displays a stability map that separates stable combinations of spindle speed and axial depth of cut (below the blue boundary) from unstable combinations (chatter above the boundary). Two sets of milling parameters are identified in the top panel. The red dot at {13000 rpm, 5 mm} represents a combination that exhibits chatter. The green dot at {16000 rpm, 5 mm} represents a stable combination. The bottom panel displays the tool vibration in the feed (x) direction for the two parameter sets. The red line is for the unstable {13000 rpm, 5 mm} pair and the green line is for the stable {16000 rpm, 5 mm} pair. The red and green dots follow the vibration as the cuts proceed. We see that the (red) unstable cut does not repeat; this gives the poor surface finish with chatter. The (green) stable cut repeats and gives the desired uniform surface finish. To generate the top panel and select stable milling parameters at the CAM stage, we: 1) measure the tool-holder-spindle dynamics; 2) select the force model based on the workpiece materials; and 3) compute the stability map. To learn more, register for our ACE online, no-cost CNC machining course. After we machine, we measure. To learn more about measurement, register for our metrology course. https://lnkd.in/dWnixj6c
© 2003 - 2024 Blain Supply, Inc. Prices were current at the time of posting. We reserve the right to change prices without notice and to correct errors.
Richard Rosenberg Distinguished Professor, University of Tennessee, Knoxville | Joint Faculty, Oak Ridge National Laboratory | Director, SEAMTN | Director, Machine Tool Research Center
What is Micro Milling? Everything you need to know Micro Milling involves using advanced CNC machines, meticulously calibrated tools, and cutting-edge technology to create intricate components with unparalleled precision. Maintaining your interest in this topic, I assure you that micromilling differs from your run-of-the-mill machining technique. It’s a revolutionary method that caters to the demands of industries like electronics, aerospace, and automotive, where precision is non-negotiable. The excitement doesn’t stop here; we’re about to explore the very fabric of Micro Milling, from the technology powering it to its diverse applications. What is Micro Milling? Micromilling is a highly advanced machining technique that takes precision to a new level. Unlike traditional milling methods, Micro Milling involves using cutting-edge CNC machines and meticulously calibrated tools to create intricate components with unparalleled accuracy. The process allows for producing miniature and highly detailed parts, making it a go-to solution for industries that demand precision, such as electronics, aerospace, and automotive. The key to micro-milling lies in using state-of-the-art CNC machines with high-speed spindles and advanced control systems. These machines operate with exceptional accuracy, enabling the creation of complex geometries and tight tolerances. The precision achieved in Micro Milling is unmatched, making it an ideal choice for projects where even the slightest deviation can impact
Let’s talk about modal analysis. We use this approach to model machining dynamics. We begin by measuring the frequency response function, or FRF, for a cutting tool-holder-spindle-machine. You can think of the FRF like a fingerprint; it’s unique for each combination. We measure the FRF by impact (or tap) testing, where we tap the tool with an instrumented hammer to apply a force (f) and record the response (x) using a low mass accelerometer. In the top panel of the figure, the real and imaginary parts of an example FRF are shown. In modal analysis, we fit each of the two vibration modes for the FRF separately and identify a single degree of freedom, SDOF (i.e., one mass, one spring, one damper), model for each. These uncoupled models are defined in modal coordinates, q, instead of physical (or local) coordinates, x. See the lower right picture. The SDOF modal coordinate models of the structural dynamics can then be incorporated in our machining process model to predict machining performance. This is more convenient that the coupled 2DOF model described in local coordinates (lower left picture). If you'd like to learn more about the relationship between vibrations and milling parameter selection, register for our ACE online, no-cost CNC machining course. Register for the metrology course to learn more about manufacturing measurements. https://lnkd.in/dWnixj6c
Radialdepthof cut
Let’s talk about chatter in milling. The top left photo shows an experimental setup we used to measure signals during milling. The steel workpiece was mounted on a flexure. This simulates a flexible workpiece, such as a turbine blade. The flexure displacement and velocity were measured using a laser Doppler vibrometer (LDV). The top right panel shows a stability map. It separates the stable and unstable/chatter zones based on spindle speed (horizontal axis) and axial depth of cut (vertical axis). The bottom left panel shows a Poincaré map that plots the flexure displacement (horizontal axis) versus its velocity (vertical axis) in the x (feed) direction. The dots show samples collected at each tool revolution. These dots were identified by sampling the displacement and velocity signals once per tool revolution using a laser tachometer (LT in the photo). Because the samples repeat, the cut is stable. An unstable result is shown in the bottom right. Here, the samples do not repeat with each tool revolution. This is chatter and produces the poor surface finish we observe. We obtain the elliptical shape because a new frequency was introduced into the dynamic system: the chatter frequency. This is the sound we hear. If you'd like to learn more about machining dynamics, register for our online, no-cost ACE CNC machining course. https://lnkd.in/dWnixj6c
Milling is a type of machining process that uses a rotating cutter to remove material in a controlled manner from a workpiece. This subtractive manufacturing technique aims to turn the workpiece into the required shape. A modern milling machine is often paired with Computer Numerical Control (CNC) for automated control over the whole process The main working part of a milling machine is the rotary cutting tool. This cutting tool is responsible for the material removal process. Milling machines can utilize both single-point and multi-point cutting tools The cutting tool in milling moves perpendicular to the rotational axis. For instance, if the cutting is rotating in the X-Y plane around the Z-axis, the movement of the cutter also occurs in the X-Y plane. The workpiece meets the cutter at the rotating tangent, resulting in the material removal process. #millingmachine #cncmilling #manfacturing
Axial depthdental
Richard Rosenberg Distinguished Professor, University of Tennessee, Knoxville | Joint Faculty, Oak Ridge National Laboratory | Director, SEAMTN | Director, Machine Tool Research Center
Axial depthof cut formula
Richard Rosenberg Distinguished Professor, University of Tennessee, Knoxville | Joint Faculty, Oak Ridge National Laboratory | Director, SEAMTN | Director, Machine Tool Research Center
#snsinstitutions #snsdesignthinkers #designthinkers Milling Machine: A Versatile Machining Tool A milling machine is an industrial machine tool that removes material from a workpiece using a rotating cutting tool. It's a cornerstone in manufacturing, capable of creating a wide range of shapes and features. How it Works * Rotary Cutting Tool: The heart of the machine, a milling cutter with multiple cutting edges, rotates at high speed. * Workpiece Movement: The workpiece is moved relative to the cutter, allowing the cutting edges to remove material. * Chip Formation: As the cutter interacts with the workpiece, it creates chips (swarf) that are carried away by coolant. Types of Milling Machines * Horizontal Milling Machine: The spindle is oriented horizontally. * Vertical Milling Machine: The spindle is oriented vertically. * CNC Milling Machine: Computer Numerical Control provides
Richard Rosenberg Distinguished Professor, University of Tennessee, Knoxville | Joint Faculty, Oak Ridge National Laboratory | Director, SEAMTN | Director, Machine Tool Research Center
Richard Rosenberg Distinguished Professor, University of Tennessee, Knoxville | Joint Faculty, Oak Ridge National Laboratory | Director, SEAMTN | Director, Machine Tool Research Center
 18581906093