About nickel - nickel chemical properties
These elements are some of the rarest materials on earth, and can therefore be enormously expensive. Gold and silver can be found in pure nugget form, making them more easily available. However, the other six elements are typically found mixed in the raw ore of the four metals they sit below on the periodic table: Iron (Fe), Cobalt (Co), Nickel (Ni), and Copper (Cu). These elements are a subset of precious metals and are generally called Platinum Group Metals (PGM). Because they are found together in raw ore, this makes mining and extraction difficult, dramatically increasing their cost. Because of their high price tag, machining these materials right the first time is incredibly important to a shop’s efficiency.
Example 2B: Calculate the speed and feed for a 1/2″ diameter, 3 flute carbide endmill if peripheral and plunge cutting in aluminum using a CNC milling machine in lab.
TIP: Plunging should generally be performed at 75% of the speed and 25% of the feedrate of the calculated peripheral cutting parameters.
Precious metals can be particularly difficult to machine due to their wide range of material properties and high cost if a part has to be scrapped. The following article will introduce these elements and their alloys as well as provide a guide on how to machine them effectively and efficiently.
Preciousmetal list
The table below contains a recommended surface speeds for common materials when using DML equipment. These values are conservative because our primary goal is fostering a safe learning environment (for our users and our tools!), not trying to squeeze every second out of each operation.
Every metal cutting operation requires selection of proper cutting parameters for success. As a DML TA, you need to understand basic calculations that will allow the tools you use to work as intended.
Precious metalslist in order
This article had some good info but it lacked any data relative to Sterling Silver and 10k-14k gold. I would find it really helpful if you were able to identify cutters withan 1/8″ shank that would do really well with Sterling silver and 14l gold.
TIP: IF this was being performed on a CNC lathe, typical parting feed rates vary between 0.001 in/rev (for steels) and 0.005 in/rev (for plastics). But remember, do NOT use the power feed when parting on a manual lathe unless you own the machine!
TIP1: Recommended peck depth when drilling less than 3xD (e.g. 3 drill diameters) with flooded coolant is one drill diameter, or when applying oil manually, or under low pressure, is 50% of drill diameter.
Where do the noblemetalstend to be located on thetable
As a member of Harvey Performance Company’s New Product Development team, Robert strategized new products to introduce with each new catalog released by Harvey Performance Company’s collection of brands.
Example 3: Calculate the speed and feed for a HSS countersink used to countersink a #10 clearance hole in aluminum using a manual milling machine.
TIP2: When drilling deeper holes (> 3xD) without high pressure TSC (thru spindle coolant), reduce spindle speed an additional 50%.
Note that these speed and feed values are guidelines assuming adequate (flooded) lubrication, workpiece stiffness and drill depth less than 3 drill diameters (0.75″). When applying oil manually (as in the lab), scale the feed and speed back to 60%, so N = 900 rpm and f = 3.6 in/min (final answer).
I didn’t know that different metals have different material properties. I need someone who can machine some steel pipes for me. I’ll have to consider getting a contractor who can weld everything for me.
Note that these speed and feed values are guidelines assuming adequate (flooded) lubrication and workpiece stiffness. When applying oil manually (as in the lab), scale the feed and speed back to 60%, so N = 330 rpm and f = 2.0 in/min (final answer).
Precious Metals
First, lookup the recommended surface speed in Table 1 (V ≈ 100 ft/min) and calculate the spindle speed from Equation 2:
Precious metals have notable material properties as they are characteristically soft, ductile, and oxidation resistant. They are called “noble” metals because of their resistance to most types of chemical and environmental attack. Table 1 lists a few telling material properties of precious metals in their elemental form. For comparison purposes, they are side-by-side with 6061 Al and 4140 Steel. Generally, only gold and silver are used in their purest form as the platinum group metals are alloys that consist mainly of platinum (with a smaller composition of Ru, Rh, Pa, Os, Ir). Precious metals are notable for being extremely dense and having a high melting point, which make them suitable for a variety of applications.
Note: when applying oil manually, scale the feed and speed back to 60%, so N ≈ 420 rpm and f ≈ 4.8 in/min (final answer). This is close enough to 500 rpm that I would first try this tool at the low end of high range with good oil application and see how it goes.
Platinum and its alloys are biocompatible, giving them the ability to be placed in the human body for long periods of time without causing adverse reactions or poisoning. Therefore, medical devices including heart muscle screw fixations, stents, and marker bands for angioplasty devices are made from platinum and its alloys. Gold and palladium are also commonly used in dental applications.
Please send an email to [email protected] with all your information and application information and they will be able to help you.
I have a tool with a diameter of 0.5mm (0.020in): 0.020×1/8×0.100×2-1/2 from Accupro. My CNC machine is a Haas OM-2. I have problems with processing platinum because the cutter breaks after an hour of work. The cutter performs work in an arc with an angle of 7.4 degrees to a depth of 1.6mm. The primary arc window is 0.4mm wide. the cutter is supposed to widen it to 0.5 so it collects only 0.05mm on the side. what feed rate and spindle speed to choose? I used spindle speed S2500 and feed rate F10. But the tool broke after making 8 windows (about 60 minutes of work). What can I improve in my work so that the cutter can withstand, for example, 20 windows. Thank you!
Next, lookup the recommended feed per tooth (chipload) in Table 3 (ft ≈ 0.004 in/tooth) and calculate the feed rate using Equation 3:
First, lookup the recommended surface speeds in Table 1 (VALUM ≈ 625 ft/min, VSTEEL ≈ 250 ft/min (notice the 2.5 multiplier))
Note that these speed and feed values are guidelines assuming proper (flooded) lubrication, workpiece stiffness and depth of cut. When applying oil manually (as in the lab), scale the feed and speed back to 60%, so N = 570 rpm and f ≈ 18 in/min (final answer). Note also this problem assumes we peripheral milling versus plunge milling (since we never teach the students the latter in lab).
Material ductility makes a sharp cutting tool essential for cutting precious metals. Variable Helix for Aluminum Alloy tools can be used for the softer materials such as pure gold, silver, and platinum.
Example 5: Calculate the speeds for parting off 1 diameter aluminum and 1 diameter mild steel workpieces on the lathe using the standard carbide part-off inserts.
TIP1: Since annular cutting is a plunging operation, it should generally be performed at 75% of the speed and 25% of the feedrate of the calculated peripheral cutting parameters (as with endmill plunging).
Precious metalslist by value
Example 2A: Calculate the speed and feed for a 1″ diameter, 4 flute HSS endmill in aluminum using a manual milling machine in lab.
Please begin by reviewing the comprehensive course document on this topic, as it clearly explains the process of calculating these parameters for drilling and milling operations. The governing equations are summarized below.
TIP: When working with plastics with good machinability, use the cutting parameters for aluminum up until the point that the plastic melts.
First, lookup the recommended surface speed in Table 1 (V ≈ 250 ft/min) and calculate the spindle speed from Equation 2:
First, lookup the recommended surface speed in Table 1 for a 1 HSS endmill cutting aluminum (V ≈ 250 ft/min) and calculate the spindle speed from Equation 2 using the aforementioned 75% speed reduction:
TIP: Reamers should generally be run at half the spindle speed and twice the feed per revolution of the equivalent sized drill bit.
Semiprecious metalslist
Hello! I have a few drawings I would like to see if you would be able to quote for me ? Are you able to provide me an email I can send these for your review?
TIP: Countersinking should generally be performed at 25% of the speed and the same feed per revolution as the equivalent sized drill.
Great question, I suggest reaching out to [email protected] with all the information about the application. One of our technical associates will be able to dive deeper into your application and find the best possible solution for you.
Next, lookup the recommended feed per tooth (chipload) in Table 3 (ft ≈ 0.008 in/tooth) and calculate the feed rate using Equation 3:
TIP2: Do not plunge an annular cutter at a feedrate less than 0.001 ipt (inch per tooth) in strain hardening materials like 304 stainless or titanium.
Sign up to receive a monthly recap of: – The latest machining solutions – Machining tips and tricks – A recap of our most popular posts
Silver and gold have particularly favorable thermal conductivity and electrical resistivity. These values are listed in Table 2, along with CC1000 (annealed copper) and annealed 6061 aluminum, for comparison purposes. Copper is generally used in electrical wiring because of its relatively low electrical resistivity, even though silver would make a better substitute. The obvious reason this isn’t the general convention is the cost of silver vs. copper. That being said, copper is generally plated with gold at electrical contact areas because it tends to oxide after extended use, which lowers its resistivity. As stated before, gold and the other precious metals are known to be resistant to oxidation. This corrosion resistance is the main reason that they are used in cathodic protection systems of the electronics industry.
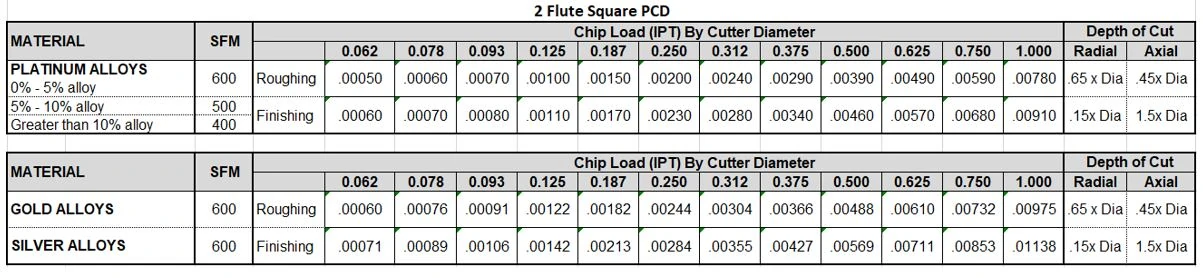
Hi Richard- Sterling Silver is a Silver alloy with around 92% silver and 8% copper therefore a non-ferrous alloy cutter can be used at the recommended speeds and feeds under “Silver Alloys”. For machining 10K-14K gold it really depends on the nickel content as this is a hardening alloy and may be more difficult to machine. If you would like to play it safe a PCD cutter would have no trouble cutting through 10K-14K gold as these types of cutters can be used to cut pretty much anything that is non-ferrous. A PCD cutter will also give you the longest tool life.
Example 4: Calculate the speed and feed for a 1″ diameter, 6 flute HSS annular cutter in ¼ thick aluminum on a manual milling machine in the lab.
Sometimes called “noble” metals, precious metals consist of eight elements that lie in the middle of the periodic table (seen below in Figure 1). The eight metals are:
Top 10precious metalslist
Pt-Ir alloys are noticeably harder and stronger than any of the other alloys and make excellent heads for spark plugs in the automobile industry. Rhodium is sometimes added to Pt-Ir alloys to make the material less springy (as they are used as medical spring wire) while also increasing its workability. Pt and Pt-Rh wire pairs are extremely effective at measuring temperatures and are therefore used in thermocouples.
Noble metal
Note: since applying oil manually, scale the speeds back to 60%, so NALUM ≈ 1425 rpm and NSTEEL ≈ 570 rpm (final answer). Note these are MAXIMUM values and lathe chuck safety must take precedence; spinning the lathe chuck at 570 rpm is about the upper limit of what we safely do in the lab, so for smaller or easier to machine workpieces, DO NOT EXCEED 600 RPM regardless of the calculation results, unless you are running a collet chuck.
A general rule of thumb for materials which are strong enough to support the drilling process is that fr is between 1 - 3% of the drill diameter, depending on the material strength.
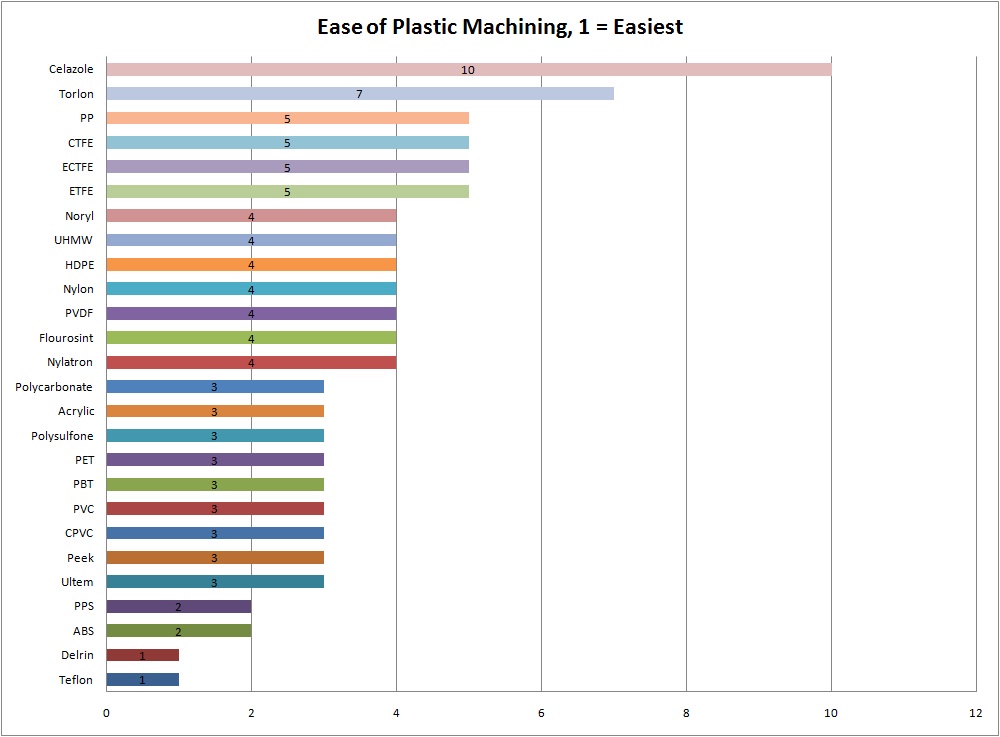
As you can see Acetal (Delrin) is one of the most machinable plastics and nylon is four times less machinable (which is why it should usually be avoided!).
Next lookup the recommended feed per revolution for the equivalent size drill bit in Table 2 (fr ≈ 0.006 in/rev) and calculate the feed rate using Equation 3:
* multiply feed values in table by 0.5 for difficult to machine materials, flexible toolholding or workpieces, or lighter-duty machines*
Note that these speed and feed values are guidelines assuming adequate (flooded) lubrication, workpiece stiffness and drill depth less than 3 drill diameters (0.75″). When applying oil manually (as in the lab), scale the feed and speed back to 60%, so N = 450 rpm and f = 3.6 in/min (final answer).
www.harveytool.com www.helicaltool.com www.micro100.com www.titancuttingtools.com www.corehog.com www.valorholemaking.com
The science behind creating these precious metals just blows my mind. It is so amazing that we are able to figure out what elements make up the metal and re-create it. I find it interesting that platinum has a high melting point, would that allow it to be used for higher temperature situations then other metals?
Platinum and its respective alloys offer the most amount of applications as it can achieve a number of different mechanical properties while still maintaining the benefits of a precious metal (high melting point, ductility, and oxidation resistance). Table 3 lists platinum and a number of other PGMs each with their own mechanical properties. The variance of these properties depends on the alloying element(s) being added to the platinum, the percentage of alloying metal, and whether or not the material has been cold-worked or annealed. Alloying can significantly increase the tensile strength and hardness of a material while decreasing its ductility at the same time. The ratio of this tensile strength/hardness increase to ductility decrease depends on the metal added as well as how much is added, as seen in Table 3. Generally this depends on the particle size of the element added as well as its natural crystalline structure. Ruthenium and Osmium have a specific crystal structure that has a significant hardening effect when added to platinum. Pt-Os alloys in particular are extremely hard and practically unworkable, which doesn’t yield many real-world applications. However, the addition of the other 4 PGMs to platinum allow for a range of mechanical properties with various usages.
Higher hardness materials still require a sharp cutting edge. Therefore, one’s best option is to invest in a PCD Diamond tool. The PCD wafer has the ability to cut extremely hard materials while maintaining a sharp cutting edge for a relatively long period of time, compared to standard HSS and carbide cutting edges.
Note that these speed and feed values are guidelines assuming proper (flooded) lubrication, workpiece stiffness and depth of cut. When learning how to use the CNC, always start lower (around 60% on the spindle speed and feedrate override buttons) and work your way up as you gain confidence or purchase your own tools (lol).
First, lookup the recommended surface speed in Table 1 (V ≈ 625 ft/min) and calculate the spindle speed from Equation 2:
First, lookup the recommended surface speed in Table 1 (V ≈ 250 ft/min) and calculate the spindle speed from Equation 2:
The two parameters that have the most effect when machining are hardness and percent elongation. Hardness is well-known by machinists and engineers across the manufacturing industry as it indicates a material’s resistance to deformation or cutting. Percent elongation is a measurement used to quantify material ductility. It indicates to a designer the degree to which a structure will deform plastically (permanently) before fracture. For example, a ductile plastic such as ultrahigh molecular weight polyethylene (UHMWPE) has a percent elongation of 350-525%, while a more brittle material such as oil-quenched and tempered cast iron (grade 120-90-02) has a percent elongation of about 2%. Therefore, the greater the percent elongation, the greater the material’s “gumminess.” Gummy materials are prone to built-up edge and have a tendency to produce long stringy chips.
Next, calculate the feed rate used for plunging. Remember annular cutters should be fed at approximately 25% of the feedrate for an equivalent sized endmill. From Table 3, lookup the recommended feed per tooth for a 1″ HSS endmill (ft ≈ 0.008 in/tooth) and calculate the plunge feed rate using Equation 3:
Next lookup the recommended feed per revolution for the drill bit in Table 2 (fr ≈ 0.004 in/rev) and calculate the feed rate using Equation 3:
 18581906093