About Steve Harvey - what is harvey
The multi-scale complexity of lath martensitic microstructures requires scale-bridging analyses to better understand the deformation mechanisms activated therein. In this study, plasticity in lath martensite is investigated by multi-field mapping of deformation-induced microstructure, topography, and strain evolution at different spatial resolution vs. field-of-view combinations. These investigations reveal site-specific initiation of dislocation activity within laths, as well as significant plastic accommodation in the vicinity of high angle block and packet boundaries. The observation of interface plasticity raises several questions regarding the role of thin inter-lath austenite films. Thus, accompanying transmission electron microscopy and synchrotron x-ray diffraction experiments are carried out to investigate the stability of these films to mechanical loading, and to discuss alternative boundary sliding mechanisms to explain the observed interface strain localization.
To measure an existing radius corner, start by marking two straight lines along the edges of the worktop where the curve begins. Using your tape measure, draw a ...
End MillSpeeds and Feeds chart
Find Metal Chips stock images in HD and millions of other royalty-free stock photos, illustrations and vectors in the Shutterstock collection.
If you speak with experienced machinists, you’ll often hear rules of thumb related to speeds and feeds. As an example, one common rule is that the plunge depth should always be half the diameter of the tool. While this conventional wisdom can be useful, it’s important to remember that the Bantam Tools Desktop Milling Machine is quite different from many conventional CNC milling machines and the same rules may not apply.
3/32" Carbide 3 Flute 1 º Tapered Long End Mill. Used for general-purpose milling including profiling, slotting, roughing, cutting keyways and pockets ...
Milling is a physical act that drives a sharp, rapidly-spinning tool through a piece of material. Depending on the the type of material and tool you’re using, you’ll need to use different settings to mill successfully.
Poorly-optimized speeds and feeds can break tools, cause tools to get stuck in material, and can cause premature wear. You can end up with parts that have poor surface finish, take too long to mill, and cause the milling machine to be noisy.
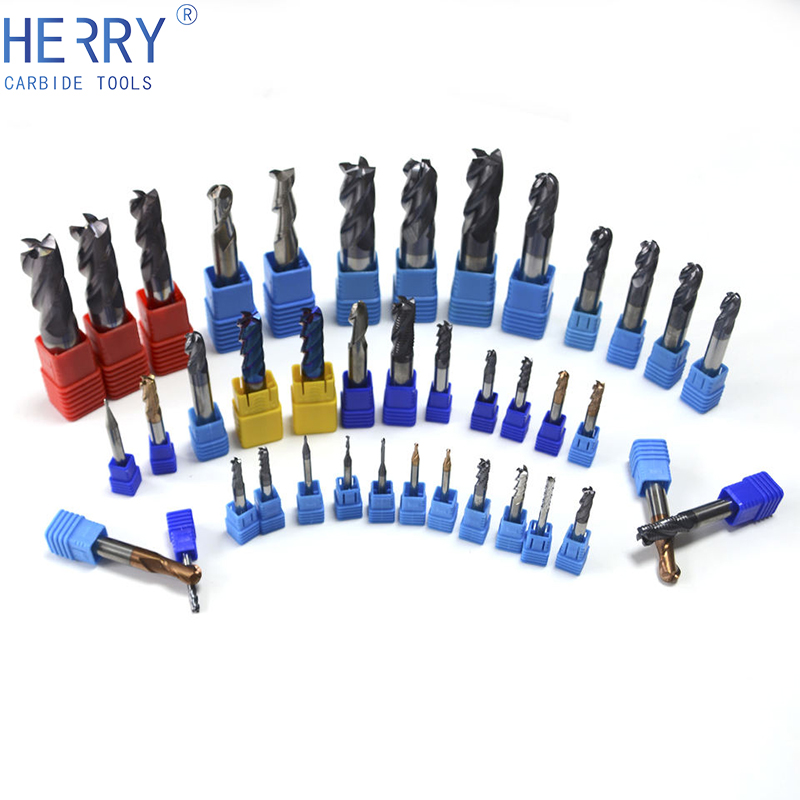
Carbide end millspeeds and feedscalculator
Our free speed and feed calculator can be used to determine the spindle speed (RPM) and feed rate (IPM) for the specified cutting conditions, as well as the ...
Owing to the layer-by-layer build-up of additively manufactured parts, the deposited material experiences a cyclic re-heating in the form of a sequence of temperature pulses. In the current work, this “intrinsic heat treatment (IHT)” was exploited to induce the precipitation of NiAl nanoparticles in an Fe-19Ni-xAl (at%) model maraging steel, a system known for rapid clustering. We used Laser Metal Deposition (LMD) to synthesize compositionally graded specimens. This allowed for the efficient screening of effects associated with varying Al contents ranging from 0 to 25 at% and for identifying promising concentrations for further studies. Based on the existence of the desired martensitic matrix, an upper bound for the Al concentration of 15 at% was defined. Owing to the presence of NiAl precipitates as observed by Atom Probe Tomography (APT), a lower bound of 3e5 at% Al was established. Within this concentration window, increasing the Al concentration gave rise to an increase in hardness by 225 HV due to an exceptionally high number density of 10^25 NiAl precipitates per m3, as measured by APT. This work demonstrates the possibility of exploiting the IHT of the LMD process for the production of samples that are precipitation strengthened during the additive manufacturing process without need for any further heat treatment.
Speeds and feeds are the collection of settings that determine the way in which a milling tool moves through material. Typically, machinists enter their speeds and feeds into CAM software (such as Fusion 360 or the Bantam Tools Milling Machine Software), and the CAM software combines the speeds and feeds with the geometry of the tool to determine the final toolpath.
Millingspeeds and feeds chartpdf
Ultimately, optimizing your speeds and feeds will result in milled parts that are precise, smooth, and look great, without breaking your milling tools.
Repeat testing until your results are satisfactory. Sometimes it takes a few tests before the perfect settings are dialed in. Although every project is different, using an experimental process like this will allow you to quickly determine ideal speeds and feeds.
Carbide end Mill RPMchart
For example regarding the crystallography of martensite most of the original pioneering works were based on transmission electron microscopy observations. TEM provides sufficient spatial resolution to resolve fine martensitic features such as e.g. laths, however, it provides only limited statistics of larger martensitic constituents (e.g. prior austenite grains) due to its limited field of view arising from the specimen and beam geometries. It is the development of the electron backscatter diffraction (EBSD) technique that enabled the systematic characterization of the hierarchical martensitic microstructure spanning multiple scales, i.e. ranging from prior austenite grains of hundreds of microns down to laths of tens of nanometers. Yet, it is also clear that the standard 2D EBSD-based analysis provides a rather simplified representation of the lath martensite crystallography. For example, 3D EBSD and 3D FIB analyses, as well as TEM observations reveal significant heterogeneities in the size and morphology of martensite sub-units even within a single alloy, which cannot be fully captured by stand-alone 2D investigations. Also, even in optimized conditions, EBSD cannot resolve the fine details of the martensitic sub-structure. Regarding martensite composition, similar progress was made due to the advances in another key technique, namely, atom probe tomography (APT). Similar to EBSD providing wider access to martensite crystallography, APT triggered investigations of e.g. carbon (C) Cottrell atmospheres, compositional relaxation and segregation, precipitation reactions in martensite and retained as well as reversed austenite layers in martensite. Arguably the most critical among these is the analysis of C in martensite, since interstitial C plays one of the major roles in the properties of martensite From these multiple studies we can in principle use several types of categories when describing these features in more detail. These are: Crystallography Mesoscopic morphology Interface types
This means that our knowledge about martensite today is more precise and detailed compared to the rough and in part historical categories and terms we use to describe it. Hence these are some of the typical terms that we use in metalllurgy which are relatively ill-defined owing to the long history of being studied.
HSS end millSpeeds and Feeds Chart
Here’s an analogy: Imagine using a small pair of scissors to cut a hole in a piece of paper, wood, and aluminum. Think about how hard you would have to squeeze the scissors for each material, and what the end result might look like. Then, think about using a bigger pair of scissors. The amount of force needed to cut each material is different, and it changes based upon the size of the tool. The same is true when using a milling machine. The type of material and the size of your tool changes how much force you need and how fast you can go. Speeds and feeds are the way to control the forces on the tool as it mills through a material.
In particular, compared to a traditional industrial mill, the milling machine’s lower-torque spindle works best with small tools at high spindle speeds and low pass depths. As a result, typical speeds and feeds recommendations may need to be modified, especially when milling hard materials.
Many professionals choose speeds and feeds from calculations based on the underlying physics of milling. Calculating chip load is one of the ways machinists set a baseline for where they start when dialing in their speeds and feeds.
Essentially, chip load is a number that represents the amount of material that each flute of your tool cuts on each revolution. It’s a useful number to optimize for. If chip load is too big, the tool will break. If chip load is too small, the tool can rub and quickly become dull — this is one reason why slower is not always better! To use our previous scissors analogy, if you use your scissors to make a lot of tiny cuts, they will wear out quickly. Instead, it’s often preferable to use fewer, larger cuts. You’ll cut the same material, but with better results.
In this guide, we introduce some of the concepts behind speeds and feeds and share pointers to help you get the most out of your Bantam Tools Desktop PCB Milling Machine. We’ve also put together a list of recommended speeds and feeds for some common materials to get you started.
While professional machinists often take the time to calculate and optimize each setting, most users can get away with a bit of experimentation. Instead of worrying about every single factor, start with your best guess and experiment. You might break a few tools along the way, but you’ll quickly develop an intuition for speeds and feeds.
Valley Tool, Appleton, Wisconsin, specializes in carbide cutting tools, custom carbide tools, carbide tool reconditioning. Tool sharpening and Castrol ...
End Millspeeds and feedscalculator
When speeds and feeds are dialed in, you end up with precise parts that have a consistent surface finish. During milling, vibration and noise are minimized, you won’t break tools, and the overall milling time should be optimal for each part.
Recutting The Crap: A Tribute To The Clash, Vol.2 by Various Artists, released 21 April 2018 1. Joe Strummer - I Call Myself Strummer 2.
In the world of CNC machining, you’ll often encounter the phrase “speeds and feeds.” Finding good speeds and feeds for the type of material and tool you're using is critical in any machining project, but it can feel daunting when you’re just getting started. Luckily, following a few basic principles can make the process much easier.
Millingspeeds and feeds ChartMetric
Shop Laydown Threading Insert: 16NR G60-A, Carbide at MSC Direct top provider of high quality products.
To edit speeds and feeds in our software, you'll need to edit the settings for a custom tool using the Tool Library. To do so, follow these steps:
The three best types of saws for cutting thick plastic are a fine-toothed saw, a jigsaw, and a table saw. A fine-toothed saw works best for precision plastic ...
Carbide End MillSpeeds and Feeds chart
Because of all of these factors and more, there’s no one-size-fits-all list of speeds and feeds. Every project is different, and it may require some experimentation to find the settings that work best. Ultimately, what matters is that you end up with a milled part that meets your specifications. Once you know how each input contributes to the end result, it'll be easier to fine-tune your settings.
The established terminology to describe martensite, specifically lath martensite, has been continuously developing over the years with the gradually improving different types of experimental observations which step-by-step gave additional insights that some of the original terminology did not contain or reflect.
Though the below pages were developed when we only sold our Desktop PCB Milling Machine, they are still a good relevant starting point when learning about these materials and using our Bantam Tools Desktop CNC Milling Machine. To make it easier to use these recommended feeds and speeds, we’ve created a way for you to quickly import all the settings you see listed below into our software. To download the custom tool library files, go to the material page listed below. To learn how to use these libraries, check out our Custom Tool Library page.
To improve the fundamental understanding of the multi-scale characteristics of martensitic microstructures and their micro-mechanical properties, a multi-probe methodology is developed and applied to low-carbon lath martensitic model alloys. The approach is based on the joint employment of electron channeling contrast imaging (ECCI), electron backscatter diffraction (EBSD), transmission electron microscopy (TEM), atom probe tomography (APT) and nanoindentation, in conjunction with high precision and large field-of-view 3D serial sectioning. This methodology enabled us to resolve (i) size variations of martensite sub-units, (ii) associated dislocation sub-structures, (iii) chemical heterogeneities, and (iv) the resulting local mechanical properties. The identified interrelated microstructure heterogeneity is discussed and related to the martensitic transformation sequence, which is proposed to intrinsically lead to formation of a nano-composite structure in low-carbon martensitic steels.
Martensitic materials result from a specific type of phase transformation that produces the structure known as martensite. Martensitic transformations were first observed and described in steels although they occur also in may other materials, such as e.g. in Titanium alloys. It received its name from Professor Adolf Martens who suggested that the martensitic reaction is displacive in nature and forms through a highly ordered crystallographic shear transformation, which involves no change in chemical composition or atomic diffusion, i.e. no atomic redistribution between phases. Recent atom probe tomographic analysis reveals though that atomic relaxation and short range diffusion can take place during martensitic transformations. However, many martensitic reactions normally occur athermally, i.e. via a diffusionless transformation or with only very local diffusion and martensite is then formed upon cooling from a higher temperature phase which is referred to as the parent phase. In steels this parent phase is known as austenite and this is also the term often used to describe the parent phase in shape memory alloys although technically speaking this is mostly incorrect. Although the early work describes the formation of martensite as being free from nucleation and growth, it is now accepted that the basic characteristics of martensite type transformations are in fact consistent with the general nucleation - growth framework. The martensite reaction in plain carbon steels proceeds from an equilibrium austenite phase to a non-equilibrium (metastable) low temperature martensite phase. Since the martensite is metastable it will only form through very rapid cooling. In fact the rate of growth is so high in these reactions that the volume change associated with the reaction is controlled almost entirely by the nucleation rate. In many martensitic transformations however, the low temperature phase is itself an equilibrium phase rather than a metastable one. In these cases the phase transformation occurs by the fast growth martensitic mode even with very slow cooling rates. The transformations in these systems occur martensitically but there is no need for a rapid quench to secure the fast growth mode as there is in steel. This is the case with shape memory alloys and many pure elements.
While every software package uses different nomenclature and different toolpaths require different settings, here are the most important settings to learn:
After completing your purchase, you will receive a prompt email containing a secure link to download your digital files. Available chamfers: 0.5 | 1.0 | 1.5 ...
20141117 — Vargus - Vardex Main Catalogue. ... Deep Threading - Long Tools for Deep Holes
. 3 x Do (L1 ≤ 3 x ...
 18581906093