Accuracy and Performance Analysis of Machine Tools - accurate performance machine
One last thing about flood coolants. Above a certain critical surface speed, they all start to work about the same. The faster you go the less cooling effect they have.
What isCNC coolantmade of
Those materials are often more dependent on the coolant for cooling to offset the inability of the material to carry heat. That inability makes it harder for the chips to carry away heat. And also harder for the workpiece to stay cool without changing size due to excess heat. Titanium further compounds the problem by producing relatively small chips.
Lack of minerals in the water supply is a primary cause of foaming in coolants. Check the water's hardness using Hardness Testing Kits is advisable.
A big downside of liquid and mist coolants is that inevitably they will create a mist in the shop air. Left to its own devices, this mist will wind up in your lungs and it’s definitely not good for you. The answer to this problem is to employ a Mist Collector to extract the mist before it can go very far.
In fact, I was very pleased when Haas released a video called, “Haas Chip Clearing and Tool Lubrication.” The video puts the emphasis where it should be and not on the cooling aspects of machine coolant. Finally, the word is getting out about what cnc coolant is all about!
Vertical lathes are good for heavy-duty since they make it easy to place workpieces. The vertical lathe allows for gravity to hold the pieces in place and reduces the need for clamps, making it more efficient for big workpieces between 1-20 meters. Just like slant bed lathes, vertical lathes also allow multi-tooling, which increases efficiency.
This is the most popular choice since they are easier to set up, cost less than vertical turning centers, come with less hassle when operating, and are easier to computerize. They are best suited for small parts and are very flexible due to having a longer bed about the spindle. A horizontal CNC turning center also comes with a tailstock (which helps to safely process and support the workpiece)- one thing that is very uncommon in vertical CNC turning centers.
While we’re on the subject of Misting, there are basically two kinds of Mister–plain old Mist systems which produce a coolant aerosol:
When using coolants that incorporate water, it is important to understand the appropriate coolant concentration to achieve the best results. This concentration is measured with a refractometer3Fukuta, Mitsuhiro; Yanagisawa, Tadashi; Miyamura, Satoshi; Ogi, Yasuhiro (2004). “Concentration measurement of refrigerant/refrigeration oil mixture by refractive index”. International Journal of Refrigeration. 27 (4): 346–352. doi:10.1016/j.ijrefrig.2003.12.007 and must be monitored regularly to offset the effects of evaporation.
It may surprise you to learn that very few recommend different feeds and speeds for mist versus flood coolant. The reason is that there is a baseline expectation that no matter what you do for coolant, you will make sure that chips are adequately cleared.
Besides, CNC turning centers necessitate just one operator, as opposed to manual lathes that demand multiple skilled workers. This substantial reduction in labor costs, coupled with the minimal training required, renders it a highly cost-effective choice for businesses.
The reason for the difference is the coolant doesn’t make efficient contact everywhere. Also, if you’re using the right cutting parameters (e.g. feeds and speeds), most of the heat is carried away in the chips, not the coolant.
References1C S Reddy, Araveeti & D V, Paleshwar & Murthy, Kln & Sandeep, B.. (2020). A Review on Coolant Feeding System of CNC Machining Process. 10.1007/978-981-15-7827-4_44. 2Application of coolants during tool-based machining – A review Khor Zheng Yang a, A. Pramanik a, A.K. Basak b, Y. Dong a, Chander Prakash c, S. Shankar d, Saurav Dixit e f, Kaushal Kumar g, Nikolai Ivanovich Vatin e3Fukuta, Mitsuhiro; Yanagisawa, Tadashi; Miyamura, Satoshi; Ogi, Yasuhiro (2004). “Concentration measurement of refrigerant/refrigeration oil mixture by refractive index”. International Journal of Refrigeration. 27 (4): 346–352. doi:10.1016/j.ijrefrig.2003.12.007
The second thing to notice is that air is pretty lousy, about 1/4 as good as water. That’s not as bad as predicted, since water carries 25x more heat than air.
Many coatings used on tools can also provide lubrication. But coatings are fragile. They wear off or chip and shouldn’t be the primary answer to BUE. In the end, a little bit of mist can deal with this problem as well as flood coolant, so it isn’t the end of the world.
On the flip side, the oil lubricates better (natch), and there are still some applications where machinists may prefer oil (usually turning) to the water soluble coolants.
Lubrication helps the tool to cut more easily so it generates less heat. As the face of the tool slides across the workpiece, it rubs while cutting. As the chip curls up, it also rubs on the tool, generating more heat. All that rubbing will produce less heat with a little lube, as any sliding fit would.
Once you have Through Spindle Coolant, you’re still not at the pinnacle. To go further, you’ll need a High Pressure Coolant system.
Vertical CNC turners have a fixed spindle and chuck, where the workpiece is held onto the chuck with jaws. It uses the natural force of gravity to hold the workpiece in place, cutting down the need for more clamps. The benefit of a vertical CNC turner is that it is less complex to use than a horizontal one and is fitted well for complex design-making.
Semi-synthetics are a hybrid of synthetics (polymer) and soluble oils. They contain 2-30% mineral or petroleum oil. The remaining percentage of semi-synthetic components consists of water and emulsifiers. Other elements may include biocides, wetting agents, and corrosion inhibitors.
A much bigger role for lubrication is reducing the likelihood of Built Up Edge (BUE). This is a big deal as anyone who has seen a big wad of aluminum get welded to their cutter will attest to. Things stop working quickly when that happens!
Workers will no longer have to work with dangerous and sharp machine tools since machines operate CNC lathes now, which reduces the risk of injuries in the workplace. Workers will also not have to be closed when the production is taking place, which will almost wholly reduce accidents.
They are cheap and are therefore in common use. They comprise 60-90% petroleum, emulsifiers, or mineral oil and adhere to the workpiece during machining. They’re ideal for lubrication and offer excellent rust resistance with the right additives.
CNC lathes are best for small productions since they are easy to set up and consist of simple parts, but they require more time to produce. However, a CNC turning center is well-suited for large-scale production as it can multi-task and remove material by itself.
The baseline role for any would-be CNC Coolant system is to clear the chips. Recutting chips is bad for the cutter, bad for your part’s surface finish, and is to be avoided. Therefore, let’s start with the assumption that whatever you’re doing about CNC Coolant it is clearing the chips. For example, manual machinists often make use of chip brushes to periodically sweep chips away. This is way too cumbersome and ineffective for CNC, but in that sense, the chip brush is a form of “Coolant”.
IsCNC coolantdangerous
To calculate proper feeds and speeds with premium cnc coolant options, just click the boxes in the machine profile that tell G-Wizard your machine has these capabilities. Then, you can operate the check boxes on the Feeds and Speeds Calculator to take advantage:
While it may seem tempting, never use water alone as it encourages rust and corrosion. Instead, choose one of the 4 coolants types listed below.
If the material you’re cutting transfers heat poorly relative to aluminum (which is an excellent conductor of heat), steel (a decent conductor), or other common materials, make sure you’ve got a good flood coolant setup and are using it well.
202049 — Axis Product Naming - Download as a PDF or view online for free. ... It explains the naming conventions for each ... Axis Communications Axis.
CNC coolant may be made of oil, oil-water emulsion, aerosols (mists), air, or other materials. They may be made from petroleum, plant oils, water, or compressed air.
The more modern, Computer Numerical Control (CNC) lathes operate with the help of computers. It works like a normal lathe, except computer programming overlooks the cutting process. This results in a high-precision finished work, that is more accurate and efficient than a manual lathe.
Performance with a High Pressure Coolant system can be amazing compared to running without one. G-Wizard is set up to give appropriate SFM bonuses when you have HPC, so go ahead and check it out. You can use G-Wizard to figure out the ROI (return on investment) for an HPC system by calculating what sort of increase in feeds and speeds the HPC will enable for you.
BTW, if you’re very conscientious about coolant and take time to make sure your nozzles are properly aimed, you can go ahead and tick the box for PCN and get the bonus. You’re doing the same thing the automation does.
CNC turning centers also allow for multiple-axis, sub-spindle, and Y-axis (ability to move up and down) capabilities, thus making them multitasking machines, which CNC lathes do not have. These make turners’ cutting ability more versatile, making them capable of performing in ways a CNC lathe cannot.
Spindle: It is responsible for rotating the cutting tool. The spindle also includes both the spindle assembly and the spindle drive system. The C-axis drive will also be included here.
BestcoolantforCNCmachines
CNC lathe parts and CNC turning parts play a pivotal role in shaping our daily lives by contributing to the manufacturing of diverse products and components. Here are some real-life examples below:
Join 100,000+ CNC'ers! Get our latest blog posts delivered straight to your email inbox once a week for free. Plus, we’ll give you access to some great CNC reference materials including:
There are two material-specific considerations for coolant. The first is the tendency for BUE. Preventing chips welding onto the cutter through lubrication is important.
When is the right time to change a CNC machine coolant? Most CNC machine makers recommend changing coolant every 6-12 months as a general rule of thumb. The exact time to change coolant will be based on the machined material, coolant type, amount of machining use, and operating condition of the CNC machine. How do I kill bacteria in CNC Machining Coolant? There are several ways to kill bacteria in CNC Machining Coolant. They range from anti-bacterial additives that can be put into the coolant to ozone treatments to preventing oil films from blocking oxygen exchange with the coolant. What causes foaming in a CNC coolant? Lack of minerals in the water supply is a primary cause of foaming in coolants. Check the water's hardness using Hardness Testing Kits is advisable. What is CNC coolant made of? CNC coolant may be made of oil, oil-water emulsion, aerosols (mists), air, or other materials. They may be made from petroleum, plant oils, water, or compressed air. What is the best coolant for CNC machines? Never use water by itself, as it can lead to rust and corrosion. Instead, use one of the following types of coolant: Soluble Oils Soluble Oils are inexpensive and are the most common in machining operations. They're created by adding mineral oil to water in specific percentages. Emulsifiers are also added to keep the solution mixed. Other additives add additional useful properties such as corrosion resistance, bacteria prevention, and lubrication. Soluble Oils work best in light-cutting operations. Synthetic Fluids Synthetic Fluids combine water with additional chemical compounds but no mineral oil. Other additives can include lubricants, rust inhibitors, and corrosion inhibitors. A primary benefit of Synthetic fluids is no foaming. Foaming is more common in mineral oil-based coolants. Synthetic Fluids are more durable than other metalworking fluids. Semi-Synthetic Fluids Semi-Synthetic Fluids are a blend of mineral oil, corrosion inhibitors, and additives for clean operation in high-speed and high-pressure CNC machines. Straight Oils Straight Oils are not mixed with water and have a mineral or petroleum oil base. The include additives that are biodegradable and environmentally friendly. Straight Oils provide the best lubrication but have the poorest cooling characteristics.
The second is the ability of the workpiece material to absorb and transfer heat. Some materials do not transfer heat very well–titanium is a good example.
A CNC turning center is much better at precision and even more versatile due to its multi-axis. The existence of the axis also makes the entire machine more complex as it can carry out 5rt6several tasks at once in a more petite time frame.
Use of sharp cutters with very high rake angles (positive rake is your friend!) can help reduce adhesion, but it’s not enough.
A fully stocked Harvey Tool product offering featuring tools with a 140° point angle, allowing for efficient plunging through composite sheet metal.

Fortunately, BUE is material-specific. It applies mostly to Aluminum and low-carbon or unalloyed Steel. Titanium is another material that has a reputation for being sticky.
CNC CoolantPrice
There are several ways to kill bacteria in CNC Machining Coolant. They range from anti-bacterial additives that can be put into the coolant to ozone treatments to preventing oil films from blocking oxygen exchange with the coolant.
Along with the Y-axis, which we explained, it can also move in the A-axis, which is the rotation of the X-axis, the B-axis, which is rotation about the Y-axis, and the C-axis, which is rotation about the Z-axis. The Z-axis is at a 90-degree angle from the cutting tool, and the X-axis stays parallel to the cutting tool.
Compared to that, CNC turning centers can go up to $500,000, depending on the number of axes and tools, but they are generally more expensive than a CNC lathe.
There’s one more thing called for from a baseline CNC Coolant system and that’s the ability to lubricate the cutter and material if needed. Certain materials, such as aluminum, require lubrication or they will tend to weld onto the cutter and disaster follows not long after–broken cutters, globby taffy-like aluminum clinging to cutter, and ruined part. Clearly avoiding this has to be a part of our baseline.
Free CNC Speed and Feed Calculator allows CNC Machinists and CAD/CAM Programmers to calculate milling and drilling speeds and feeds for a wide variety of ...
Synthetic Fluids come in two types: simple and complex or emulsifiable. Simple Sythetics are commonly used for light-duty grinding. Complex synthetics contain fluids suitable for moderate to heavy-duty machining procedures.
Choosing the right coolant strategy is important for most machining operations. Coolant delivery can be the key to superior performance of your machining process.
One last tip. Coolant and chips are messy. Most machinists like to use an air gun to spray them off the part before removing it from machine. You can automate that task with a chip fan.
Turret: Also known as a tool turret, it is used to store various tools, including external devices such as grooving and threading.
With Through Spindle Coolant, you’ve made sure the cnc coolant is being delivered to exactly the right location where it will do the most good. The next level of benefit comes from dramatically increasing the pressure and volume of coolant delivered to that sweet spot in the cutting zone. Of course this improves chip evacuation, hence the reduction in the need for peck drilling, but High Pressure Coolant (abbreviated HPC) is where there’s a chance for the cooling ability of “Coolant” to really shine.
water-basedcoolantfor machining
By now you’re probably realizing there’s another reason not to give Feeds & Speeds bonuses for flood coolant: it’s hard to properly identify whether a flood system is really clearing the chips. Operators assume they are, but most are not paying close enough attention to it. How the coolant is aimed matters tremendously.
Bob is responsible for the development and implementation of the popular G-Wizard CNC Software. Bob is also the founder of CNCCookbook, the largest CNC-related blog on the Internet.
If the cutter must recut the same chips over and over again, you’re much more likely to experience built-up edge (BUE). BUE is where chips weld onto the cutter. It’s possible to use up all the chip clearance your cutter has available. The older chips have to compete with freshly cut chips, which can lead to cutter breakage.
TSC ensures the cnc coolant is going to exactly the right spot to make the most difference. BTW, there are lathe equivalents that go through the tool rather than the spindle, but the principle is exactly the same.
Shank Toolholders and Boring bars - This wide offering of easily applicable shank and boring bar toolholders adds another level of reliability and ...
BTW, people are constantly asking on the forums which flood coolant people like and use. We did a major survey that has resulted in our Buyer’s Guide to CNC Coolants.
By launching fewer larger droplets, the Fogbuster makes sure they don’t travel all over your shop–they mostly land on the workpiece where the thing is pointed. Better for you and just as good for the machining work. They cost a little more, but for a premium Mist system they sure are worth it.
Different tool coatings can help tools resist higher temperatures and they can also reduce friction by acting as lubricants…
If you want to produce high-quality machined parts with a sleek appearance, it’s essential to consider some critical factors related to CNC machining.
Soluble Oils, also known as water-soluble oils, are excellent for general machining applications. They perform well in diluted form and provide excellent lubricity and heat transfer performance.
They are primarily employed in high-heat processes such as surface grinding because of their excellent cooling capacity.
Which brings us to our next issue, Cooling (and its Evil Twin Shock Cooling). The temperature of the tool is the biggest factor affecting tool life.
There is no formal distinction between a CNC turning center and a lathe, but one clear distinction between them is their axis. CNC turning centers can have 3-axis, 4-axis, and 5-axis, making them more modern.
Good chip clearing and lubrication where needed are the baseline assumptions that our G-Wizard Calculator makes about your CNC Coolant. However, while we don’t recommend slower feeds and speeds as the answer to poor coolant, G-Wizard does know how to take advantage of premium coolant options such as programmable nozzles, through spindle coolant, and high pressure coolant.
A CNC turning lathe is well equipped as it rotates the product to cut it, but CNC-turning centers are far more versatile due to the extra axes and twin spindles. Live tools can also easily be used with a CNC turning center, which enables the machine to use these tools and stop the spindle, which then helps to perform various activities like drilling, tapping, and milling. This means that a CNC turning machine gives a better advantage than a lathe.
The operation costs for CNC lathes are significantly lower due to fewer axes. One can expect the operational costs to be between $10 to $20. However, for CNC turning centers, the prices can go up from $25 to $30, but as production time is less for CNC turning centers, in the long run, it will save more operational costs.
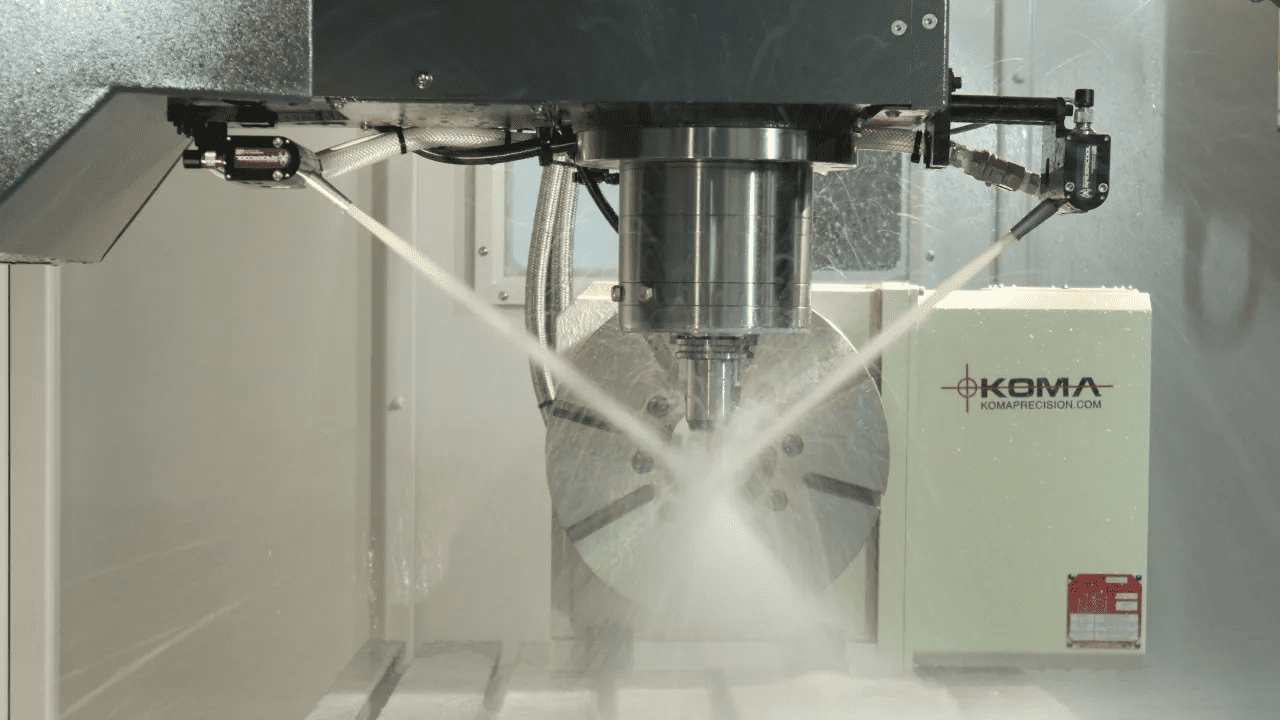
If you don’t have a full machine enclosure, flood coolant is messy and almost unusable. Fortunately, cooling is the least important thing about cnc coolant. We still must manage chip clearing and lubrication, but cooling is less important. So, we can dispense with flood coolant for many applications. A strong compressed air blast will handle chip clearing. Adding a lubricant to the air blast to make a mist takes care of lubrication.
A CNC lathe will only need one operator, compared to a traditional setting, due to the number of manual parts. CNC operators also require less training than their traditional counterparts, which also further reduces costs.
There’s another problem with liquid coolants too. It’s called “shock cooling.” Unless there is enough coolant to keep carbide from really heating up, what happens is those random droplets cool the carbide randomly. One moment it’s very very hot, the next a big droplet lands (splat, sizzle!) and it is shock cooled back down to low temperature. This leads to micro-cracking of the carbide which can severely reduce tool life. Always check with your tooling manufacturer, especially on high performance insertable tooling, whether there is a point where the coolant needs to be turned off and a pure air blast used to prolong your carbide’s life.
It is ideal for high-speed, micro-tooling of non-ferrous metals and some plastics due to a thinner-than-water viscosity that allows the ethanol to quickly cover and cool more of the surface area on fast-moving parts. The low evaporation point of ethanol makes it anefficient cooling and lubricating solution. Since the ethanol simply evaporates, disposal, recycling and their associated costs are a thing of the past. Plus, ethanol coolants leave no residue on machined parts, which makes costly secondary operations, like de-greasing, obsolete — maximizing throughput, increasing efficiency and ultimately improving a manufacturer’s bottom-line.
Types ofcoolantused inCNCmachines pdf
However, it is necessary to understand the difference between a CNC lathe and a CNC turning machine as failure to do so will lead to extra, unnecessary costs, longer lead times, and a general difficulty in operation.
2. Lubrication: Some materials, like aluminum or some steels, are sticky. They have a chemical affinity for the cutter and will try to weld themselves to the cutter. Lubrication makes things slippery so the chips are less likely to adhere and weld on. Clearing chips makes adherence less likely too.
Most tooling manufacturers recommend you turn off the flood coolant when surface speed goes above a certain point2Application of coolants during tool-based machining – A review Khor Zheng Yang a, A. Pramanik a, A.K. Basak b, Y. Dong a, Chander Prakash c, S. Shankar d, Saurav Dixit e f, Kaushal Kumar g, Nikolai Ivanovich Vatin e. They say this will increase the life of your tooling. If it was all about heat, that shouldn’t be the case as more surface speed means more heat.
This may come as a surprise to many, but the difference is almost entirely a function of which one will clear the chips better. Let’s do a simple thought experiment. Suppose you have a simple low-performance Flood Coolant system. It’s putting out a slow trickle of CNC Coolant. Maybe you’ve even turned it down so you don’t have to wear a pancho when running the machine because you have no enclosure. Imagine your machine cutting a deep pocket or slot with your trickle of Coolant. The pocket is full of cutting fluid. There’s no question the cutter is immersed in it. But are the chips being cleared? In a word, “No!” They’re sitting under that pool, and the pool is almost protecting them from removal because the force of the Flood is not strong enough to blast them out of there.
Unlike lathes, CNC turning centers are all slant beds where the way system and the bed are not on the front but on the back.
Khodiyar Industrial Products is a leading manufacturer of pneumatic, electrical, and industrial chamfering machine in Ahmedabad, Gujarat, India.
Chuck: It is attached to the headstock and holds the material, which will be turned into the final product. Three jaw chucks are used for holding, and any hexagonal and cylindrical shapes can be fitted into it.
These coolants are the friendliest non-polluters because they contain no petroleum or mineral oil. They comprise rust inhibitors and lubricants that break down in water. They’re typically mixed with water to a certain concentration to produce a metalworking fluid.
Folks can stand by giving an spritz now and then from a can of WD-40, but like the chip brush, that’s really not adequate if you plan to cut much of whatever material demands the lubrication. There are some cutter coatings that eliminate the need for lubrication, but be aware the coatings wear and the failure will be sudden when there’s no long enough coating to keep going. You can sometimes make due if your chip clearing is prodigious enough and you keep your cuts extremely shallow, but you’re probably living on borrowed time for your cutter the deeper you go and the more chips escape extraction and wind up being recut.
3. Cooling: Liquids are capable of carrying much more heat away from the cut than air. Plain water conducts heat 25 times more efficiently than air, for example. So water-soluble coolants are better at cooling than oil-based.
High Pressure Coolant can provide an alternative. By using very high pressures, 1000 psi or more, as well as high volumes, it’s intent is to deliver so much coolant that nearly all of the heat will be carried away before it can ever build up. Practically speaking, what this means is higher surface speeds, more rpms at the spindle, higher material removal rates, and longer tool life. You can trade some of that off as well. For example, let’s suppose you’ve got a job drilling thousands of holes in some material that requires carbide drill bits. You might very well sacrifice a little of the ultimate rpm potential in exchange for longer life so you don’t break a bit and have to scrap a part.
Don’t overlook the benefits of gravity for machining. On vertical mills, gravity makes it harder to pull chips out of deep holes. On lathes and horizontal mills, gravity makes it easier. Kinda makes you wonder why nobody has a machine that cuts from underneath. You’d need a pretty crazy palette loader so you could drop the workpiece onto the table and then flip it for cutting. Too far out, I thought, but then I discovered such machines actually exist. They’re called “Inverted Spindle Lathes” and are a potent alternative to bar fed lathes.
A turning center usually has more features and can do more things than a regular CNC lathe. Accuracy is a crucial factor in any manufacturing process, and CNC turning centers offer much higher levels of precision compared to manual lathes. Computer control, advanced tools, and sophisticated software help produce consistent and accurate results.
Carbide develops micro-cracks under the thermal shocks of uneven heating and cooling. Imagine submerging glass heated by boiling water into ice water. It’s going to crack.
Synthetic Fluids combine water with additional chemical compounds but no mineral oil. Other additives can include lubricants, rust inhibitors, and corrosion inhibitors.
Plain old Misters work great for machining, but they use more coolant than they need to and they fill the shop air with the mist–not the world’s best thing to be breathing all day. There is an alternative called the Fog Buster that focuses on propelling larger droplets without creating an aerosol mist:
Cnc coolantnear me
As CNC turning centers are far more advanced, they can cut more precisely and work with more complex components and intricate designs than a CNC lathe due to their flexibility.
Manual lathe work can be highly dangerous, as it involves working with sharp and often heavy tools close to the machine. CNC turning centers minimize these risks by using automated processes, which reduces accidents and injuries in the workplace.
With Through Spindle Coolant, performance can be greatly increased. It is nearly the perfect delivery system for coolants. Even higher chip loads can be tolerated, holes can be deeper, and peck drilling can be eliminated due to the improved evacuation of chips. Of course, G-Wizard Calculator has an option for TSC too.
Recutting chips destroys surface finish and dulls tools much faster. In the worst case, a cutter down in a slot or hole can get clogged with chips and get much hotter or even break.
Don’t let complexity slow you down. Choose RapidDirect for a seamless, efficient, and cost-effective CNC machining experience. Upload your design files today and unlock the potential of precision engineering!
One thing you’ll quickly discover about these bonuses is they can be a very cost effective way to improve your shop’s productivity. Investments in better coolant technology are often not that expensive relative to the benefits you get on nearly every job.
I’ve heard many professional machinsts flat out declare you can’t machine aluminum without some form of lubrication. Even a little spritz of WD-40 makes a big difference with aluminum.
Amazon.com: PVC Chamfer Tool, 2 in 1 Inner Outer PVC Deburring Tool, Pipe and Tubing Chamfer Tool for OD 0.92 to 3.89, ID 0.75 to 3.5 CPVC ABS PP PE Pipe, ...
Straight Oils are not mixed with water and have a mineral or petroleum oil base. The include additives that are biodegradable and environmentally friendly.
Programmable Coolant Nozzles are great, but they can’t guarantee the coolant goes to the optimal place every time. Some places are just not accessible, for one thing. Consider the bottom of a deep hole you’re trying to drill. No way to aim the nozzle there–it’s below the surface of the material and there is no access. Or is there?
Coolant performs 3 roles in machining1C S Reddy, Araveeti & D V, Paleshwar & Murthy, Kln & Sandeep, B.. (2020). A Review on Coolant Feeding System of CNC Machining Process. 10.1007/978-981-15-7827-4_44. :1. Chip Clearing: Spraying a cutting fluid at the cut helps move the chips out of the way of the cutter. Clearing chips minimizes recutting the chips. The chips already cut aren’t getting sloshed around and slammed aginst the walls of the cut.
Compared to the traditional straight cutterhead, the helical/spiral cutterhead has tungsten carbide insert knives mounted on the surface of the cutterhead in ...
Lathes are machine tools that rotate a workpiece to perform various operations and shape it into a desired, cylindrical shape. They were first used in Ancient Egypt, around 1300 BC, and then the French started using them around 1550 CE to produce wooden works. During the Industrial Revolution, we created the modern lathe which we still use today in many manufacturing industries. Historically, traditional lathes always consisted of a 2-axis and a flatbed, a feature we can still find in modern CNC lathe beds.
So, let us explore their abilities, differences, and advantages together to understand which is better for your CNC projects.
These oils consist of petroleum, mineral oil, animal, and other elements derived from vegetables or fats. They may also contain other ingredients, such as phosphorous, sulfur, and chlorine additives. Straight Oils are usually insoluble in water and often provide the best lubrication, rust prevention, longer sump life, and easier maintenance.
Now consider a good Misting system. There’s no pool to hide under. You can easily see whether the chips are being cleared and crank up the air pressure if not. You’re less worried about the mess because Mists are much less messy. It should now be more obvious that Mist is going to be a better CNC Coolant option than a mediocre Flood Coolant!
CNC lathes can work for extended periods without needing any halt in the process. Furthermore, they can also work on multiple parts together, which results in more production in less time.
Flatbeds are used in the manufacturing process, especially in heavy-duty (requires a lot of strength and power) turning. Due to higher stability, the beds are more stable, which leads to more precision and accuracy. This makes it a good candidate for creating complex geometrical workpieces and working with bigger workpieces. But they are more limiting when it comes to tool-changing so, for example, changing from boring to knurling tools will take time.
Through Spindle Coolant (abbreviated TSC) gains access by feeding coolant through your spindle like the name says, and from there it can exit via passages inside the tool. You really can have a nozzle built into the bottom of your drill bit, for example:
Some machining operations, such as gun drilling, emphasize cooling even less. They are recommending a coolant (oil) that conducts half as well as water.
Let’s shift our focus from Feeds and Speeds for a moment and discuss CNC Coolant. Regrettably, such liquid is referred to as “coolant” when the truth remains, cooling is its least significant function in machining.
With a CNC turning center, it is possible to outline intricate designs on heavy-duty with shorter production time and higher accuracy.
At higher speeds, there isn’t time for a big gout of coolant to make it’s way into all the nooks and crannies. Cooling becomes less and less consistent. This also contributes to the shock cooling effects that make cnc coolant hard on carbide life above certain speeds.
For many high performance applications, machinists can focus on chip clearance and lubrication and ignore the cooling issues. Above a certain surface speed, many tooling manufacturers recommend turning off the flood coolant and using an air blast (perhaps with mist for lubrication) to clear chips. Materials that don’t transfer heat well like titanium will require flood coolant regardless.
They have vastly improved productivity compared to manual lathes. They can operate for longer periods without interruption, require less physical labor, and can work on multiple parts simultaneously.
A CNC lathe will produce lower products compared to a CNC turning center as it does not have as many axes or flexibility. On the other hand, its counterpart can make more finished products in a smaller amount of time as the axes can move in several directions.
Note that the amount of heat allowed is dependent on the tool material and coating. Carbide takes a lot higher temperatures than HSS. Some coatings, such as TiAlN, need the higher temperatures to do their job properly.
1/2" Boring BAR Set PRO Quality 9 PCS Carbide Tipped Bars 1/2" Shank Lathe Tool - Boring Bits - Amazon.com.
Sandvik, in their cutting tool study course, recommend either no flood coolant or copious amounts of flood coolant to avoid this problem.
Computer Numerical Control used in the production line increases accuracy further than traditional methods since the use of computers makes them more precise, which reduces the production of faulty goods.
Soluble Oils are inexpensive and are the most common in machining operations. They're created by adding mineral oil to water in specific percentages. Emulsifiers are also added to keep the solution mixed. Other additives add additional useful properties such as corrosion resistance, bacteria prevention, and lubrication. Soluble Oils work best in light-cutting operations.
There are a couple of parts to the answer. First, we need to make sure we can generate sufficient pressure on the Flood system to make sure the chips are cleared out. When it’s cranked up good, you almost can’t see what’s going on there’s so much CNC Coolant flying around. Second, we need to make sure the Coolant is properly aimed to clear the chips. That can be a little harder. Different tools are different lengths. Things move around as the work progresses. Typically, we want to either aim for the bottom of the cut or the top of material if the nozzle can’t “see” the bottom of cut.
Slant beds are perfect for medium-sized workpieces, making them suitable for aerospace and optics. Their multi-station turrets allow for multiple tools to be used at the same time. Furthermore, they are faster, which leads to faster production cycles. They are also compatible with automation, which reduces the need for manual labor.
Deciding between a CNC lathe and a turning center can be challenging. It boils down to the nature of your project and the investment you’re ready to make. At RapidDirect, we simplify this choice for you.
Most CNC machine makers recommend changing coolant every 6-12 months as a general rule of thumb. The exact time to change coolant will be based on the machined material, coolant type, amount of machining use, and operating condition of the CNC machine.
CNC Coolantoil
Are you new to the manufacturing industry and unsure about which to choose between CNC Lathe vs CNC Turning Center? CNC machining contributes a lot to the manufacturing industry by producing products with higher precision, more efficiency, and accuracy.
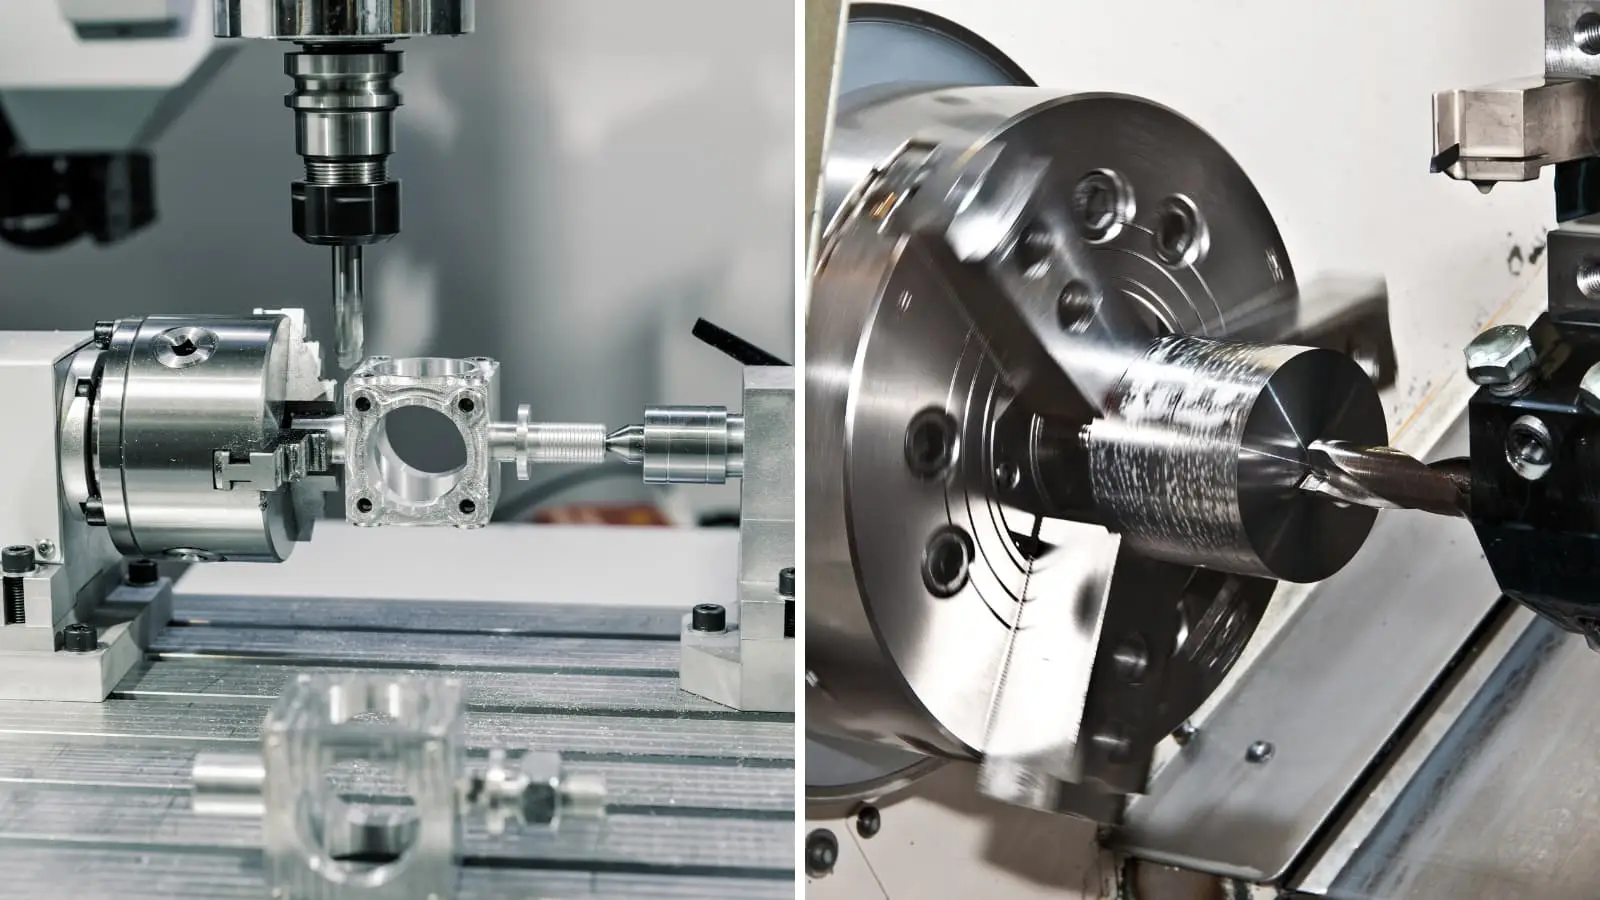
Multi-axis CNC machines act as an advantage when it comes to increasing efficiency since they reduce the need for more machinery. There is no need for a lathe and a mill because the turning center can do all of these.
Learn all about #DMAPLRC1010. Diablo's SDS-Plus rebar cutters provide one of the most durable drilling solutions on the market for rebar cutting.
A step up would be spritzing the area with an air gun. Perhaps you will even have rigged a continous air flow from a nozzle of some kind. Or, maybe you’re on a CNC Router and you’ve got a vacuum system sucking up all the chips as fast as they are made. Now we’re getting into the realm of the real baseline for CNC Coolant. A baseline provides no advantage, rather, it is the minimum acceptable level of Coolant to be usable and reliable for CNC work.
For example, drill bits made from high-speed steel (HSS) are fine for soft metals, while cobalt is the best drill bit for stainless steel. But solid carbide or ...
The trouble with Coolant’s cooling is that it can be spotty. A droplet hits the tool here, another hits the workpiece there, a third bounces off a chip, and there’s just not enough consistency. Mist and air blasts do almost as good a job cooling as a result. The exception is on materials like Titanium that don’t conduct heat very well. For those types of work, flood coolant is essential. But aluminum, for example, conducts heat extremely well. It’s hard to tell a difference between flood and mist unless you’ve really got a great flood system going.
CNC turning centers and lathes require similar maintenance; therefore, a similar maintenance cost is incurred, e.g., needing oils and coolants.
Semi-Synthetic Fluids are a blend of mineral oil, corrosion inhibitors, and additives for clean operation in high-speed and high-pressure CNC machines.
A little heat is good, as it softens the work material, making it easier to cut. A lot of heat is bad. It softens the tool, which means it wears, becomes dull, and cutting forces skyrocket. That makes it get hotter, and soon you have a vicious cycle.
The extremely high level of precision needed within the aerospace industry makes CNC machining a suitable manufacturing process for the sector.
The benefits of TiAlN aren’t even present until there is enough heat to “activate” it. So TiAlN is often used without cnc coolant. In fact, turning your cnc coolant off can often increase tool life under the right conditions because it avoids Shock Cooling.
Sure, it’s easier to photograph the action. But those piling chips are very hard on your cutter’s life and can even lead to breakage.
If your machine has no flood coolant, rig up an air blast or mist to get the chips out of there. Get paranoid about having too many chips around.
There are some materials where flood coolant still reins supreme. Stainless Steel and Titanium are two examples. It’s hard to do a good job on these with mist.
 18581906093