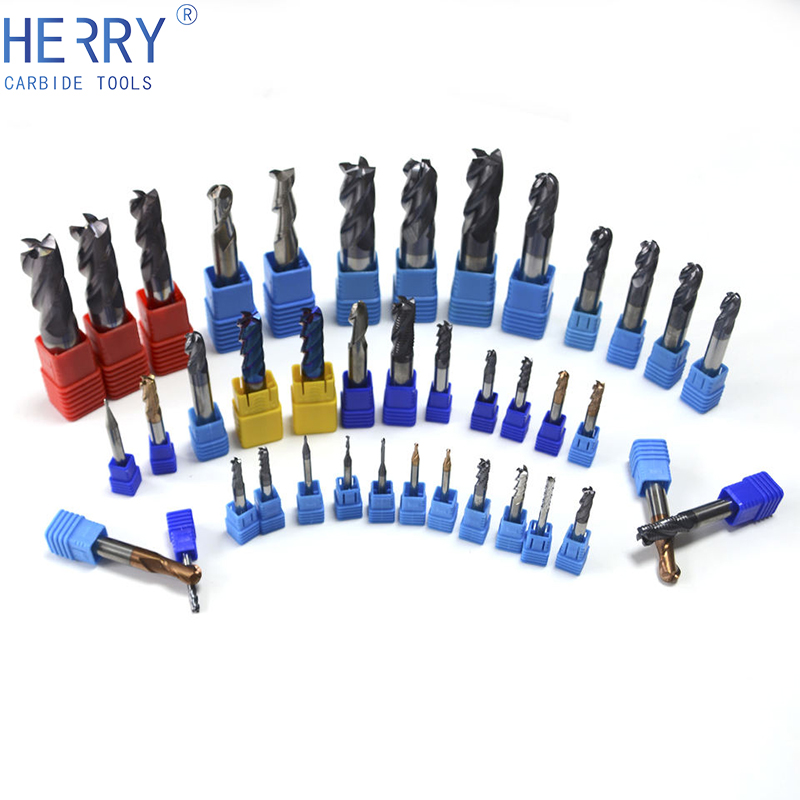
ace brand grooved shank concrete nail [1.0 - concrete nails ace hardware
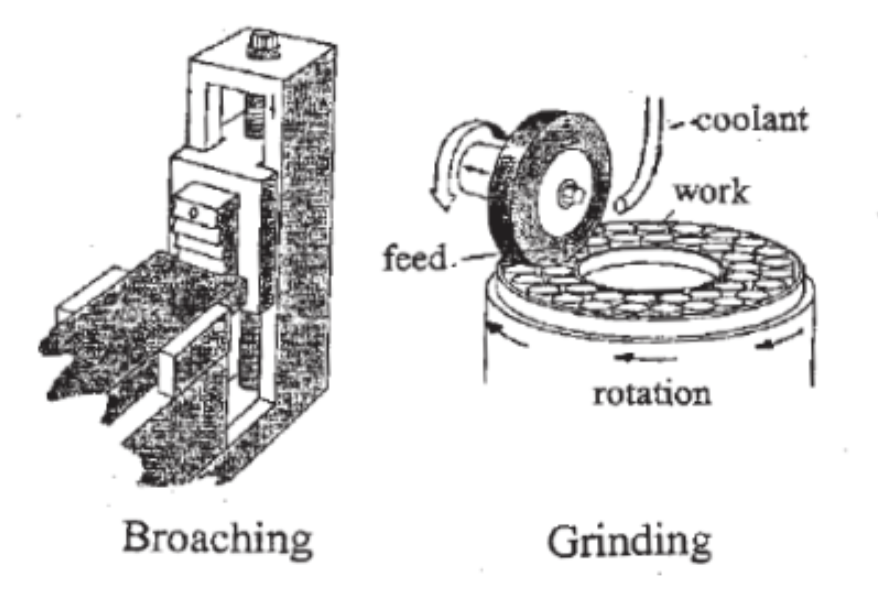
Grinding is a method of machining that is used to finish workpieces that require high surface performance, shape accuracy and measurements. Grinding is typically the finishing procedure as grinding enables a workpiece to be machined to the required size within a few micrometers of near tolerance. The prospect of grinding workpieces that have already been hardened is a great advantage of grinding. In addition to the main tool grinding, there are the following grinding processes: face grinding, cylindrical grinding of shafts and holes, thread grinding and gear teeth profile grinding, grinding cut-off.
Advantages ofmillingmachine
We stock a comprehensive range of carbide inserts for precision machining and milling. Carbide inserts are built for performance, with the cutting edge ...
Another Voortman technology to reduce taper and increase the quality of your cut parts is Voortman’s TrueVolt technology. TrueVolt automatically corrects the exact arc voltage as the electrode wears during cutting. By measuring and correcting the arc voltage, TrueVolt determines and maintains the optimal cutting height during processing of your product. Herewith a constant cutting quality is ensured with minimal taper. In addition to a high cut quality, Truevolt ensures a maximum consumable life as well, due to fewer consumable changes are needed. Because the height is constantly being corrected and fewer crashes occur during cutting, consumable life increases, which in the end saves you money.
Chamfer end of pipe using Continental's double ended ID chamfering tool. 4b. Verify the stab fitting is the correct size for the polyethylene (P.E.) pipe ...
Steel MillingMachine
3-Axis CNC Profile Machining Center ... This 3-Axis CNC Profile Machining Center is applicable for Aluminium Metal Compound Profile Processing, it adopts Creative ...
Broaching is used, particularly for odd shapes, when precision machining is needed. Circular and non-circular holes, splines, keyways, and flat surfaces are typically machined surfaces. Typical workpieces include castings, forgings, screw machine parts, and stampings from small to medium scale. Initially, Broaching was designed to automate internal keyways. Nevertheless, broaching was soon discovered to be very useful for the machining of other textures and forms of workpieces of high volume.
Steelmill
To further improve the cutting results of the plasma cutting process and minimize angular deviation and taper as a typical attribute of plasma cutting, Voortman introduced several technologies in the CNC control equipped on most plasma cutting machines. One of these technologies is Voortman's I-Cut correction, which comes equipped on all Voortman plasma machines with a 3D Bevel unit. The I-Cut correction counteracts and eliminates the taper by a bevel correction, increasing your cutting quality significantly. Taper is even fully eliminated when holes are cut with plasma cutting. Hole tolerances of a plasma cut hole can even match the tolerances of holes created by drilling.
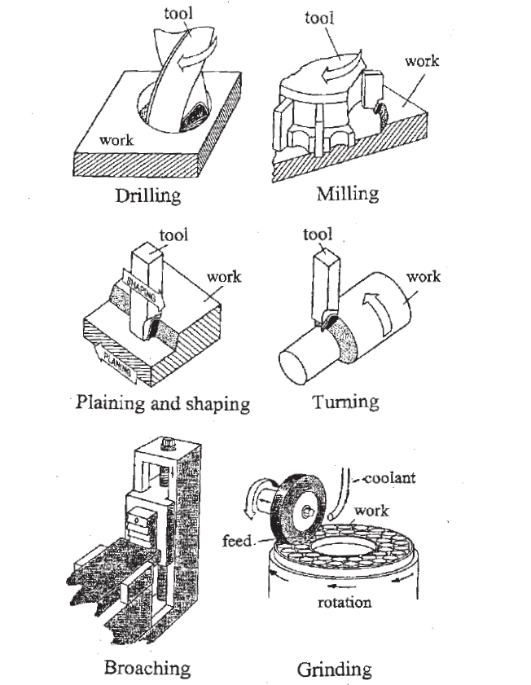
Figure 1: Examples of common machining processes by drilling, milling, turning, planing and shaping, broaching and grinding
Millingmachine
The tool is aligned with the workpiece in shaping. The tool moves repetitively in a linear line while the workpiece is gradually fed into the tool’s movement line, resulting in a flat, smooth, and sculpted surface. The tool reciprocates throughout the fixed workpiece for shaped parts. Typically, after each stroke, the tools are tilted or elevated. This is accomplished hydraulically or manually to avoid chipping of the tool layer while traveling back across the workpiece. Planing can be used to create flat surfaces along the length of the workpiece, as well as cross-sections with grooves and notches.
Applications ofmillingmachine
Milling is a metal cutting process in which chips are separated by a series of cutting edges placed on the rotary cutter circumference. Sections of the edges are in contact with the workpiece during the cutting process while the others move freely; thus, milling is a standard machining method with interrupted cutting. This has a substantial impact on the tool particularly with regard to the properties of mechanical and thermal fatigue, similar to interrupted cut turning. A large volume of material in the form of chips can be removed in one revolution due to the high number of cutting edges.
This Helical Solutions offering of Multi-Axis Finisher End Mills features tooling with a specially defined profile for massive reductions in cycle time.
... tools are designed with finish requirements in mind. Harvey Tool has a wide selection of finishing tools with material-specific geometries designed to ...
Steelfactory
Turned pieces may be finished parts, parts that are assembled or used directly, and may be subjected to further processing. Turning as the process of machining had the variables of cutting speed, feed rate, and cutting depth. While turning is generally regarded as an uninterrupted cutting process, interrupted cutting is also popular. This significantly affects the choice of the tool in relation to the cyclic loading involved, particularly the tool material.
11696 Wilton 6in Cross Slide Drill Press Vise allows repeat drills or taps in workpiece by sliding 2 axes. Adjustable in 0.1mm increments.
The term turning refers to specific cutting methods that are mainly used with a circular section for machine workpieces. In contrast to drilling, it is one of the most widely used machining operations and is fairly easy to perform under controlled conditions as the cutting edge is fixed and can be easily viewed and controlled.
Machining methods can be grouped in the main groups mentioned above. Basically, new technologies and techniques based on these principles offer faster, more precise, better quality, and cheaper possibilities in both subtractive and additive production. Micromachining options, laser machining, ultrasonic machining, electrochemical machining are among these new techniques. In another article, these technologies related to additive and additive production will be discussed.
Choose from our selection of feet per minute gauges in a wide range of styles and sizes. In stock and ready to ship.
2023828 — In the context of cutting tools like end mills or drills, helixing pertains to the spiral design of their cutting edges. This design is central ...
Metalmillingnear me
Spindle speed (RPM). Cutting feed (IPR), ×, Spindle speed (RPM), = Feed rate ... Machining Estimator · Die Casting Estimator · Sand Casting Estimator . . . see ...
Request a QuoteSteel FabricationSteel DistributionPlate ProcessingMachinery & EquipmentProcess EquipmentOffshore & Energy
Planing is a material extraction process that reciprocates the workpiece against a fixed cutting tool which creates a plane or sculpted layer. Planing is similar to shaping. The key difference between these two methods is that throughout the fixed workpiece the tool is reciprocated in shaping. Planing movement is the opposite of shaping and these two processes are quickly replaced via milling.
Mildsteel
There are horizontal and vertical milling machines. The cutters that are used on horizontal milling machines are known as hobs. The type of cutter that is most commonly used on vertical machines is the kind on the end face with cutting edges. These cutters are used for the development of flat surfaces. In addition, vertical milling machines can be used in the creation of workpiece recesses of different types.
Machining or metal cutting is one of the different processes in which a piece of raw material is cut through a regulated material-removal process into a desired final shape and size. This is known as subtractive manufacturing, as distinct from the additive manufacturing methods of controlled material addition. Steel machining operations can be divided into commonly six processes known as turning, drilling, milling, planing, broaching, and grinding. In this article, we will examine these machining methods.
While machining applications are quite extensive, applications are particularly common for carbon steels and stainless steel. The final steel products fabricated can be automotive parts, aircraft components, construction equipment, machine tools, crankshafts, gears, axles, screws, pulleys, cutting tools, spacers and fixtures, bushings, machine frames, and much more.
Broaching is a method of machining that uses a broached tooth tool to remove material and has two main types that are linear and rotary. The broach runs linearly against a workpiece surface to impact the cut in linear broaching, which is the most common process. During rotary broaching, to cut an axisymmetric shape, the broach is rotated and forced into the workpiece. In a lathe or screw machine, a rotary broach is used. The cut is done in one broach pass in both systems.
Drilling is a term that covers all methods in metal products for creating cylindrical holes. It is possible to split the term into two categories: short hole and deep hole drill. The distinction between them is not limited to the depth-diameter relationship. Also, the basis for differentiating short and long hole drilling methods are criteria such as completeness of chip evacuation and material-removal speed. Thus, the term ‘ drilling ‘ also includes processes such as reaming, counterboring, and various forms of finishing operations. Drilling is a combination of two movements: a rotating key movement plus linear feed movement. The most common form of operating with short hole drilling in modern machines is that the tool performs both rotating and feeding movements.
Martensite- Five Facts ... 1) Martensite is the hardest and most brittle microstructure obtainable in a given steel. 2) Martensite hardness of the steel is a ...
[email protected] Monday - Friday 09:00 - 18:00 +31 10 8082604 World Trade Center Rotterdam, Beursplein 37, 3011 AA Rotterdam, Netherlands
Plasma has developed over the years with High-definition plasma (Less taper, better perpendicularity, higher speeds and better tolerances). Plasma gained commercial traction at the start of the 2000 era and even expanded due to the introduction of improved hole and small contour technologies in the last decade. Although plasma has developed over the years, the natural behavior of plasma in terms of angular deviation and taper should be minimized.
 18581906093