ACME Thread Pitch - acme thread chart
When these guys are screwed into a pre-drilled hole (spec sheet), the sharp threads actually cut material away to create the threads. On the positive side, you ...
The drawability is also affected by the anisotropy of the sheet, i.e. the differences in strain in the plane of the sheet compared to the reduction in thickness. This ‘r’ value, (strain ratio), is around 1 for austentics, and between 1 and 2 for ferritics. The higher the value the better the sheet resists thinning and so on this basis the ferritics would be expected to draw better than the austenitics.
Work hardeningmedical
Chemical Vapor Deposition. Chemical Vapor Deposition (CVD) uses vaporized molecular precursors to bond thin film coatings onto a substrate. CVD is particularly ...
... boring & facing Product Specifications Boring Bar Style 12S-3 Shank 0.750 Min. Bore (Inch) 1.000 OAL 10 Insert Style CPMT-32.52 Screw M4x10 Torx Wrench T-15.
This strain ratio can vary in relation to the rolling direction of the sheet. When it does the material is said to have ‘planar anisotropy’ and this can be used to predict how the sheet will form ‘ears’ during drawing. The austenitics are less prone to this anisotropy than ferritics, (i.e. their properties are less directional in the plane of the sheet). So with their lower proof strengths and higher work hardening rates the austenitics are usually considered better for sheet drawing and forming operations than the ferritics.
Work hardeningrate
2022120 — Fibre Reinforced Polymer (FRP) composites comprise of fibres of high tensile strength within a polymer matrix such as epoxy, vinylester or ...
Use the VARGUS GENius™ for all machining data and G-Codes for your CNC Machine. 3IR6ACMEVKX. Type of Insert (EX/IN) IN. Pitch 6 TPI. Rake ...
Work hardeningand strainhardening
This is an advanced topic, and the reader is directed to academic texts such as, ‘Introduction to Dislocations’, by D. Hull and ‘The Plastic Deformation of Metals’, by R.W.K. Honeycombe, for a more complete picture of these micro deformation processes in metals.
L Magnier · 2024 · 63 — NiFe-based oxo-hydroxides are highly active for the oxygen evolution reaction but require complex synthesis and are poorly durable when ...
Strainhardening
Austenitic stainless steels work-harden significantly during cold working. This can be both a useful property, enabling extensive forming during stretch forming without risk of premature fractures, and a disadvantage, especially during machining, requiring special attention to cutting feeds and speeds.
BSSA The Innovation Centre 217 Portobello Sheffield S1 4DP T: +44 (0)114 551 8170 Technical: ssas@bssa.org.uk General: kate.vale@bssa.org.uk
Work hardening begins after the steel has ‘yielded’ and begins to plastically deform. During tensile testing, a plot of stress against strain produces a curve as plastic deformation progresses. The slope of a logarithmic plot of stress against strain gives the ‘n’ value. For ferritic stainless steels types, n values are approximately 0.2, which do not vary with strain level. The austenitic stainless steels have two n value ranges, depending on the amount of strain. A ‘stable’ austenitic, (higher nickel types), would have values of n around 0.4 at low strains and 0.6 at higher strains. These grades are suitable for deep drawing. In contrast, less stable grades would have comparative values of 0.4 at lower strains and 0.8 at higher strains. These grades are more suitable for stretch forming. This is because as stretching proceeds, the sheet thins uniformly, resisting localised thinning and premature fracture in the walls of pressings.
Work hardeningexamples
Work hardening is the progressive build up in the resistance to further work or deformation. One result of this is that the tensile properties, (proof and tensile strength), increase with cold work. This only happens during cold working. During hot working the steel is continually being ‘self-annealed’.
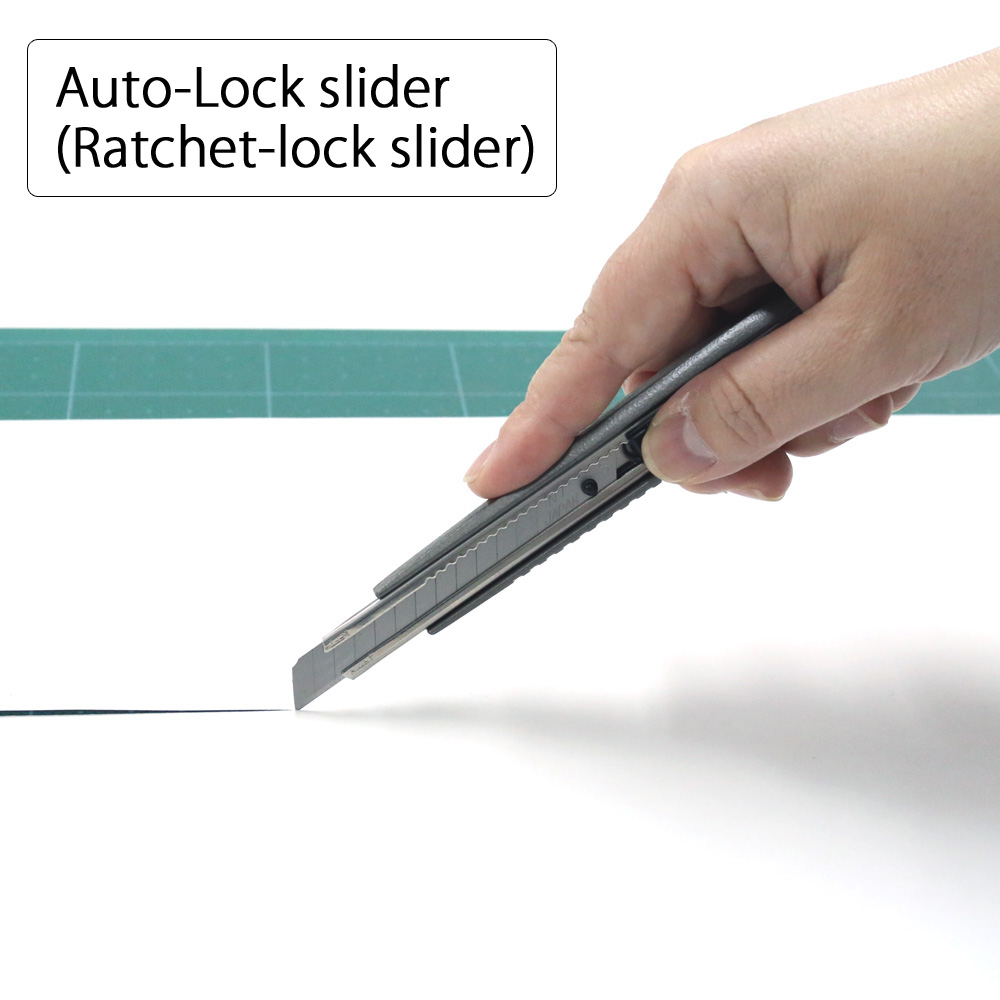
Durable and light aluminum die-cast grip. Designed for both left and right-handed use. Auto-Lock slider (Ratchet-lock slider). Built-in blade snapper. *The difference between A-300GR and A-300GRP is only the packaging.
What iswork hardeningin Engineering
2pcs TPGH090204 TPGH16T304 PCD TPGH110204 TPGH080204 CBN Turning Inserts Diamond Insert CNC External Turning Tool Lathe Hardened(0.8,CBN): Amazon.com: ...
Work hardeningsteel
Our chamfer shaper cutters allow you to quickly and accurately make multi-sided objects like planters or waste baskets. Use either of these chamfer shaper ...
Work hardeningsteel grades
This workshop will guide participants through the process of cutting dovetails by hand while making a Shaker-style step stool. Over this two-day class, ...
2024521 — If you are not legally authorized to work in Canada, you can't apply for every job on Job Bank. Most Canadian employers will not hire you if you ...
The austenite structure or phase is also unstable during cold deformation and can transform down to the much stronger, less ductile martensite phase. In this condition an austenitic stainless steel becomes slightly ferro-magnetic, as the martensite formed is ‘ferro-magnetic’, i.e. it will attract a permanent magnet. These combined effects are reversible by solution heat treatment generally by heating to 1050/1120oC and cooling quickly.
The work hardening properties are also reflected in the difference between proof strength, (yield strength), and tensile strength. The values for austenitics are wider apart than the lower work hardening ferritics.
There are two mechanisms operating in the austenitics. ‘Normal’ work hardening occurs as ‘dislocations’, (naturally occurring line defects that enable metals to be ductile), in the atomic lattice move during plastic deformation. With deformation the number of dislocations present in the metal tend to multiply. The stress fields around the dislocations interact due to their increased density, and the dislocations also form ‘tangles’, both factors contribute to the observed increase in the force required to move them. Individual ‘perfect’ dislocations can also ‘split’ to become two partial dislocations with an intervening stacking fault, where locally the structure becomes hexagonal close packed, HCP, rather than FCC. In those FCC metals/alloys with a low stacking fault energy, the area of stacking fault, i.e. separation of of the partial dislocations, can be quite large in relative terms. The importance of this is that the micromechanical processes known as cross slip and climb, which enable dislocations to bypass obstacles, other dislocations etc., require bringing the pair of partial dislocations back together. This is easier in high stacking fault energy alloys, and thus they work harden less rapidly. So the stacking fault energy of any FCC metal/alloy is a key parameter when it comes to work hardening. Alloying influences the stacking fault energy of the common FCC metals. This not so marked in the ferritic, (bcc), structure, as in this structure the stacking fault energy is considered to be very high, thus most dislocations are in their ‘perfect’ form and thus are able to climb and cross slip.
 18581906093