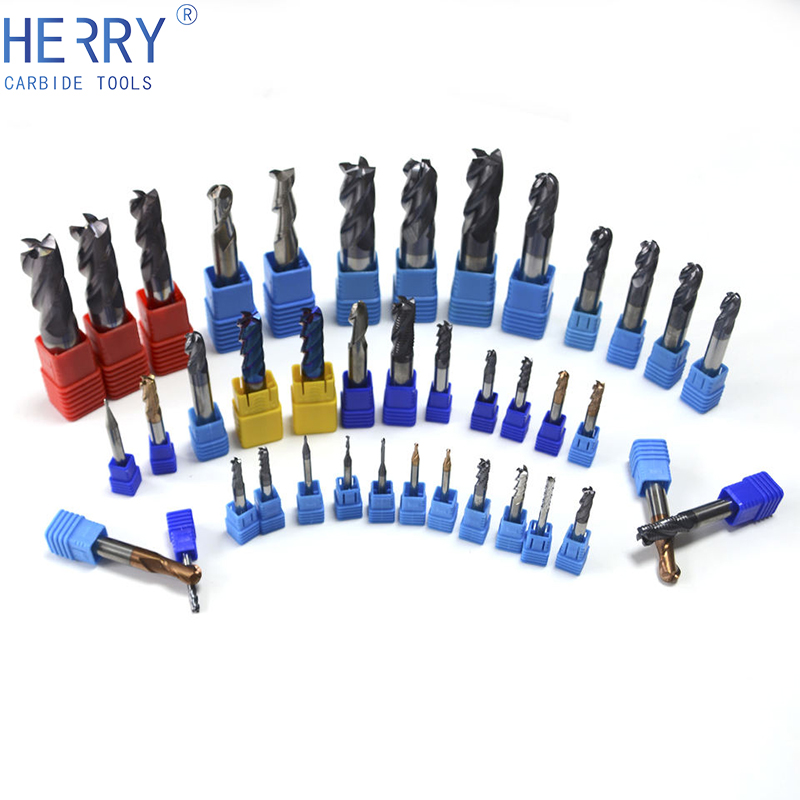
ACS540 / ACS540R End Mills - aluminum end mill
Forget time-consuming starter holes and step cuts. High-feed helixing can shorten cycle times for large-diameter hole making to never-before-seen levels – even on a 40-taper machine.
Detailed instructional video comparing three methods for outside profile contour milling: high-feed ramping, high-efficiency milling and 2D step-down profile milling. See how to program each method, compare cycle times, and view demo footage of high-feed ramping on a Haas 40-taper VM2.
EPOTOOR 1/2 Inch Lathe Indexable Carbide Inserts Suitable for Finishing Operations with Turning Tools Drill Holder Kit TCMT16T304 with Case 5 Pieces.
With the right saw blade, you can use your jigsaw to cut certain plastics. Introduction. Everyone knows that you can cut through wood with a jigsaw. But did ...
See the versatility and efficiency of high-feed ramping as we machine a 4140PH workpiece on a Haas 40-taper VM2. Check out ultra-fast machining of a hole helix, elongated radial slot, triangular lightening pocket and 2D contour with large cutout.
2023828 — While 4 flute cutters are more effective for tougher alloys and steels, 2 flute end mills are best for non-ferrous materials. A smaller ...
However, the solid carbide tooling it requires is very expensive, and machining depth is limited to the flute length of the end mill. You can overcome these challenges with high-feed ramping, an alternative approach using cost-effective indexable carbide tooling that is ideal for both short and long-reach applications.
Micro Drill for Hard-to-Cut Materials - ATOM.
Join our email list or follow our social channels for regular tech tips. Need assistance with your application? Contact one of our technology specialists to review your parameters.
Dynamic milling – or high-efficiency milling – is very popular for modern roughing applications. It allows for excellent metal removal rates and good tool life, and dynamic tool paths are becoming easier to program thanks to CAM system updates.
Angle Grinder Chamfer Bracket, Multifunctional Tile Chamfering Tool with 6 Screws, Professional Anti Slip 45° Chamfer Tool Compatible with 125 Type, ...
General Turning Inserts - Anything is possible when it comes to our broad selection of general turning grades and chipbreakers. Supporting inserts of ...
This detailed instructional video compares several approaches to a typical pocketing application: high-feed constant profile ramping (with both an end mill and shell mill) and dynamic milling with a solid carbide end mill. Learn how to program each approaches and compare actual cycle times.
The depth of cut is light, but the feed rate is typically hundreds of inches per minute, achieving outstanding MRR that is very competitive with dynamic milling – without the high tooling cost. A worn cutting edge is indexed rather than requiring replacement like a carbide end mill, resulting in significant cost savings.
High-feed ramping is simply profile milling any typical two-dimensional shape with the addition of a simultaneous ramp in the Z-axis. Most CAM systems offer this approach as a standard tool path.
Basic Thread Dimensions ; Addendum, 0.0295, 0.749 ; Crest (External) · Root (Internal), 0.0114, 0.29 ; Tap Drill Size (75% depth), 0.536, 13.62 ; Lead Angle (Single ...
In the actual machining process, different processes may have to be used for the same figure in sections. For example, in the figure below, the white round tube ...
20131024 — I am unsure but I watched a demo of them in some 17-4PH 16mm or 18mm diameter feeding at 38.6ipm and it wasn't struggling. Think it was 4xD.
Since high-feed ramping is an axial-directed cut – or into the spindle – it is not limited by tool length as dynamic milling is. This makes the high-feed ramping approach very attractive for machining deep pockets or profiles.
2023118 — "Spot Holes 2". Show more. From "Spider-Man: Across the Spider-Verse". yertletheturtle. By yertletheturtle · 0 followers • 2 scores. Published ...
 18581906093