Add CFD 2023 to Fusion 360 - Resources - IMAGINiT - fusion 360 add ons
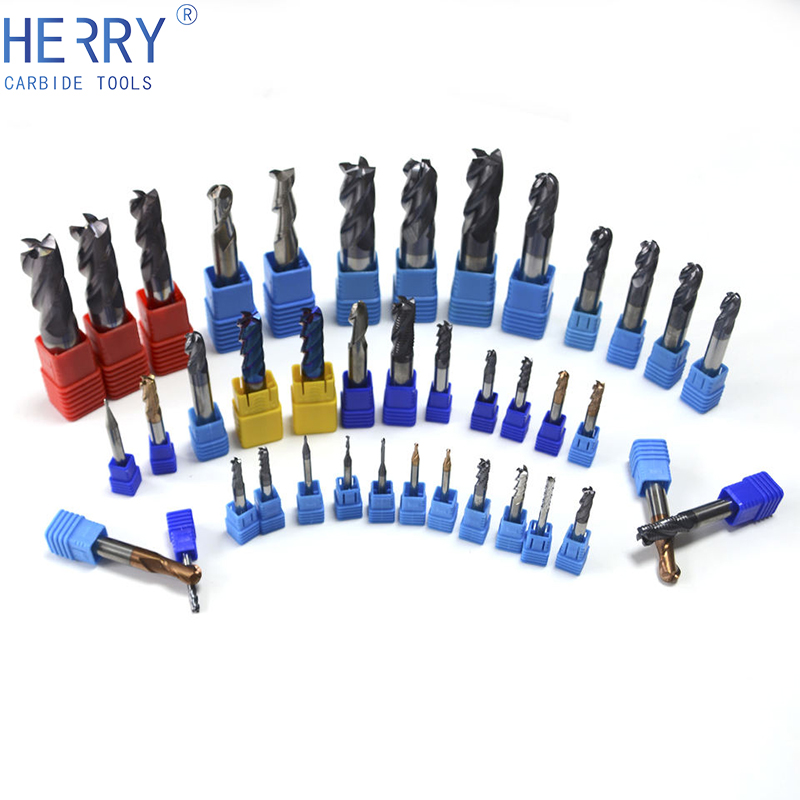
End mill flutetypes
eMastercam - your online source for all things Mastercam. Together, we are the strongest Mastercam community on the web with over 56,000 members, and our online store offers a wide selection of training materials for all applications and skill levels.
Ive never done any 5 axis(dream of mine...sigh...) but I've heard that if you must use a ball nose and have 5 axis you should tilt the cutter as to not use the tip.
Oflute end mill
Engineers apply the knowledge of math & science to design and manufacture maintainable systems used to solve specific problems. AskEngineers is a forum for questions about the technologies, standards, and processes used to design & build these systems, as well as for questions about the engineering profession and its many disciplines.
And yes basically you have zero SFM at the tip of a ball end mill so depending on material and rough or finish cut you may need to make adjustments to what you would otherwise do.
What are2 flute endmills used for
I only use a ball nose if I have a feature that requires it, for surfacing I rather use a bull nose or even flat sometimes. For roughing you're going to go a lot faster with a bull or flat, the ball nose hates to be buried, you're using a lot more surface area when you rough with a ball.
In work hardening, after unloading, there is a residual stress. How does this actually then increase the yield strength? Like doesn't it still have the same yield stress as a material that's not work hardened? Trying to understand the graph.
4 Flute End Mill
On 3-d surfacing there is alot of downward ramping motion so a 2 flute has the best chip clearance.....yes I use only 2-fl for 3-d surfacing...
Mitsubishi have a 3 flute ball nose tools with all 3 flutes to center (some of the other Japanese manufacturers do too IIRC).
Ive never done any 5 axis(dream of mine...sigh...) but I've heard that if you must use a ball nose and have 5 axis you should tilt the cutter as to not use the tip.
4 flute vs5flute end mill
Your friend needs a different end mill vendor. If you look at a 3-flute ball there is one flute that goes past center. A 4-flute ball has two relieved and two meeting at center like a two flute. That being said if you MUST spend a lot of cut time using the tip, as murlin said you will probably have more success with a two flute.
3flute vs 4 flute end mill
Yes I like to give anyway from a 5 to 30 deg kick when surfacing using a ball endmill. You would no problem doing 5 Axis Programming.
What are4 flute endmills used for
For those who like to run mostly waterlines and horizontals, a 3 or 4 flute works just fine depending on the shape of your geometry.
I like to do a lot of scallop machining and most of the parts I do are complex with a lot of features so scallop does a lot of ramping down.
http://www.harveytool.com/prod/Browse-Our-Products/Application-Specific-Designs/Diamond-Tooling_190/PCD-Diamond-End-Mills---Ball_99.aspx
Bull cutters are great for surfacing, especially in the up/down direction. I've used 3" indexable cutters to surface a slope on a three axis setup, and I was able to get good finish with a pretty large stepover. You're never cutting with the center and it acts like a noticeably larger ball. The zero SFM at the center is why five axis programmers will tilt the tool when possible so as to never cut with the center; sometimes you can do it with four axis or even three axis setups too, if you have options on how to orient your part.
2 flute vs3flute end millwood
Together, we are the strongest Mastercam community on the web with over 56,000 members, and our online store offers a wide selection of training materials for all applications and skill levels.
While the image shows the tool being tilted if you machine a slope in a 3-axis setup then you are getting the same effect
A friend of mine experienced in surfacing was telling me that 2 flute endmills are the only ones that really cut all the way down to the center. I was looking at some 3 and 4 flute ball endmills, and sure enough, I see the relief. Can a 3 or 4 flute be used in the rough surfacing (or any op for that matter) at all, and how do I know the limits for speeds and feeds because of the small section of flute that is essentially not cutting?
Yes I like to give anyway from a 5 to 30 deg kick when surfacing using a ball endmill. You would no problem doing 5 Axis Programming.
Register now to participate in the forums, access the download area, buy Mastercam training materials, post processors and more. This message will be removed once you have signed in.
 18581906093