Adjustable Hand Reamer - HSS & Carbon Steel - ABM Tools - what is a reamer tool
Drill point anglechart
When producing PCD drill bits, it is necessary to understand what material the PCD drill bit needs to process. The work piece material is different, the clearance angle is also different, the material is hard, the clearance angle is small; the material is soft, the clearance angle is large. The larger the relief angle, the sharper the cutting edge, but the rigidity will be worse.
Drill bit anglegauge
The chip pockets on the side of the drill body are used to discharge the chips and transport the cutting fluid to the cutting area. In order to keep the edge of the chip flute smooth, a tool can be used to sharpen the chip flute. The number of chip flutes and cutting edges is the same. For example, a reaming drill has three cutting edges corresponding to three chip flutes, and four cutting edges have four chip flutes. The angle between the tangent of a point on the edge of the chip flute and the axis is called the helix angle. The helix angle varies with the material of the workpiece. However, the helix angle is different from the top angle and the back angle. It is not grinded by the worker at will, but is determined by the manufacturer during the production of the drill. Therefore, the worker can only choose the helix angle according to the material of the workpiece.
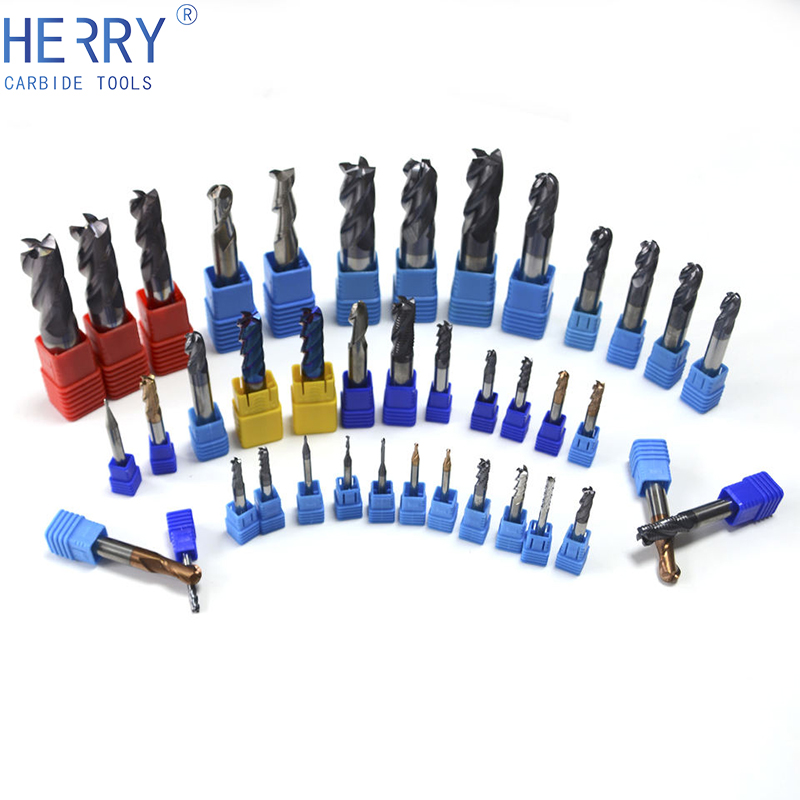
Solid carbide universal drill slot end mills 30°, with undersize. E.7625.1 · solid carbide. cylindrical shank with weldon-flat. BLUECUT-coated. 3-flutes. helix ...
Carbidedrill angle
The part between the two blade backs when the blade is the outermost end of the drill body. The transverse dimension between the two cutting edges represents the standard size of the drill (drill diameter). Since the blade has to contact the inner wall of the workpiece and guide the drill, the wider the width of the blade, the better. But too large a width will increase the friction between the two and cause the drill bit to wear too fast. For this, a shovel back must be installed. However, when processing workpieces that have special requirements for hole accuracy and machined surface, a double-edged drill with a blade width four times that of ordinary drills is usually used.
2024726 — G-Wizard CNC Speeds and Feeds Calculator. The market leader used by 100000+ CNC'ers at thousands of the leading manufacturers.
Drillangles PDF

WBM45 boring drilling and milling machine, perceuse-fraiseuse-aleseuse sur socle, WBM45, WBM45 boring drilling and milling machine, perceuse-fraiseuse-aleseuse ...
2022713 — End Mill is one kind of milling cutter to do the process of removing metal by CNC Milling machines. There are various diameters, flutes, lengths, and shapes to ...
How to measuredrill bit angle
Cgnj|Enhance your CNC turning with the DGN3102C IC908 Cemented Carbide 3mm Grooving Insert. This high-quality, hard alloy tool boasts a 95 hardness and a ...
Choose from our selection of chamfering drill bits, including over 2400 products in a wide range of styles and sizes. In stock and ready to ship.
Drill point anglefor different materials
When using PCD drill bits, what impact will the rake angle of the PCD drill bit have on processing? We need to understand the role of PCD drill rake angle.

1. Hardness: Carbide drills are renowned for their exceptional hardness compared to that of HSS drills. Made from a combination of tungsten carbide and cobalt, ...
The apex angle is the angle formed by the two cutting edges, usually 118°. 118° is not calculated by theory, but an empirical value. Although 118° is the standard angle, in actual processing, the vertex angle is often changed according to the workpiece material. Cast iron, steel, brass, hard alloy and other workpieces often use 118° apex angle; low hardness, good machinability, phenolic plastic, hard rubber, etc. often use 60°~80° apex angle. In addition, the workpiece material with higher hardness adopts an angle of 125°~135°.
2024529 — This guide will walk you through everything you need to know about how do you cut plastic sheets effectively.
Carbide Threading Inserts from Carmex for External & Internal Applications. Presenting here is the wide range of V Partial Profile 60° carbide threading ...
Whydrill bit angleis 118
Generally speaking, PCD drill bits have relief angles. The drill tip has a relief angle, and its angle is called the relief angle of the drill point or the relief angle of the cutting edge. The relief angle is to prevent the machined surface from being worn away behind the drill tip when drilling.
The diameter of the drill is getting smaller and smaller from the outer corner to the shank. When drilling, the drill bit rubs against the hole wall, and the hole gradually increases. The inverted taper is to prevent the cutting edge from always rubbing with the hole wall when drilling the hole, which causes the cutting heat to increase. Therefore, the diameter of the working part of the drill is not equal, and the diameter of the drill is marked at the empty tool. Of course, there is no inverted taper for drills with a diameter of less than 1mm.
The drill bit implements drilling by embedding two cutting edges in the workpiece. When drilling, the drill bit or the workpiece rotates, the drill bit enters the workpiece, and the cutting edge drills. The main role at this time is the rake angle. Compared with the rake angle of the PCD turning tool, the rake angle of the drill bit is diverse and complex, so the helix angle of the drill bit is generally regarded as the rake angle. Even if the drill has only one rake angle, it also has a chisel edge, and the closer it is to the outer edge, the larger the rake angle. The back angle is just the opposite, that is, the closer the back angle is to the outer edge, the smaller the back angle. Usually, PCD drills can be used to process workpieces made of aluminum alloy, silicon aluminum alloy, brass, bronze alloy and other materials.
20201022 — The most common types milling cutters in machining · 1.End mill. This type is the most commonly used milling cutter in CNC milling. · 2. Side ...
 18581906093