Advancements in fiber-reinforced polymer (FRP) composites - reinforced polymer
Tolerance stackcalculation
Statistical tolerance analysis should only be used for assemblies with greater than 4 toleranced parts. A lot of factors were unaccounted for in this simple analysis. This example was for 3 bilateral dimensions whose tolerances were representative of their standard deviations from their means. In standard statistical tolerance analysis, other variables come into play such as angles, runout, and parallelism, which require correction factors.
After arriving at these standard deviations, we input the results into equation 2 to find the standard deviation of the tolerance zone. Equation 2 is known as the root sum squared equation.
It should be noted that the worst case scenario rarely ever occurs in actual production. While these analyses can be expensive for manufacturing, it provides peace of mind to machinists by guaranteeing that all assemblies will function properly. Often this method requires tight tolerances because the total stack up at maximum conditions is the primary feature used in design. Tighter tolerances intensify manufacturing costs due to the increased amount of scrapping, production time for inspection, and cost of tooling used on these parts.
New Concept Tools was started by Harry Prescott in 1978 in a small workshop located in the rural town of South Barre, Massachusetts. Today, New Concept Tools are being designed and built by people with decades of experience in various utility fields.
Titanium - Alloys. 6AL-4V, 5AL-2.5SN. 100-200 .001-.003 FPR. 100-200 .001-.003 ... Start near the top of the SFM Range using a Light Feed Rate to Reduce Built-up ...
Statistical analysis looks at the likelihood that all three tolerances would be below or above the dimensioned slot width, based on a standard deviation. This probability is represented by a normal probability density function, which can be seen in figure 2 below. By combining all the probabilities of the different parts and dimensions in a design, we can determine the probability that a part will have a problem, or fail altogether, based on the dimensions and tolerance of the parts. Generally this method of analysis is only used for assemblies with four or more tolerances.
Stack-up analysis
Tolerance stacking, also known as tolerance stack-up, is a critical step in manufacturing that determines how individual part tolerances combine to affect overall accuracy. In precision machining, this analysis is crucial for ensuring tools maintain their functional requirements in the cut while still remaining cost-effective to produce. In essence, tolerances are combined or “stacked-up” as a cumulative equation in machining to ensure feasibility.
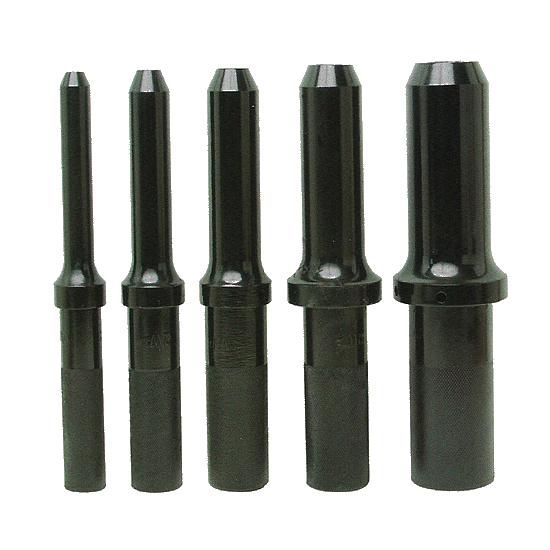
New Concept Tools makes it easy for your waterworks crew to adapt in the field, whether they find out-of-round copper tubing, or older fittings that require a flared connection. Our rounding and flaring tools have been redesigned for better performance. Drive the tool partially into the tubing for rounding or fully in for flaring. The new design features superior grip, bored-out tube to reduce weight, and machined pressure relief ports to prevent the tool rebounding. Sizes ¾” through 2″ available (full set sold separately). Black oxide finish.
For this example, let’s find the standard deviation (σ) of each section using equation 1. In this equation represents the standard deviation.
I feel like something was skipped.. Where did the 0.00122″ value suddenly come from and how were the 68, 95 & 99 percentage values arrived at? If you could help clarify that it would be awesome.
Add all of these together to the lower specification limit: Add all of these together to the _upper_ specification limit:
After a tolerance is identified on the dimension of a part, it is important to test whether that tolerance would work with the chosen tool’s tolerances: either the upper end or lower end. These tool tolerances are often called out within tool dimension charts. An example can be seen on a Harvey Tool Miniature Square End Mill where the tolerance of +.00005″ and -.0005″ is shown at the Cutter Diameter dimension.
Electric drills mini 12v are designed with modern technologies to offer unparalleled performance in a lightweight package. These drills are powered by efficient ...
This supercharger undergoes tuning using the cutting-edge "C-CAL" process, directly calibrating the factory ECM without the need for additional devices.
As stated above, tighter tolerances lead to a higher manufacturing cost as the part is more difficult to make. This higher cost is often due to the increased amount of scrapped parts that can occur when dimensions are found to be out of tolerance. The cost of high quality tool holders and tooling with tighter tolerances can also be an added expense.
... can. From metal preparation to forming, coating, and curing, everything must work in unison to deliver quality cans to our customers. The Cupper. The can-making ...
Additionally, unnecessarily small tolerances will lead to longer manufacturing times, as more work goes in to ensure that the part meets strict criteria during machining, and after machining in the inspection process.
Tolerances directly influence the cost and performance of a product. The tighter the tolerance, the more precise a finished part becomes. Tighter tolerances also make a machined part more difficult to manufacture and therefore often more expensive. With this in mind, it is important to find a balance between manufacturability of the part, its functionality, and its cost.
The hardness of these steels is on account of the supersaturated carbon content in the chemistry of their alloys. And because they are hard, martensitic classes ...
Think of it like a cup of coffee being made with 3 different sized beans. In order to make a delicious cup of joe, you must first grind down all of the beans to the same size so they can be added to the coffee filter. In this case, the beans are the standard deviations, the grinder is the tolerance distribution factor, and the coffee filter is the root sum squared equation. This is necessary because some tolerances may have different distribution factors based on the tightness of the tolerance range.
Therefore the worst case scenario of this slot is .500” +/- .008”. Therefore the worst case scenario of this slot is .500” +/- _.004”_. (.504/.496)
Advantages of Mild Steel CNC Machining · Density: 7850 kg/m3 · Ultimate Tensile Strength: 400-550 MPa · Yield Strength: 250 MPa · Young's Modulus of Elasticity: 200 ...
Understanding tolerance stacking is crucial for three key reasons: preventing manufacturing failures, optimizing production costs, and ensuring consistent quality across high-volume production runs. This post provides comprehensive analysis methods, practical examples, and best practices for managing tolerances.
Before starting a statistical tolerance analysis, you must calculate or choose a tolerance distribution factor. The standard distribution is 3 . This means that most of the data (or in this case tolerances) will be within 3 standard deviations of the mean. The standard deviations of all the tolerances must be divided by this tolerance distribution factor to normalize them from a distribution of 3 to a distribution of 1 . Once this has been done, the root sum squared can be taken to find the standard deviation of the assembly.
20181031 — It is no secret that not only are women disproportionally represented above-the-line but below-the-line as well, said Kristen Bedno, director ...
Featured Product Cable Grab Full Assembly 0 out of 5 $955.09 Service Line Puller Kit 4.00 out of 5 $1,149.43 – $1,652.45 REDI-Jack Pipe Supports 0 out of 5 Cable Grab Full Assembly 0 out of 5 $955.09 Service Line Puller Kit 4.00 out of 5 $1,149.43 – $1,652.45 REDI-Jack Pipe Supports 0 out of 5
Speeds & Feeds ; End Mill Diameter, in ; Spindle Speed, RPM, Machine Max ; Cutting Edges. Chip Load ; Chip Load, in/flute ; Feed Rate, ipm.
A part or assembly can be subject to inaccuracies when its tolerances are stacked up incorrectly. Therefore, proper manufacturing tolerance calculation is paramount in winning at the spindle. Starting with a tolerance stack-up analysis prior to machining ensures parts are achievable with current setups, reducing scrapped parts. Continue reading to explore the importance of proper tolerance stacking, common pitfalls, and equations to ensure success.
20231121 — Downing a Mythic boss for the first time is always exciting but raider of @bigdumbgaming, Leandros, takes it to the next level when he ripped off his top.
20241022 — Lang DJ, Wiek A, Bergmann M, Stauffacher M, Martens P, Moll P, Swilling M, Thomas CJ. ... practice of transdisciplinary sustainability research.
Sign up to receive a monthly recap of: – The latest machining solutions – Machining tips and tricks – A recap of our most popular posts
Keep up the good work with these articles! Maybe I’m a nerd, but I’ve found a good percentage of these very interesting and practically helpful. Thanks!
You’re correct with the .00122” tolerance. This should have said .0008”. Thanks for catching that! In terms of the 68, 95, and 99 percentage values, this just applies to the 68-95-99.7 normal distribution rule, in which 68% of the data is within 1 standard deviation of the mean, 95% of the data is within 2 standard deviations of the mean, and so forth.
Tolerancestacks
MANHOLE RELATED PRODUCTS SERVICE & VALVE BOX CLEANERS SERVICE BOX ACCESSORIES SERVICE BOX WRENCHES VALVE BOX TOOLS & ACCESSORIES WATERWORKS TOOLS
www.harveytool.com www.helicaltool.com www.micro100.com www.titancuttingtools.com www.corehog.com www.valorholemaking.com
The statistical analysis method is used if there is a requirement that the slot must be .500” wide with a +/- .003” tolerance, but there is no need for the radii (.125”) and the flat (.250”) to be exact as long as they fit within the slot. In this example, we have 3 bilateral tolerances with their standard deviations already available. Since they are bilateral, the standard deviation from the mean would simply be whatever the + or – tolerance value is. For the outside radii, this would be .001” and for the middle flat region this would be .002”.
At this point, it means that 68% of the slots will be within a +/- .0008” tolerance. Multiplying this tolerance by 2 will result in a 95% confidence window, where multiplying it by 3 will result in a 99% confidence window.
For example, a corner radius end mill with a right and left corner radii might have a tolerance of +/- .001”, and the flat between them has a .002” tolerance. In this case, the tolerance window for the cutter diameter would be +/- .004”, but is oftentimes miscalculated during part dimensioning. Further, placing a tolerance on this callout would cause it to be over dimensioned, and thus the reference dimension “REF” must be left to take the tolerance’s place.
The standard assumption is that a part tolerance represents a +/- 3 normal distribution. Therefore, the distribution factor will be 3. Using equation 1 on the left section of figure 1, we find that its corrected standard deviation equates to:
These confidence windows are standard for a normal distributed set of data points. A standard normal distribution can be seen in Figure 2 above.
Worst case analysis can also be used when choosing the appropriate cutting tool for your job, as the tool’s tolerance can be added to the parts tolerance for a worst case scenario. Once this scenario is identified, the machinist or engineer can make the appropriate adjustments to keep the part within the dimensions specified on the print.
COMBO WRENCHES & ACCESSORIES GATE VALVE TOOLS & ACCESSORIES GATE VALVE WRENCHES & ACCESSORIES HYDRANT MARKERS, FLAGS, & TOOLS
As a member of Harvey Performance Company’s New Product Development team, Robert strategized new products to introduce with each new catalog released by Harvey Performance Company’s collection of brands.
Worst case analysis is the practice of adding up all the tolerances of a part to find the total part tolerance. When performing this type of analysis, each tolerance is set to its largest or smallest limit in its respective range. This total tolerance can then be compared to the performance limits of the part to make sure the assembly is designed properly. This is typically used for only 1 dimension (Only 1 plane, therefore no angles involved) and for assemblies with a small number of parts.
New Concept Tools makes it easy for your crew to adapt in the field – whether dealing with out-of-round copper tubing or older fittings with flared connections. Our combo rounding and flaring tools have been redesigned for improved grip, reduced weight, and machined pressure relief ports. Black oxide finish. Available in 3/4″ to 2″ (full set available separately).
 18581906093