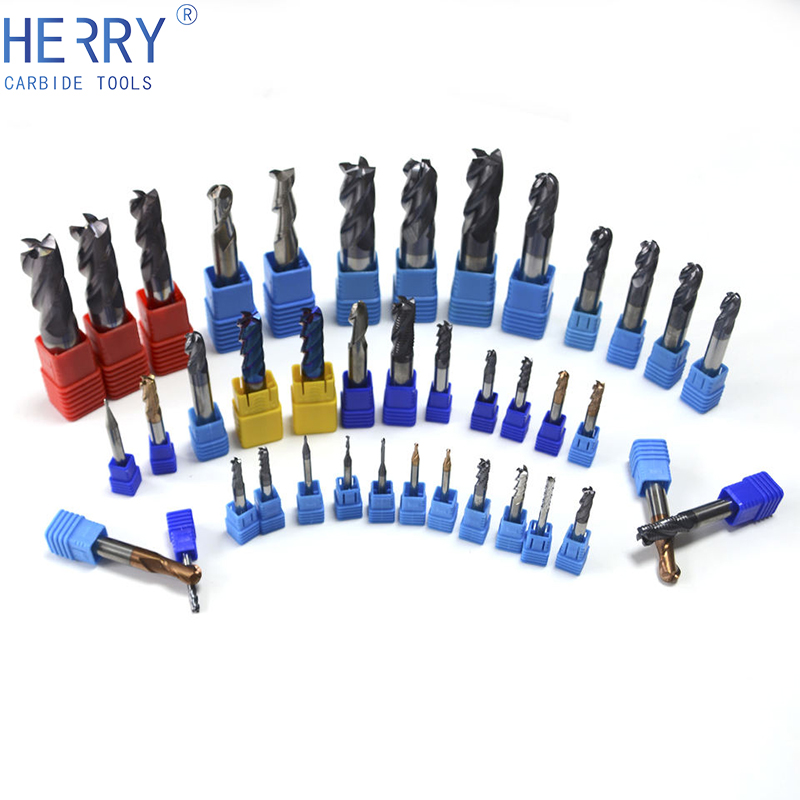
Advice on Cutters for Horizontal Mill - horizontal mill cutters
To suit the varied machining requirements, different types of face milling machines have been designed. Horizontal Face Milling Machines are designed specifically for heavy-duty milling operations. The most important feature of this machine is the ability to remove a large quantity of material in a short time. They perform best to create flat surfaces on large workpieces. Vertical Face Milling Machine, on the other hand, is designed to function both in roughing and finishing operations. They are best suited for applications that require the highest degree of accuracy and finish. These machines are normally used for finishing operations, where the working conditions demand tighter tolerances and finish.
Vibration and Chatter: Vibration and chatter can deteriorate surface finish and tool life. The following parameters should minimise those issues:
In heavy duty face milling, a wide flat cutting tool (the face mill) is used to remove large quantities of material from the work in multiples passes. On each pass, a large slice of material is removed and a suitable shape is generated from the work.
Long reachKeyseatCutters
Face milling is a machining process where the cutting tool’s axis is perpendicular to the surface of the workpiece. It primarily involves removing material from the face of the workpiece to create a flat surface. This process is widely used in manufacturing to achieve high-quality finishes and precise dimensional tolerances.
Carbide TippedKeyseat Cutter
As someone who works in the industry, I’ll give you some practical advice for maintaining spindle speed and feed rate parametres, which is critical for the best output in the process of milling for you. Here goes the breakdown; I hope it helps?
Addressing issues of milling cutter wear and failure is essential to maintaining an efficient, productive machining process. Here is a comprehensive write-up that explains how to deal with it:
Developed to machine large amounts of material in a short period of time, heavy-duty face milling allows machinists to create a large number of flat surfaces faster than using other methods. It is particularly useful for aerospace, automotive and heavy machinery industries where large volumes of metal must be shaped for rapid production of large parts.
If you carefully choose your parameters you might conclude that a milling machine will ‘work’ for you, in the sense of yielding an optimal combination of production capability and cost within the constraints of your financial resources and needs. This is the level of reasoned contemplation we hope to see among new customers, as we’re certain it would bear fruit.
Once you understand these different varieties, you’ll be able to better determine the face mill that works best for you in terms of improved material removal rates, cost savings through insert replacements, or specialised cutting requirements.
By tackling these issues using the right approach, face milling operations can be made more productive, generate better surface quality, and allow tool life to be extended.
MetricKeyseatCutters
Full RadiusKeyseat Cutter
If you incorporate these parameters, and adjust as required according to your material and your cut-off conditions, you’ll do a great job on face milling. Of course, start with default settings and errors, and then fine-tune as you see fit based on real time observation and results.
Here’s an industry insider thing I’d like to explain, from the first-person, about cutting tools and face milling. Let’s try to make it as readable as possible.
Heat Generation: Too much heat can cause tool failure and softer surface finishes. Proper coolant regimens and higher heat-resistant tooling can solve this problem.
In addition to this, further optimisation can be achieved by deploying highly advanced simulation and monitoring tools. These can perform predictive maintenance and adjustments in real time to prevent breakdowns and maintain optimal machining operations throughout. In all, the synergy between theory and practice allows for the optimisation of CNC machining processes and the production of precision mechanical parts with superior quality while also achieving a significant reduction in production costs.
With my years of experience working in your industry, I can address some commonly asked questions about heavy duty face milling:
Heating of Tool or Workpiece: Intense heating will cause damage to the tool and the workpiece, and is, therefore, to be avoided. Keep some points in mind for this purpose.
By understanding these differences, you will be in a better position to assign the right kind of milling in order to achieve your machining requirement. To ensure the optimisation of the process, the consideration of the requirement of material, requirement of the surface finish, depth of cut, position of the tool and the nature of the material will go a long way in making your milling process a lot easier.
GOLDSUPPLIER.COM expands globally, offering quality business opportunities, cost savings, convenience, and expertise in international trade. Trusted and recognized internationally.
The author is an expert in CNC machining. Optimising CNC machining of complex parts with face milling usually involves balancing many parameters to achieve high efficiency and precision. The first step is to identify the material of the workpiece and choose an appropriate cutting tool material and geometry. For example, the relief and lead angles should be selected carefully so that material removal can be carried out safely while maintaining a good surface finish.
Material Hardness: Harder materials mean more wear on your tools and the need for more robust tooling solutions. High-quality carbide inserts with a correct cutting parameters are the solution here.
Face milling utilizes a variety of cutting tools, including carbide inserts, high-speed steel (HSS) cutters, and coated tools. The choice of tool depends on the material being machined, the required surface finish, and the specific milling machine capabilities.
Let me tell you as an expert, face milling is one of the commonest operations in machining. It require some key parameters to be met for the successful machining. Let’s discuss them one after the other for a clear understanding.
In conclustion, wiper inserts will help to finish the surface, increase feed rate, decrease tool wear, ensure consistency, offer a wide range of machining options, and eliminate any additional finishing steps. As such, they are a great option to improve your machining efficiency and quality.
With more than 25 years in the industry, I provided some insights into the several kinds of face milling cutters, their range, difference, and advantages in machining. This will give you a picture about what each kind is best for; enabling you select the appropriate tool to the machining task, and in turn providing optimal results and efficiency.
As an expert in the field, I would like to explain the variations between face milling and peripheral milling, which are the two fundamental machining techniques.
As an expert in the field, I am of the moment to assist you in choosing the most suitable milling machine perfectly meets your needs.When choosing a new milling machine, there are several important parameters you need to take into consideration.
HarveyKeyseat Cutter
Vibration and chatter: these can affect surface finish and tool life. Use vibration-damping tool holders, change cutting speeds, etc to reduce these problems.
When I examine them individually, I can optimise my tool selection for the unique parameters of each face milling operation. This way, I will maximise the accuracy and longevity of my tool, while still producing the fastest, most economical cuts.

As a machining professional, it is very important for you to understand how machining parameters such as cutter angles and cutting speed influence machining process. Your machining process will have a significant influence on its effectiveness and efficiency. Let us examine, in detail, how your machining parameter influence your process.
By having a clear grasp on each of these limitations and employing the appropriate method under the right circumstances, heavy duty face milling can emerge as one of the most effective and efficient treatment in heavy metal removal in a wide range of industrial procedures.
Tolerances: Close tolerances call for delivering consistently correct milling performances. Machines have to be well calibrated, and tools as well as cutting parameters have to be adjusted to the application.
CLICK HERE to download our Speeds and Feeds Chart. Woodruff Keyseat cutters are designed for cutting keyways and keyseats as well as performing general purpose milling operations. Straight tooth cutters produce a better surface finish than staggered tooth. High Speed Steel works great in mild steels, brass, aluminum, bronze, and plastics. Shank tolerance is .500 +.000 -.0005Cutting diameter tolerance is +.010/+.015 (industry standard for all Keyseat cutters)Width tolerance is +.0000 -.0005 (industry standard)
Keyseat cutterwith corner radius
There are so many factors that go into setting up a face milling operation, especially when it comes to selecting the right cutting tool. But there are some relevant parameters that you need to look at. Let me elaborate further.
Carefully and effectively controlling at least some of these parameters can mitigate milling cutter wear and failure, improve tool life and provide better finishes in face milling.
As an expert in the field,I’ll discuss the features and limitations of face milling machine in a simple and easy to understand language. So,lets take a look at the parameters of face milling machine, which are widely used in mass production lines.Here, I will detailedly describe its key parameters.
I’ve found with milling cutters and inserts that the trick for getting the best performance is to understand and balance a number of parameters. I’ll go through what goes into my consideration step by step and in detail.
Woodruff keyCutterchart
Face milling is a machining operation that uses a rotating cutter with multiple cutting edges to create flat surfaces. It is basically the face mill that is mounted to the spindle and rotates around its axis while the workpiece is fed past the cutter. The cutting edges of the tool contact the workpiece in a series of intermittent cuts to remove material from the workpiece, thus creating the desired surface flatness and finish. The face milling can be executed on horizontal and vertical machining centres. It is a highly accurate and efficient method of manufacturing operations. Manufacturers can easily tweak out the correct results by selecting the proper type of cutter and the operational parameters such as cutting speed and feed rate.
Knowing these parameters in their depths enables you to establish optimal cutting conditions, longer tool life, better surface finish, and ultimately, successful machining operations. Each of these parameters deeply affect your workflow, so you are able to get the job done right.
Wiper inserts can be used to increase the surface finish of the parts during machining operations. The following are the main advantages of using wiper inserts:
Face milling operations (as with most other general-purpose cutting processes) can have a number of pitfalls to overcome, particularly when using larger tools in heavier-duty applications. So here’s a brief response to some of the common questions that I am asked:
Optimization can be achieved through empirical methods like Response Surface Methodology (RSM), as well as practical experience and adjustments. Utilizing specialized software and referencing scientific research, such as academic journals and industry standards, can also aid in fine-tuning process parameters for optimal performance.
IndexableKeyseat Cutter
Material Hardness: Milling softer material extends the tool life. Use high-quality carbide inserts for heavier cuts and better life. The parameters include:
It is important to keep the cutting forces and the level of vibrations to a minimum to avoid damaging the workpiece and to facilitate efficient milling. Here are a few rules of thumb on how to do that.
Furthermore, proper selection of cutting speed, feed rate and spindle speed are critical. All of these varied parameters need to be precisely calculated depending on the particular workpiece and its intended result. Raising the surface footage per minute (SFM) of the cut and optimising spindle speeds can increase productivity, but need to be controlled in order to prevent premature tool wear. On the other hand, operating at lower speeds and maintaining control of the feed rates will increase tool longevity and better surface finishes – arguably, at the cost of throughput.
Keeping Tolerances: In high-precision applications, keep the following parameters close. Key parameters to keep include:
You can only do this if you consider these parameters correctly when you choose a cutting tool for your face milling operation. When selecting your cutting tool keep in mind that you want to remove material by chipping, that this chip should be long and slender, that the chip thickness should be thin, and that you want to do all this as fast and accurately as possible and with as little wear to the tool as possible. Happy milling!
This will help the manufacturer to comprehend the core capabilities and shortcomings of it, and to decide if a face milling machine is the right fit for their production consideration.
These variables enable makers to decide upon the most appropriate milling setup for manufacturing purposes. In conclusion, while vertical CNC milling is good for precision and small parts, horizontal CNC milling is a better option for large, complex parts due to superior efficiency and flexibility.
To adapt, it’s important to have a clear understanding of what each vertical or horizontal CNC milling setup offers, in addition to knowledge of which applications are ideal for each option. Here are the key parameters to keep in mind:
Choosing the face milling tool as per your machining requirements is a combined effect of the material with desired surface finish at right machining parameters of feed, speed and flushing. With the thrust on industry and growing demand of tools in production, it is always important to choose the right tools for the right job. Hence, the finish/indentation depends upon the geometry of the tool, in particular, shape of the cutting edge and number of flutes. Balancing the cutting forces, the tool life and the chip Evacuation becomes prime to get the best result in face milling and engages to select the right carbide grade. And when ti-nitride coating are used on Carbide, the balanced result with lesser wear can be obtained. The use of titanium nitride (TiN), titanium carbon nitride (TiCN), and aluminium titanium nitride (AlTiN) coating on the face milling tools not only improves wear resistance but also heat resistance with the help of their hardness to reduce the heat generated in the metal cutting zone and thus reducing the friction.
By reviewing these sources, readers can gain a solid understanding of face milling processes, from theoretical foundations to practical applications in an industrial setting.
Surface quality requirements dictate the choice of cutting tools, their geometry, and the machining parameters. For example, achieving a smooth finish may require tools with finer teeth and precise control over the feed rate and depth of cut. Conversely, roughing operations may utilize tools designed for rapid material removal with less emphasis on finish quality.
The main point of the comparison is that high feed milling is best when you need to work fast and remove more material at a time without considering the surface finish and accuracy. And for more general face milling, it is best to balance your feeds per tooth to match the material you need to remove with the surface finish or accuracy you require for your project. This will help you determine which strategy suits your machining operations.
This way, when you follow these tips and adjust those parameters properly, you successfully maintain the optimal spindle speed and feed rate and get an efficient, qualitative milling.
For those who are not familiar with both the high feed milling and general face milling strategies, it may be interesting to compare the differences between these two methods.

The main parameters in face milling include cutting speed, feed rate, depth of cut, and the type of cutting tool used. Optimizing these parameters helps enhance surface quality, increase tool life, and improve overall efficiency of the milling process.
Face milling (also known as face cutting) is an essential machining operation in manufacturing where planar surfaces are machined on a workpiece, or when a file´s like a geometry is generated. It is a highly productive machining process since it allows one to generate planar surfaces both quickly and to high precision. In this article, you will learn the key techniques and tools that make face milling a productive machining process. Whether you have years of experience machining or are new to the industry, understanding the techniques (cutting styles, cutter types, etc.), cutting parameters (feed rates and cutting speeds), operating environment (climatic conditions, etc), and workpiece material (machine properties), amongst others, are all crucial to your performance and improving the quality of your end product. We will explore all these aspects to help you boost your machine knowledge and skills. Join us on this journey to unlock the key techniques to elevate your productivity and achieve high-quality outputs.
Various industries use face milling machines for different purposes. To name a few, automotive face milling machines are employed to make engine blocks and others. Face milling machines play a major role in manufacturing the complex parts of an airplane found in the aerospace industry. Face milling machines are also used in manufacturing molds and dies, which requires the machine to perform accurate cuts and deliver a desired surface finish. Since different applications have different requirements, selecting the right type of face milling machine and leveraging its particular advantages can help manufacturers to enhance performance, optimise machining, obtain the required surface finish, and improve overall product quality.
 18581906093