AISI 4140 Alloy Steel - 4041 steel
I’m trying to mill some aluminum (to a depth of about 3mm) and after breaking half a dozen bits that were admittedly cheaper, I’m needing to find something that’s made for the job.
They were the most recent I tried. I used half a dozen variations and they all broke the bits. The main thing I changed was I kept reducing the feed rate. 350 mm/min was the slowest I tried.
2019627 — Today we're going to teach you how to machine carbon fiber sheets as ZMorph VX Multitool 3D Printer is a perfect device for such task. Read ...
late 14c., "to play upon the flute," from flute (n.). Meaning "to make (architectural) flutes" is from 1570s. Related: Fluted; fluting.
I’m no expert, but I’ve probably got about 40-50hrs cutting AL on my X-Carve for the High School First Robotics team I’m mentoring. I gave up on cheep bits a long time ago. I don’t really use my CNC enough to warrant penny pinching on the bits. A good bit will last me a long time so I don’t mind spending a little extra (even 10x).
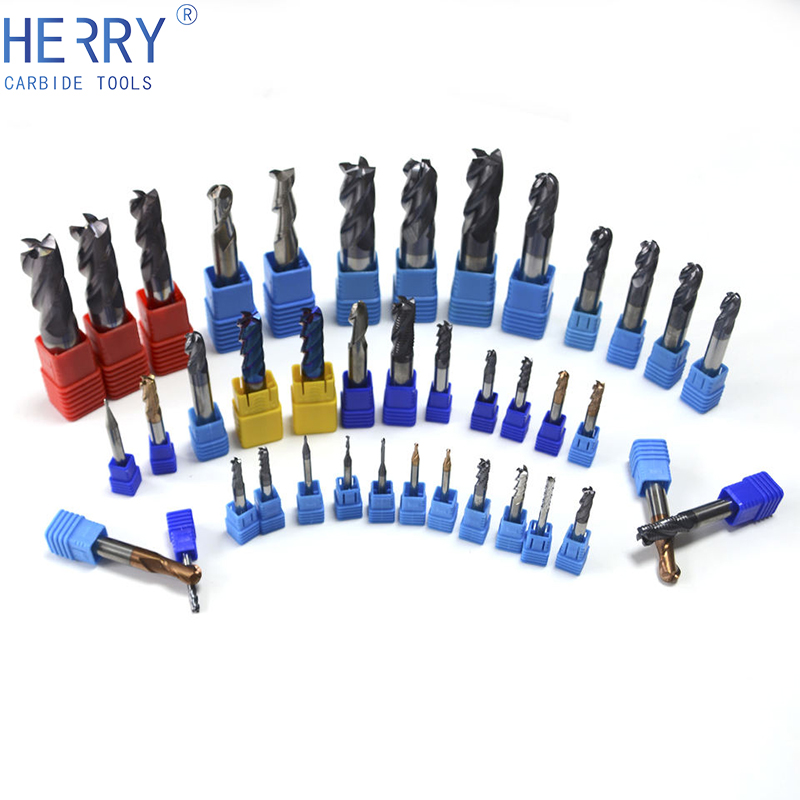
Best CNC bit for aluminum
If you are breaking viper bits then your settings are wrong. Viper bits are generally accepted as very suited for milling alu.
We use cookies to personalize content, interact with our analytics companies, advertising networks and cooperatives, and demographic companies, provide social media features, and to analyze our traffic. Our social media, advertising and analytics partners may combine it with other information that you’ve provided to them or that they’ve collected from your use of their services. Learn more.
I have had excellent result with these bits - http://www.ebay.com/itm/Lot-5Pcs-Solid-Carbide-Aluminum-End-Mill-3Flute-Cutting-Dia-3mm-Shank-Dia-6mm-/122670973669?hash=item1c8fc282e5
BALAX 10852-8QL, #4-40 Size, H5 Thread Limit, Bottoming Chamfer, Bal-Plus Premium Powder Metal, Right Hand Cut Thread Forming Tap ; Classification, 2B ; Drill ...
Mild Steel: 50 – 120m/min; Stainless Steel: 20 – 75m/min. There can be a wide range with the speeds as the quality and thickness of the steel, whether ...
Albeit not an Xcarve, but my diy inc behaves similar to the Xcarve - with 0.1mm DoC (Depth of Cut) I usually go fast, around 1200-1600mm/min with a 3F uncut helix bit at 10K rpm (Makita)
202428 — Enter the diameter of the workpiece and the RPM (revolutions per minute) into the calculator to determine the surface footage.
Take a close look at the end of the broken bit you will probably see it all galled up with melted aluminum. It is a huge problem to cut over chips in aluminum. Were you using dust extraction or air?
dont worry about the price they are all expensive I have spent over 1000.00 this month alone in tools for different jobs and I just place another order this morning for a single .125" compression spiral at 50.00 each
Best end mill for aluminum
I really like the single flute Amana Solid Carbide Aluminum Cutting Up bits (51417) for routing parts out. https://www.amazon.com/gp/product/B0184VY3OA/ref=oh_aui_search_detailpage?ie=UTF8&psc=1 I have found that I can run a 3/16" bit faster than the 1/8" bit. The 1/8" bit flexes too much and will chatter sooner. The 51417 bit has a 1/4" shaft which helps reduce flex. I tried a 1/4" cut, but found that I had to go slower due to system flex and not really having enough power to cut the AL faster. I added stiffeners to the X and Y axes, but still run the stock Z-axis. I also agree that you need to have a vacuum or compressed air to remove chips. As soon as you start getting any chatter, stop or you’ll be dealing with a gummed up bit. The one downside to the single flute is that it does not plunge cut well and will wobble as it goes in. So it does not make circular holes well.
The drill drivers are best to use for basic hole drilling and they work with a range of materials, from plastic and wood to metal. The power choice comes from ...
You need to share your project. Use a solid carbide upcut bit, do not use the downcut. dust collection is a must, dust collection and air is even better you do not want any chips in your cut path. Setting 1 on the dewalt, shallow cut (.005) and fast feed (30-50ipm) The 51471 should be fine I also use drillman1 on ebay OLIVER TOOL COMPANY | eBay Stores The Destiny Viper bits are great.
End mill for aluminum
Shop Chicago Rawhide 22550 at Applied.com, which includes; 2 in Shaft Diameter , 3 in Housing Bore Diameter , 9 mm Overall Width , Nitrile Rubber (NBR) Lip ...
For plunge cutting holes I use a two flute 1/8" Kodiak solid Carbide end mill: https://www.amazon.com/gp/product/B007BTPPVM/ref=oh_aui_search_detailpage?ie=UTF8&psc=1 The Kodiak looks and price are similar to the Destiny bit talked about above. I have not used the Destiny bit so I can’t compare them though. The Kodiak does a great job of plunge cutting holes, but it does not side cut as well as as the single flute Amana. So if it is a big job, I tend to use the Kodiak to plunge cut holes first, then cut out the actual part with the Amana.
tooling is the number 1 expense when running these machines but with the jobs that come in your customers should be paying for these tools or at least part of them
FSAE MICHIGAN's profile picture. FSAE MICHIGAN. 1,245 posts. 38,107 followers. 553 following ...
1827, from Italian flautista, from flauto "flute" (from Late Latin flauta; see flute (n.)) + Greek-derived suffix -ista.
Router End MillBitsfor Aluminum
[vc_row full_width=”stretch_row_content” full_height=”yes” parallax=”content-moving” parallax_image=”3695″ wpex_bg_overlay=”dashed” min_height=”1200″ css=”.vc_custom_1542893308971{padding-top: 230px !important;padding-right: 20px !important;}”...
2021113 — In your case, LSM6DS3TR stands for Linear Sensors Module, 3-Axis AXL + 3-Axis GYR, Digital, "S3" is the family of this specific IMU, packaged in ...
Hand ground flats can be sus- pect and common cause. Use ... End Mill Diameter – Always select the largest diameter possible for your milling operation.
There’s obviously a big price difference between the two and I’m really weary of spending $25 on a single bit given how quickly I broke the last few.
Amana CNCbits
1/4 router bit for aluminum
Find many great new & used options and get the best deals for 1/8" (.125") CARBIDE END MILL 2 FLUTE LONG DESTINY VIPER FOR ALUMINUM V20812 at the best online prices at eBay! Free shipping for many products!
I concur with @RickPeterson . The Destiny Viper bits work very well with aluminum. .005 Depth with a 40% step over at 50ipm has served me well and they last and last and last. Check tramming. That is critical when milling aluminum.
Too slow cutting speeds lead to edge build-up and blunting, while too fast results in quicker insert wear, deformation and poor finish. Tool feed calculator F.
Breaking bits will most likely happen from bit getting “gummed” up. => bit rubbing more than cutting / rates too conservative. Machine rigidity also play a factor here.
Ancient flutes were direct, blown straight through a mouthpiece but held away from the player's mouth; the modern transverse or German flute developed 18c. The older style then sometimes were called flûte-a-bec (French, literally "flute with a beak"). The modern design and key system of the concert flute were perfected 1834 by Theobald Boehm. The architectural sense of "furrow in a pillar" (1650s) is from fancied resemblance to the inside of a flute split down the middle. Meaning "tall, slender wine glass" is from 1640s.
early 14c., from Old French flaut, flaute (musical) "flute" (12c.), from Old Provençal flaut, which is of uncertain origin; perhaps imitative or from Latin flare "to blow" (according to Watkins, from PIE root *bhle- "to blow"); perhaps influenced by Provençal laut "lute." The other Germanic words (such as German flöte) are likewise borrowings from French.
 18581906093