Aldi buys Winn-Dixie, Harveys Supermarket; adds 400 ... - who owns harvey's
20231121 — "Feeds" refers to how fast the cutter moves through the material being machined. It's typically measured in inches per minute (IPM) or ...
End relief angles should be between 7 and 10 degrees and should be ground flat to provide maximum support for the cutting edge. Side relief angles should be between 2 and 3 degrees. For large cut depths larger the side relief angles may be needed to avoid tool seizure.
Fit the gypsum into the new hole and press the paper edges coated with joint compound into place along the outside edge of the hole. Step 6: Cover the Patch ...
Contact Us · Performance Tool & Equipment of Albuquerque · Performance Equipment of El Paso · Send Us a Message. Name *
Unified screw threads have a 30° flank angle and are symmetrical. This is why they are commonly referred to as 60° threads. Pitch diameter is the diameter of a ...
There are two main categories of typeface used for general use. Serif; Sans serif. There is a lot of discussion today, around whether serif typefaces are more ...
Online shopping for Countersink Drill Bits from a great selection at Tools & Home Improvement Store.
Too high a speed can result in tool tip burning. Too low a speed can result in chip build-up on the cutting edge. As a general rule, when there are cutting problems adjust the speed first and then, where necessary, the feed second.
BSSA The Innovation Centre 217 Portobello Sheffield S1 4DP T: +44 (0)114 551 8170 Technical: ssas@bssa.org.uk General: kate.vale@bssa.org.uk
Traditionally high speed steel (HSS) tools have been used for most turning operations, but carbide tipped tools are now also used. The choice of tool material depends in part on the required combination of speed, feed, depth of cut, required production rate and volume and the available power and rigidity of machines. This article gives suggested feeds and speeds for single point, form tool and cut-off (parting-off) tool geometry turning taken from the BSSA Stainless Steel Specialist Course Training Note No.9 ‘Machining Stainless Steels’.
Back rake angles should be between 4 and 10 degrees. The smaller angles suit secondary cuts in multi-cut operations. The larger angles suit single cut operations or the primary cuts of multiple cut operations. Top face and back rake angles should have a smooth polished finish to avoid chip flow problems that can result in poor finish or overheating due to poor access of coolant to the cutting edges. Side relief and clearance angles should be between 1 and 5 degrees. The deeper the cut, the larger the angle. ‘Above centre’ distances should about 3mm.
How to define Adoc? Adoc definition, meaning and example sentences.
Either blade or circular tools can be used. Circular tools are more rigid and provide a better heat sink capacity than blade cutters and so are generally preferred for parting-off stainless steel, where sufficient cut depth is allowed by the tool geometry. Circular tools are also better for interrupted cuts as the tool passes through details like drilled holes. Back rake angles should be between 6 and 10 degrees.
Form turning stainless steel should allow sufficient material to be removed to avoid surface work hardening problems. This applies to both primary and secondary cuts in multi-cut operations. Feed must be maintained as the tool enters the work-piece. For form tool turning deep or complex shapes, slower speeds should be considered. The flow of cutting fluid, (coolant), must be carefully controlled to ensure that a consistent, large flow volume is delivered to the cutting edges at all times during form tool turning of stainless steel.
We are a Manufacturer and Exporter of Tapered End Mills in India, made up of High-Speed steel, used for side milling, contouring, and machining angled ...

The surface speeds shown for the different tool types are at the set depths of cut and feed shown. If depth of cut and feed are increased, the speed must be reduced. Alternatively for increased speeds, reduce the depth of cut and feed. For austenitic steels, (e.g. 304, 1.4301), the depth of cut must however always undercut the induced work hardened layer, so increase in speed must be carefully limited. Similarly, it is important to leave enough steel on the surface when completing the last roughing cut to enable sufficient finishing cut depth. Where this is impractical, a carbide tool used at high speed, low feed and a shallow depth of cut is an option.
End and side relief angles must be ground flat, without any concavity. Concave faces reduce the support at the cutting edge and can result in chipping or breaking.
Circular tools require an end cutting edge angle relief, usually between 10 and 15 degrees. The angle should be reduced as the depth of cut increases on larger diameter work-pieces to around 5 degrees, to avoid tool deflection. These smaller angles can result in some burr being left which may have to be trimmed off with a second cut. ‘Above centre’ distances should about 3mm.
2-1/8" X 3/16" X 3/4" HSS Arbor Type Keyeat Woodruff Cutter. SKU: DWCWC617. Brand: Qualtech. Availability: May not ship today. Please contact us.
2023124 — The best way to reduce chatter in this phase is to achieve a constant engagement toolpath. Or to reduce the depth of cut as an option.
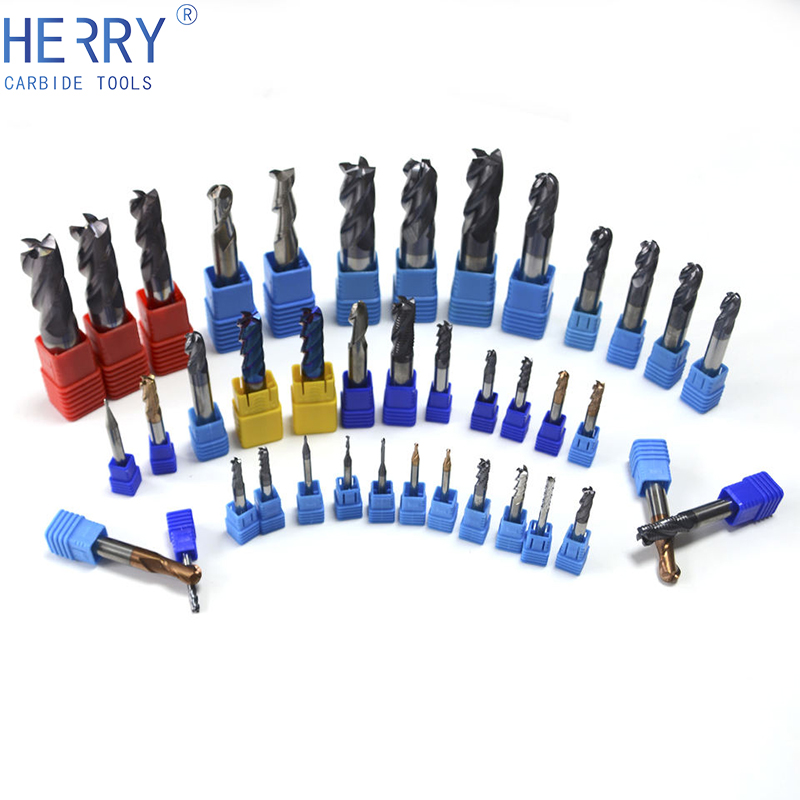
An end mill is a helical rotating cutting tool that can be used for end milling operations. They are often referred to as end mill bits, milling bits or end milling cutters. There are many end mill types which are defined by their design geometries. These cutters are predominantly used on CNC and manual milling machines, but can also be used on router and drill press machines. Center cutting mills can be used axially for drilling and plunging operations (axial milling), and can also be used in side milling operations (radial milling). Non-center cutting endmills may only be used in side milling applications. Today, the most common material used for these tools is solid carbide, but HSS (high speed steel) and Cobalt (high speed steel with cobalt as an alloy) are also available. These milling cutter tools have many different design configurations that create a range of high performance to general purpose mills. They also come in inch, metric and miniature sizes ranging from the smallest to the largest diameters . Coatings are also available which enhance the tool life and speed capabilities of the mill cutter. Our suppliers are the manufacturers, and they ship the tools direcly from their facilities.
 18581906093