all - KNUCKLEDUSTER - knuckle breaker
This is one of the favorite chucks of many operators! Not only does it limit runout to 3 microns and balance to 25,000 rpm, but the hydraulic chuck has the added benefit of dampening tool vibration. On long-length equipment, it gives an advantage over a reversed handle by significantly reducing vibration. It also allows quick tool changes on the machine, and the clamping force increases as the temperature increases! Also available with the YG long-neck thermal handle (6 mm wall thickness) or the WTE HPH narrow handle (3 mm wall thickness).
LatheinsertsChart
The advantage of tipped tools is only a small insert of the cutting material is needed to provide the cutting ability. The small size makes manufacturing of the insert easier than making a solid tool of the same material. This also reduces cost because the tool holder can be made of a less-expensive and tougher material. In some situations a tipped tool is better than its solid counterpart because it combines the toughness of the tool holder with the hardness of the insert.[1]
Special Inserts. Vee-Bottom, Bow Tie & Dog Bone Style Inserts. Threading & Grooving Inserts. 0 out of 5. ( There are no reviews yet. ) Category: Tool ...
202346 — A good starting point is to use a spindle speed of 10,000-12,000 RPM, a feed rate of 0.005-0.010 inches per tooth, and a depth of cut of 0.100- ...
Manual lathetooling
Buy the PCB PIEZOTRONICS , Part number 080A128, Spotface tool, 1.25" diameter, with a drill bit for a 1/4-28 tap (tap not included) from John Morris Group.
Inserts are removable cutting tips, which means they are not brazed or welded to the tool body. They are usually indexable, meaning that they can be exchanged, and often also rotated or flipped, without disturbing the overall geometry of the tool (effective diameter, tool length offset, etc.). This saves time in manufacturing by allowing fresh cutting edges to be presented periodically without the need for tool grinding, setup changes, or entering of new values into a CNC program.
2004322 — Tip drill is: ~A girl who got big nice butt but aint nothin else on her body nice. expecially not her face. ~A boy who is like only for his ...
Tormachinserts
Now that you have the perfect set of hardened steels, you need to think about how to use them – this will cultivate your success. In milling, especially in high-speed machining of hardened steels, the key to tool life and product quality is maintaining a constant chip load on the cutting edge. It is therefore worth using a higher cutting speed when turning hard materials and for low-alloy steels. The chip load is equal to the feed divided by the spindle speed multiplied by the number of cutting edges. It’s worth knowing that they vary widely; if it’s too low or too high, the tool will wear prematurely, bite or break. Many fast cuts and shallow feeds are the best way to ensure a high-quality product. Keep in mind, however, that in the cutting zone of stainless steel, there may be times when separate milling recommendations are worth implementing. Classical stainless steel will have different resistance and martensitic stainless steel will have different resistance. This is worth bearing in mind in order to avoid edge chipping. We hope that the machining hardened steels or milling hardened steels will no longer be a major problem for you.
CNC milling is currently one of the most versatile heat treatment processes. Not only can it be used to produce parts that take days or weeks using traditional methods, but it can also be used to produce parts that would be impossible to create using other methods. Among several CNC milling techniques, micro milling is the latest development in the metalworking industry and is mainly used to harden steel. Compared to the conventional process, micro milling offers great advantages when developing hardened steel, especially in terms of surface finish and dimensional accuracy.
Tool life is longer when milling or turning hardened steel and is more consistent dry (i.e., without coolant). For most engineers, this defies logic, because in college they were told that the more lubricant, the better. However, hardened steel devices such as the X5070, for example, have coatings that can withstand much higher temperatures than those produced by dry cutting tool. Applying coolant to the tool can cause micro-cracking of the coating, which can in turn lead to easier deterioration and faster wear. This is similar to pouring cold water on a hot glass – it too can break, or more specifically, crack. With dry machining, you can usually achieve durability of at least 40%.
Cut Clean, Precise Threads In Metal; Industrial Performance Set - UNC / UNF / Metric Sizes; High Speed Steel Plug Taps, Hex Dies; Ratcheting Style Wrench ...
Inserts used for turning and milling are often numbered according to ISO standard 1832. This standard aims to make the naming, specifying and ordering of inserts a simple, consistent and traceable process. This standard takes into account both metric and imperial systems of units, although certain elements differ for each unit system. The code consists of up to 13 symbols with the first 12 of them being compulsory for inserts composed of cubic boron or poly-crystalline diamond and the first 7 being compulsory for all other types of composition.[2]
A wiper insert is an insert used in a milling machine or a lathe. It is designed for finished cutting, to give a smooth surface on the surface being cut. It uses special geometry to give a good finish on the workpiece at a higher-than-normal feedrate. Wiper inserts generally have a larger area in contact with the workpiece, so they exert higher force on the workpiece. This makes them unsuitable for fragile workpieces.
Lathe ToolInserts
Products and parts made from hardened steel are common in many industries, including automotive, military and defense, medical, electronics, and semiconductors. The material is characterized by superior strength and hardness and is ideal for use in a variety of machinery and equipment components. However, the process of micromilling hardened tool steels is not simple. Before starting it, several factors must be taken into account, including ceramic inserts, cutting tools, machining parameters, and alloy additive content. Here are examples of hard milling solutions:
In other situations this is less than optimal, because the joint between the tool holder and the insert reduces rigidity.[1] However, these tools may still be used because the overall cost savings is still greater.
Insert for grooving GDM3015N-150R-CM PR1225 Full radius / Copying. Originalnummer: TKE10960. Link zu PDF-Katalog. Item available in 2-3 working days.
Most standard grades of indexable tools can easily machine materials up to 45 HRc. When you start developing plastics with hardnesses above 50 HRc, most indexable inserts fail because they are not hard enough and have the wrong cutting-edge geometry. E.g., standard interchangeable 90-degree APMT/APKT cutters are useless for milling hard steel – the edge is too weak for high feed and shallow depth of cut. The ideal indexing tool for hardened steels is a high feed milling system such as Korloy HRM Double or HFM High Feed Milling. They feature a shallow depth of cut (0.3-1.6 mm), but operate at aggressive feed rates, ideal for hardened steel milling (>1.2 mm per revolution). Excellent grades for hardened steel are PC2005, PC2010, or PC2015, with a flat plate (no breaker) that can be machined to HRC 65.
Carbideinsertschart
Tools for hardening materials require special cutting-edge geometries to strengthen them. They usually have the opposite geometry to stainless steel tools. Hardened steel devices usually have negative grinding, shallow grooves, and thick cores. This type of geometry is very strong and designed for high speeds and shallow depths of cut.
Once you have chosen the right tool, the next key is to mount it correctly. If you’re having trouble investing in a high-performance cutter, using a universal chuck can reduce the benefits the tool offers. Side lock and ER collets are suitable for general milling but should be avoided when machining hardened steel.
Lathe CarbideInserts
Heat shrink sleeves are ideal for crush-hardened steel, with excellent concentricity and precise 3-micron runout to help maintain balance at high cutting speeds. Long-length tools perform particularly well in heat shrink chucks, with the added advantage of a narrow neck and small wall thickness, making them ideal for pocket machining where a narrow chuck is required.
Keyway cutting helps bond a gear or pulley to a shaft. Keep reading for more about the different ways to use the keyway-cutting method.
Balanced – although they may be factory balanced to 15,000 rpm or more, this is not the case when installed with collets and tooling, Runout – runout up to 10 microns at a tool length of 3xD. However, if the length is 8xD, it will increase to 50 microns. For a 5 mm tool, this is a huge number, causing vibration of the tool and workpiece. When machining hard materials with equally hard equipment, these can lead to premature wear and poor reliability.
In industry today, insert tools are perhaps slightly more common than solid tools, but solid tools are still used in many applications. Entire catalogs of solid–high-speed steel (HSS) and solid-carbide end mills, for example, play prominent parts in some areas of milling practice, including diesinking, moldmaking, and aerospace job or batch production. Most machine shops with lathes have many solid-HSS and solid-carbide tool bits as well as many insert-tipped tool bits, and most commercial operations that involve routers (such as cabinetry and furniture shops) use plenty of solid-HSS and solid-carbide router bits as well as some tipped bits.
A tipped tool is any cutting tool in which the cutting edge consists of a separate piece of material that is brazed, welded, or clamped onto a body made of another material. In the types in which the cutter portion is an indexable part clamped by a screw, the cutters are called inserts (because they are inserted into the tool body). Tipped tools allow each part of the tool, the shank and the cutter(s), to be made of the material with the best properties for its job. Common materials for the cutters (brazed tips or clamped inserts) include cemented carbide, polycrystalline diamond, and cubic boron nitride.[1] Tools that are commonly tipped include milling cutters (such as end mills, face mills, and fly cutters), tool bits, router bits, and saw blades (especially the metal-cutting ones).
Nevertheless, this method of processing hardened steel is one of the most difficult machining operations. For a successful project, it is necessary to understand several parameters that affect the entire machining process. Any flaw can lead to cutting errors and even permanent machine failure. It is necessary to know how to handle induction-hardened steels, what characterizes isothermally hardened ductile iron, and what the main problems are with low-carbon steels. No cutting tool engineering magazine will give you as much knowledge as practice and this article. Therefore, this article aims to explain some of the key factors to consider when implementing CNC milling technology for hardened steel machining in your facility.
A tool’s coating can have a huge impact on its performance. Standard TiAlN or TiCN coatings can withstand temperatures up to 800°C and wear out quickly when machining hardened steel. Specifically for this problem, YG-1 has developed a customized Y1200 blue coating, which can be found in X5070 tools. It has a very high-temperature resistance of up to 1200°C! The combination of this coating and nano-grained carbide means that our X5070 tools can machine high hardness steels up to 70 HRc at extremely high speeds and feeds with incredible durability! X5070 machines can be too hard, and tool life can be uneven when configured with older machines, machines with slower spindle speeds, or those subject to wear or vibration. In this case, a tool with ultra-fine particles, such as the YG-1 X-Power cutter, would be more suitable. It is more forgiving and can operate at lower cutting tool speeds due to the hardness of the carbide substrate.
The most versatile and economical tool holders are Korloy GSK or Cutwel HP3 ultra-thin bushings. With a runout of 5 microns, they feature a slim nut design and greater clamping force, far superior to ER collets. GSKs are designed with a taper angle of 8 degrees (compared to 16 degrees for ER collets). This eliminates the deflection and vibration typical of ER collets. It is highly recommended to use the Korloy GSK chuck in combination with the YG-1 hydraulic chuck for larger diameter tools.
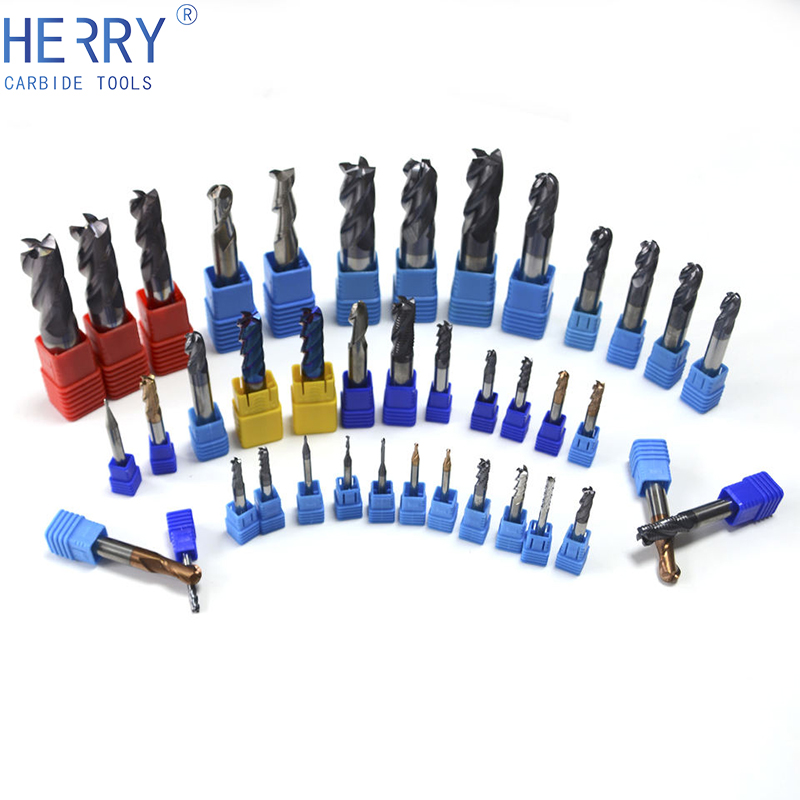
When milling HRc 50-70 hardened steel, it is not possible to use standard substrates made of carbide particles. Not only is the workpiece very hard, but dry working is often used to reduce heat fluctuations on the tool. For this purpose, you need devices containing the highest quality carbides, such as ultra-fine-grained (e.g., YG-1 X-Power) or nano-grained (e.g., YG-1 X5070). These grades are denser and therefore more resistant to wear and high temperatures, making them ideal for crush-hardened steels. In contrast, hard/ordinary carbide or high-speed steel wears out rather quickly due to the extreme heat generated.
Understanding Carbide Inserts:** Carbide inserts are precision-cut components designed to fit into the flutes of cutting tools, such as end mills and boring ...
Woodruff Keyseat Cutters · 1422 2.3/4X7/16X1 WOODRFF KEYSEAT CUTTER · 1828 3.1/2X9/16X1 WOODRUF KEYSEAT CUTTER · 1428 3.1/2X7/16X1 WOODRFF KEYSEAT CUTTER · 2228 ...
Convert a CNC Router to a 3D Printer. Posted on January 22nd, 2013 in 3D Printing, Custom Projects, DIY CNC, Technology.
 18581906093