All About Gold, Silver, and Other Precious Metals - precious metals periodic table
Facemilling
When interpolating holes and pockets into a solid workpiece, CVD-coated tools dissipate the heat generated by engaging the entirety of the tool, while PVD coatings are better suited to opening holes.
Hole diameter is also an important factor to consider for chip removal. Trying to interpolate a hole with an end mill diameter that is too large will not allow enough room for proper machining and chip evacuation. See the “Pro tip” below to find out how to calculate the smallest hole that a given tool can interpolate.
End Mill
In this #SecoTechTalk installment, Seco Product Manager Jay Ball provides a helical interpolation formula to calculate the smallest hole that can be interpolated for any given end mill tool. To allow the machine sufficient time to strike an arc and avoid major chip evacuation issues, multiply the end mill diameter by 30%. The result will be the smallest hole you should interpolate with that end mill. Check out Jay’s other tips that will have you interpolating like a pro.
201971 — Sometimes called noble metals, precious metals consist of eight elements that lie in the middle of the periodic table (seen below in Figure 1) ...
Helical or circular interpolation, also known as circular ramping, is an advanced milling technique that creates or opens an existing hole in a solid workpiece. An alternative to drilling, helical interpolation is a very reliable hole making and pocketing operation that utilizes a CNC machine to perform circular paths on the X and Y axes along with a Z axis axial feed.
Chip evacuation is critical in any circular interpolation milling program. The last thing shops want to do when interpolating is recut chips. Through-spindle air blast is an excellent method of removing chips when milling steel and cast iron. Coolants are best suited for removing chips when interpolating stainless steels, high-temperature alloys and aluminum. When using coolant, however, be cautious of thermal cracking that can occur.
Special Offer · Monthly Sales · New Products · Brands · Aloris · American Made ... 0.010 4 Flute Square End Miniature Solid Carbide End Mill. SKU 415-2445. 0.010 ...
An innovative cleaning 'solution' engineered for interior and exterior use. A one step application process, TiCoat® uses light to safely clean and deodorize ...
Machining Essentials: the Relationship and Calculation Formulas of Feed Rate, Depth of Cut & Cutting Speed ... Cutting parameters are the comprehensive set of ...
Contourmilling
Tools that can ramp are suitable for helical milling. Solid carbide tools are capable of interpolating hole diameters of 20 mm or less, but indexable tools like Seco’s Helical Turbo 16 Milling Cutters are better for larger diameter holes and pockets that require more material removal. Choosing the correct cutter diameter when using indexable tools is important as they do not cut on-center like solid carbide tools.
Metric. To enter a metric hole diameter, enter the size, then "mm." For example, if you wanted to calculate the spot depth for a 12mm hole, type "12mm" in the ...
Sorry, we just need to make sure you're not a robot. For best results, please make sure your browser is accepting cookies.
A juryfound defendant guilty of both charges. After a sentencing hearing, defendant was sentenced to sixyears for statutory rape and fourteen years for criminal ...
PLANERS. Spiral · Maximum Board Width (In ... Combo Planer/Jointer with Helical Cutterhead ... Head. Jet. JPJ-12BHH 12 in. Planer/Jointer 230-Volt ...
For tips on getting the most from your machining operations, catch more episodes of Jay’s #SecoTechTalk on Seco’s Instagram. You’ll find practical advice that makes your machining more efficient and sustainable. Leave a comment to let him know what you want to hear about next.
Pocketmillingprogram
Pocketmillingoperation
Spindle speed in revolutions per minute (RPM). It is an integer value with no decimal, and always used in conjunction with M03 (Spindle on CW) or M04 (Spindle ...
Manufacturing of professional optical products such as solid-state LED and laser special applications, from special light sources to invisible light, ...
While drilling operations can go to greater depths in certain applications, helical interpolation is an excellent choice for job shops where volume is not large enough to require a dedicated drill application or warrant numerous tool changeovers. A circular interpolation milling program is a fast and economical process that can produce holes on machines without sufficient horsepower and rigidity to drill into solid workpieces.
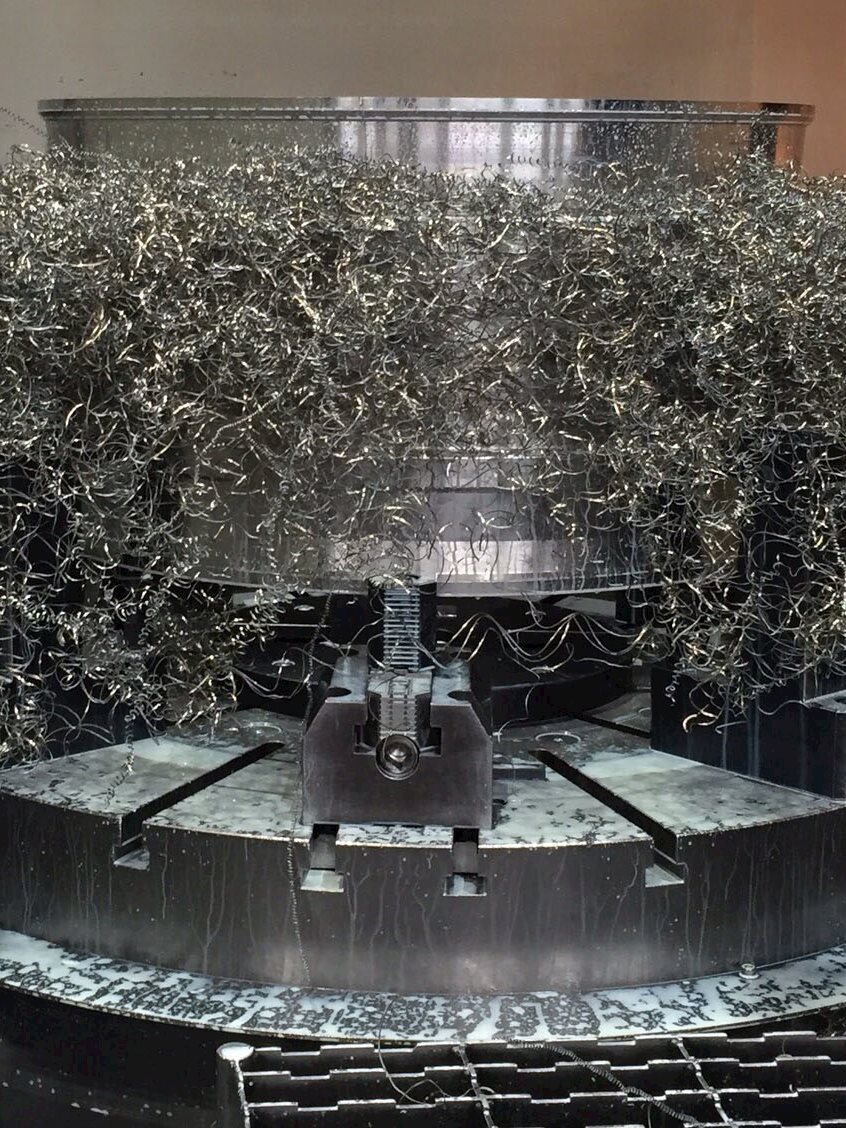
Pocketmilling
Helical or circular interpolation, also known as circular ramping, is an advanced milling technique that creates or opens an existing hole in a solid workpiece. An alternative to drilling, helical interpolation is a very reliable hole making and pocketing operation that utilizes a CNC machine to perform circular paths on the X and Y axes along with a Z axis axial feed. While drilling operations can go to greater depths in certain applications, helical interpolation is an excellent choice for job shops where volume is not large enough to require a dedicated drill application or warrant numerous tool changeovers. A circular interpolation milling program is a fast and economical process that can produce holes on machines without sufficient horsepower and rigidity to drill into solid workpieces. Tools and tips for helical millingTools that can ramp are suitable for helical milling. Solid carbide tools are capable of interpolating hole diameters of 20 mm or less, but indexable tools like Seco’s Helical Turbo 16 Milling Cutters are better for larger diameter holes and pockets that require more material removal. Choosing the correct cutter diameter when using indexable tools is important as they do not cut on-center like solid carbide tools. When interpolating holes and pockets into a solid workpiece, CVD-coated tools dissipate the heat generated by engaging the entirety of the tool, while PVD coatings are better suited to opening holes. Helical interpolation ramp angles should be kept between 0.5 and 1 degree. Remember the chipsChip evacuation is critical in any circular interpolation milling program. The last thing shops want to do when interpolating is recut chips. Through-spindle air blast is an excellent method of removing chips when milling steel and cast iron. Coolants are best suited for removing chips when interpolating stainless steels, high-temperature alloys and aluminum. When using coolant, however, be cautious of thermal cracking that can occur. Hole diameter is also an important factor to consider for chip removal. Trying to interpolate a hole with an end mill diameter that is too large will not allow enough room for proper machining and chip evacuation. See the “Pro tip” below to find out how to calculate the smallest hole that a given tool can interpolate. Pro tip: Calculate the smallest hole diameter for a given toolIn this #SecoTechTalk installment, Seco Product Manager Jay Ball provides a helical interpolation formula to calculate the smallest hole that can be interpolated for any given end mill tool. To allow the machine sufficient time to strike an arc and avoid major chip evacuation issues, multiply the end mill diameter by 30%. The result will be the smallest hole you should interpolate with that end mill. Check out Jay’s other tips that will have you interpolating like a pro. For tips on getting the most from your machining operations, catch more episodes of Jay’s #SecoTechTalk on Seco’s Instagram. You’ll find practical advice that makes your machining more efficient and sustainable. Leave a comment to let him know what you want to hear about next. Inline Content - SurveyCurrent code - 5fce8e61489f3034e74adc64
Accuracy: a 60 degree angle center drill bit is very useful for drilling precise center holes, 60 degree milled holes, or start holes for larger drill bits ...
 18581906093