All Thread Stainless Steel Rod - threading stainless steel rod
Lubricants have always been used in mechanical processing – milling, drilling, sawing, punching. On one hand, in the form of cooling lubricants to dissipate heat, and on the other, oils to reduce friction and wear.
Turninginsertidentificationchart
And one way in which we can reduce the footprint of aluminium products is through dry machining. This means no longer using oil nor drinking water and lubricants in machining centers, with the aim of eliminating them throughout the machine area.
Regardless of the approach you take when considering this option for your processes, you need to realize that doing away with coolants and lubricants in machining is an important step toward sustainability.
Inserttoolingchart
A double lead tap will travel twice that distance in one revolution. The most common use is in adjusting mechanisms where a clockwise turn will make a linear ...
If you need to drill precise holes, Kaka Industries has the right vertical drilling machine for you. Learn more about our equipment by visiting us today.
Main Application. BTA system. Sub Application. Related Tool. Family Designation: DNMG-TM, Negative relief ang., M class, 55deg rhombic insert, for medium ...
Carbideinsertcodes explained
2020521 — Calculates shaft speed of high spindle machines using the shaft's diameter and revolutions per minute (RPM)
Moving up from the shank is the body of the drill bit, which is typically made of high-speed steel or carbide. The body is the part that actually cuts into the ...
Electrical Discharge Machining · Fundamentals of Thermal Joining · Gas ... Calculator – Cutting Speed to RPM. Cutting Speed (feet per minute): Diameter ...
In manufacturing plants, we can start by questioning the resource requirements of the various processes, the type and origin of the operating materials used, their impact on the environment and their recyclability. The avoidance of operating materials is a great step toward sustainability.
Carbideinsertgradechart
CARBIDEinsert Chartpdf
CADEM CAPSturn CNC lathe programming software automatically determines the cutting feed rate based on the surface finish required and the tool’s nose radius.
ISOinsertnomenclature pdf
In a civilization that depends on machines, materials that lubricate moving parts have been considered essential. People have been using lubricants for thousands of years to improve production processes where friction causes wear. We started with prehistoric lubricants such as sludge, liquids from tree trunks and crushed reed, or wood and stones for the construction of buildings. We then moved to animal fats, fatty and oily substances from animal and vegetable oils, and whale oils.
Aluminium is the metal of the future with unique properties and endless application and design possibilities. But it still has a carbon footprint, like every other material, and when you fabricate the metal, the footprint grows. Now we can reduce this footprint with dry machining.
Aluminium profiles are traditionally machined in mechanical centers using CNC machines with cooling lubricants and lubricating oils in a minimum quantity lubrication system. Some companies machine their semi-finished aluminium products partially in a dry state, but there aren’t many.
Lathe inserttypes
In our machining centers, we have decided to carry out milling without cooling lubricants and oils, and other machining steps will follow. We call this dry machining. The key is in the tools: special geometry for chip removal and tailor-made material selection are required.
201974 — Masonry bits have a toughened tip which is quite different to normal twist drills. There is no special colour ... HSS drill bit, for metal. To ...
Creating a Circular Milling Operation · Approach clearance (A) · Plunge mode · Machining tolerance · Direction of cut · Percentage overlap · Compensation number ...
This nose radius chart shows the Rmax in microns for various combinations of nose radius and feed rate. These are theoretical values, and the actual finish that you get will depend on the tool wear, the quality of the machine, vibrations, etc. These values are however a good starting point.
Some scratching around on the www told me that the large fruit-like nest is actually made of paper, and the paper is manufactured by the wasps themselves. The wasps scrape wood from a tree or log, then use water and saliva to break down the fibers in the mouth to make soft paper pulp. They paste into the paper pulp into the required shape for the nest. The cellulose fibres in the wood are the equivalent of the steel reinforcement in buildings, and the saliva is the cement. The spherical structure is just the outer protective covering. Inside this are hexagonal cells where young wasps develop, one per cell. A whole lot of wasps live in a single nest in cooperation. There must also be a complex passage system so the wasps can navigate around the thousands of cells.
The problem is that petroleum-based lubricants pollute the environment and water directly and indirectly through the production, processing and emissions of the substances.
ISOinsertgradechart
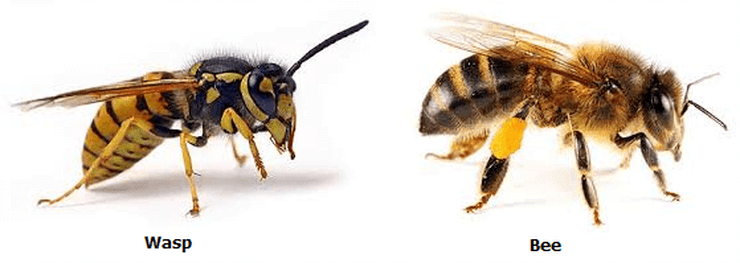
Some wasp factsWasps do not make honey. They are however closely related to honey bees, which do make honey.Wasps are primarily predators and feed on other insects.A Wasp can sting you and then retract its stinger, and stays alive after stinging you.When a Bee stings you it cannot withdraw its stinger, loses its stinger and much of its abdomen in the process, and dies.
Transitioning to dry machining is not simple, but it is attainable. Yes, there are issues, for instance with complex machining processes where realization without lubrication is demanding. Both thread cutting and deep blind holes drilling are not yet feasible without oil.
The nose radius of the insert has a direct effect on the surface finish of the part in turning. Turning actually forms a helical groove on the part – a thread. The depth of the groove is the roughness height. The roughness height (Rmax) is directly proportional to the square of the feed rate, and inversely proportional to the nose radius of the tool. You can actually use a quick reference nose radius chart to determine the feed rate that you must use to get a specified surface finish for any nose radius.
2023214 — The crystal lattice structure of mild steel is typically a face-centered cubic (FCC) structure, also known as alpha-iron.
Team Harvey: With MC Harvey, Ashley Walters, Daniel O'Reilly, Jake Wood.
Aluminium is a key building block for a more climate-friendly circular economy. Nevertheless, we are also aware of the challenges involved in making the entire value chain of the light metal more sustainable. And we need to be aware of these challenges, because the continuous reduction of the footprint of aluminium production and aluminium products is an ethical responsibility.
To improve the surface finish you can either reduce the feed rate or increase the nose radius. Halving the feed rate improves the surface finish four times (reduces the Rmax value by 75 %). Doubling the nose radius improves the surface finish twice (reduces the Rmax value by 50 %). You can use the insert nose radius chart above to quickly decide the feedrate obtainable.
 18581906093