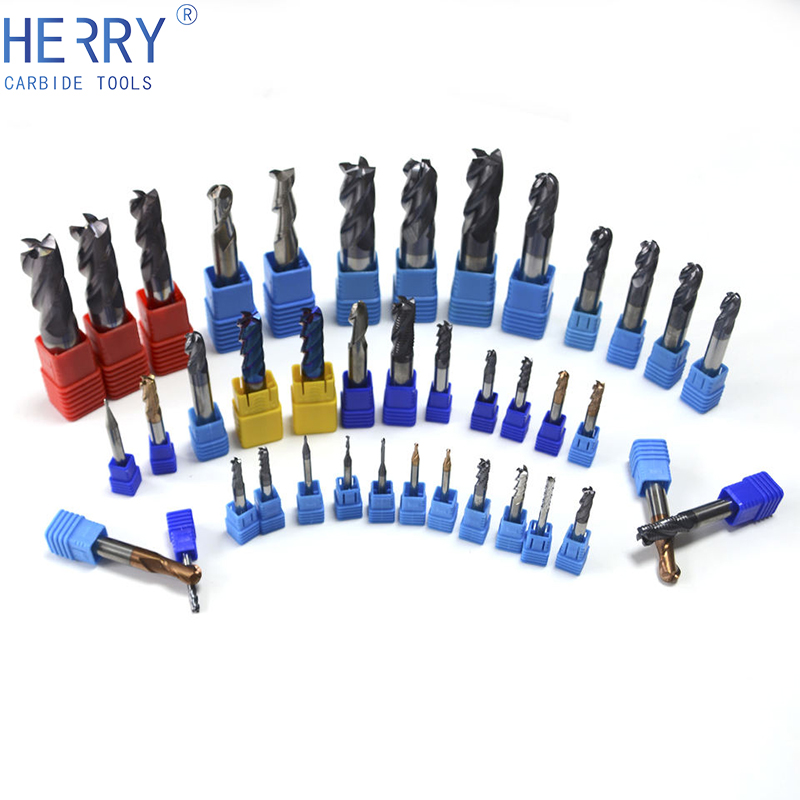
Aluminium Router Bits | Buy Online & In-Store - aluminium milling bits
Five-axis machining center
The alloying elements in steel have a big influence on hardenability. This is particularly so for diffusional transformations such as ferrite and pearlite, where the solutes not only influence the thermodynamic stability of the austenite but can slow the reactions by diffusion since their solubility in ferrite will be different from that in austenite. Displacive transformations such as bainite and martensite are less affected. Elements (Mn, Ni, C) which retard the transformation of austenite and hence shift the ‘C’ curves to longer times and vice versa (Co, Al).
The PVD coatings are biocompatible, very hard and inert, and do not react with bones, tissues or body fluids. This makes them especially suitable for the use on ...
The properties of steels are sensitive to microstructure. It is useful to know how the microstructure develops in different parts of a specimen during heat treatment. For a given steel composition, a Continuous Cooling Transformation (CCT) diagram can be constructed from experimental data, allowing the microstructural development to be followed as a function of the cooling conditions. Fig.1 shows a CCT diagram for a eutectoid
A steel with a high hardenability is one which has a low critical cooling rate, so that even slow cooling will lead to a martensitic structure. This has the advantage that hard material can be generated without the risk of "quench cracking" due to high thermal gradients associated with rapid cooling. On the other hand, it means that hard (and brittle) material may inadvertently be produced in finished artefacts, notably as a result of welding operations.
Martensite in steel can be hard but brittle because of its excessive carbon content. Tempering involves a heat treatment which allows the carbon to precipitate as carbides (e.g. cementite). This, and the annealing of defects, causes the martensite to become softer but tougher. If the tempering temperature is sufficiently high (500 ° C) then substitutional elements such as Mo and Cr become mobile. Fine carbides such as Mo2C then precipitate at the expense of cementite and lead to secondary hardening.
Machininggraphitewith coolant
Graphite material is soft, abrasive, brittle and machining may seem specialised and intensive due to these properties. However, technological developments have rendered the machining processes manageable, and even exciting for business growth. While understanding the material properties, a good knowledge on selecting the right CNC Machining Center and machining techniques for graphite machining is crucial to ensure successful results. Besides using the right CNC Machining Center and machining techniques, suitable toolings contribute significantly to achieving cost effective graphite machining. It is imperative to note that graphite machining does not produce chips, as such, avoid using coolant as it may react with the graphite dust, leading to machine issues and machining complications. Graphite machining produces extensive dust which are harmful to the CNC machine, the operators, and the environment. The conductive graphite dust can cause damages to circuits and electrical issues inside the CNC machine. It can also affect the guideway systems, ball screws as well as other mechanical parts. Overall, the machine must be sealed and protected against this rather damaging dust. A high-performance dust extraction vacuum system is essential for effectively removing graphite dust during machining. This should ensure and prevent accumulation of dust inside the machine, avoiding the risk of serious problems to the key interior components of the CNC machine and the accuracy of the graphite workpieces. Operators must wear protective masks to prevent inhalation of graphite dust if the machine does not have a proper dust extraction system in use. Ensuring proper ventilation and maintaining high air quality in the machine shop are also crucial for safeguarding the operators during graphite machining.
Due to its unique combination of properties in high strength, thermal conductivity, chemical resistance, and machinability, graphite components are useful in critical industries such as aerospace parts, spacecraft parts, semiconductor equipment, and medical devices. Graphite can be difficult to machine, however, with the right CNC machines and techniques, suitable cutting tools, proper speeds and feeds, CNC graphite machining can be rewarding, especially for manufacturers that focus on meeting the specific needs of industries requiring high precision components with unique material properties. Keen to explore or expand CNC machining for graphite? Contact us for a discussion enquiry@hwacheon.com.sg

Hardenability is also affected by the austenite grain size. A finer grain size gives a larger number density of heterogeneous nucleation sites and hence reduces hardenability.
Graphitemillingmachine
Find jobs at Sequoia companies.
Hwacheon has been manufacturing and supplying Vertical Machining Centers for Graphite globally since 1985. Hi-M G1 Pro, a Vertical Machining Center for Graphite is an optional upgraded and improved version of the Hi-M G1 fuelled by users’ feedback. Hi-M G1 Pro incorporates essential features tailored to address the unique challenges posed by the material and advanced functions for modern manufacturing of graphite components. The high efficiency dust extraction system boasts a specialized baffle, ensuring even dispersion and collection of dust across the entire filter area. With its compact size, user-friendly digital operation panel, and easy maintenance, it offers convenient operation and management for enhanced efficiency. The accuracy and performance of the machine are made possible by applying strict standards in the individual machine components and parts manufacturing processes. High precision main frames (X-, Y-, Z-Axis), bed, table, guide ways and a double column structure provides superior technology in terms of overall machine design and built. C3 class ball screw and the use of linear glass scales in all 3 linear axis are the guarantee for the machines standard 5㎛ positioning precision. Hi-M G1 Pro provides positioning accuracy within 0.005mm and repeatability within ±0.003mm. Developed by Hwacheon software HTDC (Hwacheon Thermal Displacement Control) is applied as standard to ensure high surface quality during prolonged machining. HSK-E50 spindle with 25,000 rpm with built-in motor minimize vibration and noise in high speed cutting and minimize power loss, at the same time maximize cutting efficiency. The high speed machining capabilities of the modern Vertical Machining Center for Graphite Hi-M G1 Pro is increasingly being used in machine shops serving a spectrum of industries.
For S1(O), S2(O) and S3(O), establish the critical distance along the bar at which the hardness starts to fall below that of the fully martensitic structure. For low hardenability steels martensite is produced in a thin layer near the quenched surface. Rank the specimens in order of hardenability.
Capable of resharpening all brands. Center cutting. No hidden charges on flute polishing or cut offs. Radius tolerance ...
The hardenability is measured by quenching one end of a hot bar (Fig.2). The bar is heated to the austenitising temperature, placed on a support and directionally cooled with a water jet. When cold, the specimen is sectioned and hardness measurements are made at intervals along its length. A wide variety of cooling rates and corresponding hardness data are revealed in a single and spectacular test.
The compositions of the steels studied are given in Table 1. Two sets of specimens with these compositions have already been quenched. One of these sets was tempered after quenching (Table II). There are therefore, six sections available for hardness tests along the length of the bars.
5720VS12 Series • Carbide Insert • SDMT12-EN41 • Light Machining of Steels and High-Temperature Alloys - SDMT120412EN41 KCSM40 - Shop Online.
Machininggraphitehazards


For S1(O), S2(O) and S3(O), estimate the critical cooling rates using a simple analysis of the heat flow during quenching (see practical AP1). Assume that the specimen is initially at 900°C and that the quench instantaneously brings one end to a temperature of 50°C. The error function solution then allows the complete thermal history of the bar to be predicted. (thermal diffusivity 10-5 m2 s-1.) The transformation diagram for each steel is provided in Fig.4. For the distance from the quenched end of the bar found experimentally to be the limit of martensite formation, plot on the transformation diagram the predicted (error function) thermal history and see whether this does indeed just miss the nose of the diffusional transformation curve. Calculate the (constant) cooling rate which would also give a curve passing through this point. Comment on any discrepancies.
Shop Single Profile Thread Mill: 1-5 to 1-1/4-5, 5 to 5 TPI, Internal, 5 Flutes, Solid Carbide at MSC Direct top provider of high quality products.
Graphite is a material that presents both challenges and opportunities to manufacturers due to its unique combination of high strength, thermal conductivity, resistance to high heat and corrosion, and machinability. Coupled with the precision achievable through advanced machining techniques, the use of machined graphite components is diverse and span across critical industries. Graphite components contribute to the efficiency, reliability, and performance of systems and products ranging from aerospace, healthcare to mold & die and beyond. Here are some applications of machined graphite components:
2022915 — In addition to milling planes, grooves, gear teeth, threads and spline shafts, milling machines can also process more complex profiles, with ...
Graphitemachining Near me
CCT diagrams are usually plotted with a linear temperature axis and a logarithmic time axis. A constant cooling rate therefore plots as having a continuously increasing gradient. In analysing real experimental results the true thermal history can be plotted even when the cooling rate is not constant.
In 1865, Alexander John Harvey moved to St. John's to open an import/export business similar to an operation his father was running in Nova Scotia. The company ...
The dotted cooling line represents critical cooling conditions. Cooling faster than this avoids all transformations other than martensite. Since this will normally produce a specimen having the highest hardness, the critical cooling rate is a measure of the hardenability of the steel. The hardness generally decreases with decreasing cooling rate, even for microstructures without martensite.
Most heat treatments for steels begin by heating the specimen into the austenite phase field. The resulting austenite is then cooled continuously to room temperature. This is achieved by plunging the specimen into a bath of water or oil, or by removing it from the furnace to cool in air ("normalising"). If very slow cooling is required then the sample is left in the furnace which is switched off. The actual cooling rates may vary in different regions of the sample. These variations may be large since steels are relatively poor conductors of heat (thermal diffusivity of steel is about 10-5 m2 s-1, of copper about 10-4 m2 s-1).
By submitting your particulars, you consent to receive our latest product updates, news and insights and agree to our Privacy Policy.You can unsubscribe anytime via our email link.
There are two primary types of slot milling cutters: disk mills and end mills. Disk mills can be high-speed steel, brazed carbide, and indexable-insert-based.
Machininggraphitefeeds and speeds
By submitting your particulars, you consent to receive our latest product updates, news and insights and agree to our Privacy Policy.
Sponsor Profile. Helix Professional Tools. Alex Bores. SERVICES; PORTFOLIO; CONTACT; WEBSITE. Our Services. View All. Our Work ...
Log in to see product prices and use all features and tools. Register now. Price details. Unit price. After login. Cutting diameter / DC [mm].
Examine the microstructures of the mounted specimen S2(O) at several positions along the length of the bar. Many of the important features of steel microstructures are impossible to see using optical microscopy. You will not, for example, be able to see the carbides that form on tempering martensite. Transmission or scanning electron microscopy has to be used. Examples of such micrographs have been provided. Correlate these observations with the measured hardness profiles. Repeat for specimen S2(X). Explain your observations.
The hardenability may be represented by the critical cooling rate, or the critical distance along the bar at which the hardness (martensite content) starts to drop. It is useful to examine the microstructure and correlate it with the hardness as a function of position along the Jominy bar.
Measure hardness along the length of two Jominy specimens from the same alloy, one in the quenched (O) and the other in the quenched and tempered (X) condition . Results should be shared with other groups to compile hardness profiles for each of the specimens S1, S2 and S3.
(Fe-0.8 wt %C) steel. Curves are plotted for the onset and completion of reactions to form pearlite, bainite and martensite. The former two have the "C" shape because the driving force is small at high temperatures whereas diffusion becomes sluggish at low temperatures. Martensitic transformation is represented by a line parallel to the time axis, since no diffusion is involved and because of the very high rate of growth, the fraction transformed depends only on the temperature.
 18581906093