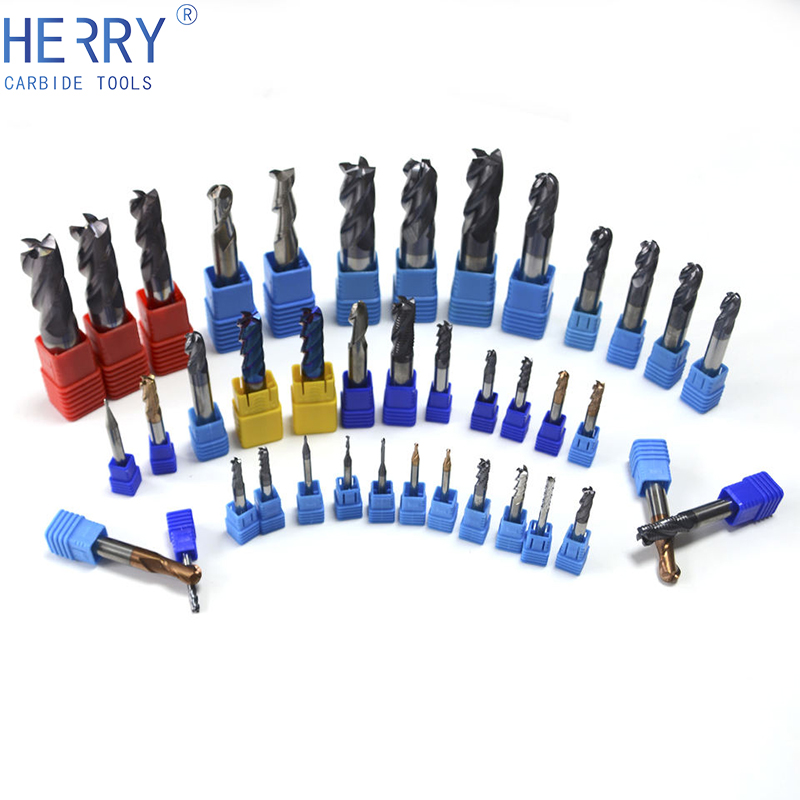
Aluminum Alloy Machining Solutions | Cutting Tools - aluminium cutting tools
A shank is the reamer’s shaft or stem. It’s just next to the flute. When choosing a shank, four major factors must be considered: diameter, type, hardness, and one or two piece construction.
Rpm to sfm formulametric
A reamer is a tool that is used to enlarge or finish holes that have been pre-drilled, bored, or cored in order to provide a high-quality finish and an accurate size. A reamer is a multi-tooth cutter that is used to cut through comparatively little material at once. There are several categories of reamers, each of which is distinguished from the others by the operation, the function, and the form.
When thread milling, calculate feed rate by the formula F = RPM \times T \times N, where T refers to the thread advance per revolution and N is the number of threads engaged. For 500 RPM, a thread advance of 0.02 inch, and 2 threads engaged, calculate F = 500 \times 0.02 \times 2 = 20 inches per minute.
Inches Per Revolution Calculator
If you need to maintain hole diameter tolerances that are more stringent than +/- 0.002 inches, using a reamer is definitely the best option for you. For instance, you might figure out the desired hole size by using our Press Fit Calculator, and then you could use a reamer to get that hole size while staying within the tolerances. The material of the workpiece has an effect on the surface finish that is produced by reaming. The range for steels is 30 to 60 rms, but the range for cast iron is 50 to 80 rms. Aluminum may be given a finish that is as fine as 8 rms by using a PCD reamer.
Feed per Tooth (FPT) is calculated by IPM / RPM / Z, where IPM is the feed rate in inches per minute, RPM is the spindle speed, and Z is the number of teeth in the cutter.
Chucking Reamer with Taper or Parallel Shank (Fluted) is another name for the tool that is often referred to as a machine reamer. The cutting blades of these sorts of reamers are short and parallel, and they have a beveled lead. The bodies of these reamers have large recesses between the shanks. Reamers often have cutting blades that are incorporated into a parallel or taper shank that is used for grasping the tool. The shanks can either be straight or taper, but the flutes themselves are invariably straight.
Distress Guide / Roadway Distresses (AC). Expand All Collapse All. Edge Cracking (7). More: Description · Severity Levels · How to Measure. Loading.
The integration of answers and work in an interactive spreadsheet, coupled with explanations via a chat interface, makes Sourcetable distinctive. This dual-display approach not only enhances usability but also ensures that users grasp the methodology behind the calculations, promoting a deeper learning experience.
When setting up your milling machine, always refer to these formulas and ensure your measurements are accurate to avoid poor finish and tool wear. Adjusting SFM according to material properties will optimize performance and extend tool life.
The reamer can be utilized in a drill press, turret lathe, or screw-cutting machine, depending on the application. It is operated at a modest pace, and the entire cutting process is completed while the flutes are in motion. The flutes travel at varying speeds and directions around the body of the reamer, which is round. Because of this, there is less of an inclination to babble. For work that requires greater precision, the use of a fluted reamer is recommended. Chucking reamers with a straight shank can have a diameter ranging from 0.5 to 32 millimeters, while those with a taper shank can have a diameter ranging from 5 to 32 millimeters.
Sourcetable enhances this process by allowing users to input variables and instantly see the effects on output. Thanks to its user-friendly spreadsheet interface, trial calculations on AI-generated data are smooth and straightforward. This instant feedback helps in fine-tuning operations, thus providing practical insights into the best practices of feed and speed calculations.
To calculate feeds and speeds for your milling operations, you must first understand key components like Surface Feet per Minute (SFM) and Inches per Minute (IPM). SFM is calculated using the formula SFM = (RPM x D) / 3.82, where RPM is the rotation per minute and D is the tool diameter.
There are several specialty carbide reamer possibilities. Chucking reamers, which generally have a straight shank and are used for general purpose reaming, automobile reamers, which are used for heavy-duty structural work, and repair reamers, which are widely used in utility and maintenance applications, are the most popular types of reamers.
In turning, determine the required spindle speed (S) using S = \frac{SFM \times 12}{\pi \times D}, where D is the diameter of the workpiece. For a diameter of 2 inches at 200 SFM, spindle speed calculates as S = \frac{200 \times 12}{\pi \times 2} \approx 382 RPM.
Feed per tooth (FPT), critical for determining feed rate, is calculated as FPT = IPM / (RPM x Z). For adjusted feed per tooth considering chip thinning (AFPT), use the formula AFPT = IPM x sqrt(D / WOC) for WOC less than half the tool diameter.
19652 | Pointed tapered carbide milling cutters d.12 x 22 on 6 mm shank.
By applying these formulas and continuously monitoring the cutting process, you can ensure optimal machine operation and tool life, leading to precise and efficient milling results.
The most common type of reamer is the straight-flute variety. When using the straight flute, chips are not compelled to go in either direction. The arrangement of the coolant that pushes the chips has an effect on it. The chips are propelled forward by the radial coolant that runs via through-holes. When it comes to blind holes, having central coolant can assist in pushing the chips up and out of the hole.
In the cutting process known as reaming, a specialized tool known as a reamer is used to widen an existing hole to a certain diameter while simultaneously creating a smooth finish on the walls of the hole. This is accomplished by the use of the reamer. A milling machine, a lathe, or drill presses are the common types of machines used for reaming. As a finishing operation, reaming is therefore performed. Before the hole can be reamed, it must first be roughed out using a different method, such as drilling. There are other ways to make holes with accurate sizes and a high quality finish on the walls, but reaming is frequently the best choice because of how quickly it can be done and how little it costs.
This reamer might have a straight shank or a taper shank, and it could be operated by hand or by a machine. The reamers feature cutting edges that are tapered to fit a Morse taper, and they have shanks that are either parallel or tapered. The flutes might be spiral or they could be straight. It is possible to purchase the reamers in a package of three, which includes a roughing, a pre-finishing, and a finishing tool. There is a choice in terms of the diameter of the reamers for the finishing.
Adjustment of feeds and speeds is used to decrease time in cut and overall production time, streamlining manufacturing processes.
This reamer has parallel cutting blades that have a taper and a bevel lead integrated with a shank that is the nominal diameter of the cutting edges, and the end of the reamer has a square. The flutes might be spiral or they could be straight. The hand reamer has a square tang, and it is designed to be operated with the hand in order to correctly size the holes. The reamers’ primary objective is to remove the least amount of metal possible between 0.05 and 0.125 millimeters. Because it needs to be easy to start, it has a modest taper towards the end over a distance that is equivalent to its diameter.
Surface grinding speeds depend heavily on material and finish requirements, but typical speeds are around 6000 SFM. For a grinding wheel of 6 inches, use the RPM calculation S = \frac{SFM \times 4}{D}. Thus, S = \frac{6000 \times 4}{6} = 4000 RPM, tailored to achieve precise surface finishes.
3D Machine, Inc. is a leading provider of precision manufacturing solutions, offering a comprehensive range of services including CNC machining, ...
IPRtoIPM calculator
When the width of cut WOC is less than half the diameter of the cutter, adjust the feed per tooth. Use AFPT = IPM * sqrt(D / WOC) to ensure tool stability and efficiency.
Mastering the calculation of feeds and speeds is essential for optimizing machining operations, ensuring efficiency, and extending tool life. Understanding how to properly configure feed and speed variables can lead to significant improvements in machining output. Utilizing a specialized tool like Sourcetable, which is equipped with AI-powered capabilities, simplifies this complex calculation, making precision accessible even to those with minimal technical background.
To optimize the cutting efficiency, calculate the chip load per tooth. It reflects the thickness of the chip each tooth cuts per revolution. The formula is cpt = IPM / RPM / Z.
A machine jig reamer has cutting edges that are short and parallel, and they have a bevel lead. Additionally, there is a guide between the shank and the cutting blades, and it is integrated with a tapered shank that is used for gripping and driving. The flutes are shaped like helicoids. The reamer can be properly located thanks to the plain portion of the body, which slides into a bushing on the jig. The reamer can have a diameter anywhere from 7 to 50 millimeters.
When reaming blind holes, one must use extreme caution. It is imperative that careful thought be given to chip evacuation in order to avoid the chips marring the hole. It is best to never chop a chip more than once. This is the situation that occurs when a chip that has been cut becomes squeezed between the reamer and the hole, and the reamer pushes the chip between the finished hole and the reamer. This leads to a hole that is of low quality or possibly one that is out of tolerance altogether.
The general conditions for using reamers and the results they produce might vary greatly depending on the state of the material, the configuration of the tool, and the equipment. The correct execution of reaming, on the other hand, calls for thorough planning and close attention to detail. Important considerations include the speeds and feeds of the drill as well as the quantity of stock that should be left over after drilling and choosing the appropriate reamer for the task. In most cases, reamers are only designed to cut away between 2% and 3% of the target size.
One issue with reamers is preventing cutting edge chipping. The cutting edges are razor-sharp. Dropping them can damage the edge by leaving a burr or creating a negative cutting edge. This would have an impact on the way any tool cuts, but particularly reamers.
Feeds and speeds calculations inform decisions when comparing different cutting tools, ensuring the selection of the most efficient option.
Reamer flutes are situated at the front of the device. Small chips are removed by passing along the reamer’s flutes. Flutes are classified into two types: straight and helical. Helix is further classified into four types: right hand, left hand, slow, and quick.
Sourcetable takes the math out of any complex calculation. Tell Sourcetable what you want to calculate. Sourcetable AI does the rest. See the step-by-step result in a spreadsheet and visualize your work. No Excel skills required.
The correct RPM for milling can be calculated with the formula RPM = (SFM x 3.82) / D, where SFM stands for Surface Feet per Minute and D for the diameter of the tool.
RPM Toinches per minute Calculator
Calculating the correct feeds and speeds is crucial for optimal milling performance. These parameters determine the efficiency of the cutting process, tool wear, and the quality of the finished part.
Maximize productivity by calculating the MRR using MRR = IPM * WOC * DOC, where WOC is the width of cut, and DOC is the depth of cut.
High speed steel is the most widely utilized material since it is reasonably affordable and works effectively on a wide range of materials. However, many other materials, such as carbide and high cobalt alloy steel, are utilized to create reamers. Carbide is more costly than high speed steel, but when reaming steel, it outlasts it by a factor of ten. The most costly alternative for reaming titanium and stainless steel is high cobalt alloy steel. The cutting fluid that must be used to extend the life of the reamer is determined by the material of the workpiece. Aluminum, brass, stainless steel, and mild steel may all be treated with soluble oil. When reaming cast iron, cold air can be utilized, and synthetic oil can be used with aluminum and plastics.
The material removal rate, calculated by MRR = Feed Rate \times Depth of Cut, is vital for comparing tool performances and improving cycle times.
Straight fluted reamers are utilized for a range of materials and applications in general. The length will be determined by the application. The entering end will be tapered somewhat. This causes the flute to self-center as it enters the hole, while the larger section of the flute will have a constant diameter to allow for the growth. Because right hand spiral reamers have a tendency to suck chips and coolant out of the hole, a right hand kind of helix should never be used on a tapered reamer; otherwise, the reamer may wedge, resulting in catastrophic tool failure.
A hand reamer is designed for manual reaming and usually has a handle. To compensate for the difficulties of beginning a hole by hand power along, it is built with a longer taper or lead in at the front than a machine reamer. It also allows the reamer to begin straight, lowering the chance of breakage.
SolidCAM''s iMachining revolutionary CAM Toolpath and Wizard, provide unbelievable cycle time savings and tool life extension, increasing dramatically the ...
2022111 — Contact Info ... Address: 39 Central St. P.O. Box 783. Rowley, MA 01969.
In spite of the fact that spiral kinds have the potential to improve chip evacuation; the straight-flute reamer is the most cost-effective option. Spirals are more difficult to manufacture than other types of blades because the machine tools need an additional axis in order to grind the blade. As a result, we’ve come up with geometries for the straight flute that either assist shatter the chips or drive them ahead.
Reaming in shipbuilding, structural construction, and plate work can be accomplished with the use of a portable electric or pneumatic tool with a machine bridge reamer, as shown in figures (A) and (B). These are the sorts of reamers that have cutting blades that are parallel to one another. They also include a lengthy lead that is an integrated part of a tapered shank for gripping and driving the reamer. The flutes might be spiral or they could be straight. The reamer has a diameter that can range anywhere from 6.4 to 37 millimeters.
Left-hand spiral reamers have a propensity to push chips and coolant in front of the cut, allowing coolant to enter the hole and the reamer to exit. On tapered reamers, a left hand spiral can be employed to aid prevent grasping and binding. They should not be used in blind hole applications because the chips will pack at the bottom of the hole and prevent the reamer from cutting all the way to the bottom. There are four crucial criteria to consider when choosing a flute: flute diameter and length, pilot diameter and length, number of flutes, and flute depth.
Ben Harvey Construction is a recognized industry leader with over 79 years of experience in providing Preconstruction, Construction Management, and General ...
SFM to RPMDrilling Calculator
Mastering how to calculate feeds and speeds is vital for machining and engineering tasks. Sourcetable, an AI-powered spreadsheet, streamlines these calculations. By simply inputting your material and tool specifications, Sourcetable's AI instantly computes the necessary parameters, ensuring precision and reducing manual errors.
Start with calculating the spindle speed in RPM using the formula RPM = (SFM * 3.82) / D, where SFM is the surface feet per minute and D is the cutter diameter in inches.
For drilling, speed (S) is calculated using the formula S = \frac{12 \times SFM}{\pi \times D}, where D is the drill diameter. For a 0.5 inch drill cutting at 100 SFM, calculate S = \frac{12 \times 100}{\pi \times 0.5} \approx 764 revolutions per minute (RPM).
SFMCalculator turning
To calculate feed rate (F) for milling aluminum, use the formula F = S \times N \times T, where S is the speed in surface feet per minute (SFM), N is the number of teeth on the cutter, and T is the chip load per tooth, typically around 0.005 inch. For an effective cutter speed of 300 SFM with a 4-tooth cutter, the feed rate would be F = 300 \times 4 \times 0.005 = 6 inches per minute.
The reamer’s material is determined by the workpiece material, however reamers may cut practically any metal. To attain exceedingly fine tolerances, the hole must be drilled, rough bored, and then ream. However, with aluminum, a reamer can occasionally remove material straight from a casting. A reamer is intended for precise hole tolerances rather than material removal. However, with aluminum, there are many cases where we can instantly run the reamer into the prefabricated hole and remove the material.
SFM to RPMlathe
Correct settings of feeds and speeds reduce undue stress on tools, thus extending their lifespan and reducing replacement costs.
Cutting edges on reamers are inherently more delicate than those on other cutting instruments, but they are also more important. All cutting edges are fragile, but protecting all reamer edges is important because if you damage even one, it will compromise your size and surface polish. If your cutting edge is chipped, one of those teeth is creating a void within that portion while it is in that cut.
By calculating the optimal feeds and speeds, machining operations can achieve higher productivity and shop efficiency, optimizing throughput.
So, we hope that we have dispelled all of your concerns regarding Carbide Reamers. HUANA carbide reamers are intended for a wide range of reaming applications and materials, including titanium, super alloys, hardened steels, stainless steels, steels, cast iron, graphite, brass & copper, composites, plastics, and wood.
The cutting action is carried out entirely by the beveled edges at the very tip, which differentiates it from the fluted kind. The angle formed by the chamfered cutting edges is 45 degrees. The body, which is fluted, may be inserted into the reamed hole. In order to prevent the body from bending when it is inserted into the hole, it has a little taper and gets narrower towards the shank. A higher amount of metal may be removed with this style of reamer as opposed to using a fluted type.
The feed rate in IPM is computed as IPM = RPM * FPT * Z. Here, FPT stands for feed per tooth, and Z is the number of teeth on the cutter.
Proper calculation of feeds and speeds ensures optimal tool performance, directly affecting the overall output and efficiency of milling operations.
The Metal Removal Rate (MRR) is found by multiplying the feed rate in inches per minute (IPM) by the width of cut (WOC) and the depth of cut (DOC), expressed as MRR = IPM * WOC * DOC.
To find the optimal feed rate, start with the manufacturer's recommended speeds and feeds, then adjust the chip load based on the operation type and further adjust the feed rate based on the machine's maximum RPM.
The Metal Removal Rate (MRR) is significant for evaluating the efficiency of your milling operation. Calculate MRR using MRR = IPM x WOC x DOC.
Understanding how to calculate feeds and speeds is essential for optimizing machine operations in manufacturing processes. Accurately calculating these parameters ensures efficient machining and prolongs the life of your tools. This guide covers the fundamental formulas and considerations necessary for determining the right feed rates and spindle speeds for various materials and cutting tools.
Accurate feeds and speeds prevent undesirable outcomes such as poor surface finish, ensuring high-quality production standards are met.
The shell reamer with an axial hole may be used on an arbor. It also features cutting edges that are almost parallel to one another and a sharpened bevel lead. These kinds of reamers are utilized for the finishing process of huge holes in order to preserve the tool. One arbor may accommodate a variety of different shell sizes when switched out. This results in a reduction in the cost of the solid shank for each individual instance. The shell reamer can either be of the rose chucking type or the fluted kind, depending on whether it is being used for finishing or truing the hole. The flutes might be spiral or they could be straight. The reamer can have a diameter ranging from 24 to 100 millimeters.
Essential tools needed include a method to measure tool diameter and knowledge of the number of teeth in the cutter (Z). You also need the rotations per minute (RPM) and the depth and width of the cut (DOC and WOC).
Reamers with numerous cutting edges typically have anywhere from four to six of these cutting blades. On the other hand, larger-diameter instruments can contain eight or even 12 blades. When there are more cutting edges, the rate of penetration will be higher, and the completed holes will have a tendency to be rounder. Additionally, more edges result in lower chip sizes. You do not want there to be a difficulty with chip evacuation because there are too many flutes. The vast majority of reamers are organized into size ranges, each of which has a certain number of teeth that corresponds to that size range.
M.A.Ford® TuffCut® 3D Multi-Flute Parallel Ball Nose End Mill 6mmx9mmx57mmx6mmSh ALtima® Xtreme.
The SFM is determined based on the material being cut and the cutting tool material. Adapt RPM using SFM = (RPM * D) / 3.82 for any adjustments in cutter diameter or material.
Additionally, we will explore how Sourcetable lets you calculate feeds and speeds and more using its AI-powered spreadsheet assistant, which you can try at app.sourcetable.com/signup.
Page 1. Solid Carbide Reamers Speed & Feed Recommendations. TECHNICAL INFORMATION.
Machine reamers have a tiny lead in, and spiral flutes offer the benefit of automatically cleaning swarf. The reamer and the work piece are pre-aligned, eliminating the chance of the reamer deviating from its intended path. The machine’s steady force guarantees that the cutting begins quickly.
Metric threads ; 0.75, -, 1.2 ; 0.95, -, 1.4.
The reamer should have a left-hand spiral or a straight flute if it is to be used for through-holes. When using the left-hand spiral, the flute’s helix turns to the left, or in a counterclockwise direction. During the process of cutting, the reamer will force the chips to advance through the hole.
Reamers with straight flutes or right-hand spirals are the ones that are recommended for use while drilling blind holes. When using the right-hand spiral, the helix of the flute will move in the right direction, which is clockwise. In order for the reamer to be able to reach the bottom of the hole, it pushes the chip back up through the cut and out the top of the hole.
Whether you're a student or a professional, Sourcetable caters to all. Its AI assistant doesn't just perform calculations; it explains them. This feature is invaluable for learning new concepts or verifying complex calculations at work, enhancing understanding and efficiency.
The geometry of the reamer changes depending on whether the flutes are spiraled to the left or the right, or if they are straight. When it comes to clearing chips, spiral flutes are superior to straight flutes; nevertheless, straight flutes may also be used because the number of chips produced during the reaming process is little.
SFMcalculator
That’s all for now, and thanks for reading. If you like our story, please tell your friends about it. If you have any inquiries or want to order carbide reamers, please contact HUANA..
Carbide reamers are specifically engineered to increase the diameter of an existing hole while maintaining a high level of precision, consistency, and predictability throughout the process.
Experience the power of AI in simplifying complex calculations by trying Sourcetable for free at app.sourcetable.com/signup.
Premium High Speed Steel Drill Bits. HSS Black and Gold Jobber Length. Sold per pack! Call or click anytime! High Performance, High Quality Drill Bits.
The taper reamer may either be driven by hand or by a machine. This features taper cutting edges for holes that fit pins with a taper of I in 50, and it has a parallel or taper shank for gripping and driving the reamer. The taper cutting edges are used to create holes that are compatible with pins. The flutes might be spiral or they could be straight.
Surface Feet per Minute (SFM) can be calculated using the formula SFM = (RPM x D) / 3.82, where RPM is the rotational speed of the spindle in revolutions per minute, and D is the tool diameter.
When working with some substances, you should avoid using a left-hand spiral. Cast iron and some aluminum alloys are examples of these types of materials. Because a spiral flute does not shear the material as well as a straight flute does, it is possible that the spiral will smear the silicon that is present in the aluminum, for instance, when working with high-silicon aluminum..
 18581906093