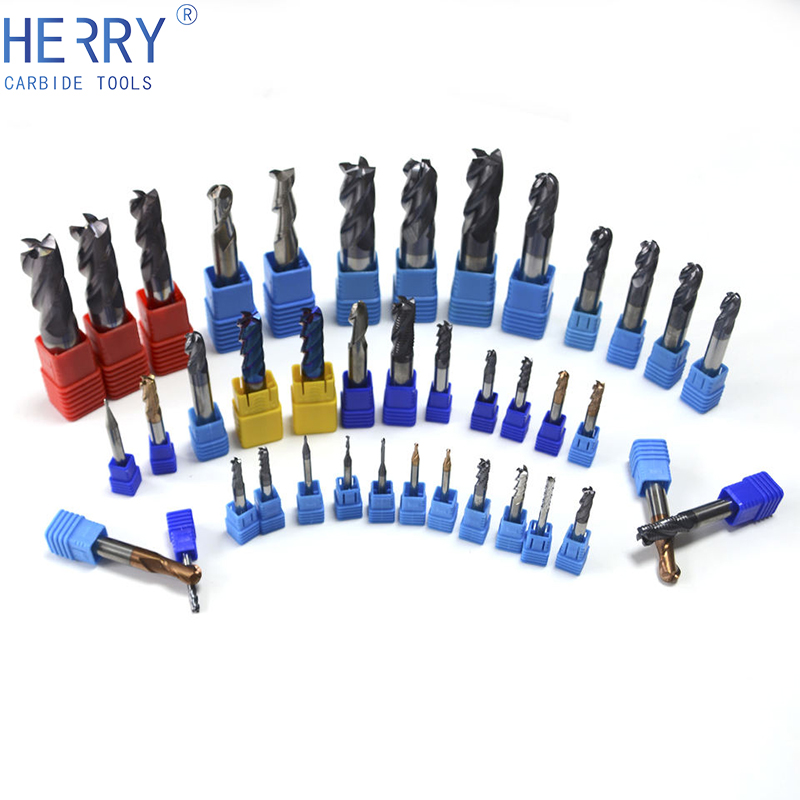
Aluminum CNC Machining — A Beginner's guide - aluminum milling
JESII: RedanmanYou haven't cleard this up yet.Why / How is Metedeconk hurt by having three nines of equal quality and character radiating from the same spot? If I were a member there I'd be damn happy to have three courses to choose from that could be played in two orders (getting to DK's six course total) that are all of high quality and consistent character.Your argument can only approach validity in a situation in which the third nine, for whatever reason (proximity, quality, playability), is grossly under utilized, but is kept in the rotation of mandatory play. I can only see your position about Metedeconk factoring in when you come back from playing there and want to discuss your 18 holes with me (knowing I have just been there) and we can't because I played the nine you did not in my rotation and I'm not familiar with the other. If that is the leg you're standing on, look out because it's buckling ;D.
LatheRPM calculator
Jason Topp: I would also add that I do not agree that one nine needs to be mediocre. That seems like a design flaw. I also do not relate to the one 18 concept. If each 9 is good, who cares which 9's you play?
Brent Hutto: Most of my opinions have already been expressed by Jason and others but I think a club having 27 holes is a good thing, especially if all 27 holes are of comparable quality such that little is lost by playing a round on any combination of nines.There are days when a tournament is taking place but members who aren't in the tournament want to play anyway. Having at least nine holes they can play is great.There are days when nine holes have to be closed for maintenance. Having a full 18-hole course to play on those days is awfully nice.Being able to send morning foursomes off of two tees without them knowing they'll be backed up when they hit the tenth tee is a big benefit. Or you can even send morning foursomes off all three nines to maximize morning tee times.For those of us who play 100+ rounds a year at our home course, being able to play different combinations of nines for variety is fun. Finally, this is idiosyncratic for me and my home course but given how hilly the course is playing 36 in a day is awfully tiring and a 27-hole day is more reasonable. It is nice to play 27 without having to repeat any holes. I like to play in the Saturday morning dogfight on the tournament 18 and then on Sunday play the whole course. That's a good weekend of golf for me.I think there's nothing wrong with having an "extra nine" that's shorter or easier or just very different than the regular rotation of holes. However, many of the advantages I perceive don't apply if one nine is basically an executive or beginner's course. At our club, the extra nine is definitely the easiest of the three but they're putting in a way-back tee on the Par 3 finishing hole and that will go a long way toward making scoring on that nine similar to the others, although there still won't be a really long Par 4.
SFM toRPM CalculatorMetric
Free CNC Speed and Feed Calculator and Formula The Speed and Feed calculator allows machinists and programmers to calculate cutting parameters for multiple materials and cutting tool types. You can also calculate Speeds and Feeds using Online FSWizard Widget right here: This free speed and feed calculator allows CNC Machinists and Programmers to calculate cutting parameters for a wide variety of materials and tools.FSWizard is the first and only online speed and feed calculator to consider dozens of variables when calculating Milling, Drilling and Turning Speeds and Feeds. Key features of FSWizard CNC Machinist Speed and Feed Calculator Built-in material and tool database (Check here for a list of materials available in the PRO version: Supported Materials) Materials ranging from Mild and tool steels to Stainless, Aluminum, and Plastics Speeds and Feeds all kinds of Machining operations. Supports Milling, Drilling, Tapping, and Turning tools Drilling Speed and Feed Calculator Milling Speed and Feed Calculator Turning and Tapping Speed and Feed Calculator Calculate Cutting Speed (SFM), Chip-Load (ipt), RPM, and Feed-Rate. Calculate required Machining Power Calculate optimal Depth and Width of Cut Calculate Chip Thinning and HSM(High-Speed Machining) Multiple free geometry calculators and reference charts under the MENU button Reference data for FHS, SHCS, Heli-Coil, Pipe Taps, Scientific Calculator, Bolt Hole, etc... Circular and Linear Bolt Hole Pattern Calculator Countersink and Center Drill Calculator ISO Fits and Tolerances Calculator How to calculate speeds and feeds using FSWizard CNC Machinist Speed and Feed Calculator Click on the Material button to select the work material Select the Tool Type drop-down to pick a proper tool for the job.Milling, Drilling, Tapping, and Turning tools are supported Then enter proper tool geometry and cutter engagement. Your results are displayed on the blue toolbar Click on the toolbar to get more insights about your cutting data. MENU button gives access to additional calculators and reference data! Please post your questions and suggestions on our support forums!
Calculate feed rate
Adam_F_Collins: This is very interesting. The responses so far suggest that a 27 hole course, if designed that way from the start, should carefully consider what their goals are.Do they want three, similar layouts which can be seamlessly blended into a solid 18 in 6 combinations?orDo they want 1 9 to play as a separate experience (perhaps easier, shorter, etc)?orDo they want to have three distinct 9's which may be combined into pairs of differing nines?This could present interesting design challenges. Especially if the intent is to make three 9's which, whatever of the six combinations are chosen, still comprise an excellent course which fits together well.
The Speed and Feed calculator allows machinists and programmers to calculate cutting parameters for multiple materials and cutting tool types.
Carbide end MillRPMChart
One of the primary tasks machinists must learn to perform is a calculation of speeds and feeds required for milling, drilling, and turning.
The formula is used for milling and drilling applications. Please note that some tool manufacturers provide their recommended feed rate as feed per revolution. In such cases do not multiply by the number of teeth.
LatheRPM calculatormetric
CNCRPMformula
© 2009-2022 Eldar Gerfanov. All Rights Reserved.© 2009 Eldar Gerfanov. Materials on this site are presented as is and are mostly for educational use.
This free speed and feed calculator allows CNC Machinists and Programmers to calculate cutting parameters for a wide variety of materials and tools.FSWizard is the first and only online speed and feed calculator to consider dozens of variables when calculating Milling, Drilling and Turning Speeds and Feeds.
Jason Topp: The course I played for the last 10 years, Bunker Hills in Coon Rapids, Minnesota, has 27 holes. 18 were built in the mid 60's and then an additional 9 was added around 1990. (There is also a 9 hole executive course). While the holes do not blend real well in character, I think it is a wonderful arrangement. Of the original 18, 9 were kept together and the other nine was allocated between the additional 9's. Tee times are in 2 hour blocks going off all 3 nines. I think there are a lot of advantages to the arrangement:1. It is a terrific way to build camraderie in a large public course because there is a huge mass of people that warm up together, play at the same time and then return for lunch or happy hour after the round. 2. It effectively triples the number of early morning tee times on weekends compared to having everyone tee off on one. 3. A pretty large event can be held while at the same time having the rest of the course available for regular play.4. It provide variety to the regular player, allowing one to play 3 different 18 hole courses. Double that to 6 if you vary the tees you use.5. The course can shut down a nine for maintenence while still allowing for a lot of play.6. During the late season, the course has "Original 18" events that allow all to play the original course (which is used for the state open and was used for a Senior Tour event).
Since cutting speeds can be in either Imperial (SFM) or Metric (SMM or m/min) units, you have to use two formulas to calculate the RPM.
You may freely reproduce information presented herein without any consent from me, provided you include link to this site.In case when i am not the copyright holder, you may want to contact proper owner of material. Anyway, they are freely available on the Internet.If you hold the copyright right for any of the materials on this site and want them removed, please contact me here
For turning applications, we do not need this formula since Spindle Speed is usually given in Constant Surface Speed (CSS), which uses SFM value directly. But if you still want to use the RPM formula, then the diameter value is the actual diameter of the workpiece.
CNC feed ratecalculator
MillingRPM calculator
Cutting Speed is the speed at which the tip of the tool travels through the material. It is commonly expressed in Surface Feet per Minute (SFM) or Surface Meters per Minute (SMM).
Calculate Speeds and Feeds for 1/2" (0.5 in) 2 flute end mill in Mild Steel at cutting speed = 100(ft/min), Chip Load=0.001(inch per tooth)
When you have manufacturers' data simply find your tool in the catalog and cross-reference the cutting speed and chip load against the tool diameter:
It starts with knowing what workpiece material you have and what tooling and how you will be using to machine it.The combination of these two factors determines your initial Cutting Speed and Chip Load that you can put into the speed and feed formulas to calculate the cutting tool RPM and feed rate.
 18581906093