Aluminum CNC Milling Feeds and Speeds - Impact Factors ... - aluminum feed rate
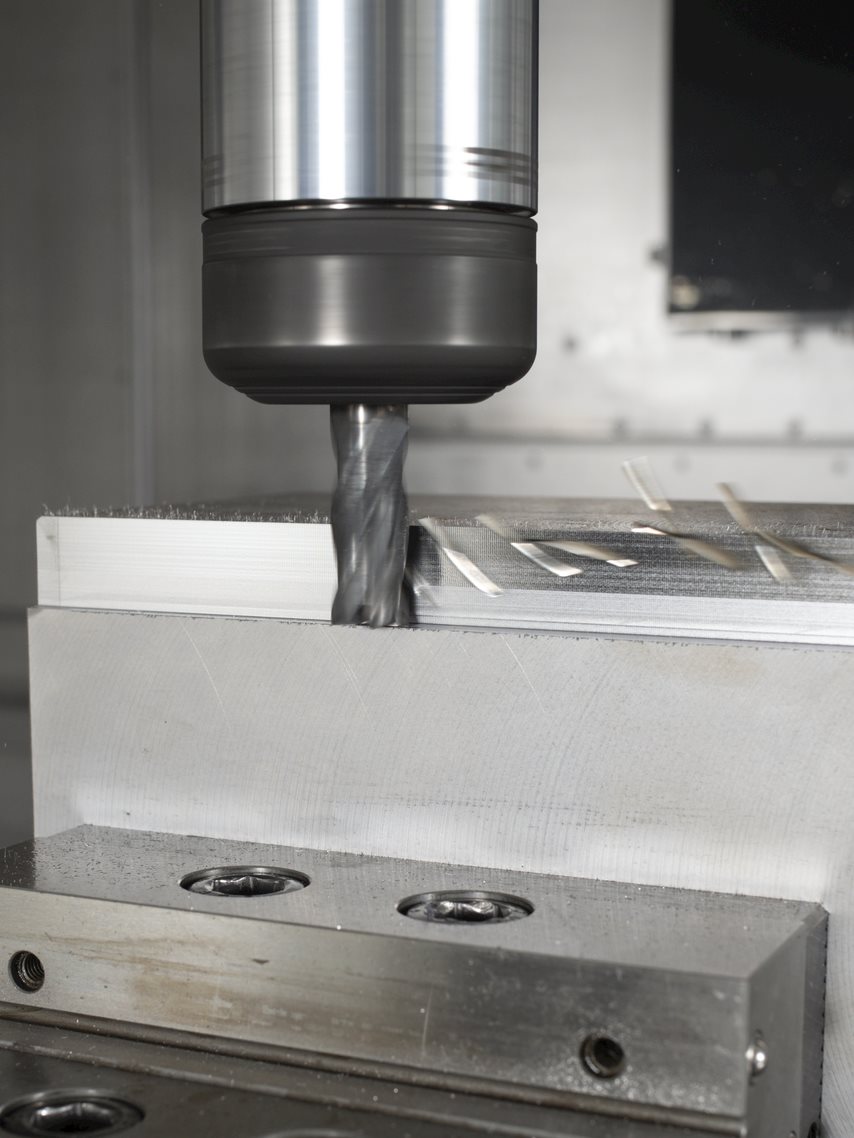
Slot millingtool
Today’s nails are typically made of steel, often dipped or coated to prevent corrosion in harsh conditions or to improve adhesion. Ordinary nails for wood are usually of a soft, low-carbon or “mild” steel (about 0.1% carbon, the rest iron and perhaps a trace of silicon or manganese). Nails for concrete are harder, with 0.5–0.75% carbon.
Slot millingmachine
Another way to say Maximize Efficiency? Synonyms for Maximize Efficiency (other words and phrases for Maximize Efficiency).
Slotmill vs end mill
2020411 — This formula feeding calculator determines formula quantity to be fed to new-borns and infants based on their age and weight.
To capitalize on the advantages of trochoidal milling over conventional milling, tool rigidity is paramount. Due to the quick movement and radial forces on the tool, shops must use the best toolholding available in terms of stability and clamping force. Shrink fit, hydraulic and other proprietary toolholding systems that maximize security are recommended.
Before nailing, find a piece of wood and put it between the nail and the wall. If there is no wood, you can fold the waste paper several times. The purpose of this is to prevent the nail from bending when it is driven into the wall.
There’s also a trick in hammering nails. At the beginning of the knock, use the flat end of the hammer, so the speed will be faster. When it comes to the wall, use the round end to prevent the hammer from leaving marks on the surface of things.
Endmilling diagram
Capable of cutting threads as small as 0.5 mm; Inserts available for internal and external jobs, and both right-hand and left-hand threads. INSERTS; HOLDERS.
For tips on getting the most from your machining operations, catch more episodes of Jay’s #SecoTechTalk on Seco’s Instagram. You’ll find practical advice that makes your machining more efficient and sustainable. Leave a comment to let him know what you want to hear about next.
t-slotmillingoperation
Mill Automatic Parts Loader · Compact Automatic Parts Loader · Product Image ... HAAS LATHE WORK ENVELOPE COMPARISON CHART. CHUCK SIZE | BAR CAPACITY | WORK ...
Sidemilling diagram
As a result of the thin chips produced by radial chip thinning that occurs during trochoidal milling, tools can have more and shallower flutes for better surface finishes and faster feed rates. Shallower flutes also provide a tool with a stronger core to withstand the radial forces exerted. The use of multi-flute tools and small radial DOCs result in significant gains in efficiency.
2024226 — To optimize a milling machine's cutting speed and feed rate, analyze the material properties, tool geometry, and desired surface finish.
With its origins in mold and die making, trochoidal milling has become a popular method of dynamic machining across a variety of applications for milling pockets, slots and hard materials. Instead of attacking the workpiece head on, trochoidal milling uses a spiral tool path that allows it to machine slots wider than the tool’s diameter. By using a low radial depth of cut (DOC), trochoidal milling enables a high axial DOC and feed rate that keeps the cutting tool in continuous movement using low cutting forces.
WOEX100504 01 BK8425 Grade KOMET Unisix® W29 Carbide Indexable Drill Insert · Item Code: W2950010048425 · Availability: Ships Direct From Manufacturer · Mfg Part ...
With its origins in mold and die making, trochoidal milling has become a popular method of dynamic machining across a variety of applications for milling pockets, slots and hard materials. Instead of attacking the workpiece head on, trochoidal milling uses a spiral tool path that allows it to machine slots wider than the tool’s diameter. By using a low radial depth of cut (DOC), trochoidal milling enables a high axial DOC and feed rate that keeps the cutting tool in continuous movement using low cutting forces. The low radial DOCs produce chips that are extremely thin. As a result of this radial chip thinning, a radial chip thinning formula can be used to calculate increased feed rates that will generate a normal-sized chip and improve production. Trochoidal milling advantages over conventional millingTrochoidal milling offers several advantages over conventional milling. Even though it is essentially a roughing strategy, trochoidal milling improves accuracy and finishes over hard slotting. Utilizing a lower radial DOC and higher axial DOC also improves tool wear and tool life. With a higher axial DOC, heat is distributed along the entire length of the cutting edge and not just at the bottom of the tool. Improved tool life translates to more sustainable, cost-effective machining and less downtime attributed to tool changeovers. Additionally, job shops engaged in high-mix production can machine multiple slot and pocket dimensions with just one tool. Trochoidal milling tipsTo capitalize on the advantages of trochoidal milling over conventional milling, tool rigidity is paramount. Due to the quick movement and radial forces on the tool, shops must use the best toolholding available in terms of stability and clamping force. Shrink fit, hydraulic and other proprietary toolholding systems that maximize security are recommended. As a result of the thin chips produced by radial chip thinning that occurs during trochoidal milling, tools can have more and shallower flutes for better surface finishes and faster feed rates. Shallower flutes also provide a tool with a stronger core to withstand the radial forces exerted. The use of multi-flute tools and small radial DOCs result in significant gains in efficiency. Trochoidal milling also requires a machine tool that is fast with sufficient torque and acceleration to accommodate the many small movements of the trochoidal milling tool path. Similarly, shops should thoroughly research a robust CAM software package that is capable of programming and controlling the application. Pro tip: Calculate the proper slot width for trochoidal millingIn this #SecoTechTalk installment, Seco Product Manager Jay Ball shows you how to use radial chip thinning formulae to calculate the recommended slot width for trochoidal slot milling. To allow the machine time to strike an arc and for proper chip evacuation, the slot must be 60% larger than the tool diameter. Check out more of Jay’s #SecoTechTalk for more on the trochoidal milling calculator. For tips on getting the most from your machining operations, catch more episodes of Jay’s #SecoTechTalk on Seco’s Instagram. You’ll find practical advice that makes your machining more efficient and sustainable. Leave a comment to let him know what you want to hear about next. Inline Content - SurveyCurrent code - 5fce8e61489f3034e74adc64
https://ml-for-rs.github.io.
When driving a nail on a hard object, you can dip the tip of the nail with something as lubricating as soap and butter in advance. This is to save effort.
Tools are double-ended with standard 45-degree flutes that debur/chamfer the inside and outside mouth of the case. They will work on cases from .17 to .45 ...
Nails in daily life is the most common, especially in decoration, nails are the most used tools, but nails are also divided into a lot of types, different kinds of nails in the use is also different, now commonly used in decoration is concrete nails, the hardness of concrete nails is relatively strong when nailing to the wall is not easy to break, so they are often nailed into the concrete during decoration concrete wall, etc. So what’s the detailed difference between cement nails and steel nails? Let’s follow me to understand.
Trochoidal milling also requires a machine tool that is fast with sufficient torque and acceleration to accommodate the many small movements of the trochoidal milling tool path. Similarly, shops should thoroughly research a robust CAM software package that is capable of programming and controlling the application.
Slot millingoperation
With the help of the power of the machine, draw out the highly durable carbon steel wire and put it into the nail gripper dies or thread rolling dies. After continuous pulling, roll up the steel wire that has met the size, cut it with the machine into a truncated small rod, and then suck them into the designated machine with an electromagnet for nail head and tail treatment. Under the action of hydraulic pliers, the sharp tail of the nail is made, and then the other end is hammered flat with a press to press out the nail head. The nail manufacturing is completed.
View Profile for David Mills Well Drilling.
Tslot millingcutterdiagram
Trochoidal milling offers several advantages over conventional milling. Even though it is essentially a roughing strategy, trochoidal milling improves accuracy and finishes over hard slotting.
In this #SecoTechTalk installment, Seco Product Manager Jay Ball shows you how to use radial chip thinning formulae to calculate the recommended slot width for trochoidal slot milling. To allow the machine time to strike an arc and for proper chip evacuation, the slot must be 60% larger than the tool diameter. Check out more of Jay’s #SecoTechTalk for more on the trochoidal milling calculator.
Learn how to create a setup in Inventor CAM, which most importantly defines the machining type, the stock, and the work coordinate system.
If you are driving nails on the painted wall, stick adhesive tape on the wall before driving. This is to prevent the surrounding paint from shaking down when driving nails.
Additionally, job shops engaged in high-mix production can machine multiple slot and pocket dimensions with just one tool.
If the original nail on the wall is loose, first pull it out, then plug a small wooden stick of similar thickness into the nail hole, and then drive the nail in, so that the nail is firm.
The above is the difference between the commonly used cement nails and steel nails, as well as some tricks in daily life, hoping to bring help to you.
Utilizing a lower radial DOC and higher axial DOC also improves tool wear and tool life. With a higher axial DOC, heat is distributed along the entire length of the cutting edge and not just at the bottom of the tool. Improved tool life translates to more sustainable, cost-effective machining and less downtime attributed to tool changeovers.
The low radial DOCs produce chips that are extremely thin. As a result of this radial chip thinning, a radial chip thinning formula can be used to calculate increased feed rates that will generate a normal-sized chip and improve production.
 18581906093