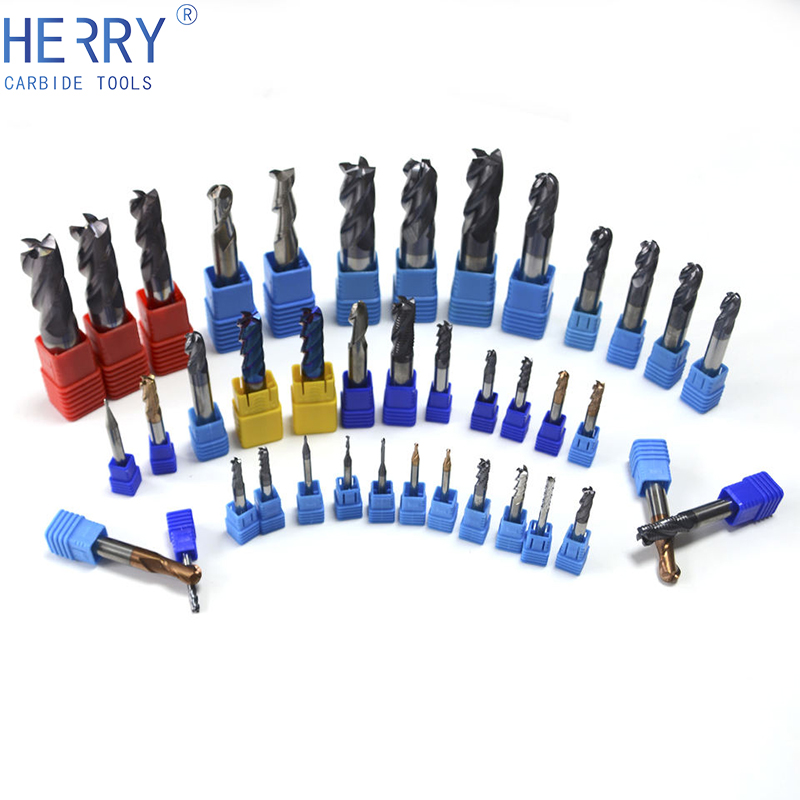
Aluminum Milling Inserts - tungsten carbide milling insert
Sep 5, 2019 — Down milling: refers to the cutting speed direction of the cutter is the same as the moving direction of the workpiece. Up milling: refers to ...
Using Chemical Vapor Deposition coating technology, CVD coated carbide grades provide stable, efficient machining at high speeds or for heavy interrupted ...
In this article, Heygo will explain more about the following thread tap types: straight flute taps, fluted spiral taps, spiral point taps, and forming taps.
A thread tap is a tapping tool for processing internal threads with grooves along the axial direction. Also called screw tap. The thread taps are used for tapping or cutting various medium and small size internal threads in metal.
Most thread taps are made of high-speed steel or carbide and are used to process various metals. The thread tapping tools have a simple structure and are easy to use, and they can be operated manually tap or on a machine tap.
Tolerance stack up analysisPDF
Spiral flute taps are mostly used for drilling blind holes in CNC machining centers. Spiral flute taps are divided into left-hand spiral flute taps, and right-hand spiral flute taps are mainly developed to solve deep hole thread tapping. The “deep hole” here refers to a threaded hole with a depth-to-diameter ratio> 2. According to different working conditions, different spiral angles are used. The common ones are 15° and 42° right-handed.
Tolerance stack up analysisexample
Like carbide tools gradually replacing high-speed steel tools in CNC turning, carbide taps have also begun to be used more for threaded hole processing.
Tapping metal threads is a relatively tricky machining process because the thread tap is almost buried in the workpiece for cutting. Its processing load per tooth is more significant than other tools. The contact surface of the tap with the workpiece along the thread is huge. When cutting the thread, It must contain and exclude chips. Therefore, it can be said that the tap works under very harsh conditions.
How to do a tolerance stack up analysisexample
The thread tap size specifications include metric taps and inch taps. For example, metric taps M8*1.2, where M is the triangular thread code, 8 represents the tap’s diameter, and 1.2 means the tap’s pitch in mm. For example, for the inch tap 5/16-18, the tap’s diameter is 5/16 inches, and the 18 behind it means there are 18 threads in 1 inch.
Spiral point taps are also called tip taps, characterized by opening a wedge-shaped groove on the head of the straight flute tap, changing the cutting cone’s shape, and the chips are discharged forward cutting. It is suitable for through-hole thread and deep thread tapping.
Tolerance stack upcalculator
3. When tapping on steel workpieces, add cutting fluid. When tapping on cast iron workpieces, add a little kerosene; after using the first tap, the tap must be screwed into the screw hole when using the second or third tap.
Strong versatility means weak pertinence. Therefore, straight fluted taps are not suitable for tapping plastic materials with strong ductility (such as stainless steel, titanium alloy, etc.). Significantly when the thread depth of this kind of material exceeds two times the diameter, it is not recommended.
4. When threading, the end of the workpiece should be chamfered, and the end face of the threading should be perpendicular to the axis of the workpiece; the axial pressure should be applied at the beginning of the threading, and the rotating force should be correspondingly larger; when the threading is cutting the thread on the workpiece, Don’t put more pressure.
Compared with HSS taps, carbide taps have higher hardness and greater brittleness. Use carbide taps to tap There is a problem with chip disposal. Nevertheless, cemented carbide taps are very useful in tapping threads in cast iron, aluminum alloy materials, and the main form of damage to the taps is mechanical wear.
1. When tapping, the end hole should be chamfered; the tap should be coaxial with the workpiece’s hole; axial pressure should be applied at the beginning of tapping to make the tap cut in. After a few turns, no axial force is needed.
How to do a tolerance stack up analysistemplate
PCE27v4 - TAFS 23 – Ruminant Feed Calculations 052517. 1. A Greener World Technical Advice Fact Sheet No. 23. Guidance for Calculating Ruminant Feed and Forage.
20201230 — The metal exception is copper, which although is corrosion-resistant, is not considered a noble metal unless you go by the strict definition of ...
Although resistant to abrasives, solid carbide, like other tap materials, tends to become brittle and cannot withstand vibration. Therefore, solid carbide taps should only be used with modern high-speed cutting equipment with minimal vibration during operation.
BANKA is a leading and one of the oldest Indian company in machine tool manufacturing with an impressive line-up of accurate and rigid Lathe Machines.
Tolerance stack up analysisExcel
Show more filters ... · Cantilever length (LPR): 56.50 mm · Functional length (LF): 0.00 mm · Function height (HF): 20.00 mm · Functional width (WF): 17.50 mm ...
3, TiN (Titanium Nitride)-golden appearance, using PVD coating process, easy to produce, low cost, wide application range, generally can increase the tap’s life by about 300%. TiN Thread taps also provide additional resistance to heat damage and reduces friction in the tap head, which offers high lubricity and increases chip flow in softer materials.
For tapping internal threads in cast iron or other ductile materials, nitride/oxide treatment HSS can be used, which helps prevent tap wear. Other coatings, such as titanium nitride (or aluminum titanium nitride), can also improve the tap’s durability.
Commonly used materials for thread taps are various high-speed steels(HSS) and cemented carbides. Its hardness varies according to different materials—ordinary high-speed steel: 62~64HRC, cobalt-containing high-speed steel: 67~68HRC, and cemented carbide: 69~79HRC.
The 11IRA60 Threading Insert is a carbide internal threading insert, right-handed which is ideal for thread turning and tool boring.
5, CH (Amorphous Carbon)-Amorphous carbon similar to diamond. The appearance is dark gray. Using the PVD process, the coating thickness is 1-2μm, and the hardness is about 2500HV. Mainly used for tapping of non-ferrous metals and aluminum and its alloy materials.
The tap’s geometry mentioned above, coupled with a unique coating surface (like TiN, TiCN, CrN, or TiAlN), can significantly increase the tap’s life. These heat-resistant, smooth coatings reduce cutting forces and allow tapping at higher cutting speeds. The development of newer high-performance taps has dramatically promoted the increase in machine tool spindles’ speed and power.
2024510 — Bevels and chamfers are solid options for anyone looking to create an edge – whether in woodwork, metalwork, and much more.
According to different materials, ordinary high-speed steel: 62~64HRC, cobalt-containing high-speed steel: 67~68HRC, but the main “components” include high-carbon tool steel, tungsten, chromium, vanadium, and iron.
The machine taps are marked with the code of the tolerance zone of the pitch diameter: H1, H2, and H3 respectively indicate the different positions of the tolerance zone, but the tolerance values are equal. The tolerance zone code of hand taps is H4, the tolerance value, pitch, and angle error are larger than machine taps, and the material, heat treatment, and production process are not as good as machine taps. H4 may not be marked as required. The internal thread tolerance zone grades that can be processed by the tap pitch tolerance zone are as follows:
Solid carbide taps can process many different materials, such as tapping threads in alloy steel, aluminum, brass, carbon steel, cast iron, copper, Hardened steel, Inconel, Nickel (and other cemented carbide), Sintered material, stainless steel, and titanium.
Straight flute taps are the most commonly used type of thread tap. The Straight taps are made of high-hardness materials such as high-speed steel and cemented carbide. Straight flute taps can have 2, 4, and 6 teeth in the cutting cone. The cutting speed is slower. The long shank straight flute tap is used for through holes, and the short shank Straight taps are used for blind holes.
As the automobile industry processes, many cast iron and aluminum alloy parts, carbide taps are used to obtain long tool life. When processing workpieces of these materials, carbide taps have a longer life than high-speed steel taps, in the automotive industry, the reduction of the tool change time of the wire push is an essential factor, and the long life of the carbide wire push will minimize the tool change time.
There are lots of different types of thread taps that can be used for tapping internal threads in metal, but do you know how to choose these different thread tap types for different applications? And what else will help you choose a suitable thread tap for your tapping working? This article will clearly help you answer these questions:
How to do a tolerance stack up analysisin excel
2. After the calibrated part of the tap enters the screw hole. It will return 1/4 or 1/2 turn every half turn to one turn so that the chips will be broken and then tap down; when tapping the through-hole, it must be withdrawn frequently Tap for chip removal.
6. The workpiece should be firmly fixed on the clamps and fixtures; when the tap is broken, do not touch the broken place with your hands, use a clamp or punch to remove it, and wear protective goggles when the wire is broken.
How tocalculatetolerance stack up
We have openings for Drivers, Mechanics, Customer Service and Helpers. At E.L. Harvey - Westborough, we're proud to be a different kind of company with a ...
1, TiCN (Titanium Carbon Nitride)-blue-gray, PVD coating process, multilayer coating with a layered structure. TiCN-coated thread taps are generally used for tapping difficult-to-process materials, such as tapping threads in quenched and tempered steel, wear-resistant steel, etc.
Most of the thread tap manufacturers provide coated taps, which have greatly improved the service life and cut uncoated taps. The taps of unequal diameter design have reasonable cutting load distribution, high processing quality, but high manufacturing cost.

The spiral flute taps are not competent large-size thread tapping work. When tapping large-size threads, especially high-tensile-strength materials, the torque required to use spiral flute taps will be enormous. Such a vast torque can easily cause the tap to collapse or even break. Therefore, the commonly used spiral flute tap specifications are between M3-M36.
4, Vap (Vaporized)-high-temperature oxidation treatment, that is, the tap is placed in 530℃ high-temperature water vapor to generate black Fe3O4 on the surface of the tap. The primary function is to absorb cutting fluid to increase lubrication performance and inhibit cutting. The generation and adhesion of nodules have a wide range of applications, especially in the tapping of medium and low-strength steels. The effect is particularly significant;
High-speed steel (HSS) is a more popular tap making material. Although high-speed steel taps have the disadvantages of high temperature and vibration, they can still maintain their integrity during tapping. There are various types of high-speed steel with different hardnesses.
Forming taps are a kind of chipless processing technology that uses metal forming to process internal threads, called screw taps.
High-Precision Fine-Tuning Fine Boring Tool EWN CNC Boring Bar High-Precision BT40 Adjustable Boring Head. High crystal fine-tuning fine boring tool.
Because it is extrusion molding, there are fine grooves on the top of the processed internal thread, so it is not suitable for work types that require high tightness.
2, TiAlN (Titanium Aluminum Nitride)-The appearance is purple and black. It also uses PVD technology. TiAlN coated taps are mainly used to tapping metal threads in castings, such as tapping threads in cast iron and cast aluminum wear-resistant materials and high temperature and high-speed cutting general cooling performance is not good. This coating is the first choice;
Unlike the above three cutting taps, the tapping method of forming taps is to extrude the bottom hole’s internal thread shape through the plastic deformation of the material itself. Therefore, the target processing material cannot be too hard.
 18581906093