Aluminum Milling Speeds For Optimal Metal Removal - milling speed for aluminum
Circular sawblade sharpening near me
Isolated components are generated through the forging process because grain structure and the metal flow of the material can be effortlessly controlled. Forged objects, parts, or components come with exceptional strength and toughness, and therefore, they are considered to be extremely reliable for highly hostile, stressed, demanding, and critical applications.
Depending upon the type of material to be forged, the temperature range in hot forging might drastically vary. The hot forging process starts with the die heating process so that temperature loss can be avoided during the operation, and also to make sure that no crystallization takes place until the forming task gets completed. Any metal when heated gets more ductile, and at the point when hot metal is squeezed by the dies, a more refined grain is achieved in the structure, resulting in more yield strength as well as ductility.
Sharpen circular sawblade with dremel
Caparo holds extensive know-how of product understanding, new-age technology, ultramodern CAD/CAM infrastructure, and outstanding product development expertise. All these things together empower the company to come up with innovation-inspired designs. The company’s design team makes sure that each and every design is integrated with 3D model simulation for better size, weight, and performance optimization.
Some of the most prominent components forged by the top steel forging manufacturers for the automotive industry include the following:
Used for the first time around 4000 B.C., forging has been identified as one of the oldest metallurgical procedures. At that time, this procedure was used to make jewelry, coins, and a large number of utensils by hammering different metals using tools made from stones. Modern forging manufacturers across the country and the world still work on the same principles but the age-old hammers and other tools are now replaced with ultramodern high-powered hammers and mechanical presses. Some of the most commonly forged and used products include the following:
How tosharpen circular sawblades by hand
Cold forging compresses different metals at an ambient temperature, whereas hot forging calls for a high level of heat. The intensity of heat is what distinguishes cold and hot forgings. Hot forging offers the feasibility of creating more complicated and sophisticated shapes in comparison to cold forging.
Sawblade sharpening jig
Sharpen circular sawblade with grinder
Metal forging is a group of different forming processes in which a billet is deformed plastically between certain tooling fixtures through the application of compression force. Forging can be carried out in a wide range of temperature ranges including isothermal, warm, hot, and cold. Forging, as one of the most significant metal processing processes, holds utmost importance, particularly in the iron and steel manufacturing industry.
As a rule, tooth faces are sharpened straight; however sometimes they are also sharpened at an angle. Tooth face machining also includes hollow face grinding. This is carried out using a grinding point at high speed. However, this method cannot be used for every circular saw blade. There must be a certain amount of chip space available in order to be able to sharpen the tooth face using peripheral grinding. In particular, it must be ensured that the grinding point is positioned exactly in the middle of the saw blade diameter and the cutting width.
Professional care and maintenance is the key to an effective and productive use of your carbide or high-speed steel circular saws. With the correct grinding technique and machine this is no problem.
Warm forging, as a manufacturing method, is getting immensely popular across the globe owing to its cost-saving advantages. As for the temperature range of warm forging of steel, it is about 800 to 1,800 degrees Fahrenheit, depending upon the alloy. Nevertheless, the narrower range from 1,000 to 1,330 degrees Fahrenheit is considered a better commercial potential for the warm forging of steel alloys. When compared to cold forging, warm forging scores heavily due to various advantageous reasons. Some of them include the following:
How tosharpen sawblades
Sharpen circular sawblade with file
As a leading steel forging manufacturer in India, Caparo is backed by 3 Closed Die Hot Forging Press Lines that range from 1600 Tons to 6300 Tons. These lines can produce press forgings weighing from 0.5 kg to 50kgs. All press lines work on a unique concept of the Single-Piece Flow Production system, through which the billet or workpiece shearing takes place only when the product is required at the end of the cycle. This renders the highest productivity with no chances of the mix-up of cut metal.
Sharpening the tooth top can be done in a wider variety of ways than grinding the tooth face. The geometries can be designed to be straight to almost round, depending on the range of applications of the carbide-tipped circular saw blade. The tooth top is sharpened with a face grinding or peripheral grinding process. Sharpening using a face grinding process is particularly time-saving. Using this method, the grinding wheel must simply be turned through a certain angle in order to produce a wide range of tooth shapes (such as trapezoidal, roof, etc.). Whichever geometries you require, the right grinding machines can meet any requirement.
In cold forging, the material is formed into the desired shape through the displacement methodology. At a moderate temperature, a compressive force constricts the metal between a die and a punch till it gets in the outlines of the die. Some of the most common examples of cold forging include the following:
Established in the year 2009, Caparo Forging manufactures a comprehensive range of forged and machined products for a variety of automotive and non-automotive applications. The company has a gigantic capacity to produce 8400 MT of finished products per annum. It is the most preferred partner for leading names in the industry such as Iljin, Daimler, Rane TRW, Woosu, AVTEC, Royal Enfield, Delphi TVS, CAT, Simpson & Co. Ltd, and many more.
We detected, that your browser supports another language than the called one. This page is also available in your language! Would you switch to this page in your language?
The flanks of a saw tooth are ground to a tapered shape in the cutting and feed direction, in order to prevent the cutting edges from pressing into the material. The precision of the tooth flanks significantly influences the surface quality. Grinding is carried out once when the circular saw is manufactured using a face grinding or peripheral grinding process.
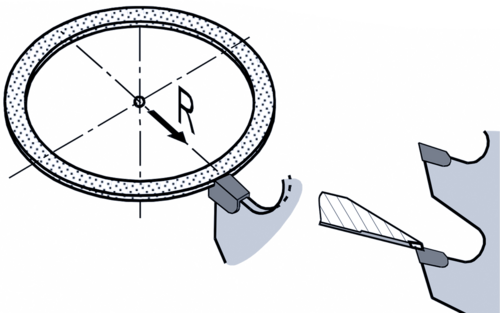
The body of carbide-tipped circular saw blades consists of pretensioned tool steel. Raw saws have a tip groove, onto which no cutting plates made of carbide can be precisely soldered. Soldering takes place during production using automatic machines. However, for service work, it is carried out manually with the aid of machines, as this only involves replacing individual broken cutting edges. Silver or a sandwich alloy is used as solder. Resistive-soldering equipment is used most frequently during repairs on circular saw blades. Defective teeth can also be removed with this equipment.
 18581906093