American National Carbide Co - Company Profile and News - american national carbide
TURNING TOOLS LATHE TOOLS HSS CARBIDE INSERTS PCD CBN INSERTS. ... TOOL HOLDER - DWLNR 2525M 08 Sandvik Coromant DWLNR 2525M 08 Turning Insert Holder, ..
There are single-row and multi-row thread mills. A single row has one row of teeth. It's virtues are lower cutting forces (beneficial on large threads) and the flexibility to do many thread sizes.
CNC Thread Milling is possible because CNC Machines allow us to program Helical Interpolation. This allows the cutter to follow a helical path that corresponds to the thread’s helix:
A Single profile thread mill only has teeth to do one thread at a time. Therefore, they can be used for a wide variety of threads by varying the depth of cut and the pitch of the thread helix. But a Spiral Flute Thread Mill can only do one helix pitch because the distance between teeth is fixed.
NYC CNCthreadmillcalculator
That’s quite a long list of advantages for carbide thread mills that may make them perfect for your application instead of tapping.
A Spiral Flute Thread Mill can cut faster than Single Profile (or Single Point) Thread Mills because more than one thread can be cut by the multiple rows of teeth. The same Spiral Flute Thread Mill can cut lefthand or right hand threads and it can vary the diameter of the threads, but they are limited to a single thread pitch governed by the spacing of their teeth.
Many thread mill manufacturers offer versions with integrated countersinks at the top of the thread mill to eliminate the need for a tool change where countersinking or chamfering is desired (almost always!).
Threadcutting speed
Thread milling is an alternative machining solution to tapping on CNC machines for cutting threads. It works by moving a cutter along a helical path that corresponds to the thread's helix.
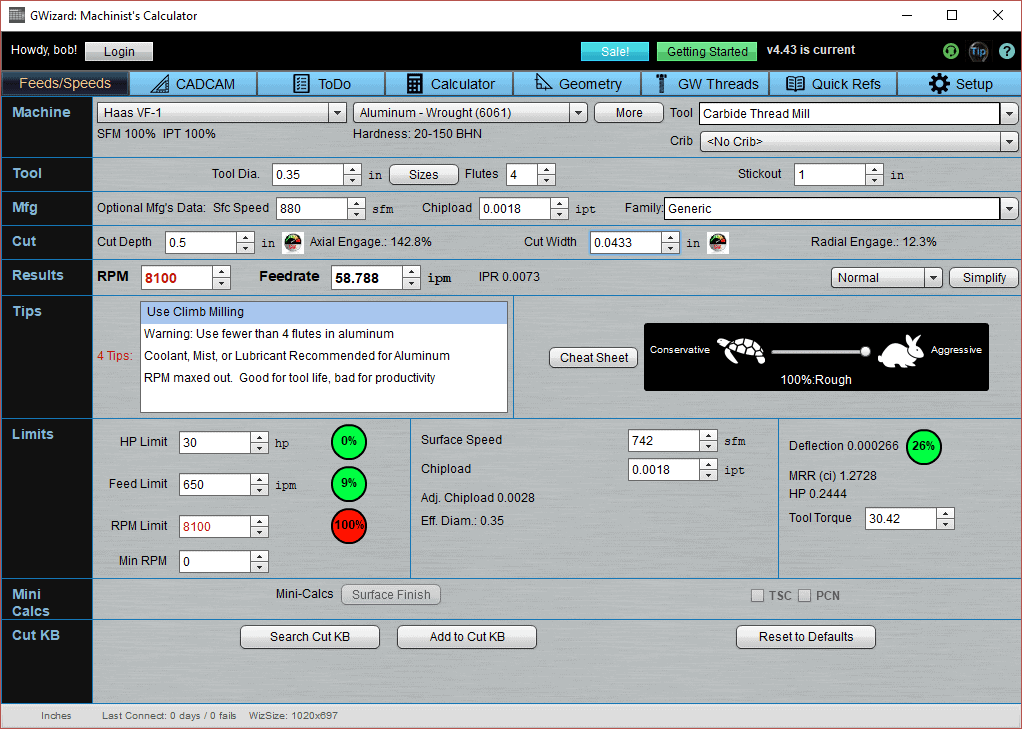
Let’s say we’re going to cut a 1/2-20 internal thread. Our rules for selecting a thread mill require no more than 70% of hole diameter for thread mill diameter. So we want a thread mill that is no more than 0.350″ in diameter. I like Lakeshore Carbide’s tooling (Carl is great to deal with), so I will go choose a thread mill from his online catalog.
Threaddepthcalculator
202268 — CNC Machining; Key Differences Between 3D Printing and CNC Milling; Subtractive vs. Additive Manufacturing; Key Decision Factors When Choosing a ...
If we wanted to take it a little easier, we can dial back the Tortoise-Hare slider more to the Tortoise side–whatever feels right for the situation.
That being the case, you might wonder why anyone ever uses Thread Mills? There are a number of advantages it has over Tapping that often make it the preferred choice of machining solutions include the following technical tips:
There are a number of reasons to thread mill instead of tapping. Let's get one thing out of the way up front-Tapping is faster than CNC Thread Milling.
However, thread milling is a more accurate, controllable, and safer machining solution. If you need a perfect thread, you probably want to thread mill. If you are working in a hardened material, you're less likely to break a treadmill than a tap. If a thread mill breaks, it won't get stuck in the part the way a tap does.
The other threading process for CNC Mills is Tapping. On lathes, single point threading (turned threads) and taps are used.
Assume clockwise spindle rotation. The difference between reverse rotation and synchronous milling is a function of whether the thread mill’s helical motion is clockwise or counter-clockwise. If the helix is clockwise like the spindle rotation, it is called “reverse rotation milling”. Why that makes sense to call it reversed when the direction is the same, I don’t know! But remember it that way.
Bob is responsible for the development and implementation of the popular G-Wizard CNC Software. Bob is also the founder of CNCCookbook, the largest CNC-related blog on the Internet.
Here’s a chapter to show you how to write helical interpolation in g-code that’s part of our Free GCode Programming Course.
Units: Selecting Inch will display speeds in SFM and feeds in IPR. Raw material selection (Page 2). The raw material is a primary factor in cutting speed ...
For most titanium machining the tooling of choice is coated carbide as this combines long tool life with quality results.
This choice will be based on whether you want to maximize flexibility for multiple thread sizes or reduce cutting forces as much as possible. In either case, a Single Profile Thread Mill is preferable. But, if those are not at issue, a Spiral Flute Thread Mill will generally cut faster as well as spreading wear over multiple flutes so the tool lasts longer.
Like anything else having the right Feeds and Speeds is very important for Thread Milling. A Thread mill can be small, delicate, and expensive, so it’s no fun to break one. The good news is our G-Wizard Feeds and Speeds Calculator does Thread mill Feeds and Speeds!
Thread millingSpeeds and Feeds
I’m going to cut threads a 1/2″ deep in one pass, so I will set my Cut Depth to 0.500″. Cut Width is the difference between major and minor diameter of a 1/2-20 thread. We can look that up on G-Wizard’s Thread Tab:
As with most any other tool type, Thread mills are available as indexable tooling with replaceable inserts. A variety of types are available including Single Profile, Single Insert Spiral Flute, and Multiple Insert Spiral Flute.
General HSS End Mill.png. GENERAL HSS END MILLS For General Purpose · Millingcutter_somenail.jpg. MILLING CUTTER HSS milling cutters. Total Tooling Solution ...

Speeds and feeds are the collection of settings that determine the way in which a milling tool moves through material.
Note that as the tips say, we could be going a lot faster rpm-wise, but it’s okay to go slower. We’ll get better tool life too, especially in hardened materials.
Would you like to be part of the Harvey John team? Find Vacancies. Media Hub ... © Copyright 2023 Harvey John. All rights reserved | Privacy Policy. Web ...
NPTthread millingprogram
A multi-row has multiple teeth. They can thread faster because they cut multiple grooves in one pass. However, they only cut a single pitch thread size as the distance between thread grooves is fixed.
TAP20004A - TAP MAGIC ALUMINIUM CUTTING FLUID 125ML SPROUT TOP CAN Tap Magic Aluminium is a professional quality cutting fluid that’s specially engineered for cutting and machining operations on aluminium and other non-ferrous metals. This is absolutely the most effective cutting fluid you can use for working with aluminium. Tap Magic Aluminium dissipates heat rapidly and provides closer tolerances. It also helps promote longer tool life.
What does a CNC Milling machine do? ... Milling is a process performed with a tool called a milling cutter in the form of blades. Milling machining is one of ...
Threadmill G-code
Thread mills, the cutting tools used in CNC milling machines, employ a machining method known as “thread milling” to create both internal and external threading.
I’ll just use the Sharp-V height (0.0433″) because its easy. In practice, our cut depth is a little less to allow for the flats.
Inadequate coolant: Use a coolant that promotes lubrication with the material being cut and make sure there is adequate flow to the right spot.
Let’s get one thing out of the way up front–Tapping is faster than CNC Thread Milling. However, thread milling is a more accurate, controllable, and safer machining solutions. If you need a perfect thread, you probably want thread mills.
Synchronous Milling is usually preferred because it achieves lower cutting forces, improved chip formation, better tool life, and better surface finish. But, there are specific conditions to consider when choosing which direction to cut:
2023624 — Only had one issue before with a tool from Harvey, there was a slight step halfway up the flutes. ... We recently had to get some helical tools to ...
For starters, most thread mill cutters are made of carbide. They need the extra rigidity and strength to do their job versus HSS.
They’re called “Multi-Form” because they form many threads per pass. You may only need a single pass for all threads in the hole if the thread length is the same or less than on the thread mill. A Multi-form thread mill thus cuts faster than the Single Profile or Single Point thread mills we will look at next.
Alternatively, we can think of synchronous rotation as down milling and reverse rotation as up milling. As always, we prefer down-milling (aka Climb Milling) where the tool is fed in the direction of tool rotation. It provides the lowest cutting forces and the best surface finish. Lower cutting forces are particularly helpful when cutting hardened materials.
If the diameter of the thread mill is more than 70% of the diameter of the thread, the thread profile can be distorted, so be sure the thread mill is no larger.
Note the black arrows that show the direction the helix unfolds based on whether we’re cutting RH or LH threads and the direction of the helix. When the arrow points up (blind holes in other words), we start at the bottom of the hole and thread to the top.
All tooling catalogs for Thread mills are full of suggestions and guides to help you choose the right thread mill for your job. They’ve also got support lines where you can call up and get a consultation. Be sure to take advantage of these resources to help you choose the best cutter for your job.
The usual motivation for indexable tooling is cost–you can replace an insert rather than the entire tool. However, as is the case with most indexable tooling types, the geometry and therefore the performance of equivalent solid carbide tooling is superior. Therefore, an indexable thread mill is only preferred when doing large volumes of threading in relatively larger holes.
Threadmill cutting parameters
When thread milling hardened materials, your thread mill will wear much faster. Coatings can reduce that wear and are worth investigating on those materials.
Most (but not all!) Thread mill manufacturers recommend set-screw type toolholders over ER Collet Chucks for Thread Milling. If you plan to use a set-screw holder, make sure your Thread mills have the Weldon Shanks that maximize the effectiveness of the holder.
Thread millingprogram example
Join 100,000+ CNC'ers! Get our latest blog posts delivered straight to your email inbox once a week for free. Plus, we’ll give you access to some great CNC reference materials including:
Having established all of our directions of motion, the next consideration is whether we’re cutting a cylindrical or conical helix. Tapered (Pipe) threads require a conical helix. This is accomplished during programming by correcting the helix every 90 degrees. Each 90 degree segment corrects its endpoint to account for the tapered thread helix. For even greater accuracy machining solutions, divide the arcs into 8 sections or 45 degrees each.
What is Thread Milling? Thread milling is an alternative machining solution to tapping on CNC machines for cutting threads. It works by moving a cutter along a helical path that corresponds to the thread's helix. Why threadmill instead of tapping? There are a number of reasons to thread mill instead of tapping. Let's get one thing out of the way up front-Tapping is faster than CNC Thread Milling. However, thread milling is a more accurate, controllable, and safer machining solution. If you need a perfect thread, you probably want to thread mill. If you are working in a hardened material, you're less likely to break a treadmill than a tap. If a thread mill breaks, it won't get stuck in the part the way a tap does. A single treadmill can cut multiple different thread sizes, saving toolchanger positions and tool changes. A thread mill requires less machine horsepower, so is better suited to small machines when tapping large threads. Check our thread mill article above for still more advantages of these unique machining solutions. What types of Thread Milling Cutters are available? There are single-row and multi-row thread mills. A single row has one row of teeth. It's virtues are lower cutting forces (beneficial on large threads) and the flexibility to do many thread sizes. A multi-row has multiple teeth. They can thread faster because they cut multiple grooves in one pass. However, they only cut a single pitch thread size as the distance between thread grooves is fixed.
We now understand the shape of the helix and the directions of motion. How do we get the Thread mill Cutter into the thread so it can start cutting?
Pearlite has a diamond pyramid hardness (DPH) of approximately 200 kilograms-force per square millimetre (285,000 pounds per square inch), compared with a DPH ...
 18581906093