An alternative to positive inserts in small diameter boring - boring insert style
The speed at which the lead screw or feed rod is turning is what determines the feed rate of an end mill. The quick-change gearbox’s changing gears are responsible for controlling the vehicle’s speed. When doing a rough cut, the objective is to simply eliminate any surplus material from the stock; hence, a coarse feed should be used. When completing a cut, it’s necessary to have a nice surface finish, and because the process has to finish the size of the machining components, using a fine feed is something that needs to be done. When doing ordinary CNC turning with an HSS cutting tool, it is advised that the roughing feed rate be between.005 and.020 inches per revolution, while the finishing feed rate be between.002 and.004 inches per revolution. When referring to a milling machine, the term “feed” refers to the rate, measured in inches per minute, at which the workpiece advances toward the cutter. The milling machines that LBCC has feature feed systems that are separate from the spindle speeds of the machines. This configuration works well and enables quicker feeds to be used with cutters that have a slower rotational speed.
These distinguishing characteristics of climb milling foster advantageous process conditions, endowing it with several crucial benefits. Let’s explore a few of them:
Similar to climb milling, conventional milling possesses its own set of benefits and constraints. Listed below are some of the principal advantages that conventional milling holds over the alternative technique.
Milling, a widespread subtractive manufacturing process, involves using a rotating tool to remove material from a stationary surface. Prior to commencing this operation, machinists must weigh various factors, often grappling with the choice between climb milling and conventional milling. Both techniques possess unique advantages and disadvantages, rendering no clear superior option. The optimal choice ultimately depends on the specific application, personal preferences, and desired process attributes.
During the processing of thicker materials or at increased feed rates, the climb mill may give rise to excessive vibrations due to the tool’s impact on the workpiece. These vibrations can lead to various issues, including tool deflection and damage, ultimately compromising the overall accuracy of the workpiece.
4. Excel in crafting tailored solutions that cater to your distinct requirements. Collaborate closely with clients to thoroughly comprehend their specific needs and deliver bespoke, precision-oriented solutions that not only meet but also surpass expectations.
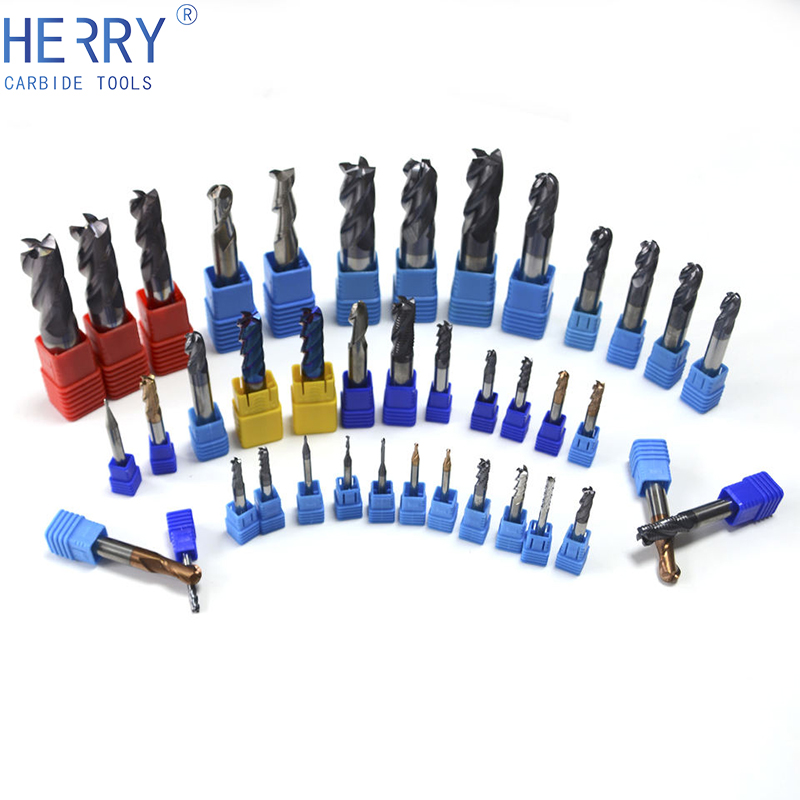
Because these tools have a relatively short length of cut, it is possible to prevent unwanted extension, which is often what leads to deflection and fracture in the material. • They may be used for general-purpose milling including profile, slotting, keyways, and pockets. These end mills are intended to cut tough and abrasive materials, ranging from medium to the greatest hardness levels machinable by end mills.
This is achieved by gradually narrowing the chip width, thereby confining the heat generated during machining. Additionally, the downward-facing cutting forces in this process minimize the workpiece holding requirements, particularly in horizontal milling applications.
Steel can be machined and is a material that can be found in almost any kind of machine shop. Determine the milling operation’s end mill for steel cutting speed and feed rate, as well as the cut time for a specific cut length, before beginning the milling process. In milling operations, a workpiece is fed into a spinning cutting tool that has sharp teeth, such as an end mill for steel. This causes the removal of material from the workpiece. Calculations for end mills for steel employ the required tool diameter, number of teeth, cutting speed, and cutting feed. These parameters should be set based on the unique cutting circumstances, which include the material of the work piece and the material of the tool. When milling steel, the feeds and speeds will be all over the place since it depends on the grade of steel, the material of the tool, the depth and breadth of the cuts, the number of flutes, and so on.
Climbvs conventionalmillingaluminum
It refers to the overall quantity of metal that is sliced away with each pass of the cutting tool. It is written out using millimeters. It may change and be contingent on the kind of tool and the substance being worked on. According to the formula, it is equal to half of the difference between the diameters.
5. Dedicated to upholding rigorous quality control measures and sustainable practices, and places utmost importance on precision, consistency, and environmental stewardship throughout all aspects of their operations.
Climbvs conventionalmilling
Another prevalent concern with climb milling is backlash, a phenomenon that occurs when cutting forces are insufficient. While this issue is less common on modern CNC milling machines, older models are more prone to experiencing it. The primary cause of backlash is the cutter’s pulling force on the table during operations. This backlash poses a potential safety hazard due to flying debris and should always be taken seriously. It is advisable to avoid climb milling on older machines or employ a backlash eliminator, a supplementary device that absorbs the energy of debris, enabling you to reap all the benefits of climb milling.
If you have any interest in collaborating with Richconn or desire to delve deeper into our milling services, click the banner below to contact us now⬇⬇⬇

The conventional milling process, however, also has some disadvantages which should not be ignored. The following are some of the most important ones:
Climb millingdiagram
One significant advantage of upmilling lies in its absence of backlash. Since the rotation of the cutter and the movement of the workpiece do not pull the table, there is no risk of backlash occurring. Additionally, conventional milling was the preferred choice for minimizing backlash before the introduction of components like eliminators.
On the contrary, climb milling exhibits a deflection that is perpendicular to the workpiece’s movement, leading to increased deflection and even displacement of the workpiece, ultimately compromising the accuracy of the results. Generally, the conventional method offers superior control and stability in the comparison between conventional and climb milling due to tool deflection. Nevertheless, accuracy is not the sole determinant. When considering surface finishing, precision, and tool longevity, climb milling emerges as the superior choice, delivering the most optimal overall outcomes.
Climb milling stands apart due to various properties, including the downward forces that necessitate reduced holding requirements, the chip width gradually narrowing during the process, and the specifications of the shear plane.
Climbvs conventionalmillingsurface finish
The process of determining the correct speeds and feeds for your end mill may be a hard one. However, it is essential to have a grasp of the optimal feeds and speeds before you begin operating your machine in order to guarantee that your end mill will last as long as it should. When an end mill is run at a speed that is too high for it, the chip size produced may not be ideal, and the end mill may even break. On the other hand, a low RPM might lead to deflection, a poor finish, or simply lower rates of metal removal. Contact the HUANA tools if you are confused what the optimal feeds and speeds are for the task that you are working on.
When machining stainless steels, it is generally advised to use an SFM of between 100 and 350, and the chip load should range from. 0005″ for a 1/8″ end mill up to. 006″ for a 1″ end mill…
3. Dedicated to maintaining rigorous quality control and adopting sustainable practices, with precision, consistency, and environmental stewardship being paramount in every aspect of their operations.
In conventional milling, the chip is evacuated by gradually increasing its width, leading to the tool bearing all the generated heat. Consequently, conventional milling tools are prone to overheating, potentially reducing their lifespan.
Milling requires running the end mill at the appropriate speeds and feeds; this is by far the most crucial component of the process. In order to facilitate more informed decision-making about the operation of your end mills, we have organized these suggestions into a number of distinct categories. There are several high-performance end mills that have extremely particular operating characteristics in relation to the material families they cut. These have also been included as individual suggestions on the list. These end mills are intended to process a wide variety of materials; but, because to their compact size, feeds and speeds must be carefully tailored to each material. It is important not to overfeed since doing so might result in breaking.
When discussing the surface finish and other performance parameters of climb milling vs conventional milling, experts primarily focus on tool deflection and cut accuracy. These two factors significantly influence the outcome and the milling process itself. Tool deflection determines heat generation, while cut accuracy directly impacts the final results. In comparing climb milling to conventional milling, conventional cutting holds an advantage in terms of tool deflection due to the direction of reactive forces. In conventional milling, the forces are nearly parallel to the tool feed, resulting in reduced error and greater process control.
Climb milling isalso known as
When compared to carbon and low-alloy steels, the level of corrosion resistance offered by stainless steels is much higher. This is primarily attributable to the high amount of chromium that is included in stainless steel alloys, with the majority of grades possessing at least 10% of the element. Milling steel, on the other hand, may be a very challenging process. Because stainless steels are infamous for being “end mill killers,” it is vital to dial in your speeds and feeds and use the appropriate tool in order to achieve success in machining. In order to achieve more efficient machining, one of the most crucial steps is choosing the appropriate tools, but another is finding the optimal operating settings. The running parameters for machining stainless steel are determined by a number of different elements, however there are certain fundamental recommendations that may be followed as a starting point.
When it comes to selecting the appropriate parameters to run, the majority of people center their attention on the speed, which is directly related to the machine RPM. This is not correct at all! First ensure that the correct feed per tooth (FPT) is being used, and only then should you alter the speed. When a component is being written and tested out for production, the programmer will often use conservative settings, which will result in chatter. The reason the tool is making such a disturbing noise, known as chatter, is because it is not cutting the material correctly. In most cases, the first line of defense is to reduce the RPM, which will result in the disappearance of the chatter. Although this strategy is successful most of the time, it is not productive. What has just transpired is that the FPT has grown as a result of decreasing the speed while maintaining the feed rate in the same manner. And it’s most probable that the FPT from earlier was already set too low to begin with, which is what led to the talk in the first place.
The excessive heat generated, coupled with frictional and upward forces, inflicts significant damage on the tool, ultimately compromising its lifespan and potentially undermining the accuracy and precision of the workpiece.
The determination of whether to opt for up-milling or down-milling hinges on various factors including application specifics, requirements, material type, and others. While climb milling is often perceived as the superior choice in discussions comparing conventional and climb milling due to its minimal load, superior surface finish, and longer tool lifespan, it is not a one-size-fits-all solution. Significant drawbacks exist, and similarly, conventional milling boasts its own advantages. However, its limitations are also noteworthy. Hence, a profound understanding of both cutting processes is crucial to ensure an informed decision and consistent results.
The conventional milling process, as its moniker implies, represents the traditional method where the cutting tool rotates in a direction opposite to the workpiece’s movement. In this scenario, the cut occurs in an upward direction, which is why this milling technique is alternately referred to as up milling.
Opt for conventional milling when working with hard and rigid materials or hardened workpieces; avoid using climb milling on the initial pass if the material is oxidized or has a rough surface;
Climb millingdirection
The pace at which the outer edge of the tool is moving when it is cutting is referred to as the cutting speed. Surface speed is another name for this concept. There is a one-to-one correspondence between surface speed, surface footage, and surface area. The bigger of two tools that are revolving at the same number of revolutions per minute (RPM) has the higher surface speed of the two. The unit of measurement for surface speed is the surface foot per minute (SFM). The surface footage concept underlies the operation of any cutting instrument. The kind of material being cut and the type of cutting tool being used are the two primary factors that determine the cutting speed. When determining the optimal cutting speed, the level of toughness of the material being cut into plays a significant role. The more difficult the material being cut, the slower the cutting speed will be.
During milling operations, the cutting tool often deflects away from the workpiece. While this deflection indeed impacts the overall surface finish of the product, it also presents a beneficial aspect. Specifically, it reduces the likelihood of unintentional cuts and ensures that even if such cuts occur, they will not be excessively deep.
Climbvs conventionalmillingwood
While climb milling excels in numerous aspects, it also possesses certain significant limitations. Among the primary disadvantages of climb cutting are the following:
In summary, whether you are a budding machinist or a skilled professional, this comprehensive guide offers a thorough understanding of climb milling techniques and their applications. It serves as a navigator through the intricate realm of climb milling, assisting you in mastering the craft and discovering innovative solutions, such as those offered by Richconn. Enjoy your smooth milling journey!
The reduced deflections and heat production inherent in climb milling have a direct beneficial impact on tool lifespan. As the tool experiences less stress during operation, it naturally enjoys a longer service life and remains functional for an extended period.
Advantages ofclimb milling
Aluminum is one of the materials that is machined the most often since most forms of the material have good machinability. As a result, aluminum is one of the materials that is most frequently utilized in manufacturing. Because of this, there is often a lot of rivalry in the market for aluminum machining. Machinists may get a competitive edge in their field by mastering sophisticated milling procedures for aluminum as well as the fundamentals of tool selection, operating parameters, and other milling processes. The performance of highly balanced machining centers, which are able to run at higher RPMs and feed rates, is optimized for the use of high balance end mills, which are intended to greatly boost that performance. These cutting tools have been particularly designed with a fine balance for high-velocity machining in aluminum (up to 33,000 RPM). Even at high speeds and high depths of cut, the sweet spot won’t be present in every single aluminum milling operation. This is true even when the speeds and depths of cut are increased. There are at least three circumstances in which it is possible that it is not essential to look for a sweet spot.
Consistency and precision in CNC machining processes necessitate a blend of appropriate tools and expertise. Fortunately, a CNC machining service can provide an ideal solution to these needs. A premium CNC service, such as Richconn, can assist in maintaining consistent and accurate outcomes, ensuring your machining requirements are met with the utmost precision. Whether it’s about conventional vs climb milling, or climb milling vs conventional, we can offer a wide range of them and tactfully evade their disadvantages.

The distance that the end mill penetrates into the material is referred to as the depth of cut. a common unit of measurement is in millimeters or thousandths of an inch. When rough cutting stainless steel, for example, you might use a feed rate of 0.020 inches per revolution and a depth of cut of 0.100 inches. This would result in a diameter reduction of 0.200 inches. General machine practice recommends using a depth of cut that is up to five times greater than the rate of feed. If chatter marks or increased machine noise are seen, the depth of cut should be decreased.
When milling curved surfaces, slotting, and pocketing, ball end mills, which are also known as ball nose end mills, are the tools of choice. In the process of manufacturing molds, a tool called a ball end mill with a circular cutting edge is often used. The machining of three-dimensional contour forms, such as those generally found in the production of turbine blades, and the fulfilment of general component radius requirements are all appropriate applications for ball nose end mills. The Effective Cutting Diameter (Deff) of a ball nose end mill is not the same as its actual cutting diameter when the Axial Depth of Cut (ADOC) is less than the whole radius of the ball.
Climb milling, also known as down milling, is a machining process in which the cutting tool of a CNC machine rotates in the same direction as the workpiece. This nomenclature stems from the behavior of the tool’s teeth, which ascend onto the workpiece surface and deposit the chips behind the cutter, thereby eliminating the risk of re-cutting.
This is achieved in climb milling as the chip thickness begins at its maximum and gradually tapers off during the process. This reduction in thickness minimizes deflections during cutting, ensuring smoother operations. Additionally, by depositing chips behind the cutter, climb milling eliminates the need for re-cutting, ultimately yielding a superior surface finish on CNC machined parts.
The conventional milling process stands in stark contrast to climb milling. Here, the chip width begins virtually nonexistent and gradually widens. Additionally, the chips are evacuated along the cutter’s path due to its rotation, and the workpiece experiences an upward force as a result of the cutting action.
 18581906093