Anatomy of a Fastener – Nails Explained - what are metal nails made of
Turning insertnomenclature PDF
As you know that in conventional milling the cutter geometry forces operate in the opposite direction i.e. upward. This makes the achievement of smoot finish impossible. Both the cutting force of the cutter and the deflection in both the cutter and the workpiece cause rough surface finish.
The reason behind fast roughing is that the transition of chip from thick to thin causes less heat generation. Also, the cutting forces are lighter.
The gradual chip formation in the conventional milling process. This causes overheating of the cutting tool since the tool has to rotate for longer periods of time. Overheating not only damages the tool but also affects tool life. It actually reduces the tool life.
The chip formation in climb milling is also very interesting. During the initial stage of the process the chip width is higher and it is thicker. As the process progresses the chip becomes thinner.
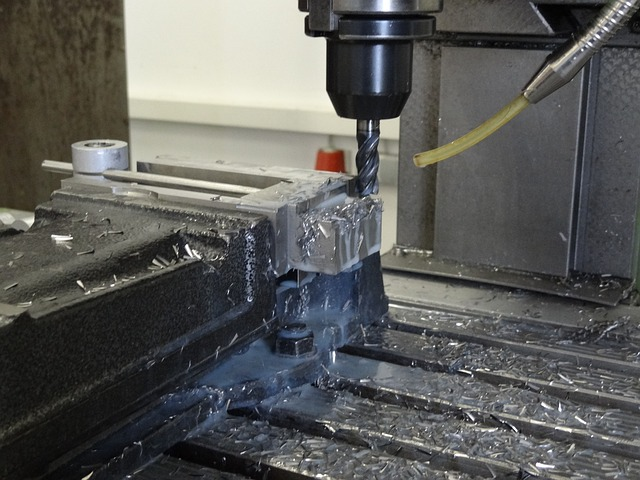
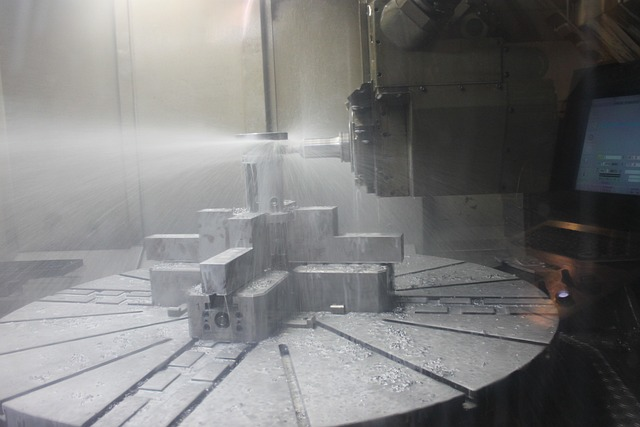
Before understanding the concepts of conventional mill, and climb milling it is better to first know about milling. Milling is a subtractive method of manufacturing. When a rotating tool moves on the surface of a flat surface and does cutting the process is known as milling.
But which technique is important for what situations needs better understanding. This part focusses on the suitability of both techniques. Here we shall pay attention to the climb mill, vs conventional milling debate.
Material compositions are very important in enable climb milling vs conventional debate. Both techniques have different suitabilities for different materials. Aluminum, acrylic, polycarbonate etc. are among the category of soft materials. Therefore, they use climb milling.
For micro milling conventional milling is a better option. However, for obtaining smooth finish pass climb milling is preferred. In certain situations, both processes can be used one after the other.
Both climb milling and conventional milling are complex technical processes. Having better understanding of both in terms of parameters such as tool deflection, heat generation and suitability to different materials is important.
The decrease in the tool life comes with many other disadvantages as well. Not only it damages the tool because of excessive heat generation but it also impacts the accuracy surface quality of the results produced.
1 Contents Grade GC1040 Insert grade for stainless steel milling with high toughness and long-lasting edge sharpness. D2 T-Max® P, ISO S geometries A complete serie of new geometries for productive turning of HRSA and titanium alloys with low tool pressure and chip control in focus. A2 CoroMill® 325 Thread whirling rings and inserts for highprecision threading of long, slender components D9 Highlights from the latest product introductions
CNMGInsertspecification
A 5 GENERAL TURNING GENERAL TURNING Finishing with –SGF geometry For highest surface quality demands Applications - Finish to semi-finish turning with highest accuracy and lowest tool pressure Features and benefits - Periphery ground with sharpest edge line - Extreme accuracy - Lowest tool pressure - Chip control - Highest quality surface integrity Stronger geometries for larger depths of cut For heavier roughing, insert sizes need to be larger to handle higher loads, interruptions and uneven hard skin. We have strengthened the geometries as the insert size grows. Security and productivity...
In case of climb milling the cutting tool does not have to face much stress. The level of heat generated is low. Also, the tool deflection is low in this process. This causes a reduction in the tool wear. The tool life is increased by a percentage of fifty percent as compared to that of conventional milling. The longer tool life has better service life.
5 Contents MILLING Grade GC1040 for stainless steel D2 Tools for gear milling D6 Thread whirling D9 Sharp new –NL geometry and extra-close pitch cutters D13 Higher performance with new end mill D15 The versatile milling cutter D18 Successful grades for titanium D20 The exchangeable-head milling system D21 New possibilities for exchangeable-head D22 Wiper inserts for CoroMill® 345 D24 Accurate slot milling in more widths D25 The cutting edge for titanium milling D27 Silicon nitride grade for profiling D28 High productivity in rough milling HRSA D28 CoroMill® 490 face and shoulder mill D29...
3 Contents Coromant Capto® Disk Interface CDI, the quick-change tooling interface for turning centres is now available as standard. G1 CoroThread® 266 New chip-breaking inserts offer more secure performance for the market-leading threading tool. C2 A global assortment The CoroPak 10.2 supplement now contains all of our latest products in both metric and inch, with dual dimensions when required. Highlights from the latest product introductions
Climb milling and conventional milling are two ways to perform the milling process. They are both different than each other. Understanding them thoroughly will help machinist and engineers make the right machining decisions.
Although the preferred way for most of the machinists and engineers is climb milling yet in some cases the use of conventional milling becomes mandatory. During the cutting process the cutting tool faces backlash. The climb milling backlash occurs when the tool is experiencing backlash beyond its capacity.
2 CoroMill® 170 Precision and productivity is combined with this new gear milling cutter for roughing of internal and external gears. D6 CoroBore® XL The rigid and reliable solution for fine and rough boring in large diameter holes. F2 CoroTurn® SL70 Standard blades and adaptors provide added reach for profiling and pocketing. B6 Highlights from the latest product introductions 2
Machinists prefer the climb milling process because the chances of recutting are almost near to zero. This is also a major advantage of the climb milling process.
Turning insertshapes
This is probably the best advantage of conventional milling. The absence of backlash in case of conventional milling is because of force is carried upward. This does not cause backlash in the machine table and therefore no vibrations or deflections.
General turning B Parting and grooving I General information Multi-task machining H G Tool holding systems F Boring Drilling E D Milling C Threading A 4 GENERAL TURNING GENERAL TURNING Light roughing with –SMR geometry For secure and reliable production Applications - Medium to light roughing - Continuous, interrupted and demanding cuts - Forged- and cast skin Features and benefits - Security - Highest edge line toughness - Chip control - High feed rate capacity Semi finishing with –SM geometry For secure production in long continuous cuts Applications - First choice geometry -...
Now that we have gained in depth knowledge of both climb milling and conventional milling it is important to focus on the differences between the two. For some purposes climb milling is a better option and for others conventional milling.
For rough and harder materials consider conventional milling. However, in case of harder objects try making the final cut using climb milling. It is because climb milling produces smooth surface finish as compared to the conventional cut milling that produces a rough surface finish.
During climb milling operation the operator exerts force through the cutting tool in the downward direction. During these operations the cutting tools exerts a force in the opposite direction towards the operator. However, in case of conventional milling the case is opposite.
When using milling machines in micro milling the tool deflection is at its maximum. Therefore, in such cases selecting conventional milling machine is the best option. Among the two milling methods i.e. conventional milling and climb milling, conventional milling produces less tool deflections.
In the Cutting process tool geometry plays a vital role. However, in certain cases climb mill might produce negative cutting geometry.
General turning B Parting and grooving I General information Multi-task machining H G Tool holding systems F Boring Drilling E D Milling C Threading A 2 GENERAL TURNING GENERAL TURNING T-Max® P New geometries for HRSA and titanium alloys Logical geometry chain It must not be hard to choose an insert for highest performance in a given application when machining heat resistant super alloys (HRSA) and titanium alloys. With a new series of optimized ISO S turning geometries and easy-tochoose guidelines, the best solution is soon in your hands. Benefits - Easy choice for optimized productivity -...
A 3 GENERAL TURNING GENERAL TURNING When to use the new geometries - ISO S: HRSA and titanium alloys - From roughing to last-cut finishing - Continuous and interrupted cuts More than 300 new inserts Inserts: Double-sided T-Max® P inserts Insert styles: S, C, D, T, V, W Nose radii: 0.4 - 1.6 mm (1/64 - 1/16 inch) Geometries: -SF, -SGF, -SM, -SMR Insert grades: GC1105, GC1115, GC1125, S05F, H13A For full information on assortment, please refer to ordering pages on page A15. Easy to choose insert geometry Insert geometries are designed to handle depths of cut from 0.2 to 10 mm (0.008 to 0.393...
Turning insertchart
When you are using manual machines, it is always better to use conventional milling. Conventional milling requires force in the upward direction providing more optimal control to the operator. optimal control is a top priority when using manual machining therefore in that climb milling vs conventional milling debate conventional milling wins this debate.
A 7 GENERAL TURNING GENERAL TURNING Finish machining For finish machining in HRSA or titanium alloys, surface quality demands are often very high. Surface integrity (e.g. deformation depths, hardness profiles, tensile stresses, presence of cracks) are thoroughly investigated for critical parts. The last cut is crucial as it defines the surface quality. Avoid trailing edge notch Notch wear on trailing edge is detrimental for the surface finish. Avoid trailing edge notch by choosing a CVD coated insert grade, S05F, and a low entering angle. Obtain a low entering angle by keeping depth of cut...
Insert geometrychart
CNC machining is the most common process for the manufacturing and design of complex machining parts. It creates intricate designs and patterns. Climb milling and conventional milling are the two techniques used by machinists for the creation and manufacturing of machining parts. However which technique is better for which material is a difficult trade off decision.
Therefore, the force and the backlash can sometimes be so strong that it can result in breakage of the table. This can also result in injuries to the person operating the tool.
The cutting process in which both the cutting tool and the flat surface rotate in the same direction is known as climb milling. This cutting process is also known as down milling. During climb milling the teeth of the cutting tool climb onto the surface beneath the workpiece, hence the name.
This blog is a complete guideline for machinists and engineers who want to make an informed decision about whether to choose climb milling or conventional milling for manufacturing purposes. It highlights advantages, disadvantages and a comparison between both processes. This blog assesses both processes from the aspect of different parameters.
The cutting tool should have the ability to counteract the backlash otherwise it may face breakage. It can also cause a potential injury because of a shrapnel. Therefore, for manual machines that have the backlash are prohibited.
In cutter in climb milling exerts a very strong force on the workpiece. The downward force of the cutter causes the table or the object holding the workpiece and the workpiece itself to exert a reactive force. This force in reaction is known as “backlash”.
During application on hard materials the probability of tool breakage increases. This is especially true when tools are made up of materials like titanium, steel and cast iron.
Turning insertmaterial
Micro milling is an advanced level milling style or technique. This milling style uses CNC milling machines and other tools with high calibrations. The purpose of this milling style is to obtain high level of accuracy and creation of intricate patterns and designs.
We have discussed before that the thickness of the chip in a climb cut and milling decreases with the progress in the process. This is a major advantage of climb milling. This causes less tool deflection. The extracted chip tends to deposit behind the cutter. This eliminates the possibility of recutting. Therefore, guaranteeing a wonderful surface finish.
Even if accidentally the operator does a cut in the workpiece its depth is negligible. It does not produce any visible effect on the appearance of the workpiece. It is all because of the optimal control which conventional milling provides to the operator over the cutting tool.
General turning B Parting and grooving I General information Multi-task machining H G Tool holding systems F Boring Drilling E D Milling C Threading A 8 GENERAL TURNING GENERAL TURNING CoroTurn® HP More new cutting units with High Pressure coolant CoroTurn HP revolutionalizes coolant delivery The latest introduction of CoroTurn® HP tool holders completes the assortment of high pressure coolant tools for negative inserts. CoroTurn HP is now available for the widest range of inserts and Coromant Capto® coupling sizes. CoroTurn HP tool holders accurately direct high pressure coolant jets to...
The possibility of backlash is especially high when the cutting tool is operating at a very high tendency. However, these days the potential of backlash is near to zero. It is because of the use of backlash eliminating tools in the market. These tools reduce backlash and enhance the positive impacts of the climb milling procedure.
CNMGinsertangle
Apart from several advantages there are some drawbacks associated with climb milling as well. Some of them are listed below:
The gradual reduction in the chip width with the process progress has many benefits. One of the benefits is that it causes a reduction in the heat generated. During horizontal milling process the cutting force is in downward direction. This causes a reduction in the cutting load. It also leads to proper workpiece handling.
The downward exertion of force keeps both the workpiece and the cutting tool intact. This causes a reduction in the machining chatter.
The backlash and string vibrations can cause deflections in the cutting tools as well. These affects cutting accuracy too. This also has a negative impact on the cutting tool’s accuracy. As the cutting tool rotates the resulting deflection affects surface finish. Not just the surface finish but it also impacts the result.
The harm of breakage is not only limited to the tool holding the cutter. It also impacts the workpiece on which the cutter is being used. When operating at a high capacity the backlash can cause string exertion of forces even on the workpiece. As a result of these cutter forces the workpiece can break.
A condition of dynamic system that satisfy design objectives is known as optimal control tool diameter. This is another great advantage of the conventional milling process. Since the force is in upward direction and conventional milling has zero tool deflection effects the chances of producing unexpected cut is in the workpiece are minimum.
4 Contents GENERAL TURNING New geometries for HRSA and titanium alloys A2 Cutting units with High Pressure coolant A8 Insert geometry with larger cutting depths A11 High productivity grade for HRSA A12 Silicon nitride grade for dimple inserts A12 New CBN grade for grey cast iron A13 Adaptors for square shank tools A14 Front clamping units in dampened boring bars A14 Inserts Negative basic-shape inserts A15 Positive basic-shape inserts A23 Inserts - Advanced cutting materials A31 External machining CoroTurn® HP cutting units A39 Coromant Capto® cutting units A43 Shank tools A46 Shank tools...
Conventional milling has several advantages. It does have certain limitations as well. To optimize the use of this technique you should have knowledge of both.
In case of climb milling the deflection, force vector is perpendicular to the cut. In both cases there are chances of error. The vector lengths in case of climb cutting and of conventional milling are also longer. Longer lengths indicate the possibility of deflection as well. It is also because of heavy cutting forces.
Considering the climb milling vs. conventional mill finish pass debate tool deflection and cut accuracy are two very important factors. The deflection force vector in case of conventional milling is parallel to the cut. This indicates an exertion of high cutting forces.
It is these deflections that make conventional milling a preferred process for hard materials. Hard materials include cast iron and steel.
While using the conventional machining both the operator and the conventional cutting tool operate in the downward direction. Along with optimal control it makes the whole conventional milling process more stable. This reduces the chance of inaccuracy and damages as well.
Turninginserts types
However, in case you are using traditional approach of working with traditional machines than you should use a backlash eliminator. It is because in that case there is a possibility of deflections.
For such unique circumstances conventional milling process is used. Conventional milling process is almost same in procedure to climb milling. The main difference between the two is that it moves in the upward direction as compared to the downward direction in climb milling.
Therefore, for roughing purposes you should choose climb milling. Because in this case tool deflection does not impact accuracy of the process. Also, it helps you to rough faster.
Climb milling is not a favorable technique for use on hard materials. Chip thickness is the main reason behind it. In the initial stage of the process chip thickness is highest. It becomes thinner with the progress of the process.
 18581906093