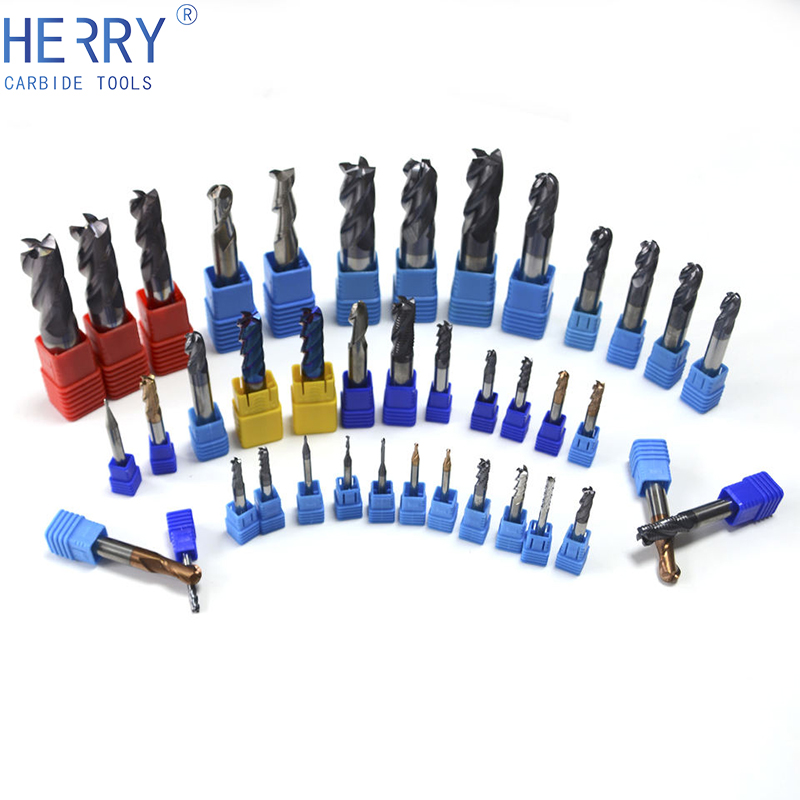
Autodesk HSM: What is it? | Symetri. ... - hsm solidworks
Laser cutting is a precise and highly efficient method for cutting thin stainless steel sheets. The laser beam focuses high energy on a small area, allowing for clean and accurate cuts with minimal material waste. This method is particularly useful for detailed or intricate designs, though it may not be the best option for thicker materials due to slower cutting speeds.
By reducing the heat generated during the cutting process, coolants allow for more precise cuts and less material waste. They are essential for anyone looking to cut stainless steel efficiently.
Cutting stainless steel can be challenging due to its hardness, heat retention, and resistance to corrosion. Unlike regular steel, stainless steel requires specialized tools and techniques to achieve precise cuts without damaging the material or the tools. This guide, based on three article by houstonmetalsawing will help you understand the best tools, methods, and practices for cutting stainless steel effectively.
Band saws are one of the most reliable tools for cutting thick pieces of stainless steel. These saws use a continuous blade with sharp teeth, which ensures clean cuts on even the toughest materials. With the right blade, such as the Q1002 Carbide Tipped Band Saw Blade, band saws are capable of cutting stainless steel pipes, sheets, and rods with ease.
Coolants play a crucial role in extending the lifespan of your cutting tools and ensuring clean cuts. When cutting stainless steel, heat can build up quickly, leading to wear and tear on the blade. Using a coolant, such as QFluids C-5200 or C-5300, helps manage heat and reduces friction. This not only extends the life of the tool but also prevents the material from warping or developing rough edges.
Have you ever tried a button cutter for milling? If so, you’ll know that these versatile tools can really do a good job for you. They’re commonly used for pocketing, die/mold roughing, face milling, slotting, step milling, and even helical interpolation of holes. There’s a lot to recommend round inserts as they have a number of properties that contribute to their success. If you’ve used one turning, you know that their large radius can yield some very nice surface finishes. They can leave a good finish when milling too, but they have a number of other advantages. Their round shape makes them particularly strong as they have no weak corners that can chip. If you do wear or chip one, they can be rotated to expose a fresh edge. They’re advantageous for lighter machines too. When operating at heavier depths of cut, they create cutting forces that are more radial. But, by taking a lighter depth of cut, they transition to behave more like high-feed machining tools. This means most of the cutting forces are directed straight up the spindle, which is the strongest rigidity on any machine. That’s one reason plunge milling is so advantageous on light machines. Button cutters provide an alternative. It seems that for whatever reason, the physics of cutting favors circles. HSM toolpaths do better than conventional paths by adopting loops rather than sharp corners. And button cutters do well because corners on inserts are a weak point that can chip or break off. You can load up a button cutter pretty hard and they’ll hang in there. If you do manage to chip one, just rotate the insert until the chipped portion is not being used and keep going.
The physics of button cutters mean that some very special calculations have to be done when figuring their feeds and speeds. There are several important issues to consider:
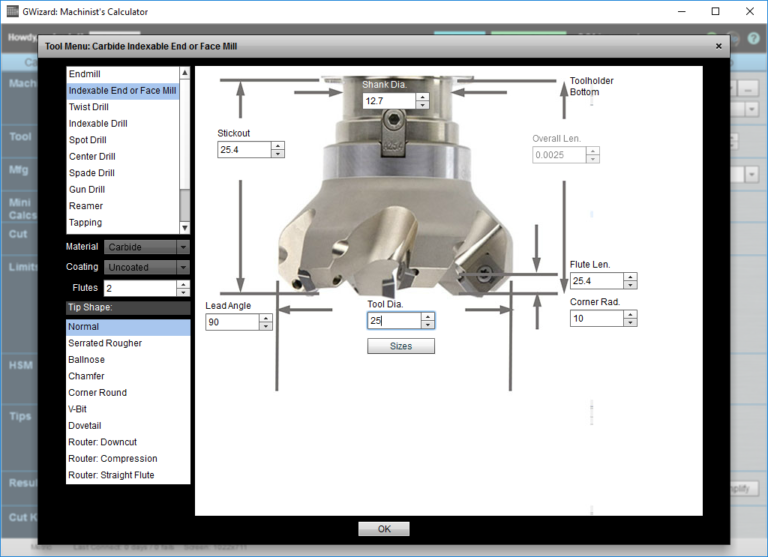
Suffice it to say that simple tables are not going to yield the best results. You need to be prepared to do some extra calculating, or to use a calculator like my G-Wizard Software that does all that for you. There is a lot else to recommend button cutters. For example, they make great tools for helical interpolation of holes. And, they tend to convert a lot more of the cutting force to the axial direction, which is the stiffest direction for most machines. The lower the depth of cut, the more of the force is translated axially. Lastly, when roughing out steps, you get a smooth scallop instead of a shoulder with a corner. This can make life easier for your finishing cutter. Before we leave the topic, let’s consider a few basics in terms of how to operate a button cutter: 1. Try to keep at least a 75% stepover so the inserts spend a lot of their time in the cut. This minimizes the chip thinning in one direction, but it’s okay since round inserts get chip thinning in the other direction. The reason to maximize the stepover is that most of the wear and tear on the inserts is on entry into the cut. 2. Speaking of entry into the cut, arcing in and helixing in are far preferably to plunging in. Try my Conversational CNC Surfacing Wizard and Hole Wizard for some gentle tool paths when using one of the cutters for face milling or helical interpolating holes. 3. Keep the depth of cut below the cutter radius. 4. As you’re considering the best depth of cut, try to keep the width of cut relatively high (about 75% as mentioned in #1). Keep depth of cut less than the insert radius. In fact less is more with these cutters, so drop it down as far as you can while keeping acceptible Material Removal Rates. You can play with these tradeoffs using G-Wizard Calculator to find the sweet spot. Setting Up G-Wizard Calculator for a Button Cutter Setting up a Button Cutter in G-Wizard is pretty simple. We’ll use Tormach’s 25mm cutter as the example. As mentioned, it has a 25mm diameter. It uses a round insert with a 10mm radius. So, choose an Indexable end or face mill tool type, tell it how many inserts (3 for the Tormach) or flutes, and click the “Geometry” button. Set it up as shown:
Basically, you just want to set it up with the right diameter and corner radius. By the way, there’s a trick if you are running in Imperial and want to enter metric values. So, for the cut diameter, I entered “25/25.4” and hit "Enter" and it did the calculation right in the field. You can also enter “25m” to convert mm to inches and 25i to convert inches to millimeters. This post originally appeared on the CNC Cookbook blog.
For more in-depth information on how to cut stainless steel effectively, as well as access to a range of cutting services, materials, and informative videos, visit Houston Metal Sawing. Their website offers expert advice, detailed cutting techniques, and showcases advanced tools and technology. Whether you’re looking to learn more or need professional cutting services, Houston Metal Sawing has the resources and expertise to help you achieve precision cuts every time.
Choosing the right blade for your vertical band saw can significantly impact the quality of your cuts and the lifespan of your tool. If you’re looking to improve your cutting performance and achieve cleaner, more precise results, check out our detailed guide on “How to Choose the Best Blade for Your Vertical Band Saw.” This article covers essential factors like blade material, tooth count, and cutting speed to help you make the best decision for your specific cutting needs. Don’t miss out on these expert tips!
Portable band saws allow you to cut stainless steel in remote locations or confined spaces, making them a convenient choice for professionals.
Portable band saws are versatile tools, especially in construction or fieldwork, where mobility is key. These saws are designed for portability without sacrificing cutting power. Here’s a comparison of some key features to look for:
In the most demanding applications, button cutters compete with high-feed cutters. For many shops, a high-feed cutter is a direct replacement of their button cutter that allows them to crank up the feeds and speeds. For this reason, some have said button cutters are on their way out. But, there are cases where the button cutter still makes better economic sense:
The key advantage of using band saws lies in their ability to maintain precise cuts without overheating the material, especially when paired with a coolant like QFluids C-5300.
When it comes to cutting stainless steel, the tool you choose will depend on the thickness and type of the material. Some of the most effective tools for cutting stainless steel include:
Cutting stainless steel effectively requires careful consideration of the tools and methods you use. Whether it’s a portable band saw for on-site jobs or a laser cutter for precise designs, matching the right tool to your project ensures better results. Always remember to use appropriate coolants to prevent overheating and extend tool life, and choose blades specifically designed for stainless steel to get clean, accurate cuts every time.
Selecting the right blade is crucial for cutting stainless steel effectively. For example, using a high-performance carbide-tipped blade like the Q601 M42 Bimetal blade ensures that you can cut through both thin and thick stainless steel without dulling the blade too quickly. The material, thickness, and type of cut required will all influence which blade is best for your job.
 18581906093