
BALAX 10852-8QL #4-40 Size Thread Forming Tap - 4 40 roll tap drill size
LatheInsert Holder
What is the difference between axial and radial runout? Plus, how to measure both.
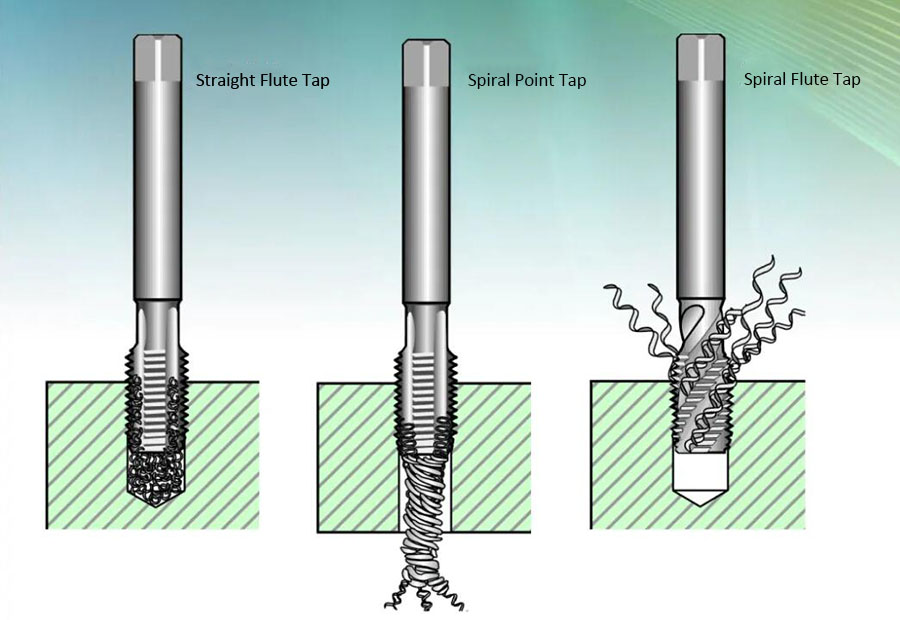
Tap is a commonly used tool for processing internal threads. There are different types of taps according to different classification methods:
Lathe insertsChart
Reversion Mechanism from Deformation Induced Martensite to Austenite in Metastable Austenitic Stainless Steels. Tomimura, Kouki; Takaki, Setsuo; Tokunaga, ...
Reduce the number of chip slots in the tap and expand the chip space in the chip slots; Increase and deepen the bottom hole.
It may be caused by incorrect tap selection, high cutting speed, insufficient cutting cone length, poor chip removal, small bottom hole diameter, cold and harsh conditions, etc. The solutions include: selecting the correct tap according to the processing conditions, reducing cutting speed, increasing the length of the cutting cone, improving chip removal, controlling the hardness of the workpiece, and selecting safety clamps.
Carbide insertschart
In this article, we'll take you through the world of machining stainless steel, exploring its different grades, unveiling the best tools to shape it, and ...
BYU Idaho. · Electric: Western Michigan University. . VIRTUAL RACING ... Formula SAE Electric at Northeastern. Formula SAE Electric at Northeastern.
It should be noted that the specific solution needs to be analyzed and determined based on the specific problem. When performing tap machining, operators should have a high level of skill and experience in order to better deal with various problems and improve machining quality.
Carbide InsertsforLatheTools
To calculate the overall star rating and percentage breakdown by star, we don’t use a simple average. Instead, our system considers things like how recent a review is and if the reviewer bought the item on Amazon. It also analyzed reviews to verify trustworthiness.
It may be caused by the selection of a small bottom hole for the thread, poor chip removal, insufficient drilling depth when the thread cannot be tapped, high cutting speed during tapping, different axes between the tapping tap and the bottom hole, inappropriate selection of tap grinding parameters, unstable workpiece hardness, and excessive wear of the tap. The solutions include: selecting the appropriate diameter of the threaded bottom hole, improving chip removal, increasing drilling depth, reducing cutting speed appropriately, correcting the fixture, increasing the lead angle of the tap, shortening the length of the cutting cone, controlling the hardness of the workpiece, selecting safety card heads, and replacing the tap in a timely manner.
Carbide insertsHS code
Now imagine this mesh of screens drenched in liquid plastic and VViViD039s Carbon Fiber vinyl wraps.
Browse 2551 beautiful Electric Drill stock images, photos and wallpaper for royalty-free download from the creative contributors at Vecteezy!
2024212 — In this post, we will focus on the go-to workhorse insert shapes that are the most popular for job shop CNC turning operations.
Turning process: The shape of the tap is processed into a cylinder through a lathe, and the accuracy of its diameter and length is ensured.
Customer Reviews, including Product Star Ratings help customers to learn more about the product and decide whether it is the right product for them.
2024814 — Register now to participate in the forums, access the download area, buy Mastercam training materials, post processors and more. This ...
What arecarbide insertsused for
It may be caused by excessive selection of the lead angle of the tap, excessive cutting thickness of each tooth of the tap, high tap hardness, tap wear, and other reasons. The solutions include: reducing the front angle appropriately, increasing the length of the cutting cone appropriately, reducing the hardness appropriately, and replacing the tap in a timely manner.
In addition, the production process of taps includes about 20 processes, mainly including three parts: rough machining of materials, heat treatment and finishing. The tap production equipment used for finishing is mainly a grinder, not only because of the high processing accuracy of grinding, but also because the hardness of the heat-treated tool steel is very high and can only be processed with a grinder. These tap production equipment mainly include tap square tail grinding, tap cylindrical grinding, tap groove grinding and tap thread grinding, etc.
Own this business? Claim it. See a problem? Let us know. United ...
Endurance athletes are more familiar with the term 'energy gel.' But, we don't want to call our product a gel, because: Our texture is different. Our ...
A tap is a tool used for cutting threads, commonly used for machining various sizes of internal threads. When using a tap, it is important to choose the appropriate type, material, and size of the tap, as well as the correct usage method, to ensure machining efficiency and thread quality.
Sharpening process: The cutting part of the tap is sharpened through a sharpening machine to ensure the cutting performance and thread quality of the tap.
It may be caused by incorrect tap selection, poor spindle rigidity of the machine tool, and incorrect tap tolerance selection. The solutions include: selecting the correct tap according to the processing conditions, using floating tapping threads, selecting the correct tap tolerance, etc.



 18581906093