58" Long Arm Tool by PRO-LOK - long reach tool
These cookies enable this website to provide enhanced functionality and personalisation. They may be set by us or by third party providers. Functional cookies are used by social networking services to track the use of their built-in features. For example, these cookies allow you to share pages from this website with your social network. Advertising cookies may be set through this website by our advertising partners based on the data obtained. They identify your unique browser and Internet device and may be used to provide anonymized demographic data, build profiles of your interests, and display advertising relevant to those interests.
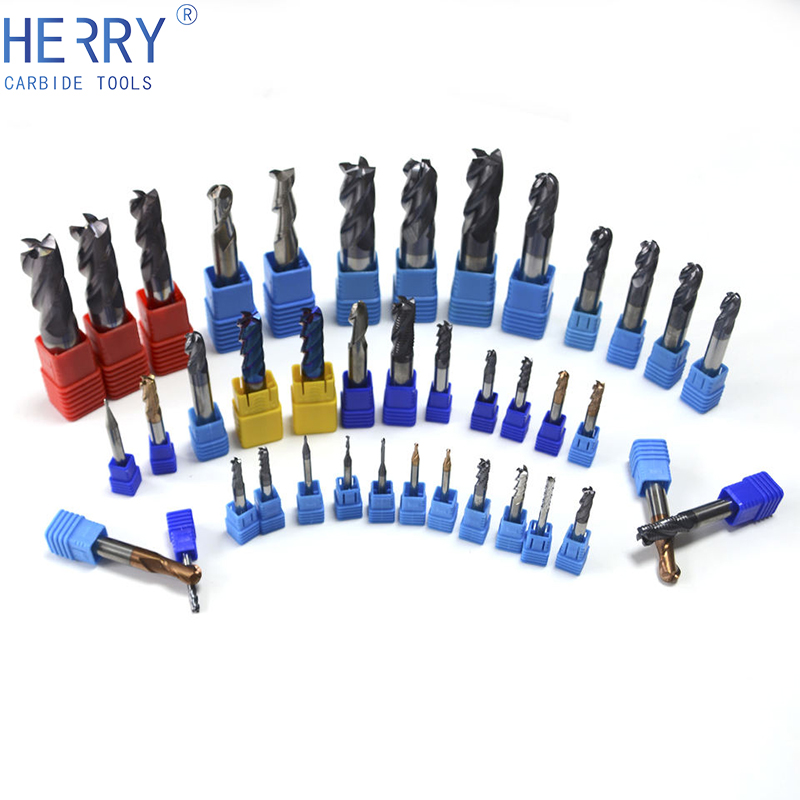
EndMill
Analytical cookies collect information about your use of this website in an anonymous and aggregated form. These cookies are used to analyze and improve the functionality of this website.
1/4" x 60" Used Libert Circle Shear Nibbler, Mdl. 1060, Foot Switch, Worklight, #A3689. Stock No: #A3689. Manufacturer: Libert. Model: 1060. Capacity: 1/4
First, calculate the cutting length per min. from the feed and spindle speed. l=f×n=.008×1000=8IPM Substitute the answer above into the formulae. Tc=lm÷l=4÷8=0.5(min) 0.5×60=30(sec) The answer is 30 sec.
Bull noseendmill
Substitute f=.008IPR, RE=.031 into the formulae. h=(.008)2÷(8×.031)×1000=.258µinch The theoretical finished surface roughness is .258µinch.
CornerRoundingEndMill
Toray Advanced Composites' Research and Development team have developed a new look for the recycling of advanced thermoplastic composites through introduction ...
Speeds & Feeds Calculator · Calculate RPM · Calculate Cutting Speeds · Calculate Cycle Time · Calculate Surface Finish.
Our Smart Feed and Speeds wizard will recommend the best cutting speed, feed rate, and carbide grades for Milling, Turning, Drilling and Grooving.
Substitute f=0.2mm/rev, RE=0.8 into the formula. h=0.22÷(8×0.8)×1000=6.25µm The theoretical finished surface roughness is 6µm.
EndmillCorner Radiuschart
First, calculate the cutting length per min. from the feed and spindle speed. l=f×n=0.2×1000=200(mm/min) Substitute the answer above into the formula. Tc=lm÷l=100÷200=0.5(min) 0.5×60=30(sec)The answer is 30 sec.
Gorilla mill
BallEndMill
Also found in: Dictionary, Thesaurus, Wikipedia. Related to Martensite: austenite. martensite. [′mär‚ten‚zīt]. (metallurgy). A metastable ...
Aug 15, 2011 — Drill a pilot hole into the concrete wall, using a drill and masonry bit. The hole should be the same size in diameter as the masonry nail ...
Bull noseendmill vs flatendmill
Necessary cookies are used to help this website function properly. For example, they provide login retention functionality.
Gorilla Mill products that fall under the High Performance Threadmills category.
※Divide by 1000 to change to m from mm. vc (m/min) : Cutting Speed Dm (mm) : Workpiece Diameter π (3.14) : Pi n (min-1) : Main Axis Spindle Speed
There are some distinct differences between thread milling and tapping. This article explains the advantages and disadvantages of each.
2024526 — Best Overall: Freud Diablo Finish Saw Blade ; Great Bang for Your Buck: DEWALT 10-Inch Miter Table Saw Blades ; Heavy Duty Work: IRWIN Tools ...
2023122 — ADOC files are traditionally categorized as 3D Image Files. The ADOC File Extension can be viewed on the Windows, Mac, and Linux operating systems.
 18581906093