58" Long Arm Tool by PRO-LOK - long reach tool
AutodeskSOLIDWORKS
In many of today’s CNC machines, most operations, including facing, are programmed using constant cutting speed, which is specified in sfm in inch mode or m/min. in metric mode. At constant cutting speed, a CNC lathe automatically applies the correct rpm based on the following formulas for inch and metric systems:
Hardinge supplies D-style, WW and 3C collets and step chucks for instrument lathes, turret lathes and micro-drilling machines.
HSMWorksstudent
Facing is a turning operation in which the workpiece is machined to its center. It involves moving the cutting tool perpendicular to the workpiece’s axis of rotation.
Terry Ashley, training manager for Walter USA LLC, Waukesha, Wis., provided the following technical information on facing aluminum alloy wheels:
HSMWorks2025
Mike Lynch, president of CNC Concepts Inc., Cary, Ill., described four advantages of constant surface speed in his article “The Pros and Cons of Constant Surface Speed” (Modern Machine Shop, January 2009, pp. 62, 64).
Microprocessor-based controller dedicated to a machine tool that permits the creation or modification of parts. Programmed numerical control activates the machine’s servos and spindle drives and controls the various machining operations. See DNC, direct numerical control; NC, numerical control.
HSMWorksvs Fusion 360
2 flute, down-cut, fish-tail, end-mill. For woods, and phenolic. Primarily used for veneered woods, balsa, foam, or other materials with fragile top ...
HSMWorksfor Inventor
Inventor CAM (formerly known as Inventor HSM) Is integrated CAM software for machine workflows. Computer-Aided Manufacturing (CAM) to simplify the process.
Turning machine capable of sawing, milling, grinding, gear-cutting, drilling, reaming, boring, threading, facing, chamfering, grooving, knurling, spinning, parting, necking, taper-cutting, and cam- and eccentric-cutting, as well as step- and straight-turning. Comes in a variety of forms, ranging from manual to semiautomatic to fully automatic, with major types being engine lathes, turning and contouring lathes, turret lathes and numerical-control lathes. The engine lathe consists of a headstock and spindle, tailstock, bed, carriage (complete with apron) and cross slides. Features include gear- (speed) and feed-selector levers, toolpost, compound rest, lead screw and reversing lead screw, threading dial and rapid-traverse lever. Special lathe types include through-the-spindle, camshaft and crankshaft, brake drum and rotor, spinning and gun-barrel machines. Toolroom and bench lathes are used for precision work; the former for tool-and-die work and similar tasks, the latter for small workpieces (instruments, watches), normally without a power feed. Models are typically designated according to their “swing,” or the largest-diameter workpiece that can be rotated; bed length, or the distance between centers; and horsepower generated. See turning machine.
Edmund Isakov, Ph.D., is a consultant, writer and frequent CTE contributor. He is the author of the books “Mechanical Properties of Work Materials” (Modern Machine Shop Publications, 2000); “Engineering Formulas for Metalcutting” (Industrial Press, 2004); “Cutting Data for Turning of Steel” (Industrial Press, 2009); the CD-ROM “International System of Units (SI)” (Industrial Press, 2012); and the software “Advanced Metalcutting Calculators” (Industrial Press, 2005). For more information, call (561) 369-4063 or visit www.edmundisakovphd.com.
202086 — Anatomy of Drill Bits | Types of Drillbit | Industrial Drill Bit ... With a large number of drill bit types and 1000s of sizes out there, we're ...
Is HSM express free
Figure 1. The lathe operations calculator page for cutting time for facing from www.calculatoredge.com. Courtesy of Calculator Edge
On a rotating tool, the portion of the tool body that joins the lands. Web is thicker at the shank end, relative to the point end, providing maximum torsional strength.
DCMT Turning Inserts 55° Rhombic Insert Insert Grades QX5020 (ISO P10-P35 M10-M30 K10-K30) CVD Coated. An excellent general purpose grade for medium ...
HSM Premium
Schematic of a facing operation, where n is the spindle speed, Ro is the workpiece radius at the start of facing, Rmin is the workpiece radius at which the machine tool’s spindle is running at its maximum speed (nmax), Vc is the cutting speed, and f is the feed rate.
AWS San Diego Section · Officers · Scholarships · Student Chapters · AWS Student Chapter @ Workshop For Warriors · District 21 · AWS San Diego Section ...
1. Permanently damaging a metal by heating to cause either incipient melting or intergranular oxidation. 2. In grinding, getting the workpiece hot enough to cause discoloration or to change the microstructure by tempering or hardening.
CAM plugin forSOLIDWORKS
Tangential velocity on the surface of the tool or workpiece at the cutting interface. The formula for cutting speed (sfm) is tool diameter 5 0.26 5 spindle speed (rpm). The formula for feed per tooth (fpt) is table feed (ipm)/number of flutes/spindle speed (rpm). The formula for spindle speed (rpm) is cutting speed (sfm) 5 3.82/tool diameter. The formula for table feed (ipm) is feed per tooth (ftp) 5 number of tool flutes 5 spindle speed (rpm).
SpiroGrooving is a simple yet sophisticated manufacturing process for grooves on sealing rings. The method is used with the CoroBore XL system.
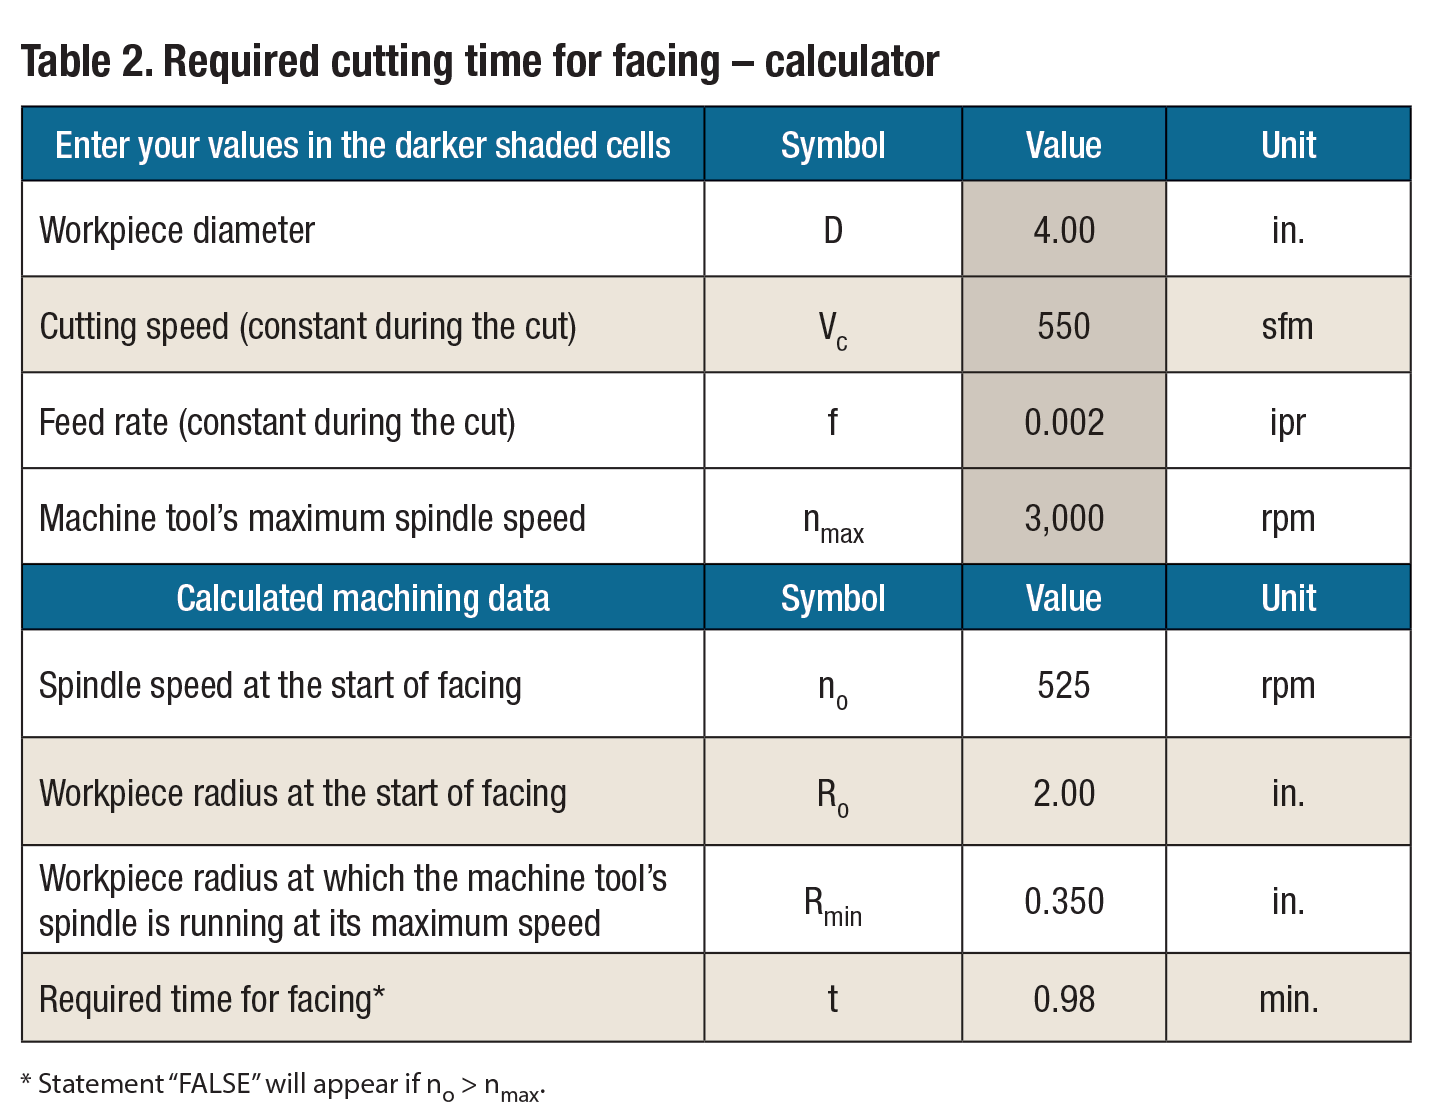
This article’s author developed a formula and designed a calculator for required cutting time when facing at constant cutting speed. The calculator is developed in Microsoft Excel and available in inch and metric units. Table 1 shows its computational worksheet (inch units) before the required values for computation of the cutting time are entered. Table 2 shows the calculator after process parameter values have been entered and cutting time calculated.
This operation can be performed at a constant surface speed (sfm, m/min.), which is recommended, or at a constant rotational speed (rpm), which is not recommended. Facing at a constant rpm decreases the cutting speed, because the diameter of the facing surface gradually decreases by the amount of a feed per revolution. The closer a cutting tool is to the center of a workpiece, the lower the cutting speed. It approaches zero at the center of a workpiece. A low cutting speed can cause built-up edge.
The author also developed a similar calculator based on constant rpm. A sample calculation using the same workpiece diameter, feed rate and rpm instead of the cutting speed is shown in Table 3. Comparison between the two methods of facing shows that machining at a constant sfm (0.98 minutes) requires significantly less time than machining at a constant rpm (1.90 minutes).
thread mill,thread mills,radius tools,chamfer tools,rotary broach,hex broach,thread milling,carbide threadmill,endmill,end mill,carbide endmill,carbide end ...
Workpiece is held in a chuck, mounted on a face plate or secured between centers and rotated while a cutting tool, normally a single-point tool, is fed into it along its periphery or across its end or face. Takes the form of straight turning (cutting along the periphery of the workpiece); taper turning (creating a taper); step turning (turning different-size diameters on the same work); chamfering (beveling an edge or shoulder); facing (cutting on an end); turning threads (usually external but can be internal); roughing (high-volume metal removal); and finishing (final light cuts). Performed on lathes, turning centers, chucking machines, automatic screw machines and similar machines.
... Edges of the object. Fill Corners. Toggle to enable the Fill Corners feature for Chamfer tool. The third and the last of the Fill Settings is called Fill ...
Therefore, end users have a dilemma: facing at a constant speed or a constant rpm. One way to calculate cutting time for facing is to use Web sites such as www.calculatoredge.com, which offers online calculators for engineers at no charge. Among the numerous categories, the lathe operations calculator provides a variety of calculations, including cutting time for facing. It calculates time for facing as a function of the constant rpm, workpiece diameter and feed per revolution. A representation of this calculator and an example of calculating time for facing at selected cutting parameters is shown in Figure 1.
KNUTH's conventional lathes are ideal for workshops, repair shops, job shops, as well as for educational purposes. Our lathes feature extensive standard ...
If the facing of the same wheels were performed at a constant rpm (equivalent to the same cutting speed) and the same feed rate, the cutting time would be significantly longer—about twice as long (Table 5).
 18581906093