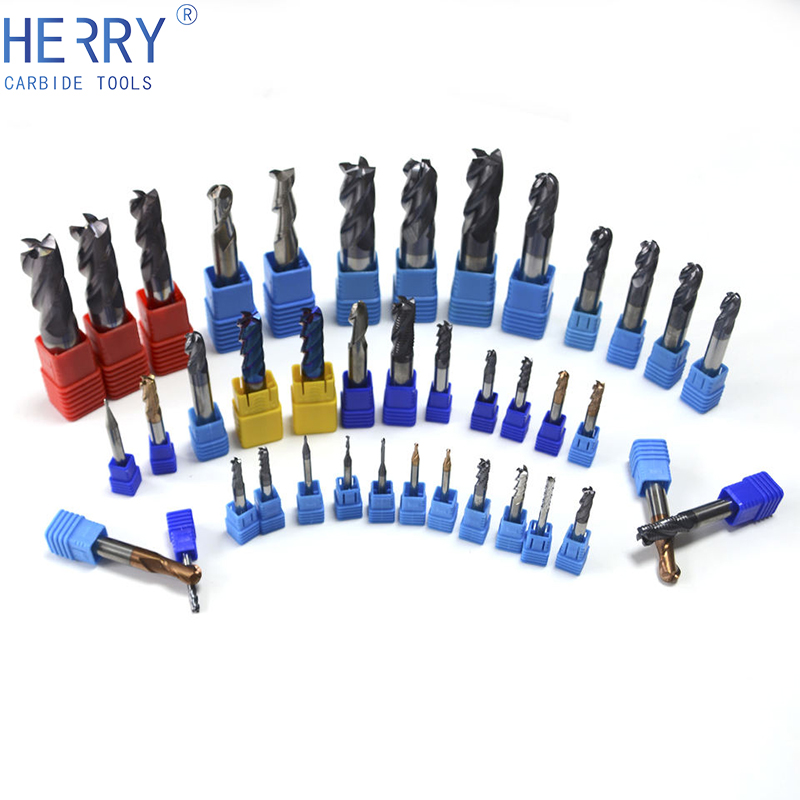
744 40.98 mm Reamer - reamer bit
Mitsubishiinsert nomenclature
The essence of identifying carbide inserts using the system is it allows you to know precisely the piece you need when ordering.
Technology development enables both CVD and PVD to be combined for coating cemented carbides to regulate coating properties.
Moreover, the shape can be octagonal to increase the number of different edges applied as a single edge after one wears out.
Choose a company with a dependable and high-quality supply chain. This ensures short delivery times with assured quality service.
ANSIinsert nomenclature
You can use these cutting tools at high speed, which allows for faster machining resulting in better material surface finishes.
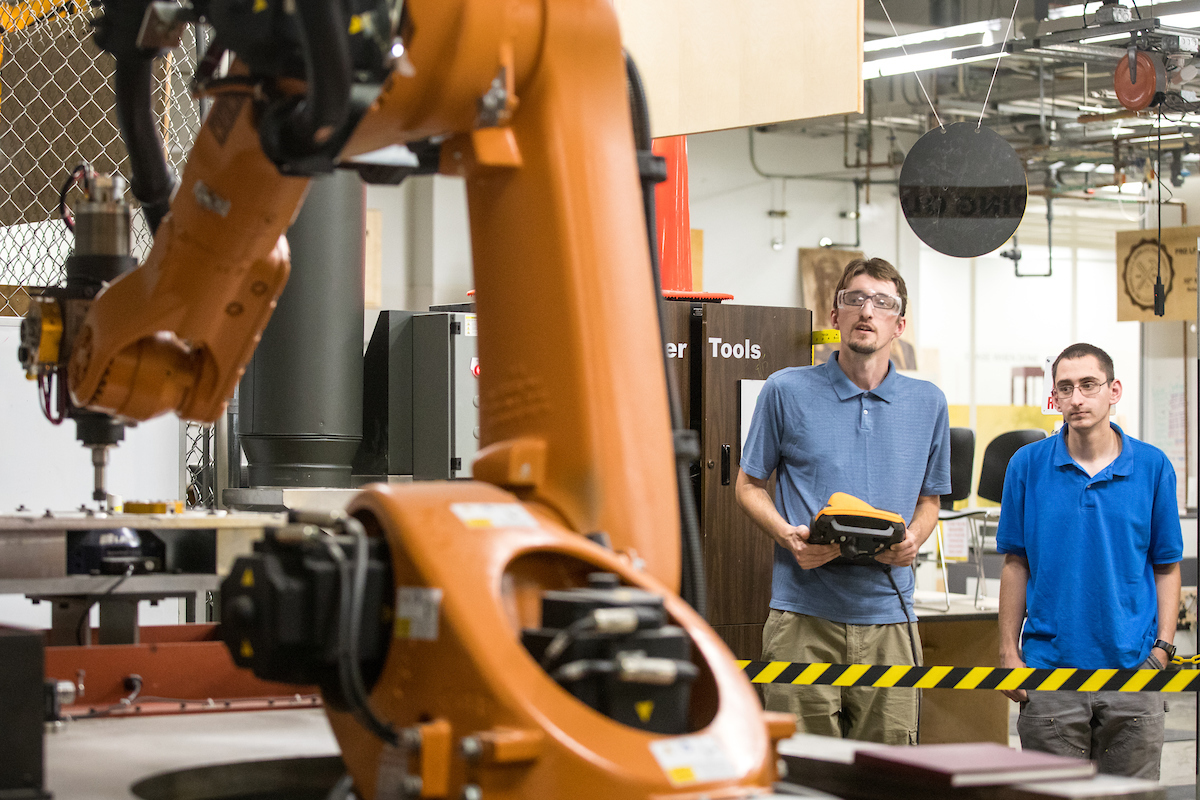
The robot is huge. It’s like the Incredible Hulk’s arm, but made of orange metal. Together, the robot and the table it’s mounted on weigh 13,000 pounds — as much as an African bush elephant. The arm, which can hold 120 pounds and reach a little over 6 feet, machines parts to aerospace tolerances (think one-15,000th of an inch).
When you buy coated carbide inserts, you can be certain of a tool with improved wear-resistance and enabled high speeds and feeds.
“You’re bringing together multiple disciplines from engineering — management, global supply chain — and scheduling weekly industry partner meetings,” he said. “We kept them in the loop, and they kept us in the loop.”
Of course, in the inserts’ codes, the first letter denotes the insert shape while the second letter of the code specifies clearance angle.
Typically, all carbide inserts manufacturers must comply with specific quality standards depending on the target market.
It is a mark of quality standard confirming carbide inserts’ conformity to outlined health, safety, and environmental requirements.
Ultimately, such factors determine whether you’ll attain good machining performance and chip control for desirable results.
Always select a carbide insert size based on the specific application needs and space for cutting tools in the application.
The system provides a universal framework you can use to identify the exact carbide insert you’re using, or you want to buy.
Of course, different companies have different pricing policies as far as purchasing these components is concerned. Wodenco guarantee to give customers the best price on the basis of the best quality.
From definition, properties, features, material grade to certification – you will find all information you’re looking for right here.
ISOinsert nomenclaturepdf
For Dolgin, his learning curve was managing the group. “It was being able to coach them through the waiting periods,” he said. “It was no small task.”
The insert is mainly made from tungsten carbide and cobalt in different proportions, and the original form of the raw material is powder. The prepared raw materials are placed in containers weighing several hundred kilograms to produce different powders. In the workshop, dry raw materials are mixed with ethanol and water to form a mixed solvent, which is a gray pulp with a consistency similar to yogurt. After the pulp is dried, the sample is sent to the laboratory for quality inspection. These powders are composed of many particles with a diameter of 20-200μm, which are very small (the diameter of a hair is 50-60μm).
Boring bars – They refer to cylindrical bars for internal machining, specifically for producing precise holes on workpieces.
Holders – This component supports carbide inserts to ensure it stays strong and rigid to minimize deflection and possible vibration during operation.
We continues to enhance our visibility and reputation, including exhibitions all over the world and we also actively taking corporate social responsibility.
The completion of the coating means that the production process of the blade has been completed. Then they will be sent to the inspection room again for the last procedure. Before packaging, the inspection staff will carefully inspect all the working parts of the inserts through a high-definition electronic magnifying glass to ensure that the quality meets the requirements, check for bruises, cracks, defects, etc., and check the drawings and batch numbers. After the inspection, the inserts will be sent to the packaging workshop, marked with correct materials with a laser, and then they will be packed in a labeled packaging box. Finally, the packed inserts will be put into the warehouse. The staff will record and filed all the products and specifications in the computer. The whole manufacturing process is finished.
This standard certification is common for products in the European Union market. However, they are also applicable in other markets too.
“It was just as much a project dealing with Raytheon and ASU as much as the robot,” he said. “I don’t mean that in a bad way. It was just getting an organization as big as Raytheon and an organization as big as ASU to meet in the middle was not easy.” Doucette graduated with a BSE in mechanical engineering systems.
ISOturning insert nomenclature
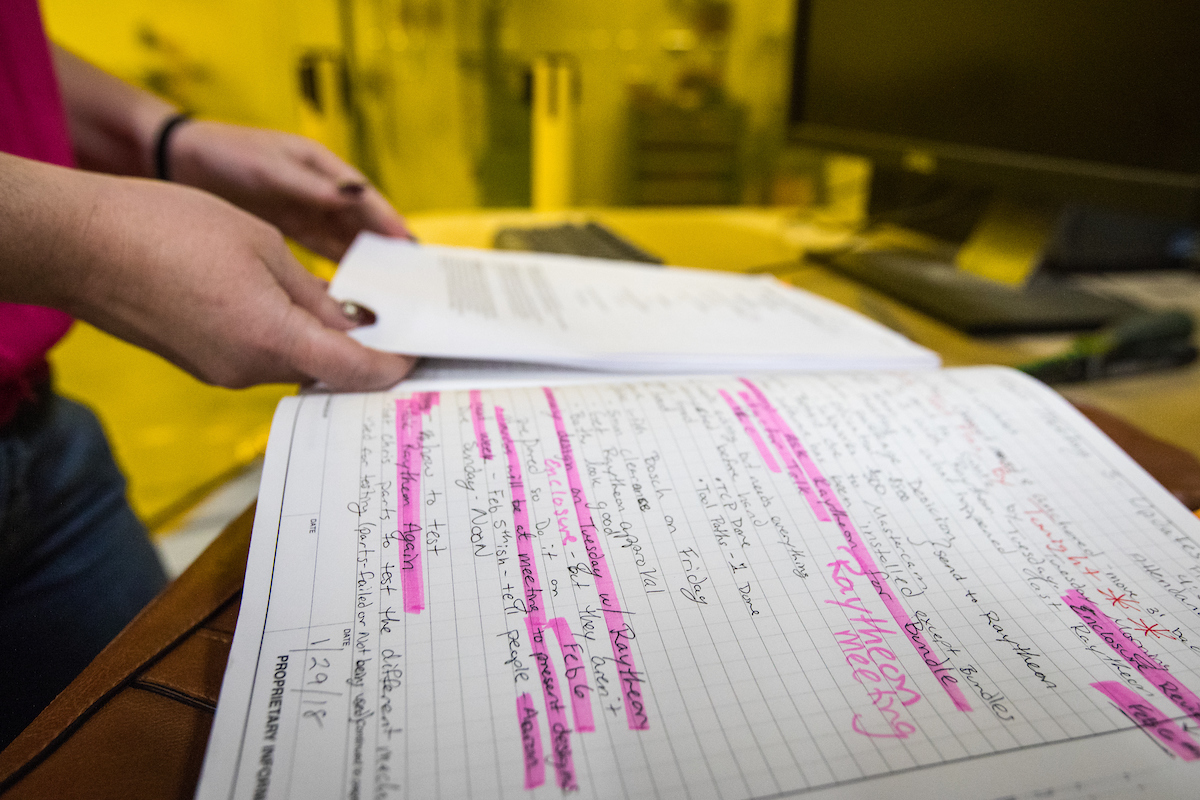
Recent robotics engineering graduate Rebecca Bell reviews her engineering notebook, called "The Bible" due to her meticulous notes on all meetings and all work done on the robotic arm. Photo by Charlie Leight/ASU Now
The robot works at eye-blink speed when it’s throttled up. It’s actually a little eerie to see something so huge move so quickly, smoothly and precisely.
The stamped inserts need to be heated by a sintering furnace to harden them. The sintering furnace can process thousands of inserts at a time. The stamped insert powder is heated to about 1,500°C in a process of up to 13 hours and melted into cemented carbide, a material with extremely high hardness. The shrinkage ratio of the sintering process is about 50%, so the insert size after sintering is only half of the original size.
These tools and accessories are always used in conjunction with the carbide inserts during a specific workpiece operation.
Raytheon shipped the robot from Tucson to the innovation lab on ASU's Polytechnic campus in Mesa. The industrial corporation chose to use the university's eProjects program, which brings students and industry together to solve real-world problems. Industry partners fund project expenses and receive full access to the results.
Also, they are excellent on gummy materials and for threading and cut-off operations. Moreover, this coating type makes it easy to identify the specific carbide insert corners that have been used.
To reduce unnecessary vibration, it is recommended to select carbide inserts with a nose radius smaller than depth of cut.
Express shipping is more expensive than air freight. But you are guaranteed to get the shipment within 72 hours at your preferred drop-off point.
Ideally, a manufacturer with rich experience is an added advantage since you are certain of getting the right type of tool for your needs.
These components are manufactured from a wide range of material grades. Thus the price is likely to vary based on the quality of the particular material.
These powders are packed in a drum with a volume of about 80 kg and transmitted to the punching machine used to manufacture the inserts. The operator puts the stamp dies (dies for stamping different inserts) into the machine tool and debugs them, and then enter the order numbers into the computer. After the above steps, the dies will be filled with powder according to the order information. The pressure of every insert stamping is 12 tons, and the weight of every insert will be weighted by the machine tool under the observation of the operator. At this stage, the inserts are very fragile and easy to break.
Primarily, negative carbide inserts have zero degree clearance angle. The positive inserts, on the other hand, always have a clearance angle ranging between 1-90°.
These codes are comprehensive systems facilitating easy identification of the right tool and not necessarily random letters and numbers.
Moreover, the tool materials must meet the specific appropriate requirements of strength, hardness, thermal and oxidation resistance.
Drill – It is a cylindrical shaft with a conical cutting tip with one or more helical flutes designed to evacuate chips out of the workpiece.
You may also consider a company that can send its representatives to understand the challenges you could be facing with the tools.
Coating carbide inserts is an integral element in enhancing the effectiveness, performance, and durability of these cutting tools.
At WODENCO, we focus in machining very precise carbide inserts, using high quality material grade to meet the dynamic application requirements in your industry.
Nearly 14 billion years ago, a mysterious energy sparked the Big Bang, causing the universe to expand rapidly and generating all known matter — a process described by the inflationary universe theory…
After reaching the required thickness, further grinding is required to obtain precise geometry and sizes. A 6-axis grinding plate is used to meet extremely strict tolerance requirements.
“They were really impressed because we found a lot of issues,” said Marcos Valenzuela, who graduated with a BSE in mechanical engineering.
It is relatively affordable, safer, and more convenient for shipping these items. Additionally, it also takes a few days to receive your shipment.

After grinding, the inserts will be cleaned, passivated and coated. To avoid any grease or dust, gloves must be worn when handling the inserts at this stage. The inserts are placed on the holder of the turntable, and then sent to a coating furnace with a lower pressure for coating. The blades show different colors after coating.
The robot arm was mounted in the top of the table, but it couldn’t reach everything. When the robot was lowered below the surface, it “thought” everything that was on the table was now in the table. The team had to figure out the mess. The challenge? Make it dance and get chips flying. At times it felt like starting from scratch might have been easier.
When using carbide inserts, there are other accessories, which are equally fundamental in ensuring you attain the best results.
Even so, the actual use of these tools is dependent on several factors such as geometries, cutting edge, and mode of operation.
Insert Nomenclaturechart
However, in life and engineering, “you’re not always starting on something from scratch,” said Rebecca Bell, who earned her BSEBachelor of Science, Engineering in robotics this spring. “We had a lot of debugging to do. It was diving in to see what the current state was and how to solve the problems.”
The commonly used ones include the following; Swiss-type, CNC lathe, 5 axis, turning machine, lathe machine, conventional VMC among others.
Turning insert nomenclaturePDF
“We plan to continue working with the ASU Poly campus to refine their manufacturing engineering curriculum and better prepare their manufacturing engineering graduates to immediately contribute when they enter the professional workforce, perhaps at Raytheon,” Spalt said.
Carbideinsertidentification chart pdf
Therefore, you can consider a manufacturer who is reliable and ready to offer well-informed suggestions on the working procedures of these tools.
Use of carbide inserts can be a bit technical given it involves use of different machines hence requires different settings.
Contrarily, negative carbide inserts feature double or single-sided, zero-clearance, heavy cutting conditions, and high edge strength.
“We may be the first capstone project to have middle management,” Chicci said. (Capstone projects are senior-year projects that require students to draw on everything they have learned. Chicci graduated with a BSE in robotics.)
Seat – It refers to a piece of carbide similar size to the insert it supports. Usually, it is placed between the insert and the bottom of the packet, where the carbide insert fits in a tool holder.
They are cutting tools used to accurately machine different metals such as cast iron, steel, carbon, non-ferrous metals, and high-temperature alloys.
“We had placed the robotic deburr project in storage at Raytheon after one of our suppliers could not complete development,” said Chad Spalt, a missile systems engineering fellow at Raytheon. “The ASU Polytechnic eProject program was an affordable way for us to continue technical development on the project, while building a stronger relationship with the ASU Polytechnic campus. The students solved a number of technical issues, and the robotic work cell will soon be slated for use in an industrial working environment.”
Every year, a legion of hackers, programmers, cybersecurity professionals and researchers descend on Las Vegas for the most storied convention in the hacker community: DEF CON.Since 1993, the…
An internship at Northrop Grumman taught him a lot. (Dolgin now works there, after graduating last spring with a BSE in electrical engineering.)
There are two main methods utilized for coating, which include Chemical Vapor Deposition (CVD) and Physical Vapor Deposition (PVD).
American National Standard Institute oversees development of voluntary consensus for different products, including carbide inserts.
After the quality inspection is completed, the top and bottom of the inserts will be ground to the required thickness. Because cemented carbide is very hard, it needs to be ground with industrial diamond.
Recent engineering graduates Aaron Dolgin and Rebecca Bell talk about their work on the robotic arm at the Innovation Hub on the Polytechnic campus. Photo by Charlie Leight/ASU Now
On an airplane, motions of air on both small and large scales contribute to turbulence, which may result in a bumpy flight. But turbulence on a much larger scale plays an important in how stars form…
In particular, ANSI B212.4-2002 describes the specifications of indexable inserts, including the minimum requirements for producing one.
Millinginsert Nomenclaturepdf
Carbide inserts are indexable, which implies you can exchange, rotate or flip them without disturbing general cutting tool geometry.
Top photo: The robotic arm goes through its paces at the Innovation Hub on ASU's Polytechnic campus on May 17. Raytheon delivered the nonworking deburring robot to ASU in hopes that it could reprogram the device after the former integration company failed. In the 60-day time frame, engineering students were able to program, run and test the massive arm. Photo by Charlie Leight/ASU Now
These angles are the difference from 90° measured in a plane normal to cutting edge derived from angle between flank and insert’s top surface.
Defense contractor Raytheon had a $350,000 robot arm, used for smoothing the rough edges of metal, but it wasn't complete.
“I was either in class, here, or on the toilet,” said Jesse Wittkowski, who graduated this spring with a Bachelor of Science, Engineering in robotics and manufacturing.
For the rest of polygons, dimension B denotes the distance measured along the bisector of round-off corner angle and gage roll of nominal I.C
Recent robotics and manufacturing engineering graduates Jesse Wittkowski (left) and Riley Chicci watch the Kuka robotic arm perform functions. Photo by Charlie Leight/ASU Now
The PVD process is a comparatively low-temperature process offering a finer crack-resistant grain structure with a low coefficient of friction.
The design configurations of these carbide inserts comprise a body with replaceable cutting elements thus, known as indexable inserts.
For instance, the specific type of carbide inserts you are buying influences the precise cost you’ll pay when purchasing.
It is the sixth position with a significant one or two-digit number denoting the number of sixteenths of an inch thickness of carbide insert.
In a dazzling feat of technical know-how and tireless dedication, the student engineers had the deburring robot up and running in 60 days. It dominated the students' schedules.
A carbide insert with code CCMT120206 on the description chart shows that the second letter “C” implying its clearance angle is 7°.
Each group features different types, commonly known as tool material grades or simply grades, tantalum carbide, and tungsten carbide.
 18581906093