ACME Industrial - acme threaded inserts
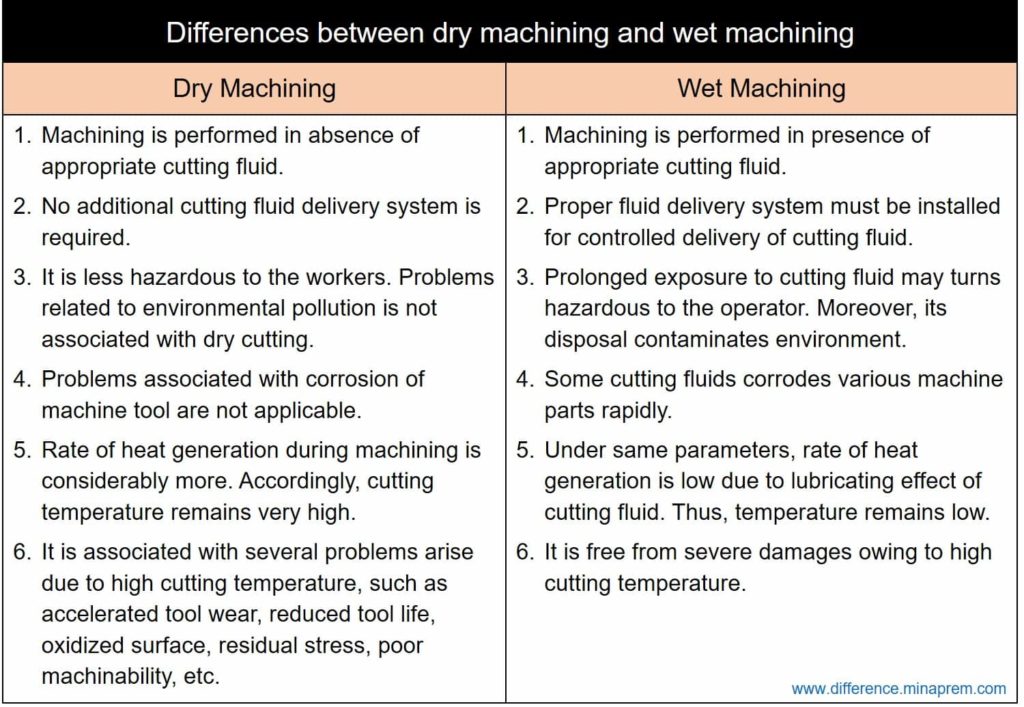
This cutting heat increases the temperature of relevant parts (such as machined part of the workpiece, cutting tool and chip). Excessive cutting temperature has several detrimental effects on cutting tool as well as finished surface of the job. Two possible ways to keep the cutting temperature within limit are—(i) reducing the co-efficient of friction between chip and rake surface by lubricating the contact surfaces in order to minimize the rate of heat generation, and (ii) removing the generated heat from the cutting zone. Both effects can be achieved by delivering an appropriate cutting fluid in proper orientation (cutting fluid acts as coolant and lubricant simultaneously). When machining is carried out in presence of cutting fluid, it is termed as wet machining or wet cutting. If no cutting fluid is deliberately applied during machining, then it is termed as dry machining or dry cutting. Various similarities and differences between dry machining and wet machining are given below in table format.
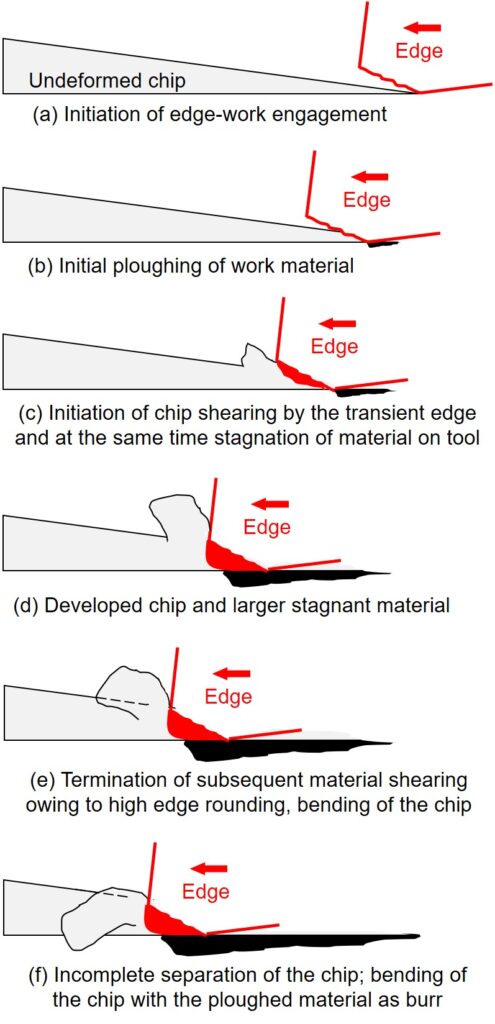
Machining is one secondary manufacturing process that is performed to impart desired shape, size and surface finish by removing unwanted material from a solid 3-D blank. In conventional machining operations, the cutting tool compresses a thin layer of workpiece material to gradually shear it off in the form of chips. The primary shear zone exists surrounding the concentrated shear plane along which work material undergoes shearing to become chip. Initially after forming, this chip flows under pressure over the rake surface of the cutting tool until it reaches the point of separation and finally leaves the cutting zone. Presence of immense pressure and relative velocity between flowing chip and cutting tool gives rise to secondary deformation zone. Both these zones (along with flank wear zone) are sources of cutting heat; however, secondary deformation zone accounts for 70 – 90% of cutting heat.
Minaprem.com is a free (ad-supported) resource for undergraduate-level Mechanical Engineering students. Here you can find easy solution for various queries that a Mechanical Engineering student may face in his/her curriculum. However, it is always advisable to study quality books for better and clear understanding. For any kind of requirement, you can contact at admin@minaprem.com
Our turning carbide inserts could to be processed Alloy steel, Tool steel, carbon steel, stainless steel, Cast iron and Titanium alloy. Working material as following:
 18581906093