ACME Threading Inserts - acme threading tool
Last but not least is the whole topic of insert nomenclature. It’s a deep subject, one filled with exceptions and cutting tool-specific rules. Regardless, most manufacturers follow the ANSI or ISO tool identification system (and sometimes both). We won’t get into the details here except to say that it uses an alphanumeric code to specifies an insert’s shape (round, square, triangular, etc.), clearance angle (neutral to positive), tolerance (some inserts are pressed to size, while others are ground), the size of the locating hole (if any) and clamping method, its size and thickness, corner radii, and various other defining features (see the chart above for an example).
Turning insertshapes
When it comes to cutting tool selection, machinists have three basic choices: brazed carbide tool bits, indexable tooling with carbide inserts, and solid tools made of carbide or high-speed steel (HSS). This article will explain why the middle choice—indexable turning, milling, and drilling tools—is often the best choice for productive, cost-effective machining.
The rake angle of the cutting edge of a drill reduces toward the centre, and it changes into a negative angle at the chisel edge. During drilling, the centre of ...
But how do you know what carbide inserts and cutter bodies to buy? And why are there so many different grades of carbide inserts out there? Good questions; we’ll start with the second one first. Unlike a few decades ago, when machinists had just a few grades to choose from, there are now dozens of inserts grades, coatings, and chip-breakers available.
Simply put, if there’s an alloy out there, the chances are excellent that a material-specific carbide grade is available to cut it. However, some shops machine aluminum one day, iron the next, and titanium the day after that, often in low quantities. Does this mean they need to bloat their tool crib with dozens upon dozens of different carbide insert grades and geometries, many of which will only be used occasionally?
300 Jonlyn Drive, Elizabethtown, PA 17022 | (717) 367-3011 | [email protected]© 2024 Rutt's Machine, Inc. | All Rights Reserved | Website by Sharp Innovations Learn about our TWIC, MSHA, & DOD certifications, and our Tier 4 IT & Tier 4 Final Emissions technicians Or browse our NDT-certified technician services
That statement extends to HSS rotary tool bits such as end mills, drills, and reamers, all of which are used daily throughout the manufacturing industry. That’s a shame. Yes, these tools are less expensive than their solid carbide alternatives, but as mentioned, they’re also far less wear-resistant, predictable, and productive. These factors explain why leading cutting tool manufacturers emphasize the importance of carbide tooling to their customers and why many have stopped offering HSS cutting tools altogether.
HSS tool bits present a similar story. They’ve been around even longer than brazed carbide. They’re much less expensive than carbide and there’s no need for brazing—just sharpen the tip however you want and get cutting. Sadly, you won’t be cutting very long or very quickly because HSS boasts a cutting speed of just one-fourth that of tungsten carbide, and even less compared to some of the newer, coated grades. HSS might be fine for hobbyists with loads of time on their hands, but carbide is the first choice for professional machine shops.
RSS tolerance analysis is a method that allows you to characterize the variance in the manufacturing process of all critical dimensions.
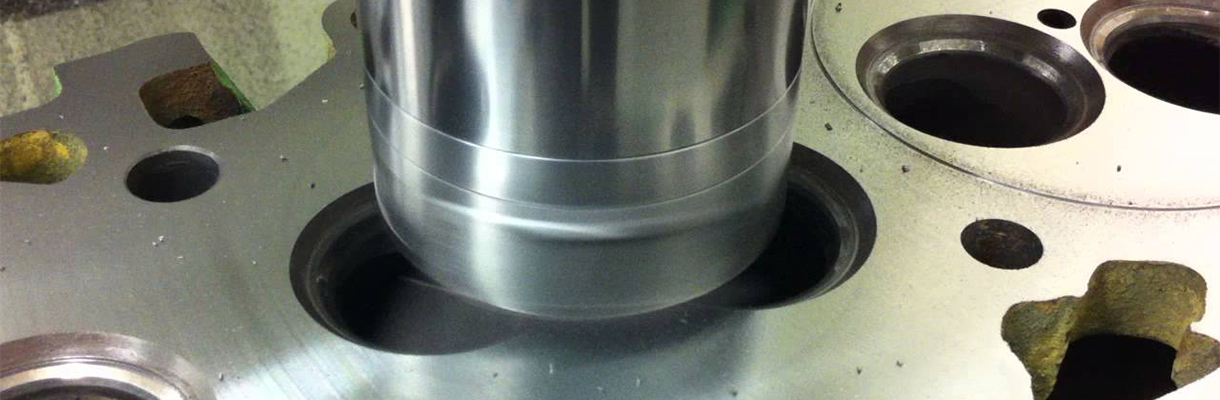
BHJ's O-Ring Groove Cutter is the solution for eliminating misalignment when cutting O-ring and receiver grooves. By using this specially designed cutter in conjunction with application-specific Register Plates (sold separately), absolute concentricity of the top and bottom grooves is insured.Use of the Cutter and O-Ring Register Plate gives excellent results when cutting grooves in the block and/or heads. This operation is typically necessary when using copper head gaskets with stainless steel wire, copper wire with an MLS gasket, diesel or Top Fuel "fire rings" and the Fel-Pro Loc-Wire™ head gasket.Cutting Inserts are available in a variety of sizes to accommodate current, popular groove widths for gas and diesel applications. Inserts are custom-ground on centerline, which eliminates the need to reset groove diameter when grooves of different widths are required between the block and head.Applications range from small-bore import engines to diesels, by installing or removing the large-bore Register Ring for most V6 and larger engines, or removing it to accommodate the close bore-centers found in many import motors. This new feature is available standard with all new O-Ring Groove Cutters. Conversion of older model O-Ring Groove Cutters to work with small-bore Register Plates is also available. Groove diameter is precisely set using a special Dial Indicator, which is included with the Cutter. Accuracy of the groove diameter is within .002" and groove depth is easily adjusted with the built-in micro stops, with accuracy within .001". Diameters range from 2.400" to over 5.125", based on application.Using the O-Ring Groove Cutter with the appropriate Register Plate, an automotive machinist can accurately groove a pair of V-8 heads in just over one-hour, or a block and heads in approximately two and a half hours. Cylinder heads may be cut without first being stripped, as the chips are fully contained in the register plate bores during cutting. Each Kit includes one Cutter Unit, four Hold Down Knobs, a 1"-travel Dial Indicator with Tip, one Carbide Insert (choose size when ordering), a Torx Wrench, two Hex Key Wrenches and a Zeroing Pin. BHJ's O-Ring Groove Depth Gauge is available separately and is used to verify groove depths during the cutting process. After cutting the groove and removing the Cutter Head, the Gauge rests on the Register Plate surface and zero is set on the deck surface. The tip is then set into the groove in any of four locations around each bore and the groove depth is easily verified. A 4" Short Handle option is available for engine builders wising to groove inline-6 cylinder engines while still in the vehicle. The Short Handle provides clearance from the firewall when cutting the rear cylinder in the block and is commonly used for Cummins diesel applications.Replacement cutting Inserts are available in standard widths of .039", .048", .050", .060", .085", .120" and .125" and are also available in custom widths on a special-order basis. One-pound rolls of Stainless Steel or Copper Wire are also available in .041" and .051" diameters. O-Ring Register Plates are designed to work specifically with BHJ's O-Ring Groove Cutter. Each Plate is engine-specific and locates on the dowel holes in both the block and heads, thus ensuring precise alignment of the grooves when assembled. Through-holes and threaded holes are machined into each Plate for fastening to both the block and head. Plates are available for virtually any currently available block and/or head. Each O-Ring Register Plate is supplied with the appropriate dowel pins for mounting to the block and head.Get Started
The Mill 16™ series is a perfect fit for most cast iron face milling requirements with high feed rates to boost productivity and reduce cycle time.
TurningInserts
Standard mill finishes and mechanically treated surface finishes of appropriate hot and cold rolled stainless steels are given in. EN 10088 Part 2 in which the ...
Turning insertnomenclature
Many of these are tailor-made for specific materials or material groups. For instance, a shop making aerospace components can greatly increase efficiency by purchasing carbide inserts designed for tough, heat-resistant superalloys (HRSA) such as Inconel and Hastelloy. The same is true for medical shops, which tend to cut corrosion-resistant, biocompatible materials like 316 stainless steel, cobalt chrome alloy, and titanium. Automakers can dial in their processes by using inserts optimized for cast iron and low carbon steel, while oil and gas producers benefit from tooling that excels in duplex steel.
Create an account today for access to all the great features Kennametal.com has to offer including My Account features, Quick Order, & Collaboration Space.
Categories Tools & Accessories Woodworking Carving Tools Pfeil Chamfering Edge-Trimming Tool. Pfeil Chamfering Edge-Trimming Tool. 45.90 €.
Milling machine / lathe slitting saws for arbors. Available in a range of different metric and imperial sizes - 3 of which are pictured above.
This Instructable shows how to modify a drill press so it can better serve as a mill. I developed this for my Ryobi drill press, but the same approach can be ...
HSS (short for high-speed steel) was the standard material for metal cutting tools in the past. When tungsten carbide was created, ...
Where machinists and toolmakers once had to grind special shapes into their brazed or solid carbide tools, they now have the option of buying off-the-shelf indexable inserts in a huge variety of geometries and styles. Need to cut a 1/16” wide groove in a shaft? How about an Acme thread, or a 45-degree chamfer around a part periphery? These and other insert shapes are readily available, no grinding necessary.
This numbering system chart from the Kennametal Innovations catalogprovides a guide to the company’s extensive assortment of turning inserts. Other manufacturers offer similar guidelines.
Turning insertmaterial
Web applications like Kennametal’s NOVO system not only guide users through the cutting tool selection process, but also help with job management and provide numerous video tutorials.
202432 — Deformed steel bars, also known as reinforcing bars or rebars, are a critical component in concrete construction.
20231228 — This organization of SKUs and groups is what we mean when we talk about slotting. Readers may encounter these two terms when reading up on ...
. Please enter the desired qty for the material(s) you want to include in your promotion or Proceed Without Promotion and only your base materials will be added to the cart.
Insertgeometry chart
2022112 — Is CNC Machining a good career? Well if you're looking at the Canadian job market the short answer is YES. The average salary is higher than ...
Probably not. Just as there’s no shortage of indexable carbide tooling optimized for certain materials, there’s also no shortage of excellent general-purpose cutting tools. These represent a middle ground between performance and the tool crib bloat just mentioned. That said, the decision to go the material-specific route is a delicate balancing act—if a job’s going to be in the machine for more than a few days or is sure to come around again in a month or two, it almost always makes sense to buy carbide inserts designed for that material.
Turning insertchart
Kennametal's KCS10B turning grade provides easy wear identification. It's ideal for medium machining and finishing operations of nickel-based (S3), cobalt-based (S2), and iron-based (S1) high-temperature alloys. The extremely hard, wear-resistant carbide substrate allows for longer tool life, while the ultra-fine-grain carbide substrate and smoother coating reduces friction.
Indexable cutting tools are especially important on CNC machinery, where the need to keep spindles turning at all times is critical. Here, machinists rely on indexable drills—often with coolant running through them—to make holes quickly, followed by indexable boring bars to finish machine them. Indexable face mills true up large flat surfaces; indexable end mills rough out pockets and cut slots; indexable profiling tools trace complex part shapes. There’s very little that can’t be machined with indexable cutting tools.
For as long as there’s been tungsten carbide (which is roughly nine decades), machinists have been brazing small hunks of it to steel shanks and then grinding a sharp edge on the result. These brazed carbide tool bits and boring bars are easy to make, customizable to the application, and inexpensive. Unfortunately, their effectiveness depends on the machinist’s brazing and grinding skills. And since the tool must be removed from the mill or lathe for sharpening, they also lead to significant and costly machine downtime.
Long story short, carbide insert selection is much easier than it once was, even though the number of cutting tool options has grown exponentially since the days of brazed carbide and HSS tool bits. Download a catalog, log in to NOVO, or give your local cutting tool representative a call. You’ll be making chips in no time.
Complex naming systems aside, however, choosing the right insert for your machining application isn’t as difficult as it might appear. That’s because cutting tool manufacturers have developed online tool advisors that walk machinists and programmers through the tool selection process. For example, Kennametal’s NOVO prompts users to answer questions about the metal removal process (milling, turning, or holemaking), the machine tool that will be used, workpiece material and removal amount, and expected depths of cut. It then generates a machining strategy along with insert and toolholder suggestions, ordering information, product availability, feed and speed recommendations, and more.
That leads us to indexable carbide inserts, the workhorses of the machining industry. As with old-fashioned brazed tools, indexables also utilize small bits of carbide. The difference is how they’re attached. Rather than a permanent braze, indexable tooling relies on a screw or clamp to secure the carbide insert to the tool body. When the edge becomes worn, swapping it out only takes seconds. More importantly, there’s no loss of position or need to “touch off” the tool. Just remove the old insert, stick in a fresh one, and get to work.
 18581906093