ACME Threading Inserts - indexable carbide threading insert
YG-1
The goal is to select an insert that meets your requirements for quality and performance, while providing good chip control, and a reasonable combination of ...
62015-5601-U1D BRAKE | Konecranes US Store | English - Buy now...
D Ozkan · 2020 · 88 — In this study, the production, characteristics and industrial usages of CFRP composite materials, milling and drilling operations carried out on them are ...
WIDIA
UP milling, also called conventional milling, involves the cutter and feed moving opposite each other, while down milling, also called climb milling, ...
If the machine is operating in a high-temperature environment, the coolant may need to be changed more frequently. This is because the heat can accelerate the degradation of the coolant.
In summary, CNC coolant is a vital element in the machining process. It’s critical to change it regularly to maintain its effectiveness and prevent damage to the machine or tool bits. While the frequency of coolant changes can vary depending on several factors, most manufacturers recommend changing the coolant every six to twelve months. In addition, regularly monitor the pH level and observe signs indicating the need for coolant replacement, such as foul odors, cloudiness, or compromised cutting quality.
Ingersollcuttingtools
It is essential to change your CNC coolant regularly. CNC (Computer Numerical Control) coolant is a crucial element in the machining process. It helps to cool and lubricate the cutting tool, preventing overheating and prolonging its lifespan. However, like all liquids, CNC coolant can degrade over time. This reduces its effectiveness and can potentially damage the machine.
2019212 — A drill press assumes constant axial load, straight up in to the spindle. This means the tapers are forced against each other. Drilling just ...
Calculate feed and speed for CNC tools, machines and projects with our free calculators below. Chose a calculator, input the parameters and press calculate!
How do I cut a dovetail? Do you have anything to help cut consistent, even dovetails? Would you ever gang cut dovetails? Do you use a coping saw to cut…
The tap is designed for internal thread cutting, so this would be used on the fastener hole or a nut, whereas a die is used for the external thread, like on a ...
Carbide grade is often dependent on the type of metal used: tungsten, titanium, or tantalum. Grades have different levels of hardness, toughness, and wear ...
Harvey Tool
Our mission has always been simple. It is to provide the metal working industry with the oil skimmers and metalworking fluid management systems they need to complete jobs quickly and efficiently. Innovative and affordable solutions have gained us many accolades. Our continued growth is due in no small part to our excellent customer service… Not to mention our satisfaction guarantees and the performance of our tools.
The interval at which coolant needs to be changed varies based on multiple factors. Look at your coolant type, the machined material, and the machine’s operating conditions. As a general rule of thumb, most CNC machine manufacturers recommend changing the coolant every six to twelve months. Nevertheless, this serves merely as a recommendation. It is crucial to consistently monitor the coolant to determine the appropriate timing for its replacement.
If you notice any of these signs, it’s essential to change the coolant as soon as possible to prevent damage to the machine and maintain the quality of the finished product.
After successful registration an E-Mail will be sent to the address provided in the form with a link to verify your E-Mail Address, this is a required step to place orders on the website.
Walter
TitanUSA
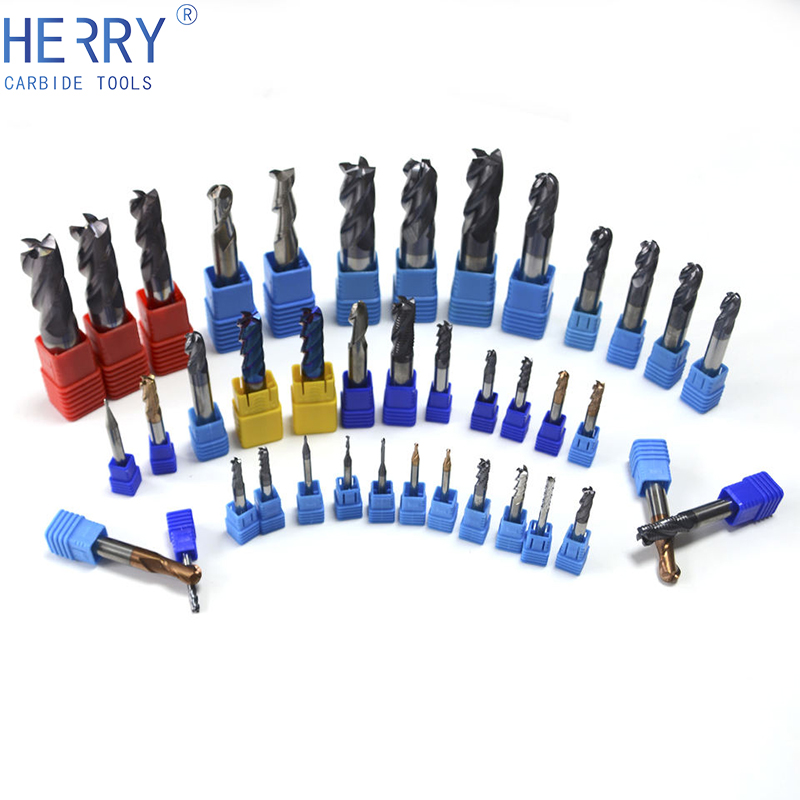
Titan USA End Mill, Center Cutting Regular Flute Single End Square End, Series: 101, 3/4 in Cutter Dia, 4 in Overall Length, 1-1/2 in Length of Cut, 2 Flutes, Spiral Flute, 3/4 in Shank Dia, Right Hand Cutting, 30 deg Helix Angle, Cylindrical Shank, Solid Carbide, AlTiN Coated
One way to determine when to change the coolant is by measuring its pH level. Coolant becomes acidic over time due to the buildup of bacteria and contaminants These cause corrosion and other potentially harmful issues. Regular monitoring of the pH level enables you to determine the appropriate time for coolant replacement. Typically, a pH level from 8.0 to 10 is recommended for coolant, and any variation from these numbers requires changing.
Our 1/4" Corner Radius End Mill is versatile, allowing for both sculpting and 2-D profiling operations with a single tool when machining aluminum and other non ...
By adhering to these measures, you can ensure optimal performance of your CNC machine and achieve high-quality end products.
In this blog post, we will delve into the frequency at which CNC coolant should be replaced and the various factors that can influence this.
Before we dive into the frequency of coolant changes, let’s briefly discuss why coolant is essential in CNC machining. Cutting tools generate significant heat during material cutting. This leads to rapid wear and potential breakage. Coolant performs a vital function by circulating around the tool and efficiently dispersing the heat, effectively removing it. This heat reduction not only prolongs the cutting tool’s lifespan but also enhances the overall quality of the finished product. Coolant also helps remove chips and debris from the cutting area. This reduces the risk of damage to the machine and improves the accuracy of the cuts.
 18581906093