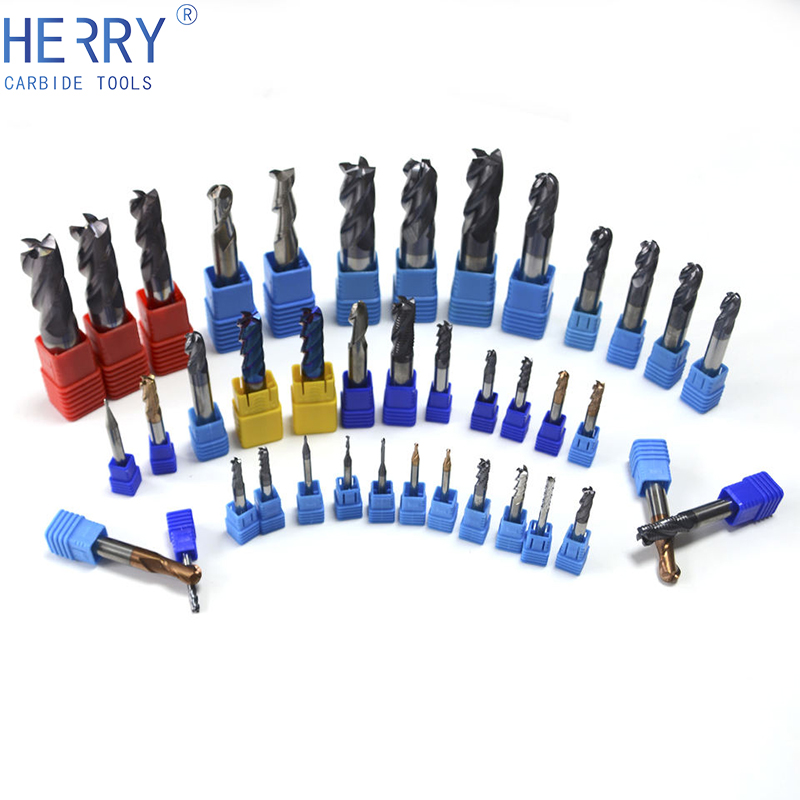
All About Chamfer Machine - chamfering operation
4. Apply the total statistical tolerance. Adding and subtracting the statistical tolerance from the nominal dimension gives the likely or probable maximum and minimum distance values. Hence in this case, Nominal = 21. RSS Tolerance Value = +- 2.739. Hence the gap = 21+-2.739. Correspondingly the probable maximum = 21+2.739 = 23.739, and the probable minimum = 21-2.739 = 18.261.
Note: While Tolerance Stack-up Analysis can be applied to components and assemblies designed with GD&T (Geometrical Dimenstionaing and Tolerancing) specifications, this article uses the conventional dimensioning system for the sake of explanation.
Indexableinsert
20241020 — Kids Web Services · Developer Community · Fab . Tactical Male Soldier 0. . soldier male ,with 3 LODs , without ammo bags ...
The relationship between the RSS tolerance and the standard deviation in the process, is considered that level of process controls of the inputs represents the level of process controls of the output. Which would imply that if all the component tolerances are assumed to be ±1σ, ±2σ, or ±6σ, then the RSS tolerance stack-up result represents ±1σ, ±2σ, or ±6σ, respectively.
Our builder, while loading the sleds incurs shifts in the assembly of stones. This is universal to all mechanical assemblies, and is known as Assembly Shift. Assembly shift accounts for the freedom parts have to move from their nominal locations due to the clearance between mating internal and external features at assembly.
The evaluation of the standard deviation allows the engineer to evaluate the "Percentage defects" incurred for an assumed gap size. Using this, the Parts Per Million failure can be found. This article however does not delve into this evaluation and will be discussed in subsequent articles. Please refer to the references for material that explains this in great detail.
WOW! That was fun! While the Worst Case Tolerance Stack-up analysis gives us extremely essential information, it is however extremely conservative and at times an overkill to design based only on it. This is due to the fact that the variations incurred in manufacturing processes are modeled as Normal distributions.
Gallas Label & Decal. 6559 North Avondale Avenue. Chicago, Illinois 60631 o. 773.775.1000 f. 773.775.1001 www.GallasLabel.com.
4. Next, Positive dimensions are indicated by placing a “+” sign adjacent to the dimension value and Negative dimensions are indicated by placing a "-" sign adjacent to the dimension value.
Product Design Engineer | GD&T | 1D, 2D & 3D Tolerance stackup analysis | 3DCS | Vismockup | VIS VSA | CETOL | NX | CATIA |Geometric Assurance |
InsertEnd Mill Cutter
Before we delve into performing tolerance stack-up analysis, it is essential to understand the popular tolerance formats that occur in design specifications.
Well, there you have it! Now you have access to a step-by-step procedure to perform to perform Linear Tolerance analysis in 1D.
1. Select the distance (gap or interference) whose variation is to be determined and label one end of the distance as A and the other end as B as shown below
6 days ago — SFM definition: surface feet per minute | Meaning, pronunciation, translations and examples.
2.Take each tolerance value, (the absolute value) and square it. Place this value in the Statistical Tolerance or Squared Tolerance Column next to each tolerance. Sum up the Squared Tolerances column as before.
Special thanks to Jeff Hall and Evan Jackson, without whom I would have never been introduced to this beautiful art and science. They went out of their way to teach and train me, all while being extremely patient with me. Thank you gentleman. I would not have been the engineer I am today without your support.
Once again, this article is not a comprehensive guide for tolerance stack-up analysis and the material presented in the reference section are highly recommended for an in-depth understanding. What this article does provide, is a quick and easy, step-by-step procedure to perform linear tolerance stack-up analysis on a 1D stack-up.
Oct 20, 2021 — Tungsten. This is hailed as the strongest and toughest naturally occurring metal for its ultimate tensile strength of 250,000 psi or 1725 MPa.
The technique that will be presented subsequently and used by our friend the builder requires all dimensions to be converted into an Equal Bilaterally Toleranced Dimension.
I pray that this was as enjoyable to you to read as it was for me to write. Please comment your thoughts and share it with your friends if you liked it.
. Please enter the desired qty for the material(s) you want to include in your promotion or Proceed Without Promotion and only your base materials will be added to the cart.
Milling inserttypes
New TCMT21.51 Carbide Inserts 10 Pcs/Box - Black Soild Insert TCMT 21.51 - Amazon.com.
3. Begin building a "dimensional loop" starting from Points A or B. In this case, we start from A. The objective of this loop is to form a path of dimensions of features/parts in direct contact with one another. Note, it is very important to form a continuous path.
ToolHub: Specialist B2B distributor of tools and hardware | Thousands of products across Power Tools, Power Tool Accessories, Hand Tools, ...
What a great beginners guide for stackup analysis. I would ask you: is there an explanation for using Equal Bilaterally Toleranced Dimension over unequal ones? We usually encounter many technical drawings with the latter format than the former one. I am trying to find the meaning of this conversion. Thanks in advance
6. Now all the dimensions and tolerances are entered into a chart and totaled for reporting purposes. Place each positive dimension value in the positive column on a separate line. Place each negative dimension value in the negative column on a separate line. Place the tolerance value for each dimension in the tolerance column adjacent to each dimension.
Hence, to incorporate assembly shift, add the shift as +- Value to the tolerance column without any dimension value. Proceed as usual after that.
Solid carbide 3 flute fine pitch rougher high helix uncoated. End Mills are made in the USA. Hardness. Feed Per Tooth. Material. Bhn SFM 1/8dia ¼ ...
Milling insertspecification
Note: If it is desired to take a slightly more conservative approach, multiply the RSS tolerance by an adjustment factor (such as 1.5 for example), substituting the larger adjusted RSS value for the RSS value. Hence in this example, 1.5 x RSS = 4.109. The corresponding gap = 21+-4.109
As a continuation to Part one, this article discusses step-by-step procedures for the two major types of tolerance stack-up analysis:
2. Equal Bilaterally Toleranced Dimension: Specifies a nominal value and the amount a dimension may deviate from nominal. The tolerance values are equal in each direction.
The family of companies to which Palmetto State Armory belongs includes: DC Machine in Summerville, SC; Ferrous Engineering in West Columbia, SC; Special Tool ...
3. Take the square root of the sum of statistical tolerances (RSS). Enter this result at the bottom of the chart. This is the RSS Tolerance Value.
ACME General Purpose Thread Design Calculator 8.375 4THD ACME - Free download as PDF File (.pdf), Text File (.txt) or read online for free.
Long edgemillingcutter
Assembly shift is added to the tolerance stack-up as a line item without a sign or direction, as it allows the parts to shift in both the positive and negative directions, similar to an equal-bilateral tolerance.
2. Determine the Positive and Negative Directions for the dimensions. The positive direction is the direction from point A to point B.
One of the most fundamental operations performed on any machined part is creating a smooth workpiece surface through face milling. Kennametal indexable face milling inserts and bodies are the ideal tooling system for the perpendicular cutting of flat surfaces in a variety of materials. Our face milling platform features different sizes, cutting edges, and precision grades. Regardless of your application, you can trust the quality and designs of Kennametal indexable face mills to get the job done.
ToolInserts
Welcome back dear reader. I take it that you obtained a brief background to the marvelous art and science of Tolerance Stack-up Analysis, and to our friendly prehistoric builder from part one of this article.
As a Recap of part one of this article, the prehistoric builder is faced with a conundrum of estimating the potential "gap" or "interference" between the last stone and the wall of the wooden sled. This problem is particularly tricky for him as he has a number of stones and sleds and clearly cannot evaluate each case by trial and error.
In the recent future, I will share some tips and tricks that I happened to pick up during my internship that pertained to tolerance stack-up analyses.
Like all things in life, the art and science of Tolerance Stack-up analysis takes practice. I too am in the process of getting better at it every day. The process is often performed on a spread-sheet to have quick and easy calculations, yet the algorithm for the process remains the same.
8. Subtract the negative total from the positive total. This gives the nominal dimension or distance. In cases where all the dimensions and tolerances in the chain were not originally in equal-bilateral format this value will probably be different than the distance that is measured directly from a drawing, CAD model, or what our builder estimated.
Helical supplies comprehensive speeds and feeds charts for every product in its catalog. View charts by clicking the Speeds & Feeds tab on each product table.
9. Apply the total tolerance. Adding and subtracting the tolerance from the nominal dimension gives the maximum and minimum distance values. Hence, the Gap: Worst Case Maximum = 21+5 = 26; and the Worst Case Minimum = 21-5 = 16.
 18581906093